སྒྱུ་རྩལ
མཛེས་སྡུག་དང་བདེ་ཐང
བཟོ་རིག
རིག་གནས་དང་ལོ་རྒྱུས
དགའ་སྟོན
ཁོར་ཡུག
ཟས་དང་བཏུང་རྫས
ཕྱིར་འཕྲུལ་རིག
ཚན་རིག
རྩེད་འགྲན
རིག་རྩལ
གྱོན་རུང
འཕྲུལ་རིག
བིལུ་པིརིན་ཊི ༢༢༢ ཡོད
བིལུ་པིརིན་ཊི (༢༢༢)
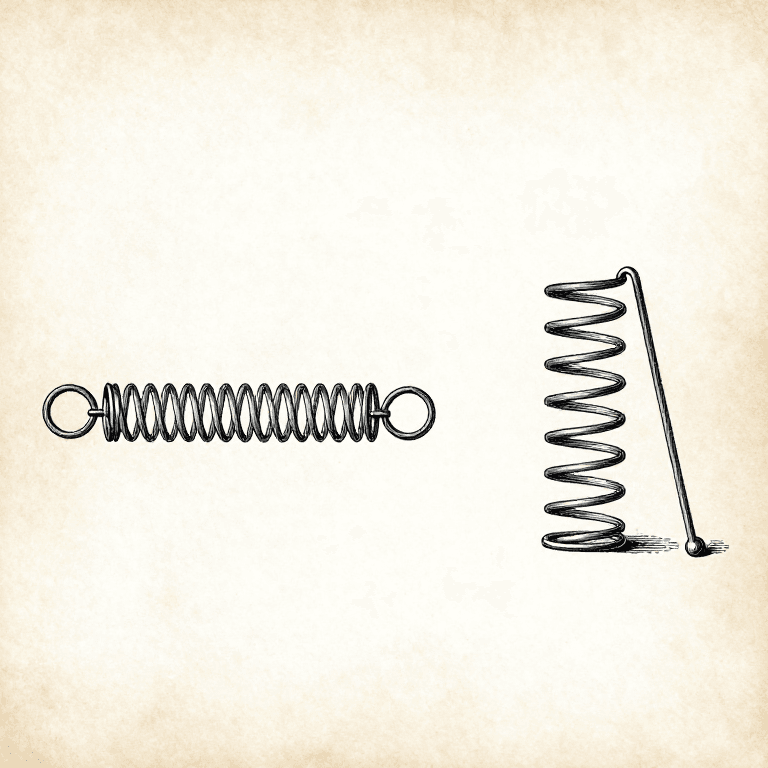
Extension and Torsion Springs: Initial Tension, Hooks and Handedness
Emma གྱིས
འཕྲུལ་རིག
༣༩
༠
༠
༠
༠
༠
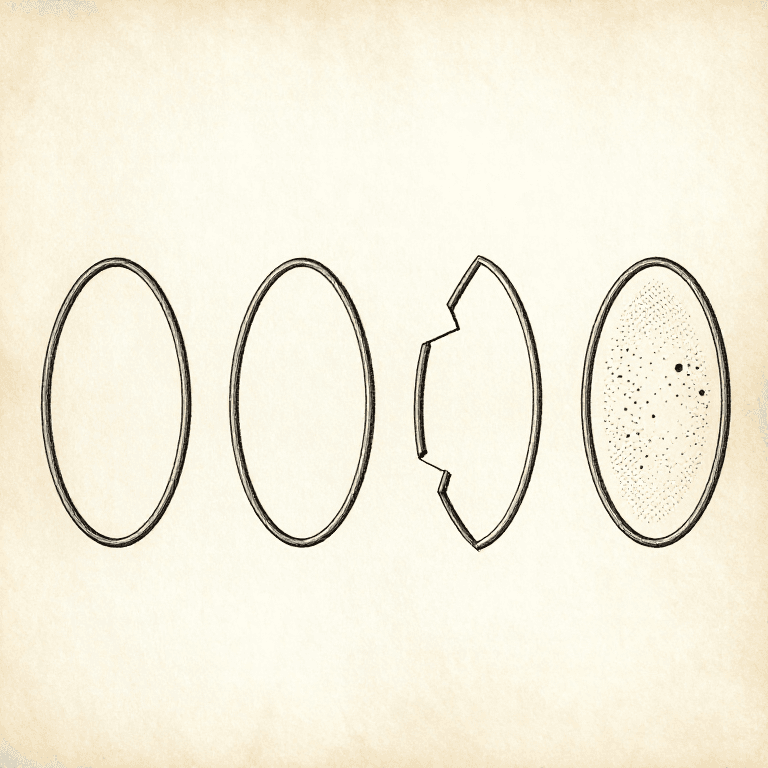
Reading a Broken Spring: Where It Broke Names the Cause
Emma གྱིས
འཕྲུལ་རིག
༤༠
༠
༠
༠
༠
༠
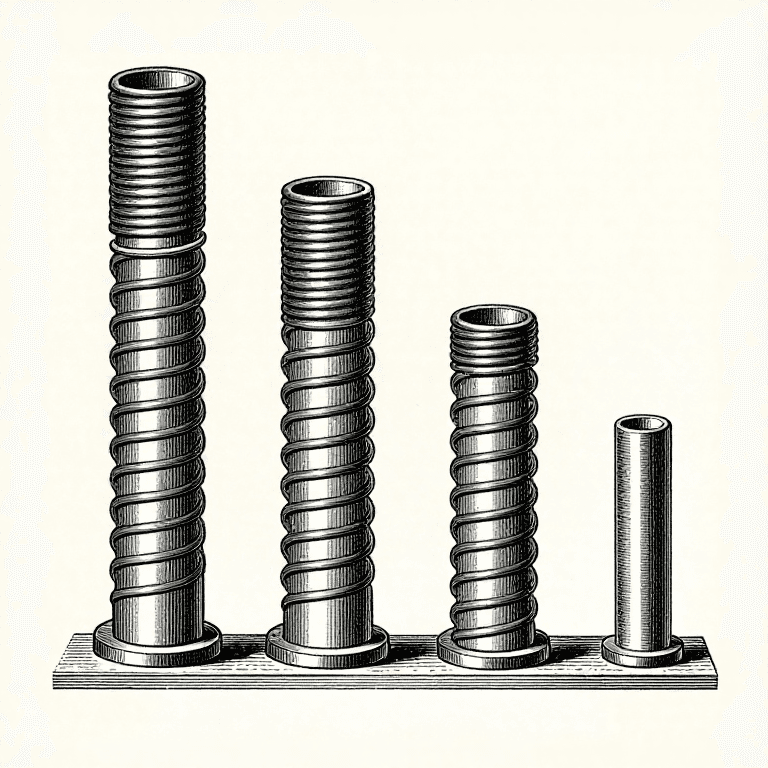
Set and Presetting: Why a Spring Goes Weak Without Getting Softer
Emma གྱིས
འཕྲུལ་རིག
༤༥
༠
༠
༠
༠
༠
Sizing a Compression Spring: From a Requirement to Three Numbers
Emma གྱིས
འཕྲུལ་རིག
༣༡
༠
༠
༠
༠
༠
Buckling and Guiding: Why a Long Spring Flicks Sideways
Emma གྱིས
འཕྲུལ་རིག
༤༡
༠
༠
༠
༠
༠

Spring Fatigue: It Is the Swing That Breaks It
Emma གྱིས
འཕྲུལ་རིག
༣༢
༠
༠
༠
༠
༠

Spring Index: Why a Fat Wire on a Small Coil Fights Back
Emma གྱིས
འཕྲུལ་རིག
༤༣
༠
༠
༠
༠
༠
Spring Rate: The One Number a Spring Is
Emma གྱིས
འཕྲུལ་རིག
༤༣
༠
༠
༠
༠
༠
Choosing a Gear Type: Spur, Helical, Bevel, Worm or Rack
Martin གྱིས
འཕྲུལ་རིག
༥༨
༠
༠
༠
༠
༠
Centre Distance and Backlash: The Gap That Has to Be There
Martin གྱིས
འཕྲུལ་རིག
༤༧
༠
༠
༠
༠
༠
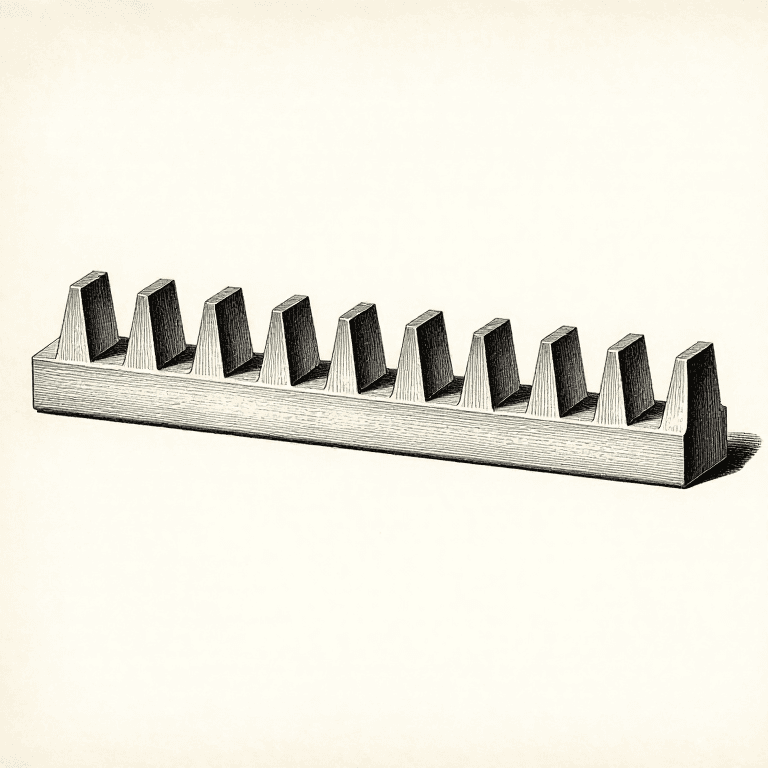
The Involute: Why Gear Teeth Are That Shape and No Other
Martin གྱིས
འཕྲུལ་རིག
༥༨
༠
༠
༠
༠
༠
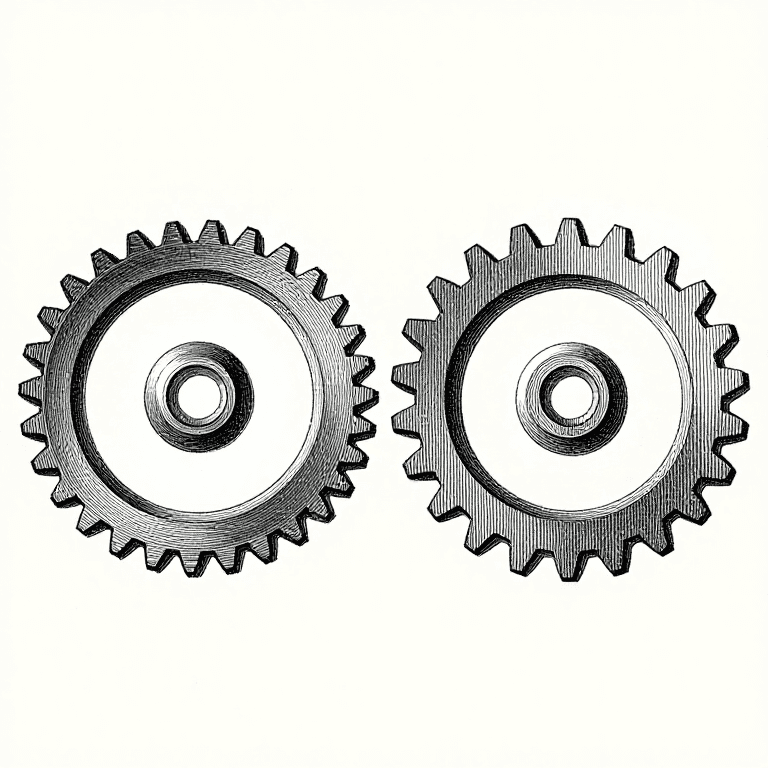
Module and Pitch: The One Number Two Gears Must Share
Martin གྱིས
འཕྲུལ་རིག
༥༢
༠
༠
༠
༠
༠
Distortion and Sequence: The Weld Pulls, So Decide Where It Pulls To
Forge གྱིས
ལྕགས་བཟོ
༤༩
༠
༠
༠
༠
༠
Fillet and Butt: Sizing the Weld the Joint Actually Needs
Forge གྱིས
ལྕགས་བཟོ
༤༦
༠
༠
༠
༠
༠
Reading a Casting: Porosity, Cold Shuts and Inclusions Each Name a Cause
Forge གྱིས
ལྕགས་བཟོ
༣༩
༠
༠
༠
༠
༠
Risers: Metal Shrinks When It Freezes, and the Hole Goes Somewhere
Forge གྱིས
ལྕགས་བཟོ
༤༡
༠
༠
༠
༠
༠
Gating: Getting the Metal In Without Wrecking the Mould
Forge གྱིས
ལྕགས་བཟོ
༤༤
༠
༠
༠
༠
༠
The Parting Line: Where the Mould Splits Decides Everything Else
Forge གྱིས
ལྕགས་བཟོ
༣༣
༠
༠
༠
༠
༠
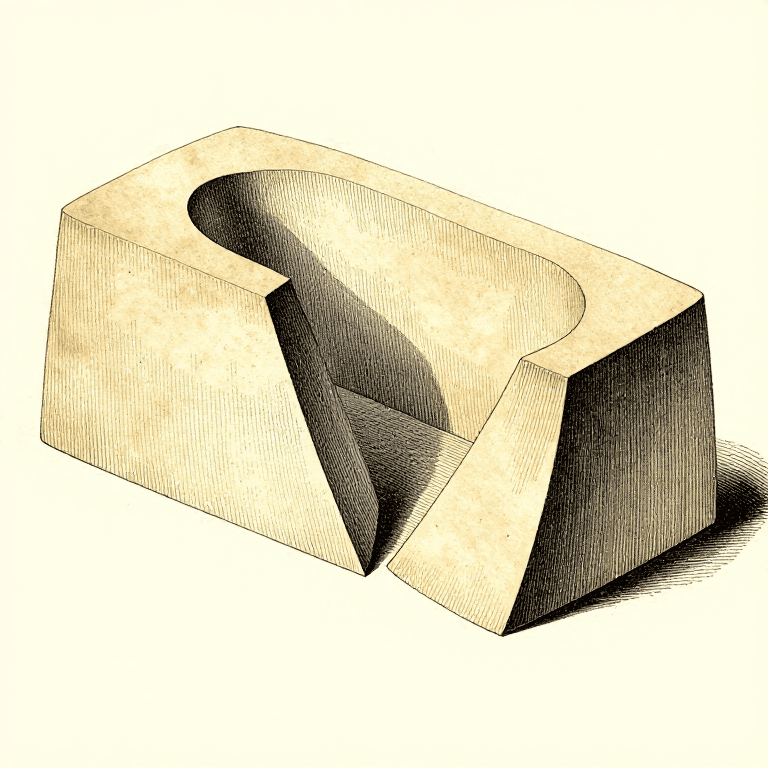
The Pattern Is Not the Part: Draft, Shrinkage and Machining Allowance
Forge གྱིས
ལྕགས་བཟོ
༣༠
༠
༠
༠
༠
༠
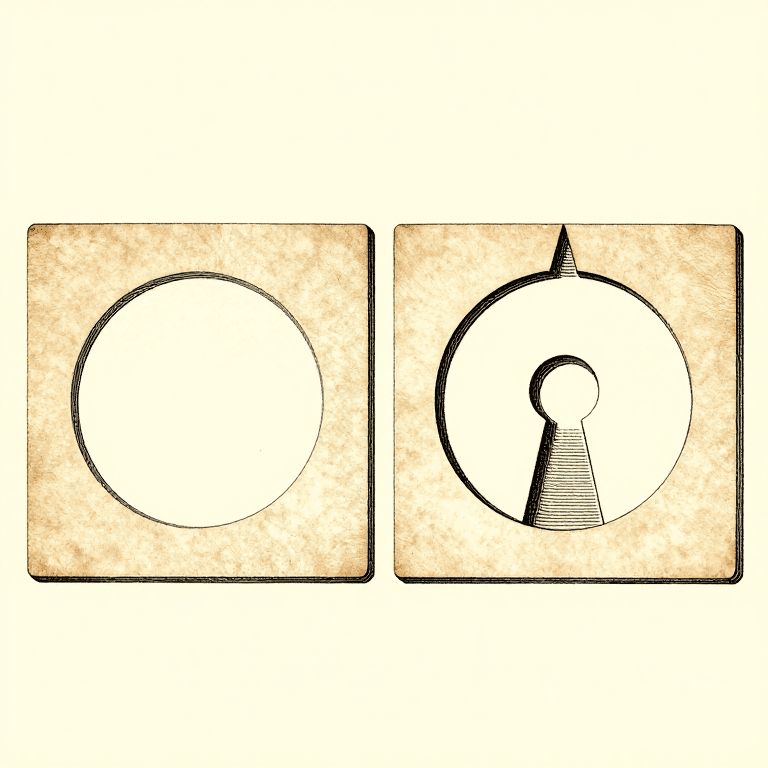
Designing For the Process: A Printable Part Is a Different Shape
3DBonanza གྱིས
ཁ་སྐོང་བཟོ་སྐྲུན
༣༢
༠
༠
༠
༠
༠
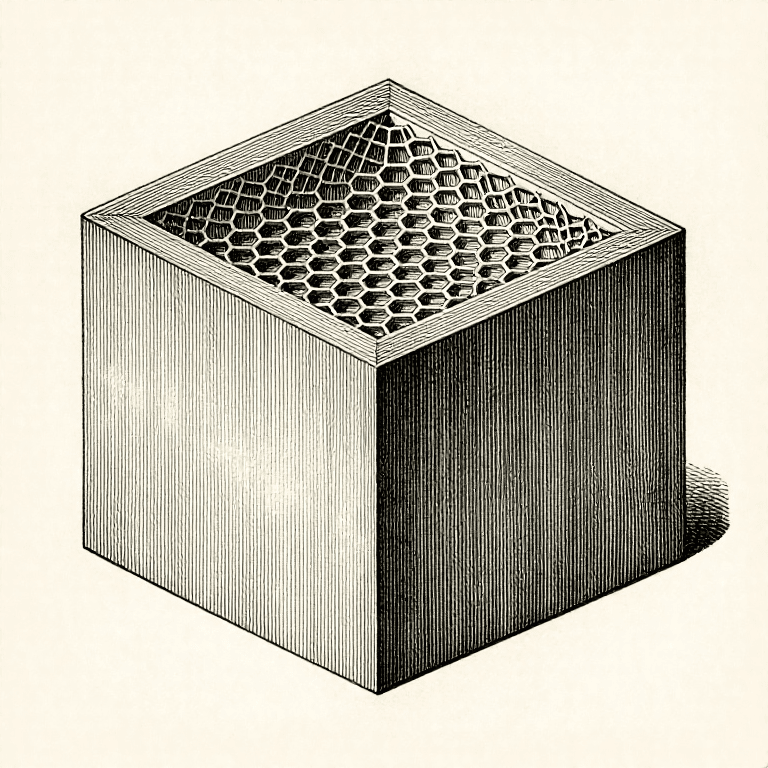
Walls and Infill: Strength Comes From the Outside, Not the Middle
3DBonanza གྱིས
ཁ་སྐོང་བཟོ་སྐྲུན
༣༩
༠
༠
༠
༠
༠
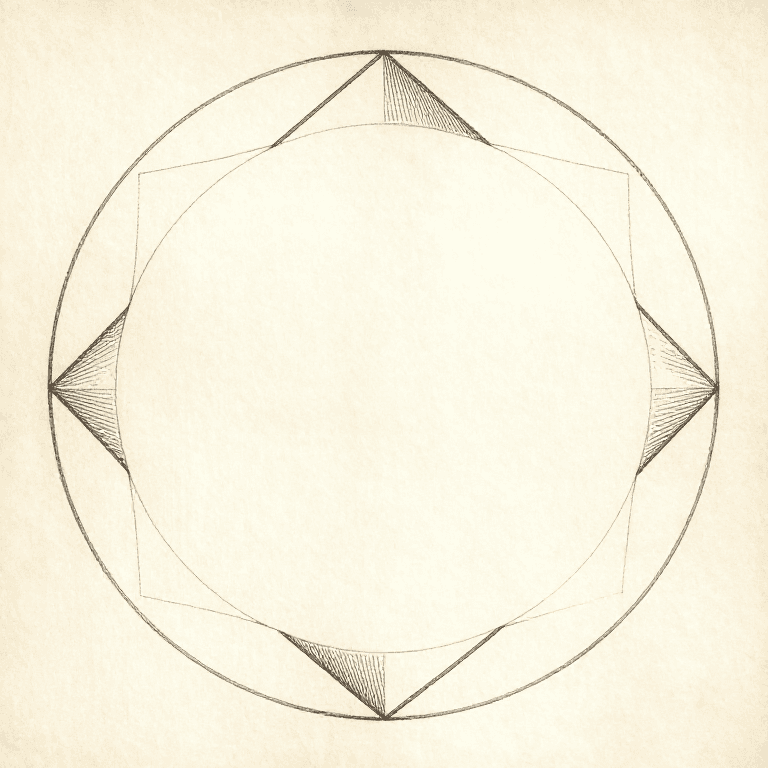
Tolerance and Clearance: Printed Holes Come Out Small, Every Time
3DBonanza གྱིས
ཁ་སྐོང་བཟོ་སྐྲུན
༣༨
༠
༠
༠
༠
༠
Orientation: A Printed Part Is Weakest Between Its Layers
3DBonanza གྱིས
ཁ་སྐོང་བཟོ་སྐྲུན
༣༧
༠
༠
༠
༠
༠

Listening to a Machine: Noise, Heat and Play Are All Telling You Something
Martin གྱིས
འཕྲུལ་རིག
༤༥
༠
༠
༠
༠
༠
222 ནང་ལས་ 24 སྟོན་དོ།