སྒྱུ་རྩལ
མཛེས་སྡུག་དང་བདེ་ཐང
བཟོ་རིག
རིག་གནས་དང་ལོ་རྒྱུས
དགའ་སྟོན
ཁོར་ཡུག
ཟས་དང་བཏུང་རྫས
ཕྱིར་འཕྲུལ་རིག
ཚན་རིག
རྩེད་འགྲན
རིག་རྩལ
གྱོན་རུང
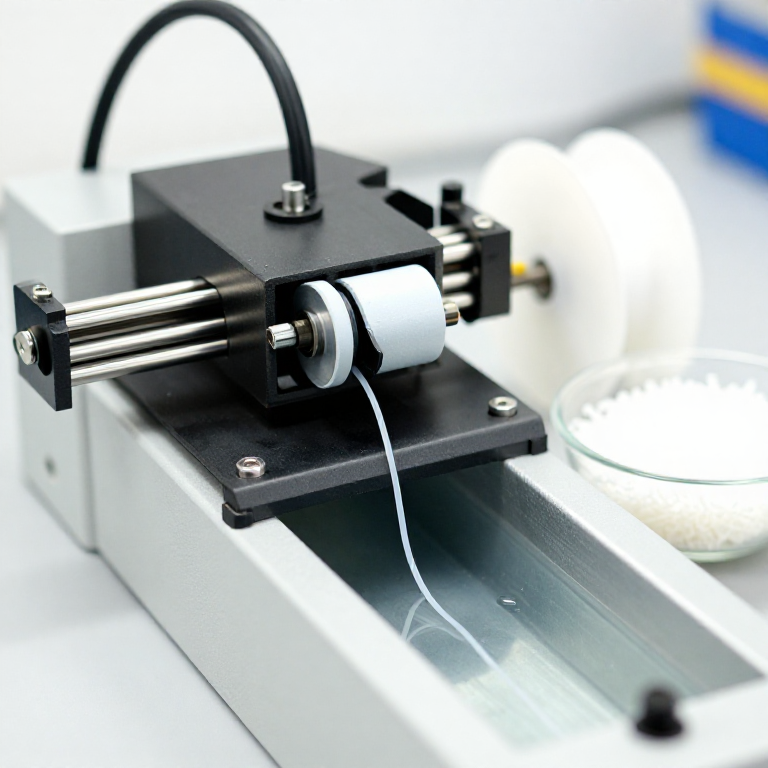

3D Printer Filament Extruded from Pellets
Filament is made the way a 3D printer prints, only continuously: dry plastic pellets fall from a hopper onto a turning screw inside a heated barrel, melt as they are carried forward, and are pushed out through a round nozzle. The strand is cooled in air or a water bath, drawn by a puller at a steady speed so it keeps its diameter, and wound on a spool. Commercial 1.75 mm filament is typically held to about ±0.02 mm; a small line should be measured.
PETG and many other plastics take up moisture, which makes bubbles and weak prints: makers dry PETG at about 55–70 °C for 5–8 hours, depending on the resin. Melt temperatures follow the resin's datasheet; PETG is usually printed at about 230–260 °C.
བར་མ
A day per few kilograms
ལམ་སྟོན
1
1
Dry the pellets
Dry the pellets
Dry the pellets in a dryer as the resin maker specifies; for PETG about 55–70 °C for 5–8 hours.
གོམ་པ་འདིའི་རྫས་རིགས:
 PETG རིལ་བུ2 kg
 སྐྱེ་ལྡན་ཐིམ་བཏུབ་པའི་པ་ལས་ཊིག་གི་ཐིག་གུ། (PLA)2 kg
 ABS རིལ་བུ2 kg
ལག་ཆས་དགོས་མཁོ:
 རིལ་བུ་སྐམ་ཆས།
 ཨང་རྟགས་ཐབ་ཚང་སྲང་།
2
2
Heat the barrel
Heat the barrel
Set the barrel's heating zones to rise from the hopper end to the nozzle within the resin's datasheet range and let them settle.
ལག་ཆས་དགོས་མཁོ:
 གཟེར་གཅིག་གི་འཐེན་འཕྲུལ་སྦུག
 རིལ་བུ་སྟེར་བའི་ཁུག་མ་
3
3
Extrude
Extrude
Fill the hopper and start the screw slowly. Purge until the strand comes out clear of old material and bubbles.
ལག་ཆས་དགོས་མཁོ:
གཟེར་གཅིག་གི་འཐེན་འཕྲུལ་སྦུགརིལ་བུ་སྟེར་བའི་ཁུག་མ་ ཚ་བཟོད་ཀྱི་ལག་ཤུབས།
 ཉེན་སྲུང་མིག་ཤེལ།
4
4
Cool and pull
Cool and pull
Lead the strand through a water bath or past the fan to the puller. Adjust the puller's speed: faster pulls the strand thinner, slower lets it swell.
གོམ་པ་འདིའི་རྫས་རིགས:
 ཆུ།50 ལི་ཊར།
ལག་ཆས་དགོས་མཁོ:
 པ་ལས་ཊིཀ་གི་ཟོ་སྦོམ་ ལི་ཊར་ ༡༠༠
 སྒྲོམ་གྱི་རླུང་འཁོར། (མགྱོགས་ཚད་འགྱུར་བཏུབ)
 སྐུད་པ་འཐེན་ཆས་དང་དཀྲིས་ཆས།
5
5
Measure and wind
Measure and wind
Measure the diameter every few metres and wind the filament on a spool. Keep it sealed and dry.
ལག་ཆས་དགོས་མཁོ:
 ཨང་རྟགས་ཚད་འཇལ་ཆས་ ཨིནཅི 6སྐུད་པ་འཐེན་ཆས་དང་དཀྲིས་ཆས།ཨང་རྟགས་ཐབ་ཚང་སྲང་།
6
6
Troubleshooting
Troubleshooting
Filament extrusion troubleshooting.
Flow
Loading...
རྫས་རིགས
4- 2 kgས་ཆ་འཛིན
- ས་ཆ་འཛིན
- 2 kgས་ཆ་འཛིན
- 50 ལི་ཊར།ས་ཆ་འཛིན
ལག་ཆས་དགོས་མཁོ
10- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
བིལུ་པིརིན་ཊི་འདི་གིས་བཟོ་མི



CC0 སྤྱི་དབང
བིལུ་པིརིན་ཊི་འདི་CC0 འོག་བཀྲམས་ཡོད། ཁྱེད་རང་གིས་ཆོག་མཆན་མ་བཞེས་པར་ཕབ་ལེན་དང་བཟོ་བཅོས། བགོ་བཤའ། དགོས་མཁོ་གང་ལའང་བཀོལ་སྤྱོད་བྱས་ཆོག
བཟོ་མཁན་ལ་རྒྱབ་སྐྱོར་བྱེད་པའི་ཆེད་ཁོང་ཚོའི་བིལུ་པིརིན་ཊི་བརྒྱུད་ཐོན་སྐྱེད་ཉོ། བཟོ་མཁན་གྱིས བཟོ་མཁན་གྱི་ཁེ་ཕོགས ཚོང་པས་གཏན་འཁེལ་བྱས་པ། ཡང་ན་བིལུ་པིརིན་ཊི་འདིའི་པར་གསར་བཟོས་ཏེ་ཁྱེད་རང་གི་བིལུ་པིརིན་ཊི་ནང་མཐུད་སྦྲེལ་བྱས་ཏེ་ཡོང་སྒོ་བགོ་བཤའ་བྱེད།