སྒྱུ་རྩལ
མཛེས་སྡུག་དང་བདེ་ཐང
བཟོ་རིག
རིག་གནས་དང་ལོ་རྒྱུས
དགའ་སྟོན
ཁོར་ཡུག
ཟས་དང་བཏུང་རྫས
ཕྱིར་འཕྲུལ་རིག
ཚན་རིག
རྩེད་འགྲན
རིག་རྩལ
གྱོན་རུང

Speeds, Feeds, and What the Chip Is Telling You
Every cutting tool has a speed at which it works and a speed at which it dies, and the difference between them is often a factor of two. Run high-speed steel at carbide speeds and it will be blunt in seconds; run carbide at high-speed-steel speeds and it will chip because it never gets hot enough to cut properly.
The number that matters is not the spindle's revolutions but the SURFACE SPEED — how fast the metal passes the cutting edge. That depends on diameter, so the same tool on the same machine needs a different spindle speed for every size of work, and a part whose diameter changes needs the speed changed with it.
The arithmetic is one formula. The judgement is reading the chip, which tells you what is really happening at the edge where you cannot see.
བར་མ
3 hours
ལམ་སྟོན
1
1
One formula, and the reason it has a diameter in it
One formula, and the reason it has a diameter in it
Jupyter ཚང་དེབ་མངོན་གསལ་འབད་དོ་…
ལག་ཆས་དགོས་མཁོ:
 ལྕགས་ཀྱི་འཁྲུལ་འཁོར།
 རྩིས་འཕྲུལ།
 ཟིན་དེབ།
2
2
Feed decides the finish, not depth of cut
Feed decides the finish, not depth of cut
Jupyter ཚང་དེབ་མངོན་གསལ་འབད་དོ་…
ལག་ཆས་དགོས་མཁོ:
ལྕགས་ཀྱི་འཁྲུལ་འཁོར།རྩིས་འཕྲུལ།3
3
Read the chip
Read the chip
Stop and look at what is coming off. The chip is the only direct report you get from the cutting edge, and it is unambiguous once you know the vocabulary.
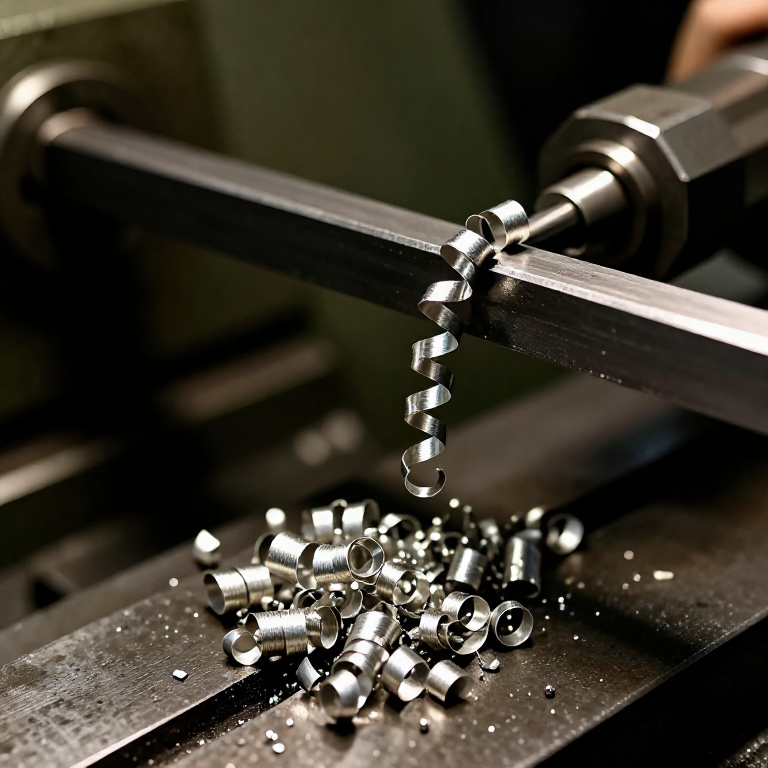
SHORT TIGHT CURLS, warm and silver-grey: correct. LONG STRINGY RIBBONS that wrap the work: feed too light or no chipbreaker, and dangerous — they are razor-sharp and they will grab. DARK BLUE OR STRAW chips: the cut is running hot, speed too high for the tool, and on HSS you are minutes from a blunt edge. DUST rather than chips on steel: the tool is already blunt and rubbing.
A chip that changes colour part way through a job is telling you the tool is wearing, not that the metal changed. Listen too: a steady hiss is a cut, a rhythmic chatter is the tool or work springing and needs less stick-out, a slower speed or a smaller nose radius.
གོམ་པ་འདིའི་རྫས་རིགས:
 ལྕགས་འཇམ་གྱི་ལྕགས་ཕྲེང་སྒོར་སྒོརམ།1 དུམ་བུ།
ལག་ཆས་དགོས་མཁོ:
ལྕགས་ཀྱི་འཁྲུལ་འཁོར། འཁོར་འཕྲུལ་ལག་ཆས་ཆ་ཚང་། (HSS)
 ཉེན་སྲུང་མིག་ཤེལ།ཟིན་དེབ།
4
4
Cutting fluid, and when it does harm
Cutting fluid, and when it does harm
Flood steel generously with cutting oil. It cools the edge, floats the chip out of the cut and stops material welding to the tool, and it buys a large multiple of tool life on stainless in particular.
Cast iron is cut DRY. Its graphite lubricates the cut by itself, and fluid turns the fine dusty swarf into an abrasive paste that gets into the slideways and wears the machine.
The one rule that matters with carbide: apply fluid steadily or not at all. An intermittent squirt onto a hot carbide tip thermally shocks it and cracks the edge, and a cracked tip fails suddenly rather than gradually. Aluminium wants something to stop it welding to the tool — paraffin or a dedicated aluminium cut fluid works where general cutting oil is indifferent.
གོམ་པ་འདིའི་རྫས་རིགས:
 གཏུབ་སྣུམ།1 དུམ་བུ།
ལག་ཆས་དགོས་མཁོ:
ལྕགས་ཀྱི་འཁྲུལ་འཁོར།འཁོར་འཕྲུལ་ལག་ཆས་ཆ་ཚང་། (HSS)5
5
Write down what worked
Write down what worked
Keep a page per material: tool, diameter, spindle speed, feed, depth of cut, and one word about the chip and the finish. It takes fifteen seconds at the end of a job.
Published cutting-speed tables are a STARTING POINT computed for industrial machines with rigid setups and plenty of power. A small lathe on a bench will often chatter at the book figure and be perfectly happy at two thirds of it. What you actually want is a table for YOUR machine.
After a dozen jobs you will stop calculating for the common cases, which is the point: the formula is how you handle the unfamiliar material, and the notebook is how you stop re-deriving the familiar ones.
ལག་ཆས་དགོས་མཁོ:
ཟིན་དེབ།རྩིས་འཕྲུལ།རྫས་རིགས
2- 1 དུམ་བུ།ས་ཆ་འཛིན
- 1 དུམ་བུ།ས་ཆ་འཛིན
འབྲེལ་ཡོད་བིལུ་པིརིན་ཊི
བིལུ་པིརིན་ཊི་འདི་ཚུ་ཐབས་ལམ་དང་རྫས་རིགས། སྤྱི་ཆོས་བགོ་བཤའ་བྱེད



CC0 སྤྱི་དབང
བིལུ་པིརིན་ཊི་འདི་CC0 འོག་བཀྲམས་ཡོད། ཁྱེད་རང་གིས་ཆོག་མཆན་མ་བཞེས་པར་ཕབ་ལེན་དང་བཟོ་བཅོས། བགོ་བཤའ། དགོས་མཁོ་གང་ལའང་བཀོལ་སྤྱོད་བྱས་ཆོག
བཟོ་མཁན་ལ་རྒྱབ་སྐྱོར་བྱེད་པའི་ཆེད་ཁོང་ཚོའི་བིལུ་པིརིན་ཊི་བརྒྱུད་ཐོན་སྐྱེད་ཉོ། བཟོ་མཁན་གྱིས བཟོ་མཁན་གྱི་ཁེ་ཕོགས ཚོང་པས་གཏན་འཁེལ་བྱས་པ། ཡང་ན་བིལུ་པིརིན་ཊི་འདིའི་པར་གསར་བཟོས་ཏེ་ཁྱེད་རང་གི་བིལུ་པིརིན་ཊི་ནང་མཐུད་སྦྲེལ་བྱས་ཏེ་ཡོང་སྒོ་བགོ་བཤའ་བྱེད།