སྒྱུ་རྩལ
མཛེས་སྡུག་དང་བདེ་ཐང
བཟོ་རིག
རིག་གནས་དང་ལོ་རྒྱུས
དགའ་སྟོན
ཁོར་ཡུག
ཟས་དང་བཏུང་རྫས
ཕྱིར་འཕྲུལ་རིག
ཚན་རིག
རྩེད་འགྲན
རིག་རྩལ
གྱོན་རུང
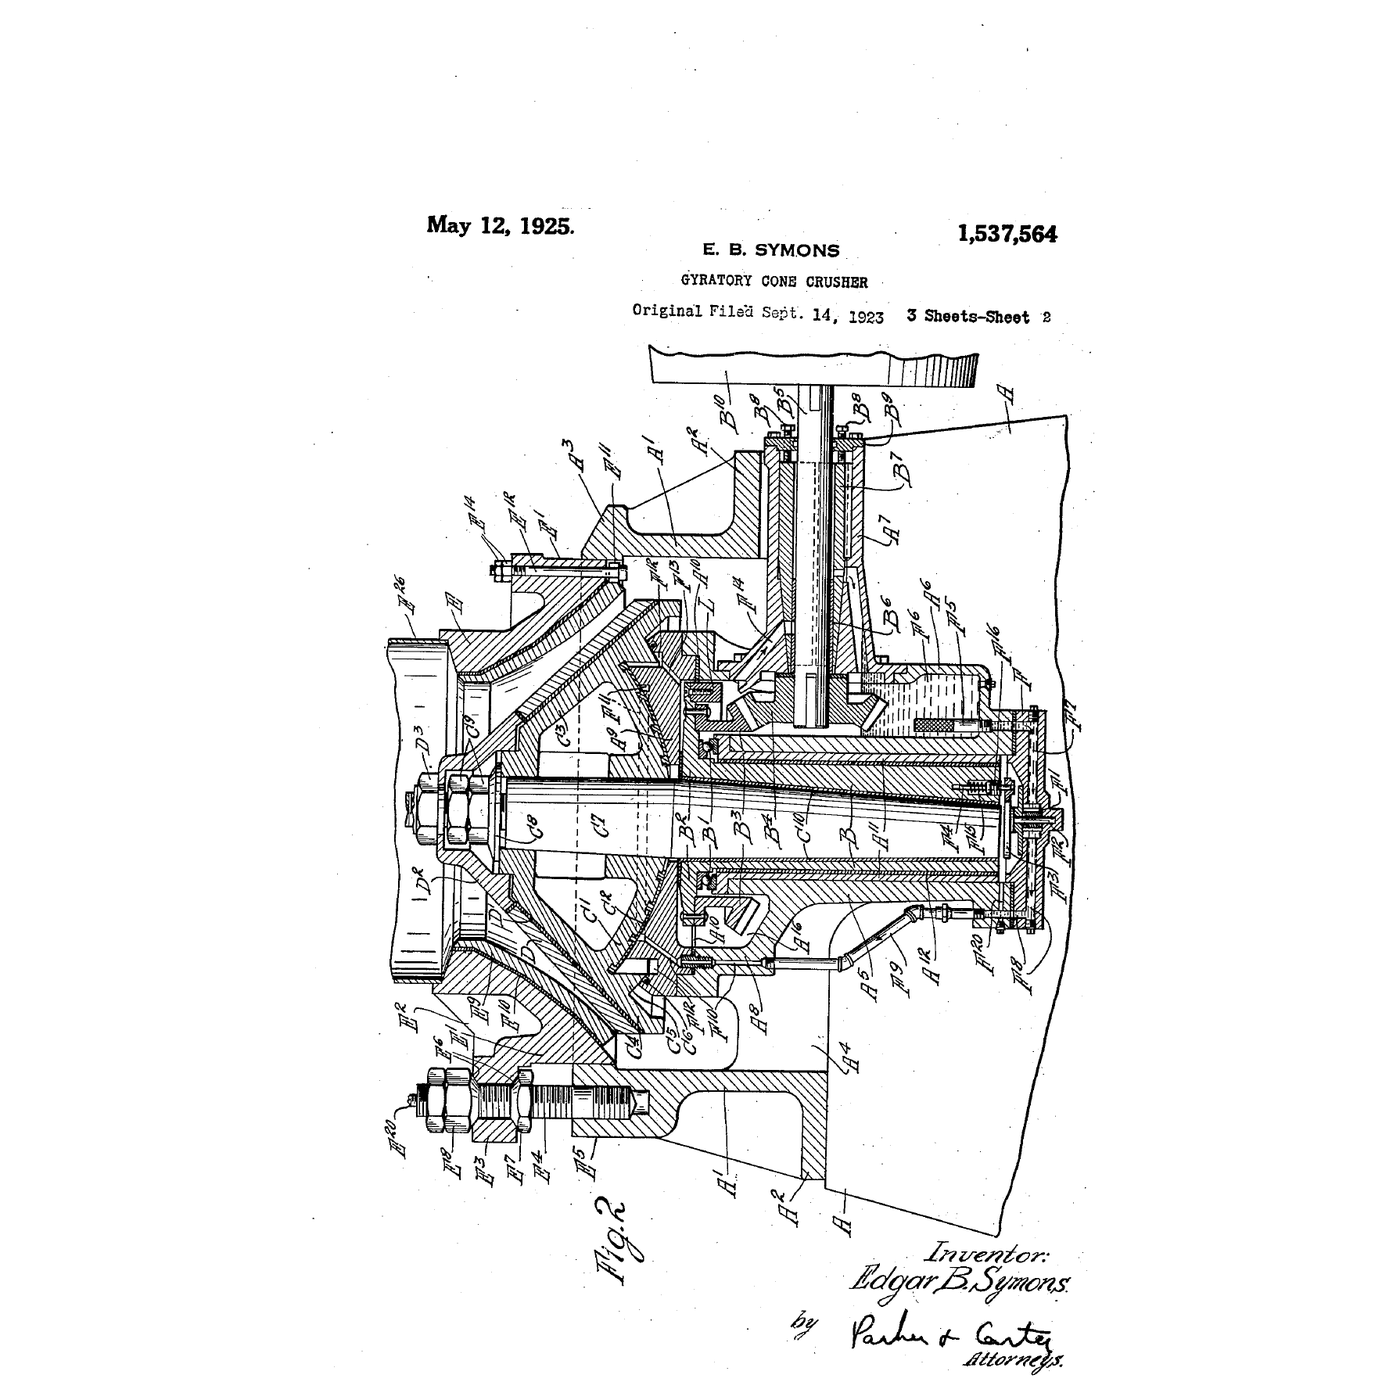

The Cone Crusher: A Parallel Zone Nothing Gets Past
A gyratory crusher's chamber narrows all the way to the bottom. A stone that arrives at the discharge on the open side of the cycle falls straight out, and whether any particular stone got squeezed is partly luck.
Edgar Symons' answer was to stop the chamber narrowing. The last stretch above the discharge is **parallel** — mantle and concave the same distance apart for a hand's breadth or more — so nothing can cross it without the gap closing on it. At normal running speeds every particle is caught three to five times on the way out.
That is the difference between a machine that reduces stone and a machine that makes a product to a specification. This rung works out how many squeezes the parallel zone actually delivers, why a full chamber crushes differently from an empty one, and what choke feeding does to the liner bill.
མཐོ་རིམ
About 3 hours
ལམ་སྟོན
1
1
See the difference between a converging chamber and a parallel one
See the difference between a converging chamber and a parallel one
Two pieces of plate in the vise again, as in the jaw rung — but this time with a step in the geometry.
First, set them converging: wide at the top, narrow at the bottom, meeting at the setting you want. Drop a handful of mixed stone through as you open and close. Sieve what comes out and look at the top size.
Now pack a spacer so the last thirty millimetres of the gap is **parallel** — both plates the same distance apart over that length — and repeat with the same stone and the same setting.
The second product has a tighter top size. It is the same machine, the same setting, and the only change is that nothing could take a straight run at the exit.
Keep both samples. Look at the shape as well as the size: the parallel-zone product tends to be blockier, because a particle that has been caught several times has had its protruding corners taken off.
གོམ་པ་འདིའི་རྫས་རིགས:
 བསགས་རྡོ།1 ལག་གང་།
 ལྕགས་འཇམ་གྱི་ཤོག་ལེབ་སྟུག།2 དུམ་བུ།
 ལྕགས་ཀྱི་དབྱུག་གུ་རྗེན་མ1 དུམ་བུ།
ལག་ཆས་དགོས་མཁོ:
 ལས་ཅོག་གི་འཛིན་ཆས།
 ཚགས་མ་རྩུབ་མོ།
 དྲ་ཕྲ་བའི་ཚག་མ།
 ཨང་རྟགས་སྲང་།
 ཨང་རྟགས་ཚད་འཇལ་ཆས་ ཨིནཅི 6
 གསལ་བའི་ཉེན་སྲུང་མིག་ཤེལ།
 ཀོ་བའི་ལས་ལག་ཤུབས།
2
2
How many squeezes the parallel zone actually gives
How many squeezes the parallel zone actually gives
Jupyter ཚང་དེབ་མངོན་གསལ་འབད་དོ་…
3
3
Set it, and then check it where it is worn
Set it, and then check it where it is worn
The closed side setting is measured, not read off a dial. The classic method is a piece of soft lead — a fishing weight or a flattened pipe offcut — hung on a wire and dropped through a running chamber, then fished out and measured with calipers. The thickness it has been squeezed to *is* the closed side setting.
Do it in several places round the chamber, not one. Liners wear unevenly — a segregating feed chute will wear one side of a chamber twice as fast as the other — and the setting that matters for your product top size is the **largest** gap anywhere round the circle, not the average one.
Then record it against the hours run. A setting that has to be tightened more often than it used to is a liner approaching the end of its life, and the point at which it should be changed is not when it is worn through but when the parallel zone has worn into a taper. Past that, the machine has quietly turned back into a gyratory and the top size has drifted.
Nothing goes into a running chamber except on a wire, held from outside the guard, by somebody who has done it before.
གོམ་པ་འདིའི་རྫས་རིགས:
 མེན་ག་ནིསི་ལྕགས་ཀྱི་འདྲུད་འཕྲོག་ཤོག་ལེབ།2 དུམ་བུ།
ལག་ཆས་དགོས་མཁོ:
ཨང་རྟགས་ཚད་འཇལ་ཆས་ ཨིནཅི 6 འཇལ་ཐག
 ཐིག་ཤིང་།
 ལག་བཟུང་གི་ཆ་ཚང་ཀོ་བའི་ལས་ལག་ཤུབས།གསལ་བའི་ཉེན་སྲུང་མིག་ཤེལ།
 ཉན་ནུས་སྲུང་སྐྱོབ།
4
4
Choke feed: what changes when the chamber is full
Choke feed: what changes when the chamber is full
Jupyter ཚང་དེབ་མངོན་གསལ་འབད་དོ་…
5
5
Feed it in the middle, and feed it graded
Feed it in the middle, and feed it graded
A cone crusher is fed through a hole in the top of the frame and the material falls onto a distributing plate. Two things about that are easy to get wrong and both are expensive.
**Off-centre feed** loads one side of the chamber. The crushing force is then unbalanced around the head, the eccentric bushing is loaded on one side of its circle, and the liners wear into a taper. On a machine where the whole product specification depends on a parallel zone, that is not cosmetic. Check the feed distribution with the machine stopped and the chamber empty: the heap should be centred and even.
**Segregated feed** is the subtler one. If the material arrives off a conveyor and over a head pulley, the coarse fraction throws further than the fines, so one side of the chamber gets the rock and the other gets the sand. The fines cushion, the rock does the work, and the two sides of the same liner wear at different rates. A feed box that lets the material fall vertically before it enters, or a rotating distributor, is the cure.
Both faults have the same signature: uneven liner wear measured round the circumference. That is why step 3 asks for the setting in several places rather than one.
གོམ་པ་འདིའི་རྫས་རིགས:
བསགས་རྡོ།1 bucket ལྕགས་འཇམ་གྱི་ལེབ་ཤོག1 དུམ་བུ།
ལག་ཆས་དགོས་མཁོ:
འཇལ་ཐག ཆུ་ཚད་འཇལ་ཆས།
 ཁེམ།ཀོ་བའི་ལས་ལག་ཤུབས།གསལ་བའི་ཉེན་སྲུང་མིག་ཤེལ།
 ཐལ་བའི་ཁ་རས།
6
6
History and context
History and context
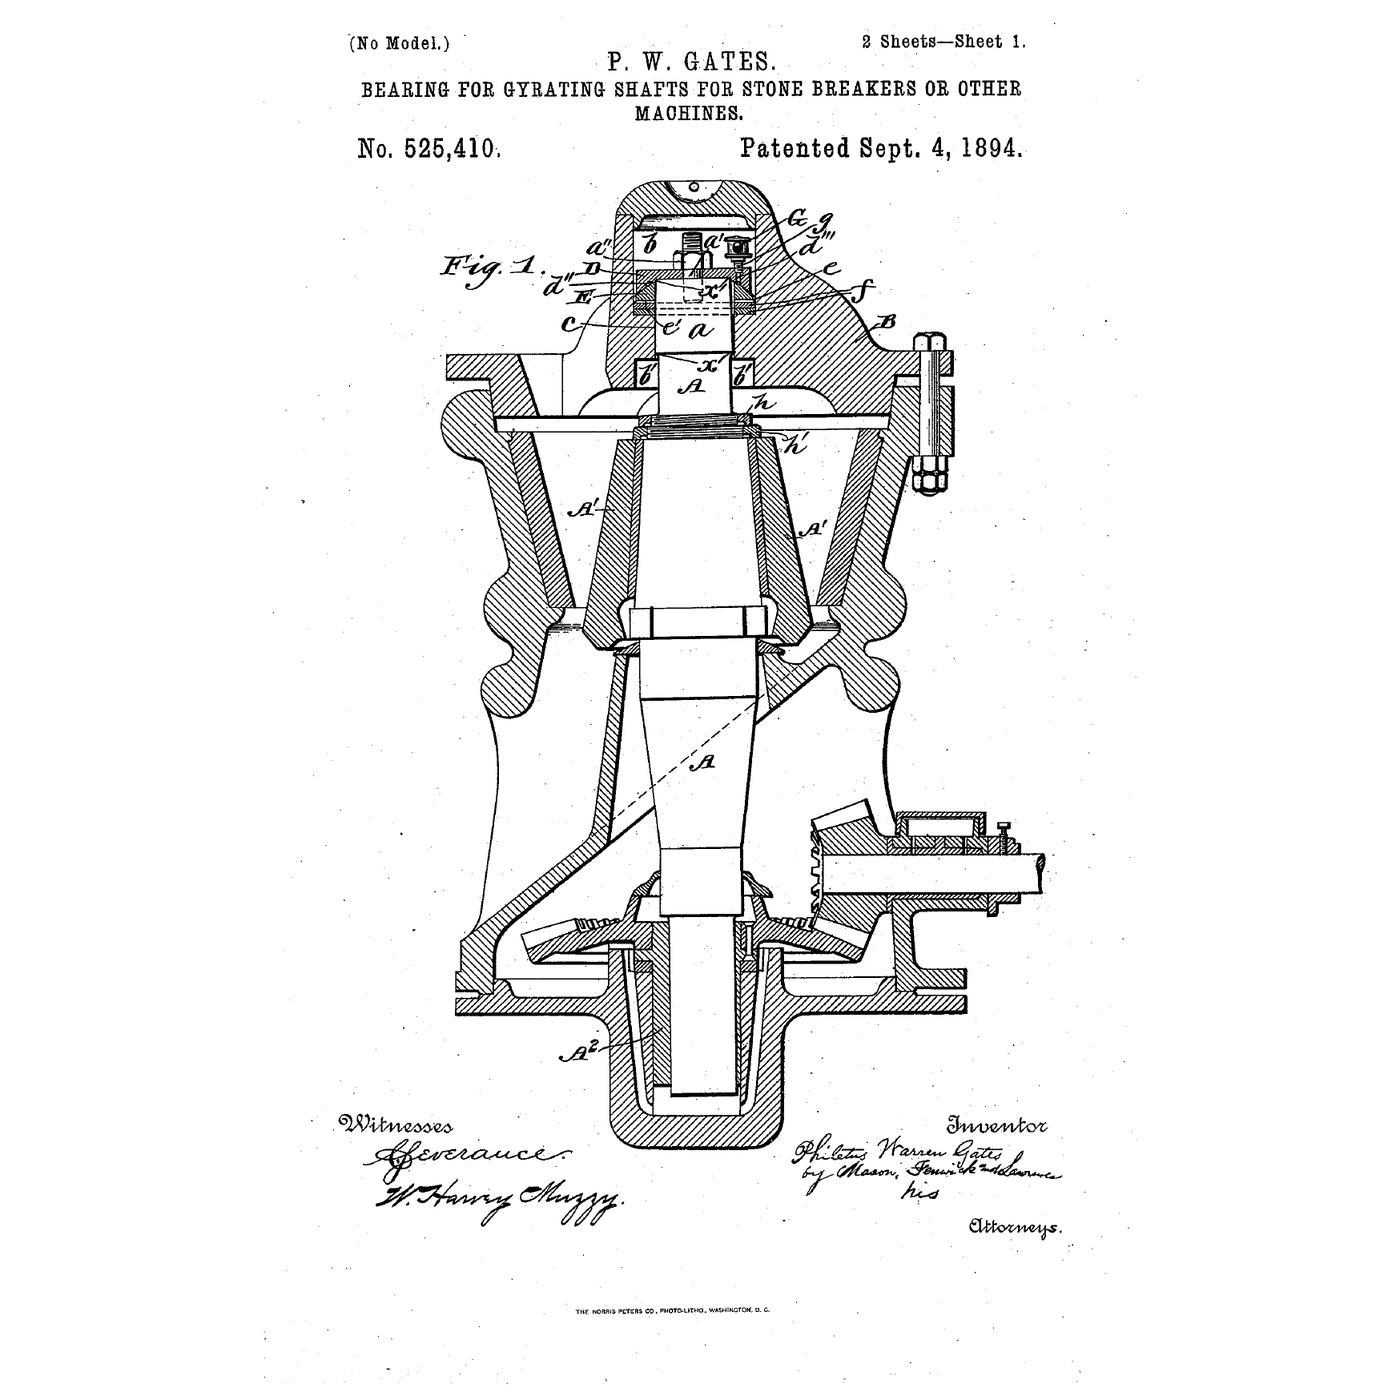
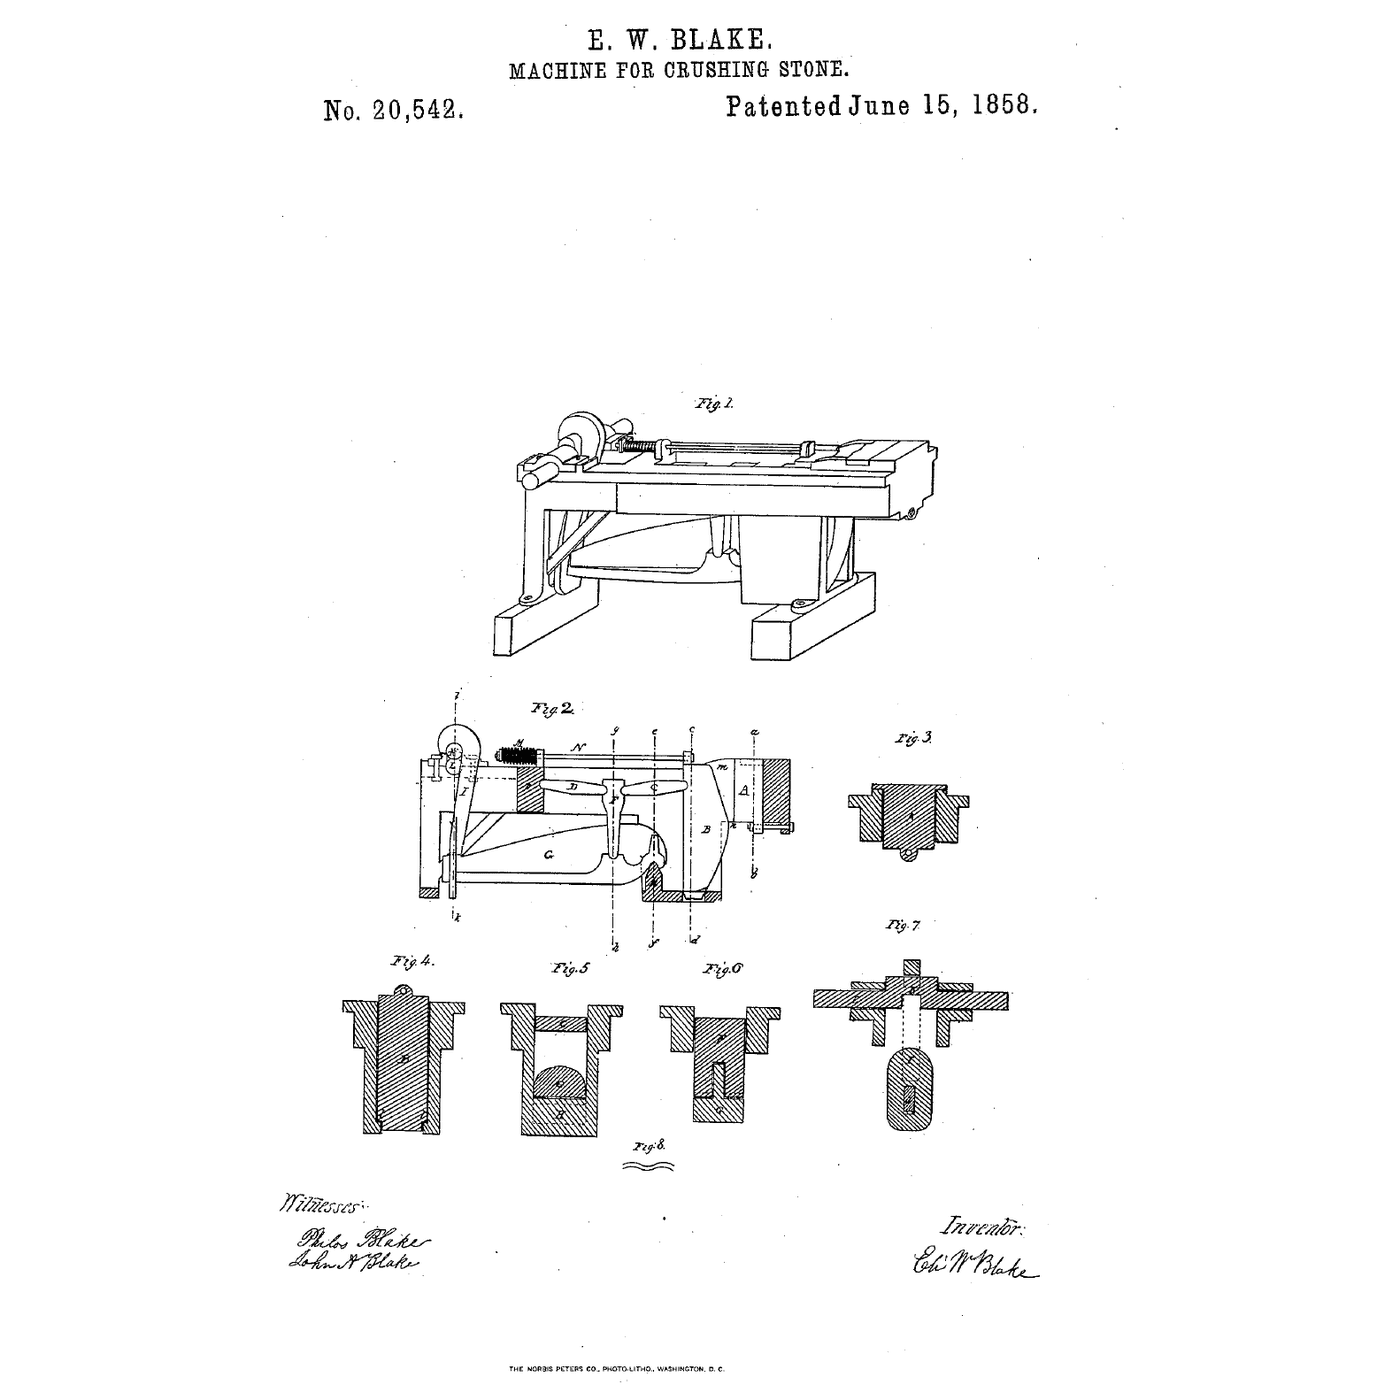
**US 1,537,564, 'Gyratory Cone Crusher', Edgar B. Symons, originally filed 14 September 1923, granted 12 May 1925.** A second verified patent, **US 1,791,584, 'Cone Crusher', filed 9 December 1929 and granted 10 February 1931**, shows how fast the type developed.
Edgar Symons and his brother Loren worked the idea out in the early 1920s; the design rights went to Nordberg Manufacturing, who acquired the Symons cone crusher business in 1928, and the machine has been called a Symons cone ever since regardless of who built it.
What it did to a quarry was change what could be sold. A jaw and a gyratory make broken stone. A cone crusher with a parallel zone makes *graded aggregate* — a product with a guaranteed top size and a predictable shape — and the concrete and asphalt specifications that the twentieth century was built on could then be written and met.
**Honest limits.** A cone is a secondary and tertiary machine: it wants a feed that has already been through a jaw or a gyratory, and it will not take a large lump. It must be choke fed to work properly, which means it needs a surge bin and a feeder ahead of it, not just a conveyor. It is intolerant of tramp metal, and although the hydraulic or spring relief will let the head lift, letting it lift is a violent event. It is unhappy with wet sticky fines, which pack the chamber. And a cone crusher that has been run with a worn parallel zone has been making out-of-spec product for some time before anyone noticed, because nothing about the machine's behaviour announces it.
རྫས་རིགས
5- 1 bucketས་ཆ་འཛིན
- 2 དུམ་བུ།ས་ཆ་འཛིན
- 1 དུམ་བུ།ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- 1 དུམ་བུ།ས་ཆ་འཛིན
ལག་ཆས་དགོས་མཁོ
14- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- 1 vendor sell this, none ship to you yetས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ཉན་ནུས་སྲུང་སྐྱོབ།ཁེ་ཕོགས 10%ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
འབྲེལ་ཡོད་བིལུ་པིརིན་ཊི
བིལུ་པིརིན་ཊི་འདི་ཚུ་ཐབས་ལམ་དང་རྫས་རིགས། སྤྱི་ཆོས་བགོ་བཤའ་བྱེད



CC0 སྤྱི་དབང
བིལུ་པིརིན་ཊི་འདི་CC0 འོག་བཀྲམས་ཡོད། ཁྱེད་རང་གིས་ཆོག་མཆན་མ་བཞེས་པར་ཕབ་ལེན་དང་བཟོ་བཅོས། བགོ་བཤའ། དགོས་མཁོ་གང་ལའང་བཀོལ་སྤྱོད་བྱས་ཆོག
བཟོ་མཁན་ལ་རྒྱབ་སྐྱོར་བྱེད་པའི་ཆེད་ཁོང་ཚོའི་བིལུ་པིརིན་ཊི་བརྒྱུད་ཐོན་སྐྱེད་ཉོ། བཟོ་མཁན་གྱིས བཟོ་མཁན་གྱི་ཁེ་ཕོགས ཚོང་པས་གཏན་འཁེལ་བྱས་པ། ཡང་ན་བིལུ་པིརིན་ཊི་འདིའི་པར་གསར་བཟོས་ཏེ་ཁྱེད་རང་གི་བིལུ་པིརིན་ཊི་ནང་མཐུད་སྦྲེལ་བྱས་ཏེ་ཡོང་སྒོ་བགོ་བཤའ་བྱེད།