艺术
美容与健康
工艺
文化与历史
娱乐
环境
食品与饮料
逆向工程
科学
体育
技术
可穿戴设备
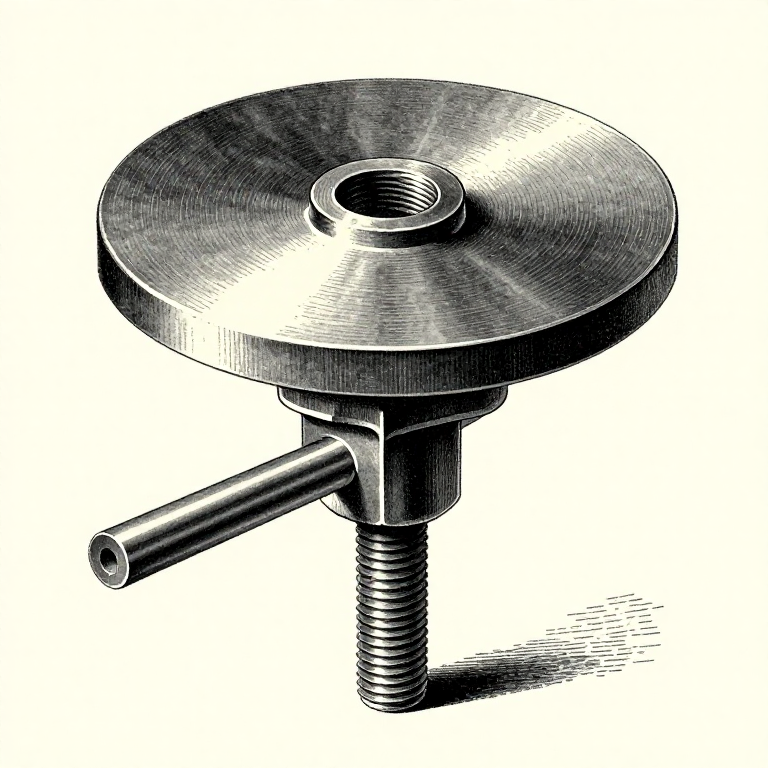

Cutting a Thread with a Die: Making Your Own Bolt
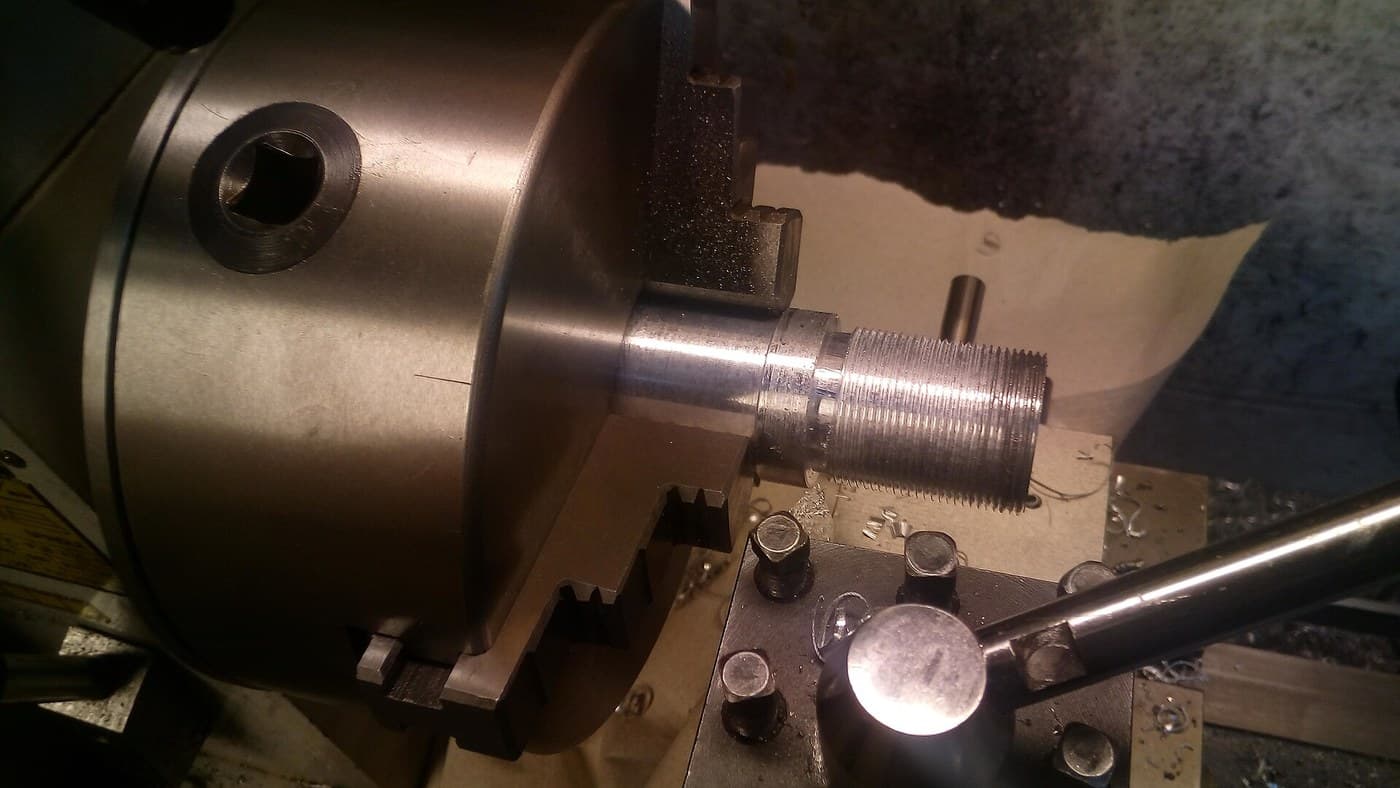
A die cuts a thread onto the outside of a bar — the mirror of what a tap does inside a hole, and the way to make a bolt, a stud or a threaded rod in exactly the length you need.
It is more forgiving than tapping in one way and less in another. A die cannot break off inside anything, so the worst outcome is a spoiled bar. But getting it square is harder, because there is no hole to guide it — the die will happily start at an angle and cut a drunken thread.
The preparation matters more than the cutting: the bar has to be the right size and it has to be chamfered.
中级
3 hours
说明
1
1
The bar must be slightly UNDER nominal
The bar must be slightly UNDER nominal
An M8 thread wants a bar of about 7.8 to 7.9 mm, not 8.0. Commercial round bar sold as 8 mm is usually a little under already, which is why it works.
A bar at full nominal diameter forces the die to remove metal right at the crest of the thread, where it has the least clearance. The result is a tight, rough thread, high cutting torque, and a crest that tears rather than cuts. Turning or filing a few hundredths off first transforms the job.
Measure before you start. Bar stock varies, and a bar that is a tenth of a millimetre oversize is the difference between a die that cuts sweetly and one that has to be forced.
此步骤所需材料:
 低碳钢条1 个
所需工具:
 游标卡尺
 锉刀(手用锉)
 重型台钳
2
2
Chamfer the end — always
Chamfer the end — always
File or grind a 45 degree chamfer on the end of the bar, down to roughly the thread's minor diameter. The die then has a tapered surface to sit on and centres itself.
Without a chamfer, the die meets a flat square end and has nothing to align against. It will start crooked, and a crooked start on a die cannot be corrected at all — the thread that follows simply repeats the error down the bar.
The chamfer also becomes the lead-in of the finished thread, which is what lets the bolt start easily into a nut. A bolt with no chamfer is difficult to start and is the commonest cause of cross-threading.
此步骤所需材料:
低碳钢条1 个所需工具:
锉刀(手用锉)重型台钳游标卡尺3
3
Which way up, and starting square
Which way up, and starting square
A die has a lead on ONE face — the first few threads are tapered — and that face goes against the work. Look for it; it is usually the side without the printed size, and putting the die on backwards means it cannot start at all.
Seat the die stock flat against the bar end and press down hard while turning. The pressure is doing the work for the first two turns; after that the thread pulls the die along on its own and you can ease off.
Check square after two turns exactly as with a tap. A round split die can also be adjusted slightly by its screws: opened out for a first roughing pass, closed for a second finishing pass. On a tough material that two-pass approach halves the torque and gives a better thread.
所需工具:
 板牙架
 丝锥板牙套装重型台钳
 蓝色显示剂
4
4
Back off, oil, and test it on a real nut
Back off, oil, and test it on a real nut
Half a turn forward, a quarter back — the same rhythm as tapping and for the same reason. Use cutting oil generously; a die has far more cutting edges in contact than a tap and generates correspondingly more heat.
Cut to the length you need and no further. A thread run right up to a shoulder leaves no clearance and the nut will not seat, so stop two or three threads short.
Test the result by running a real nut down the full length by hand. It should turn with light finger pressure the whole way. If it tightens progressively, the bar was oversize or the die is closing; if it is loose and rocks, the die was opened too far. Both are diagnosed in ten seconds by the nut and by nothing else.
此步骤所需材料:
 切削油1 个低碳钢条1 个
所需工具:
板牙架 螺母与垫圈组合
 棉布
 透明安全眼镜
相关蓝图
这些蓝图共享知识——技术、材料或原理
CC0 公共领域
此蓝图以 CC0 协议发布。你可以自由复制、修改、分发和使用此作品,无需征得许可。
通过购买蓝图中的产品支持创客,他们将获得 创客佣金 (由供应商设定),或创建此蓝图的新版本并将其作为连接包含在你自己的蓝图中以分享收入。