合作
艺术
美容与健康
工艺
文化与历史
娱乐
环境
食品与饮料
逆向工程
科学
体育
技术
可穿戴设备


Melt, Mix and Shoot: One Screw Doing Two Jobs
The injection moulding rung already in the catalogue describes the process: melt, force into a cavity, cool, eject. It does not say how the melting is done, and for the first eighty years of the industry the answer was bad.
A ram pushed cold pellets through a heated tube round a 'torpedo' and hoped. Polymers conduct heat about a thousand times worse than steel, so the middle of the charge arrived cold while the outside cooked, the melt was never properly mixed, and the cycle was measured in minutes.
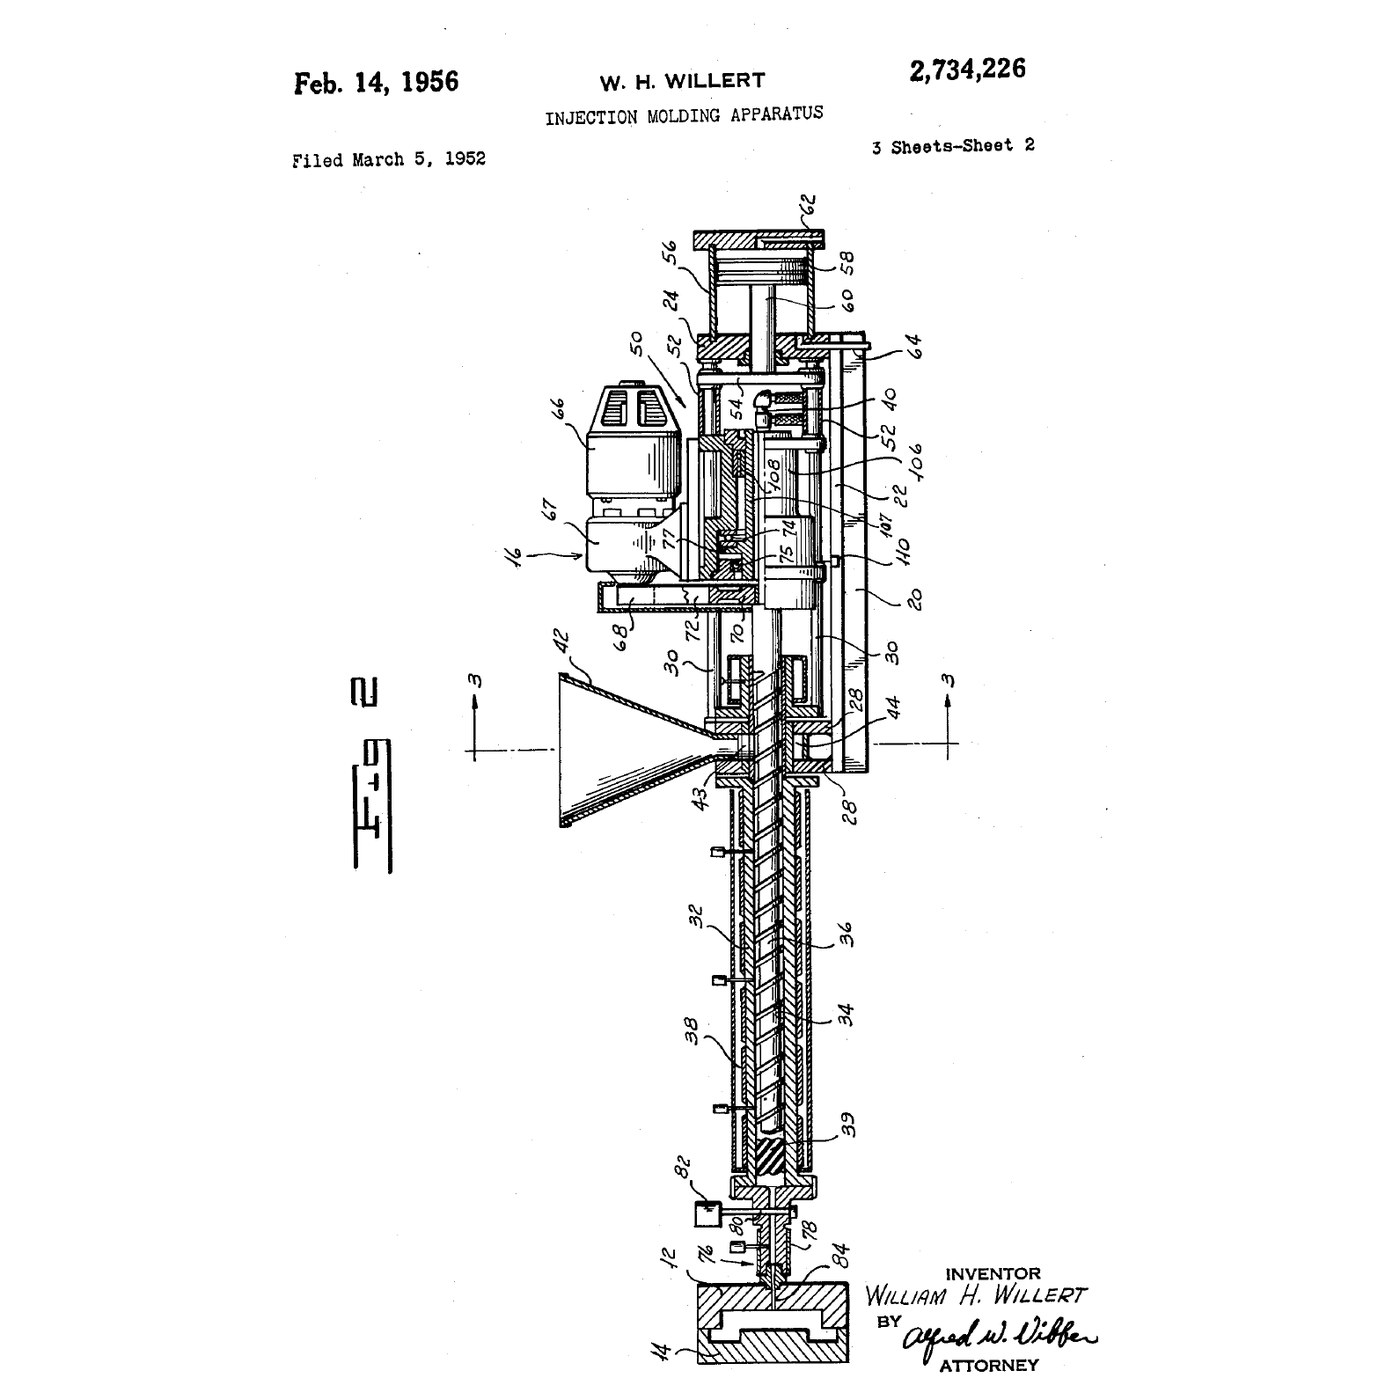
William Willert's 1952 answer was to make the screw do both jobs: **rotate** to convey, melt and mix — heating the polymer mostly by shearing it, from the inside — and then **slide forward as a ram** to inject. One shaft, two motions, and the machine that made plastic cheap.
中级
About 3 hours
说明
1
1
Read the claim, and name what it replaced
Read the claim, and name what it replaced
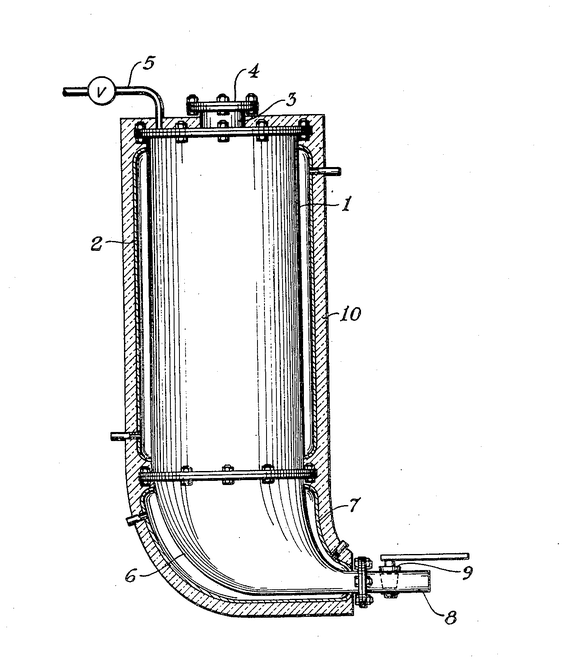
**US 2,734,226**, *Injection Molding Apparatus*, **William H. Willert** of Clifton, New Jersey; application **5 March 1952**, Serial No. 274,897, patented **14 February 1956**; 10 claims, US class 18-30. Expired. The drawing on this page is the patent's own sheet 2.
The specification opens by describing what it is fixing. It relates to *a mechanism for plasticizing and delivering* plastic, so that the material is *thoroughly mixed and plasticized* and reaches the mould in an *optimumly plasticized condition*. And it names the prior art directly: *over and over, various forms of "preplasticizers"* had been tried, *all the various types of preplasticizer units* falling short.
Write down the three things the arrangement does at once, because the invention is that they share one shaft:
1. **Convey.** The flights drag pellets forward from the hopper.
2. **Melt and mix.** The channel narrows, the polymer is sheared, and shear does most of the heating — step 4 works out how much.
3. **Inject.** Melt accumulates ahead of the screw tip, pushing the screw BACK; then the whole screw is driven forward as a ram and that accumulated shot is injected.
The three zones along the screw have names worth knowing: **feed** (deep flights, solid pellets), **compression** or transition (the channel shallows, the solid bed melts against the barrel), and **metering** (shallow flights, homogenising what is now fully molten).
2
2
You already own a ram machine — find where it runs out
You already own a ram machine — find where it runs out
A filament 3D printer is, in its melting arrangement, the machine Willert replaced: a solid rod of polymer is pushed as a **ram** through a short heated tube, and everything depends on conduction from the wall. That makes it the best bench demonstration of the problem there is, because you can drive it until it fails.
Print a single-wall tube — a 'vase mode' cylinder 60 mm across — and run the same print at rising flow. Increase speed in steps and, at each step, catch the extrusion mid-air and weigh a measured length, or simply measure the printed wall with the calipers.
Plot **actual flow against commanded flow**. The two agree, and agree, and then the line bends over: beyond some rate the hot end cannot get heat into the middle of the filament fast enough, the core arrives unmelted, pressure climbs and the extruder skips.
That knee is the conduction limit from step 4, and it is the entire reason the industry abandoned ram melting. Note two things about how it fails:
- **Raising the temperature helps less than you expect**, because the limit is how fast heat crosses the filament, not how hot the wall is. Beyond a point you are only degrading the surface.
- **A longer melt zone helps a lot.** That is what a high-flow hot end is: more length, so more time at the wall. A screw solves it differently — by making the melt film thin and adding shear — and gets an order of magnitude more.
Record the knee flow rate in mm³/s. You will compare it with a moulding machine's in step 4.
此步骤所需材料:
 PLA 线材1 个
 PETG线材1 个
所需工具:
 3D 打印机
 6 英寸数显卡尺
 精密数字天平
 秒表
 红外测温仪
 安全眼镜
 实验记录本(带复写页)
3
3
Find the shear heat
Find the shear heat
Shear heating is not a detail of the theory; on a production machine it is most of the energy in the melt. You can see it on the bench in two ways.
**On the printer.** Get the hot end to steady state with no extrusion and note the heater duty cycle — many firmwares report PWM, or you can watch how often the heater LED pulses. Now extrude hard and watch again. The heater works **less**, not more, because the filament being forced through the nozzle is dissipating its own work as heat. If your firmware shows nothing, put the infrared thermometer on the nozzle block and watch the overshoot when a fast extrusion stops.
**With a hand press.** Put a disc of polypropylene sheet between two steel plates, warm the stack to just below softening, and squeeze it in the shop press while reading the surface with the infrared thermometer. Squeezing forces the polymer to flow radially — that is shear — and the temperature rises where the flow is fastest, at the rim, not where the heating is.
Neither is a calibrated measurement. Both show the direction, which is the thing worth carrying: **in a polymer, flow is a heat source.** Step 4 turns that into numbers.
Hot ends reach 250 °C and up, and molten polymer sticks to skin. Never clear a nozzle with fingers, never put a hand under a moving gantry, and ventilate — ABS and some filled filaments give off genuinely unpleasant volatiles at temperature.
此步骤所需材料:
 聚丙烯板(A4)1 个PLA 线材1 个
所需工具:
3D 打印机 液压机红外测温仪
 K 型热电偶配 MAX6675 模块
 低碳钢板
 热风枪安全眼镜
 丁腈手套
 通风柜(带排风管)实验记录本(带复写页)
4
4
Conduction, shear and residence time
Conduction, shear and residence time
正在加载 Jupyter 笔记本…
所需工具:
 坐标纸
5
5
History and context
History and context
**Attribution.** US 2,734,226, *Injection Molding Apparatus*, William H. Willert, Clifton NJ; filed 5 March 1952, granted 14 February 1956, expired. The drawing on this page is the patent's own.
**What came before.** Injection moulding of a sort dates to the Hyatt brothers in 1872, pushing celluloid through a heated cylinder with a plunger — the celluloid rung is already in the catalogue. For eighty years the machines stayed plungers, and the industry worked around the consequences: thick sections were unmouldable, engineering polymers with narrow processing windows were impossible, and shot-to-shot consistency was poor because no two charges melted the same way.
The screw extruder itself was old — rubber and thermoplastics had been extruded on screws since the nineteenth century. **Willert's contribution is not the screw, it is making the screw reciprocate**, so that one shaft plasticises continuously between shots and then becomes the injection ram. That deletes the transfer between a preplasticizer and a separate ram, which was where the previous generation lost its temperature uniformity.
**Why it mattered.** Cycle times fell, engineering thermoplastics became mouldable, and the cost per part collapsed. Practically every plastic object made since is made on a machine that works this way; look at the photograph of any moulding machine and the long horizontal barrel with a hopper part-way along it is this patent.
**Honest limits.** A screw is a shear machine, and shear degrades some polymers as surely as heat does — PVC and some filled compounds need gentle screws and short residence times. Residence time is a real constraint, as step 4's last table shows: a small part on a large machine cooks. And none of this is bench-reproducible; a moulding machine is a serious piece of industrial equipment, which is why every hands-on step here uses a printer, a press and a heat gun to isolate the *principles* rather than pretending to reproduce the machine.
相关蓝图
这些蓝图共享知识——技术、材料或原理


CC0 公共领域
此蓝图以 CC0 协议发布。你可以自由复制、修改、分发和使用此作品,无需征得许可。
通过购买蓝图中的产品支持创客,他们将获得 创客佣金 (由供应商设定),或创建此蓝图的新版本并将其作为连接包含在你自己的蓝图中以分享收入。