KUNST
SCHÖNHEIT & WELLNESS
HANDWERK
KULTUR & GESCHICHTE
UNTERHALTUNG
UMFELD
ESSEN & GETRÄNKE
REVERSE ENGINEERING
WISSENSCHAFTEN
SPORT
TECHNOLOGIE
WEARABLES
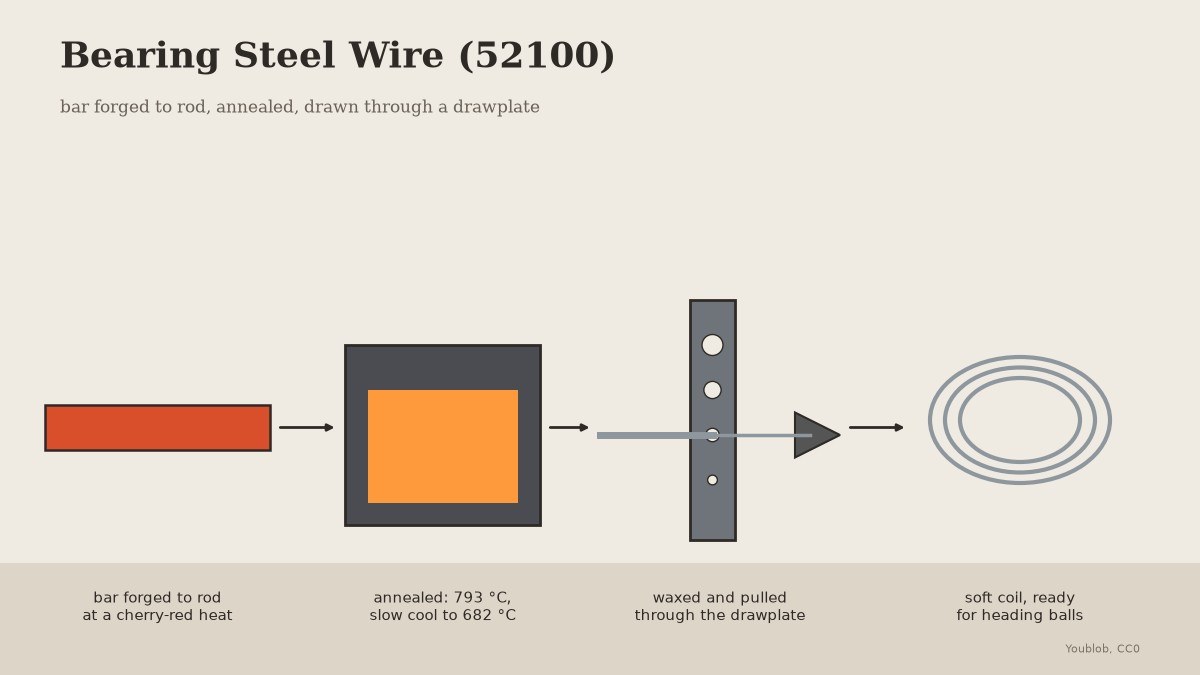


Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
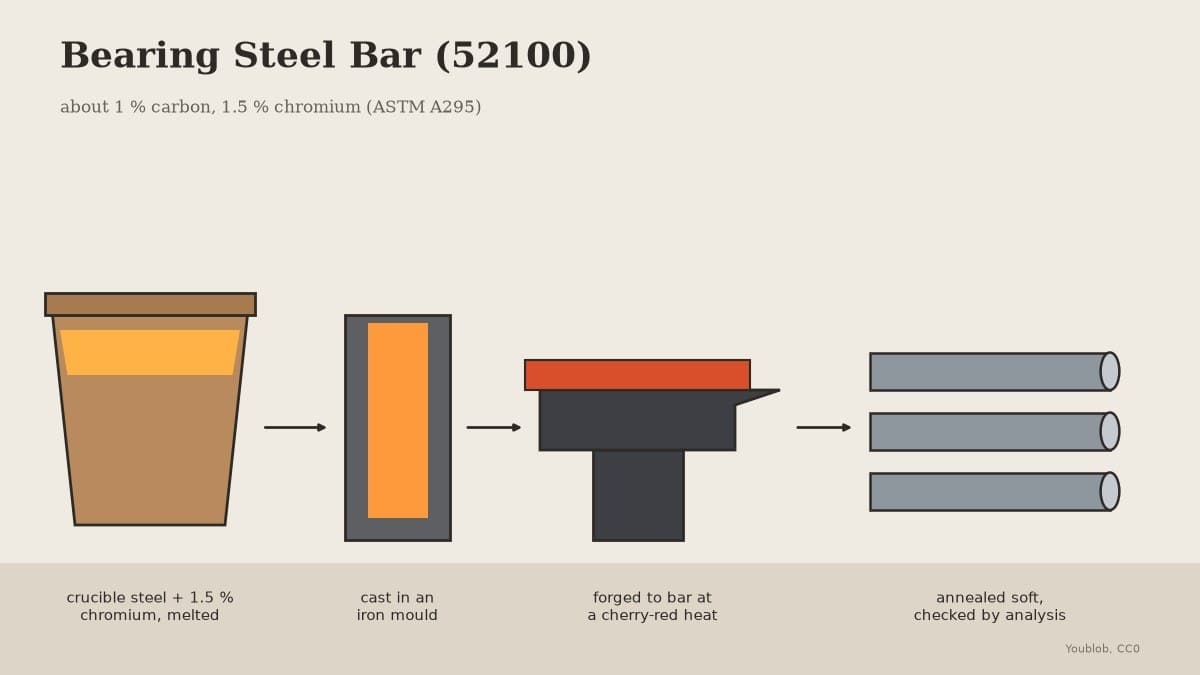
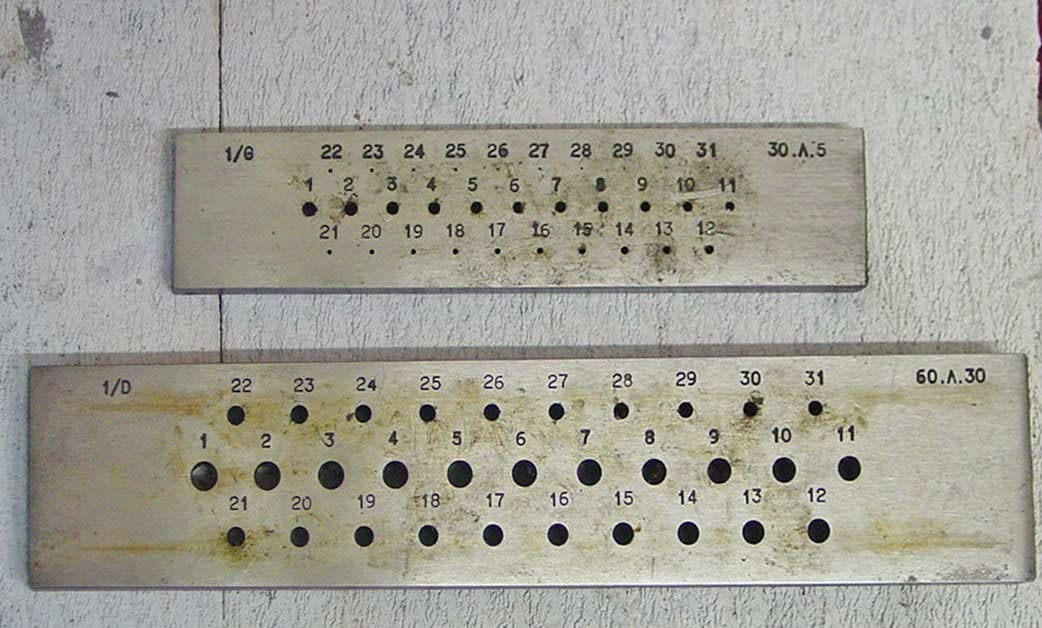
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
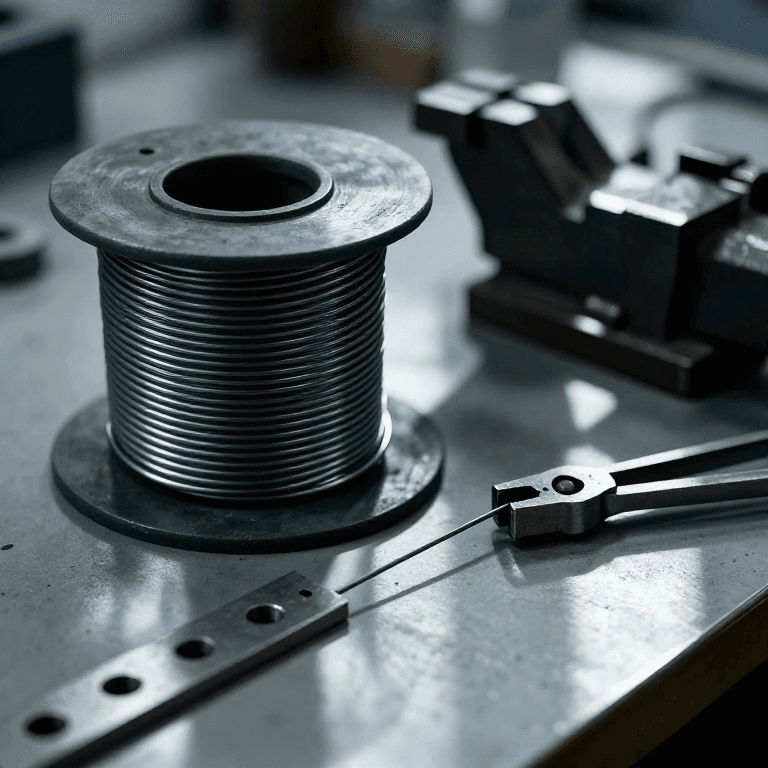
The picture: our drawing, bar to coil.
Erfahren
2 days
Anweisungen
1
1
Forge to rod
Forge to rod
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
Materialien für diesen Schritt:
 Wälzlagerstahlstange (52100)1 kg
 Holzkohle1 as required
Benötigte Werkzeuge:
 Schmiedeesse
 Amboss
 Kreuzschlaghammer
 Schmiedezange
 Schweißerhandschuhe
 Schutzbrille
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Benötigte Werkzeuge:
 Wärmebehandlungsofen
 Thermoelement mit AnzeigeSchmiedezangeSchweißerhandschuhe
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
Benötigte Werkzeuge:
 Drahtbürsten-Set
 Feilensatz
 Schraubstock
4
4
Wax and draw
Wax and draw
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
Materialien für diesen Schritt:
 Bienenwachs20 g
Benötigte Werkzeuge:
 Zieheisen aus Stahl
 ZiehzangeSchraubstock
 Lederarbeitshandschuhe
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Materialien für diesen Schritt:
Bienenwachs1 StückBenötigte Werkzeuge:
Zieheisen aus StahlZiehzangeWärmebehandlungsofenThermoelement mit Anzeige6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
Benötigte Werkzeuge:
 Digitaler Messschieber 6 ZollWärmebehandlungsofenThermoelement mit Anzeige
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
Materialien
3- Platzhalter
- 1 as requiredPlatzhalter
- 1 StückPlatzhalter
Benötigte Werkzeuge
15- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
- Platzhalter
Dieser Bauplan stellt her
Verwandte Blueprints
Diese Blueprints teilen Wissen — Techniken, Materialien oder Prinzipien
CC0 Gemeinfrei
Dieser Blueprint ist unter CC0 veröffentlicht. Sie dürfen dieses Werk für jeden Zweck frei kopieren, ändern, verbreiten und verwenden, ohne um Erlaubnis zu fragen.
Unterstützen Sie den Maker, indem Sie Produkte über seinen Blueprint kaufen, wo er eine Maker-Provision von Anbietern festgelegt, verdient. Oder erstellen Sie eine neue Iteration dieses Blueprints und verbinden Sie ihn in Ihrem eigenen Blueprint, um Einnahmen zu teilen.