Colaboración
ARTE
BELLEZA Y BIENESTAR
ARTESANÍA
CULTURA E HISTORIA
ENTRETENIMIENTO
MEDIO AMBIENTE
COMIDA Y BEBIDAS
INGENIERÍA INVERSA
CIENCIAS
DEPORTES
TECNOLOGÍA
TECNOLOGÍA VESTIBLE
English


PTFE Thread Seal Tape: Paste-Extruded, Calendered, Never Sintered
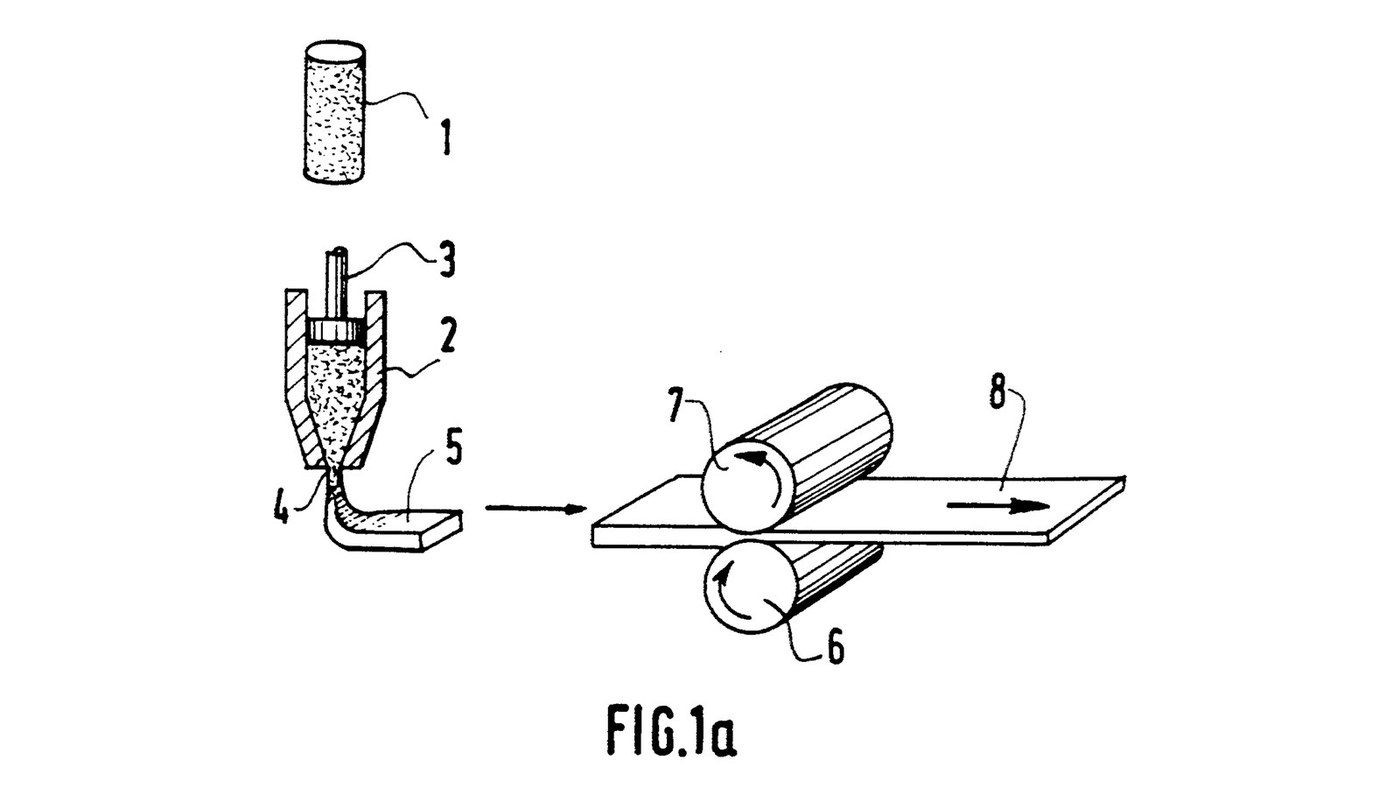
The white tape wound on pipe threads is PTFE that has never been melted. Fine PTFE powder is mixed with a lubricant, pressed into a slug, squeezed through a slit die by a ram, rolled thin between two rolls, and dried. Kept below the sintering heat (about 350 °C) it stays soft and conforms to the thread (process: US 5,415,939, 1995). The targets and tests are those of the Indian standard IS 14643 (from BS 4375): no fillers, at most 0.1 % lubricant left, usually 12 mm wide and 0.075 mm thick.
The lubricant (naphtha) and the slitter are ours. The picture: Fig. 1a of the patent.
Avanzado
1 day
Instrucciones
1
1
Wet the powder
Wet the powder
Mix fine (dispersion-made) virgin PTFE powder with a lubricant that can be driven off completely. Granular PTFE will not paste-extrude. No fillers. Ours: naphtha, as required.
Materiales para este paso:
 Polvo fino de PTFE1 batch
Herramientas necesarias:
 Nafta
2
2
Press a preform
Press a preform
Compact the wet powder into a cylindrical preform in a mould with a plunger.
Herramientas necesarias:
 Molde de compresión
 Prensa hidráulica
3
3
Ram-extrude a flat tape
Ram-extrude a flat tape
Put the preform in the extrusion press. The plunger pushes it out through a slit die as a thick flat tape.
Herramientas necesarias:
 Prensa de extrusión hidráulica
4
4
Calender it thin
Calender it thin
Pass the tape between two counter-rotating rolls to a thin tape, aiming at about 0.075 mm.
Herramientas necesarias:
 Laminador
 Micrómetro
5
5
Dry off the lubricant
Dry off the lubricant
Dry the tape until the lubricant is gone. Keep it well below the sintering heat (about 350 °C): sintered tape is stiff and will not seal.
Herramientas necesarias:
 Horno de secado
6
6
Slit and spool
Slit and spool
Slit it to width, usually 12 mm (±0.5 mm), and wind it on spools.
Herramientas necesarias:
 Cortadora-rebobinadora
7
7
Check the tape
Check the tape
It must look white, with no visible specks or torn edges. Measure the thickness at five points along a sample; each must be within 10 % of their mean.
Herramientas necesarias:
Micrómetro8
8
Test the residual lubricant
Test the residual lubricant
Weigh about 15 g of tape. Extract it in a Soxhlet with petroleum spirit (40-60 °C) for at least 4 h, dry it at 100 °C, then heat it at 300 °C for 6 h, cool and weigh. The loss must be 0.1 % or less.
Herramientas necesarias:
 Extractor Soxhlet
 Éter de petróleoHorno de secado
 Crisol de acero
 Cámara de desecación (pequeña)
 Báscula digital de precisión
9
9
Wrap a thread
Wrap a thread
Wind tape round an R 1/2 taper pipe thread with 50 % overlap, two layers deep, just tight enough to take the thread form. It must hold the form, not break, and its end must stay put.
Herramientas necesarias:
 Accesorio roscado para tubería
Materiales
1- 1 batchMarcador de posición
Herramientas requeridas
14- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición

Blueprints relacionados
Estos blueprints comparten conocimiento — técnicas, materiales o principios


CC0 Dominio público
Este Blueprint se publica bajo CC0. Eres libre de copiar, modificar, distribuir y usar este trabajo para cualquier propósito, sin pedir permiso.
Apoya al Maker comprando productos a través de su Blueprint, donde gana una Comisión del Maker establecida por los vendedores, o crea una nueva iteración de este Blueprint e inclúyela como conexión en tu propio Blueprint para compartir ingresos.