Colaboración
ARTE
BELLEZA Y BIENESTAR
ARTESANÍA
CULTURA E HISTORIA
ENTRETENIMIENTO
MEDIO AMBIENTE
COMIDA Y BEBIDAS
INGENIERÍA INVERSA
CIENCIAS
DEPORTES
TECNOLOGÍA
TECNOLOGÍA VESTIBLE
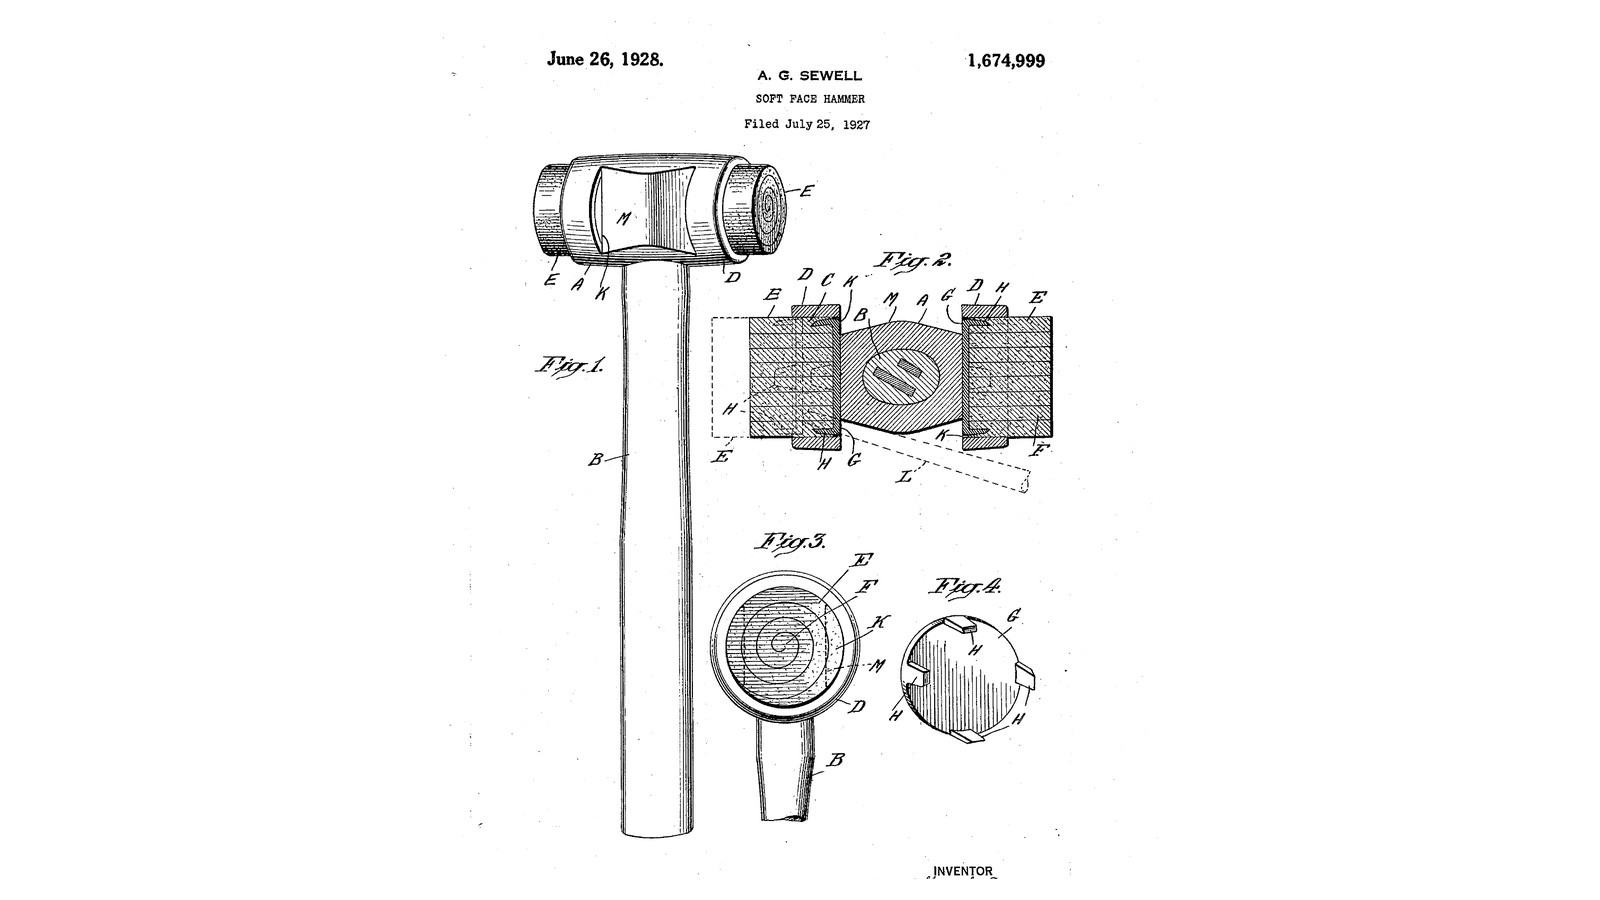


Renewable Rubber-Face Hammer: Rolled Faces Pressed Onto Pronged Discs, Driven Out Through a Notch When Worn (Sewell, 1928)
Albert G. Sewell received US 1,674,999, dated 26 June 1928, for a soft-face hammer whose worn faces can be renewed instead of throwing the hammer away. Each end of the head is a cup. A face rolled from a strip is pressed into the cup onto a loose sheet-metal disc whose prongs bite into it and wedge it tight. When a face is battered, a rod pushed through a notch at the bottom of the cup drives the disc and the face out together, and a new face goes in. He preferred rawhide and named rubber among face materials; ours are rolled from rubber sheet.
The patent gives no sizes; every size here is ours.
Intermedio
About 1 day
Instrucciones
1
1
Rolling a face plug
Rolling a face plug
Cargando el cuaderno de Jupyter…
2
2
Read US 1,674,999
Read US 1,674,999
"Thus, by hammering or otherwise thrusting a rod or suitable device against the wedging member, the latter, with the striking face member, can be forced or driven out of the socket or recess, after which a new striking face member may be forced into the socket, to be secured therein by the wedging member."
3
3
Turn the head
Turn the head
Grip 40 mm steel round bar in the chuck and turn a head 110 mm long: the two ends stay 40 mm across for 26 mm as the flanges D, and the middle is waisted to 30 mm. Bore each end 32 mm across and 22 mm deep for the sockets C, flat at the bottom. Drill a 20 mm eye B through the middle, square to the axis, in a V-block on the drill press.
Materiales para este paso:
 Barra redonda de acero dulce1 pieza
 Aceite de corte1 pieza
Herramientas necesarias:
 Torno de metal
 Plato de torno de 3 mordazas
 Herramienta de corte para torno
 Barra de mandrinar
 Gubia de tronzar
 Taladro de columna
 Bloque en V
 Juego de brocas
 Calibre digital de 6 pulgadas
 Gafas de seguridad
4
4
Cut the notches K
Cut the notches K
On the handle's side of each flange, saw and file a notch 8 mm wide through the flange's wall at the very bottom of the socket, so a rod can be pushed in at a slant against the edge of the disc at the bottom.
Herramientas necesarias:
 Tornillo de banco
 Sierra para metales
 Juego de limas
 Granete
5
5
Pronged discs G
Pronged discs G
Cut two discs of 1.5 mm steel sheet 31.5 mm across. At four places round each rim, snip two cuts 6 mm deep 5 mm apart and bend the tab between them up at a right angle with the pliers: the prongs H. Drop one disc loosely into the bottom of each socket, prongs out.
Materiales para este paso:
 Chapa de acero dulce1 pieza
Herramientas necesarias:
 Tijeras de chapa
 Alicates de boca planaTornillo de bancoJuego de limas
6
6
Roll and press in the faces E
Roll and press in the faces E
Cut two strips of 3 mm natural rubber sheet 32 mm wide and about 270 mm long. Roll each tightly into a coil, trimming the strip until the coil just enters a socket, and tie it. Press the coil into its socket in the vice, between soft packing, until it bottoms on the disc and its prongs bite in, leaving the face standing about 10 mm out. Cut the tie and trim the face flat with the knife.
Materiales para este paso:
 Plancha de caucho natural1 pieza
Herramientas necesarias:
 Cúter de precisiónTornillo de bancoCalibre digital de 6 pulgadas
7
7
Handle
Handle
Turn an ash handle 300 mm long, its end a tight fit in the eye. Saw a slot down its end, drive it into the eye, and glue and drive a hardwood wedge into the slot; saw it off flush.
Materiales para este paso:
 Tabla de madera dura1 pieza
 Cola de carpintero1 pieza
Herramientas necesarias:
 Torno de madera
 Juego de herramientas de torno (HSS)Sierra para metales
 Martillo de bola
8
8
Renew a face
Renew a face
When a face is worn, push a steel rod through the socket's notch against the disc's edge and tap it out with the hammer; the disc and the face come out together. Put the disc back, prongs out, and press in a new rolled face.
Herramientas necesarias:
Martillo de bolaTornillo de banco9
9
Troubleshooting
Troubleshooting
Soft-face hammer troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
**Albert G. Sewell**, US 1,674,999, dated 26 June 1928, filed 25 July 1927. He describes a head with a socket at each end formed by annular flanges, a striking face member of relatively soft material rolled from a strip and pressed in as a plug, a loose sheet-metal wedging disc with prongs in the socket's bottom, and openings through which a rod drives the disc and face out. He preferred rawhide and his head was cast iron; ours is turned steel with faces rolled from rubber sheet, which he lists among the face materials in use. He gives no sizes; every size here is ours.
Materiales
6- 1 piezaMarcador de posición
- 1 piezaMarcador de posición
- 1 piezaMarcador de posición
- 1 piezaMarcador de posición
- 1 piezaMarcador de posición
- 1 piezaMarcador de posición
Herramientas requeridas
20- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
Este plano hace

Blueprints relacionados
Estos blueprints comparten conocimiento — técnicas, materiales o principios
CC0 Dominio público
Este Blueprint se publica bajo CC0. Eres libre de copiar, modificar, distribuir y usar este trabajo para cualquier propósito, sin pedir permiso.
Apoya al Maker comprando productos a través de su Blueprint, donde gana una Comisión del Maker establecida por los vendedores, o crea una nueva iteración de este Blueprint e inclúyela como conexión en tu propio Blueprint para compartir ingresos.