ARTE
BELLEZA Y BIENESTAR
ARTESANÍA
CULTURA E HISTORIA
ENTRETENIMIENTO
MEDIO AMBIENTE
COMIDA Y BEBIDAS
INGENIERÍA INVERSA
CIENCIAS
DEPORTES
TECNOLOGÍA
TECNOLOGÍA VESTIBLE
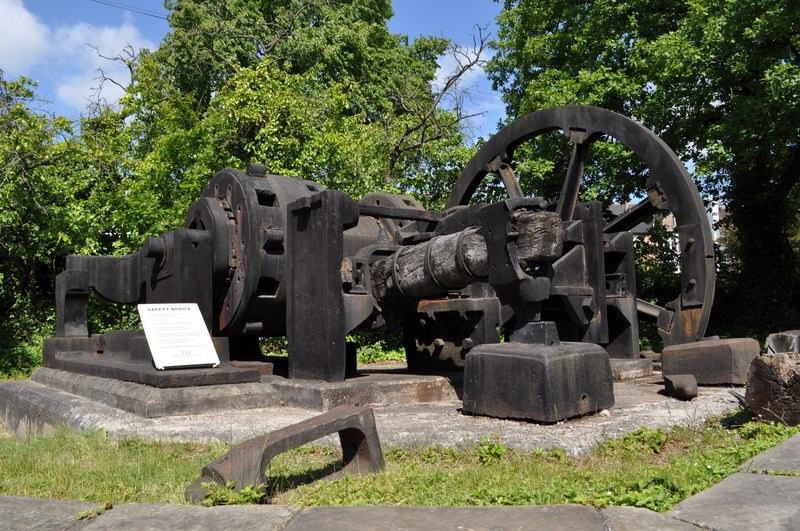


Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
Sheffield poured its crucible cast steel into octagonal or rectangular iron moulds and drew the ingots out into rods under the tilt hammer. That bar, eight-sided or square, was the stock for chisels, punches, files and blades. Andrew Ure's 1839 warning still holds: this steel must not go much above a cherry-red heat, or it turns brittle.
The picture: a water-driven tilt hammer at Abbeydale Industrial Hamlet, Sheffield.
Avanzado
A day at the forge
Instrucciones
1
1
Heat gently to cherry red
Heat gently to cherry red
Bring the crucible-steel ingot up slowly in the forge to a cherry-red heat and no hotter. Ure: in its usual state cast steel will not bear much more without becoming brittle, and it will not take a welding heat.
Materiales para este paso:
 Acero al crisol2 kg
 Carbón vegetal1 as required
Herramientas necesarias:
 Fragua de herrero
 Tenazas de herrero
 Guantes de soldador
 Delantal de cuero
 Gafas de seguridad
2
2
Draw out a billet
Draw out a billet
On the anvil, with a striker on the sledge, draw the ingot out square, turning it a quarter after each pair of blows. Reheat as soon as the colour drops below red; never hammer it cold. Stop at a square billet of the size you need, or carry on drawing it flat into a rectangular bar for axe heads and picks.
Materiales para este paso:
Carbón vegetal1 as requiredHerramientas necesarias:
 Yunque
 Mazo pesado
 Martillo de peña transversalTenazas de herreroGuantes de soldadorDelantal de cueroGafas de seguridad
3
3
Knock the corners to an octagon
Knock the corners to an octagon
For octagon bar, set the square bar on a corner and hammer the four corners down evenly until all eight faces are equal, finishing in the matching groove of a swage block.
Herramientas necesarias:
YunqueMartillo de peña transversal Bloque estampadorTenazas de herreroGuantes de soldadorDelantal de cueroGafas de seguridad
4
4
Check and cool slowly
Check and cool slowly
Check the size across the flats with a caliper, then let the bar cool slowly in the dying forge (our choice, to leave it soft for cutting and filing).
Herramientas necesarias:
 Calibre digital de 6 pulgadasFragua de herrero
Materiales
2- 2 kgMarcador de posición
- 1 as requiredMarcador de posición
Herramientas requeridas
10- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
Este plano hace

Blueprints relacionados
Estos blueprints comparten conocimiento — técnicas, materiales o principios


CC0 Dominio público
Este Blueprint se publica bajo CC0. Eres libre de copiar, modificar, distribuir y usar este trabajo para cualquier propósito, sin pedir permiso.
Apoya al Maker comprando productos a través de su Blueprint, donde gana una Comisión del Maker establecida por los vendedores, o crea una nueva iteración de este Blueprint e inclúyela como conexión en tu propio Blueprint para compartir ingresos.