Collaboration
ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
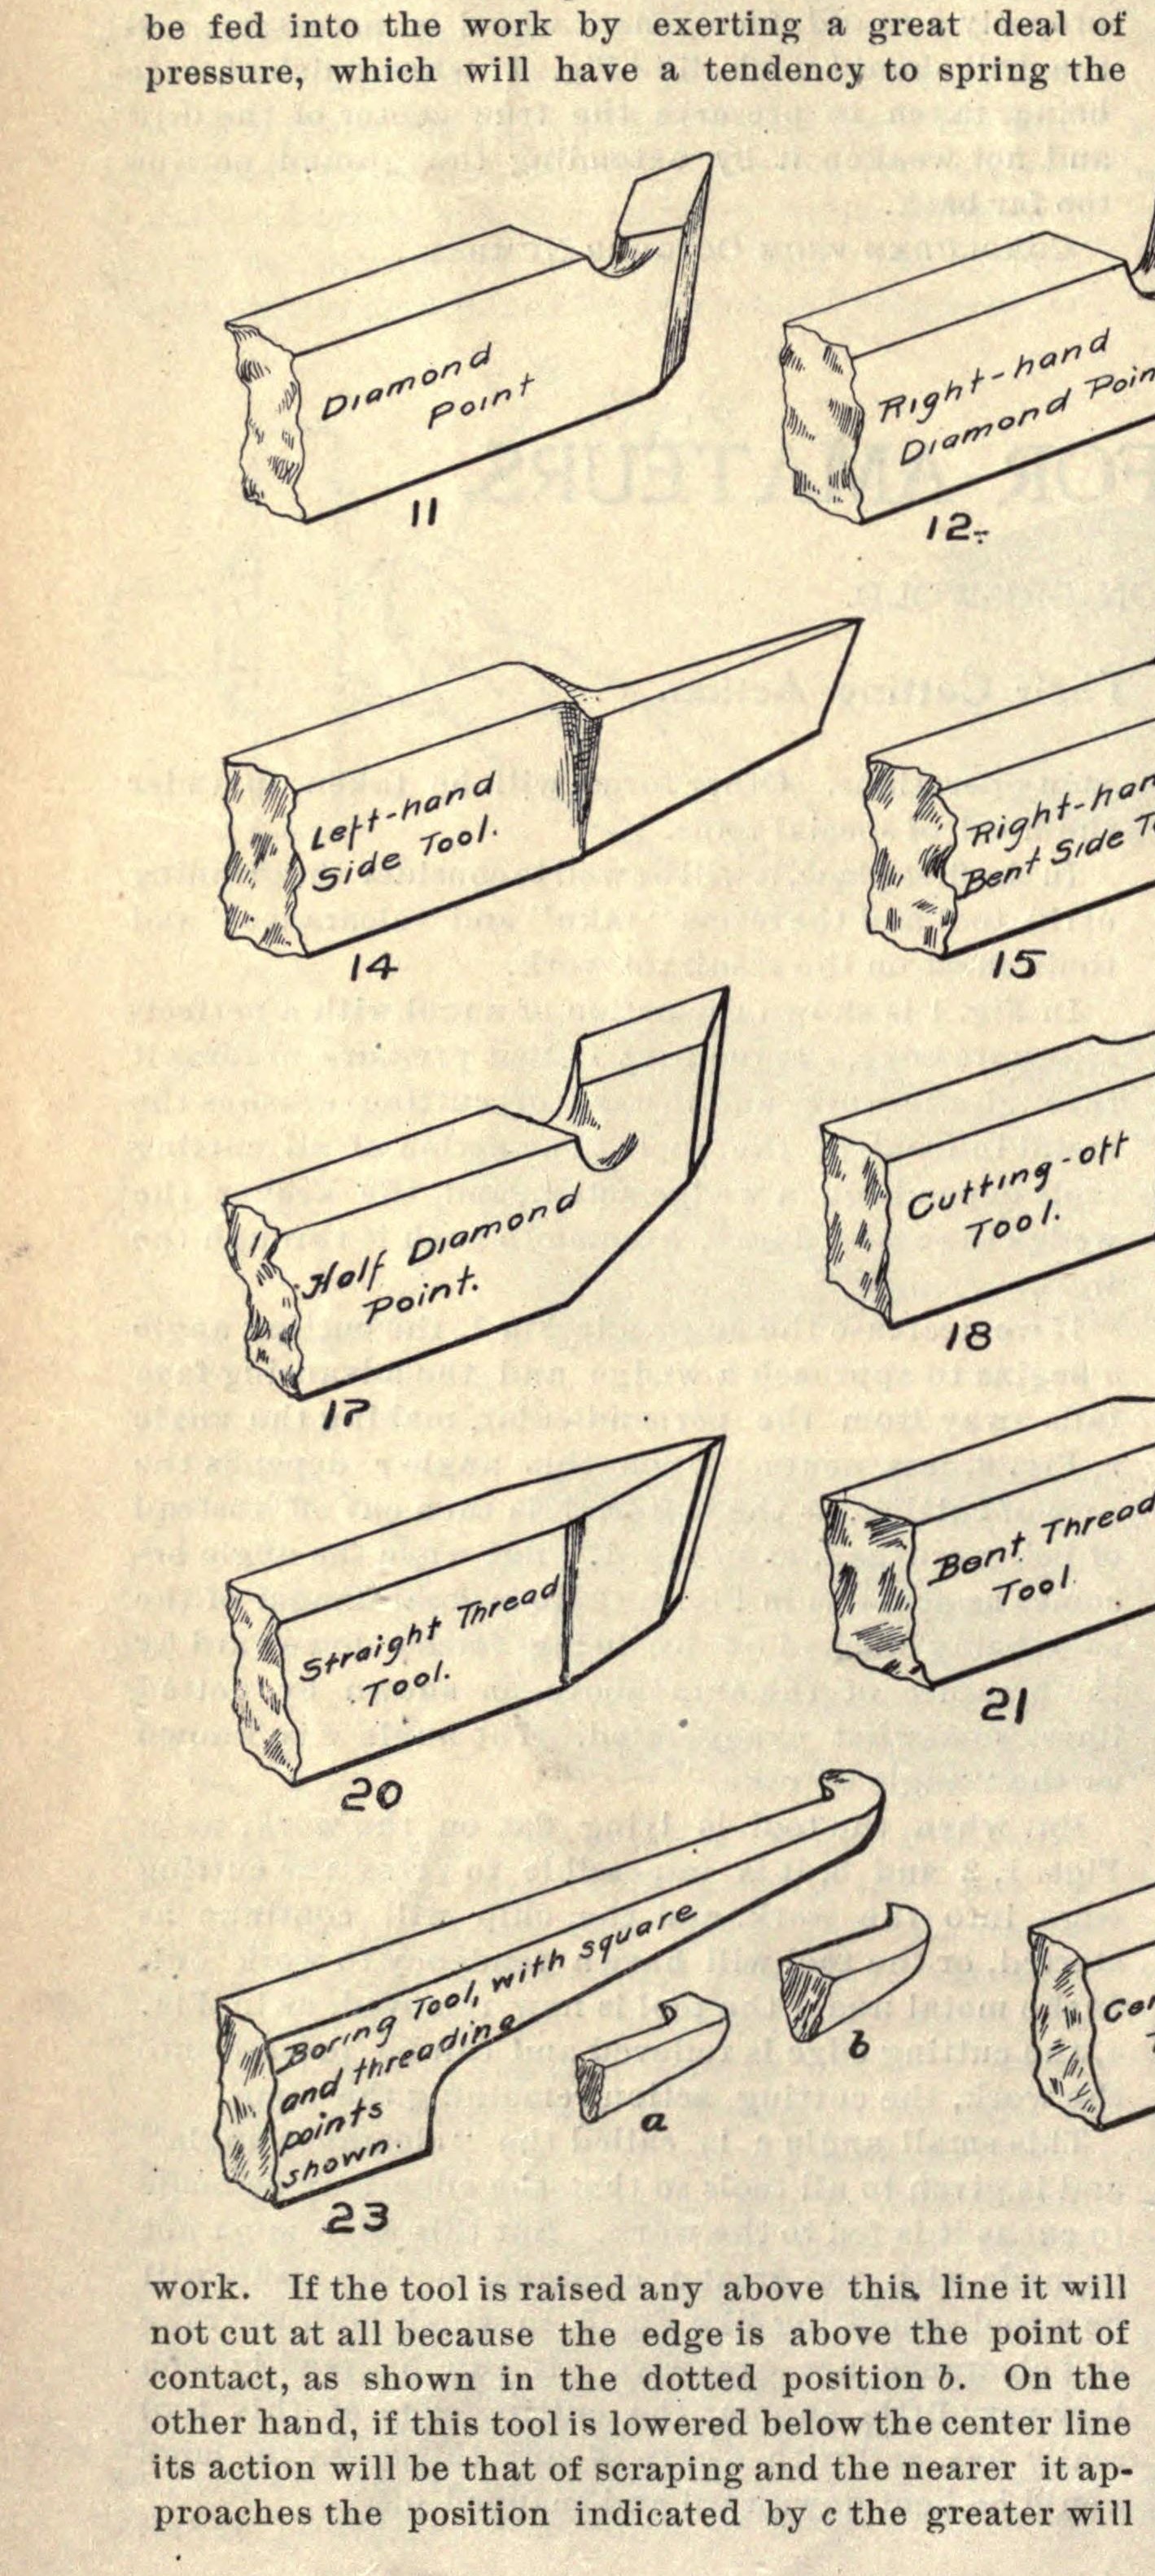

Forged Lathe Tools: Narrow Cutting-Off Tool and Bent-Tip Inside Boring Tool, Ground to Rake and Clearance (Griswold, 1904)
Two of the forged lathe tools in Robert Gibson Griswold's Tool Making for Amateurs (Boston, 1904): a cutting-off (parting) tool deep under a very narrow edge with relieved sides and a chip-splitting groove, and an inside boring and threading tool drawn to a long taper with the tip bent left; both ground to 3-5 degree clearance and the rake suited to the metal.
Avancé
Half a day per tool
Consignes
1
1
His angles
His angles
Chargement du notebook Jupyter…
2
2
Read Griswold
Read Griswold
"The writer uses a tool slightly less than 1-16 in. wide and 1 in. deep for short cuts."
3
3
Forge the cutting-off tool
Forge the cutting-off tool
Forge tool steel (stock size ours, to suit your tool post) into a blade deep under the cutting edge, with the point the widest part and the sides relieved behind it so it cannot bind (his fig. 18): slightly under 1/16 in. wide and 1 in. deep for work up to 1/2 in., about 3/32 in. wide for work up to 2 in.
Matériaux pour cette étape :
 Barre d'acier à outils1 pièce
Outils nécessaires :
 Forge de forgeron
 Enclume
 Marteau
 Pinces de forgeron
4
4
Forge the boring tools
Forge the boring tools
Draw three blanks to a long tapering end and bend the extreme tip to the left (fig. 23).
Matériaux pour cette étape :
Barre d'acier à outils1 pièceOutils nécessaires :
Forge de forgeronEnclumeMarteauPinces de forgeron5
5
Harden and temper
Harden and temper
Carbon tool steel: harden the ends (ours: cherry red into water) and temper in the yellows. Self-hardening steel must never be quenched in water.
Matériaux pour cette étape :
 Eau1 pièce
 Toile émeri1 pièce
Outils nécessaires :
Forge de forgeron Seau
6
6
Grind the cutting-off tool
Grind the cutting-off tool
Give it front and side clearance of 3-5 degrees and little top rake. For larger work grind a round groove in the facing edge so the chip splits into two strings.
Outils nécessaires :
 Touret à meuler
7
7
Grind the boring points
Grind the boring points
Grind one boring tool as a diamond point, one as a small square point that works into corners, and one as a 60 degree thread point. Rake 3-10 degrees for iron and steel, little or none for brass and copper; hone the edges.
Outils nécessaires :
Touret à meuler Pierre à aiguiser
8
8
Troubleshooting
Troubleshooting
Lathe tool troubleshooting.
Flow
Loading...
9
9
History and honest limits
History and honest limits
From Robert Gibson Griswold, "Tool Making for Amateurs" IV, **Amateur Work** (Boston), vol. IV (1904-05), pp. 23-26 and figs. 11-25 (checked on the archive.org scan amateurwork04bostrich). He shows a full set (diamond point, side, round-nose, thread, centering, brass tools); this blueprint makes the two our heads need. Stock size and quench are ours.
Matériaux
3- 1 pièceEspace réservé
- 1 pièceEspace réservé
- 1 pièceEspace réservé
Blueprints liés
Ces blueprints partagent des connaissances — techniques, matériaux ou principes
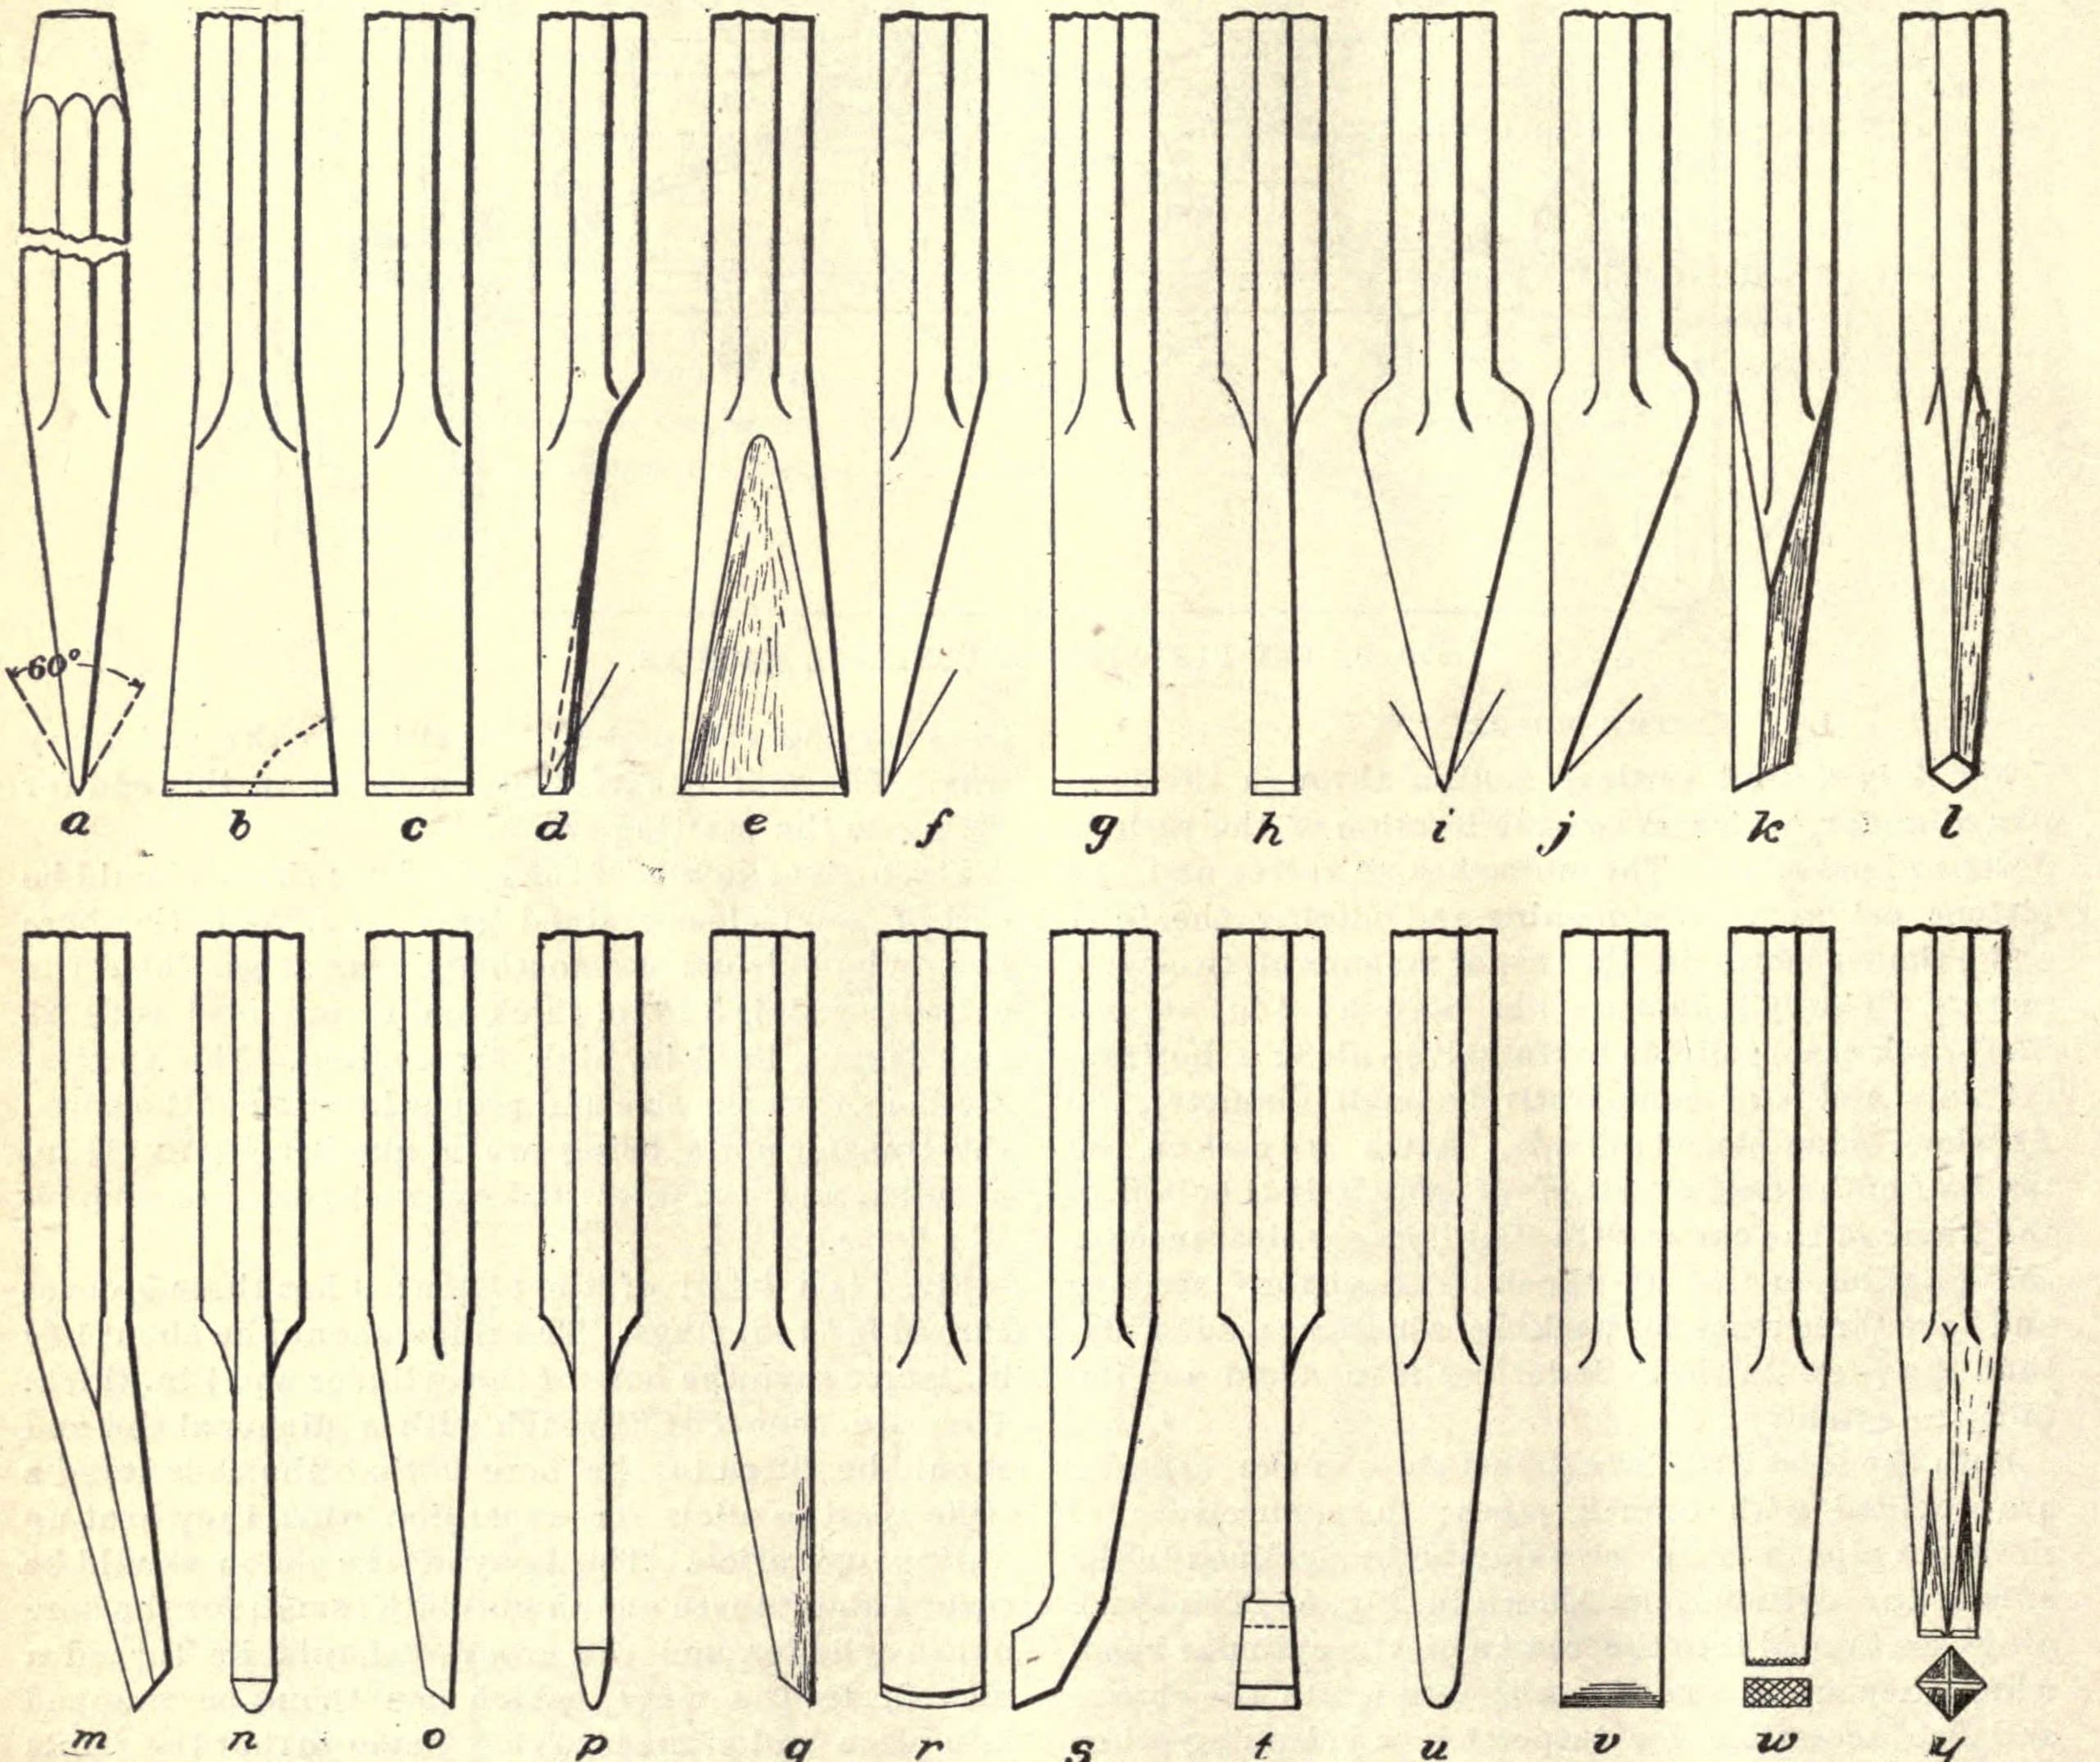
A Set of Cold Chisels: Flat, Gouge, Side, Cape, Diamond-Point and Round-Nose, Edge Hardened Only, Tempered Purple (Griswold, 1904)
par Forge
Travail des Métaux
11
0
0
0
0
0
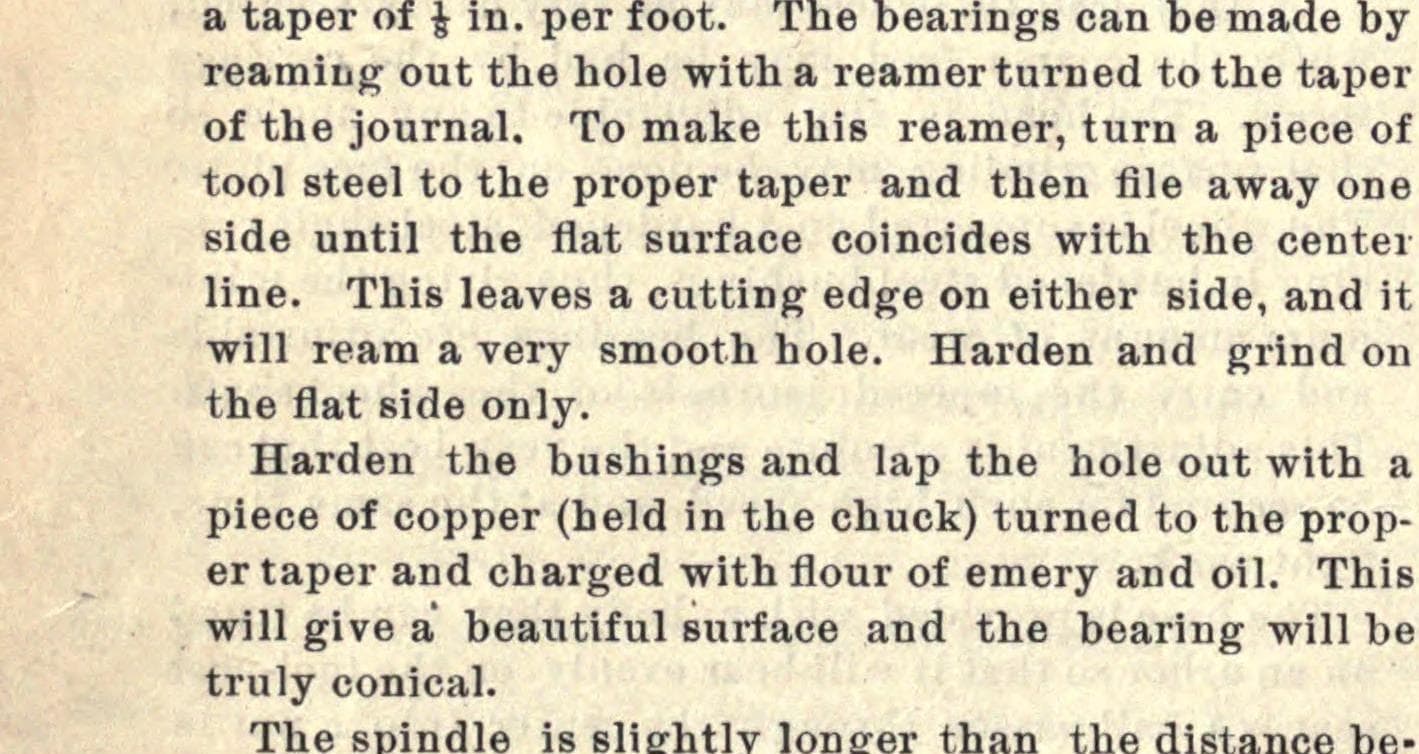
Half-Round Taper Reamer: Tool Steel Turned to the Taper, Filed Flat to the Centre Line, Hardened (Griswold, Amateur Work, 1905)
par Forge
Travail des Métaux
9
0
0
0
0
0
CC0 Domaine public
Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.
Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.