ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE

The Cast-Back Curry Comb: Iron Run Around Toothed Plates Held in a Notched Bar
A curry comb's toothed plates have to be fixed to a back and a handle, and riveting or soldering each plate is slow and works loose.
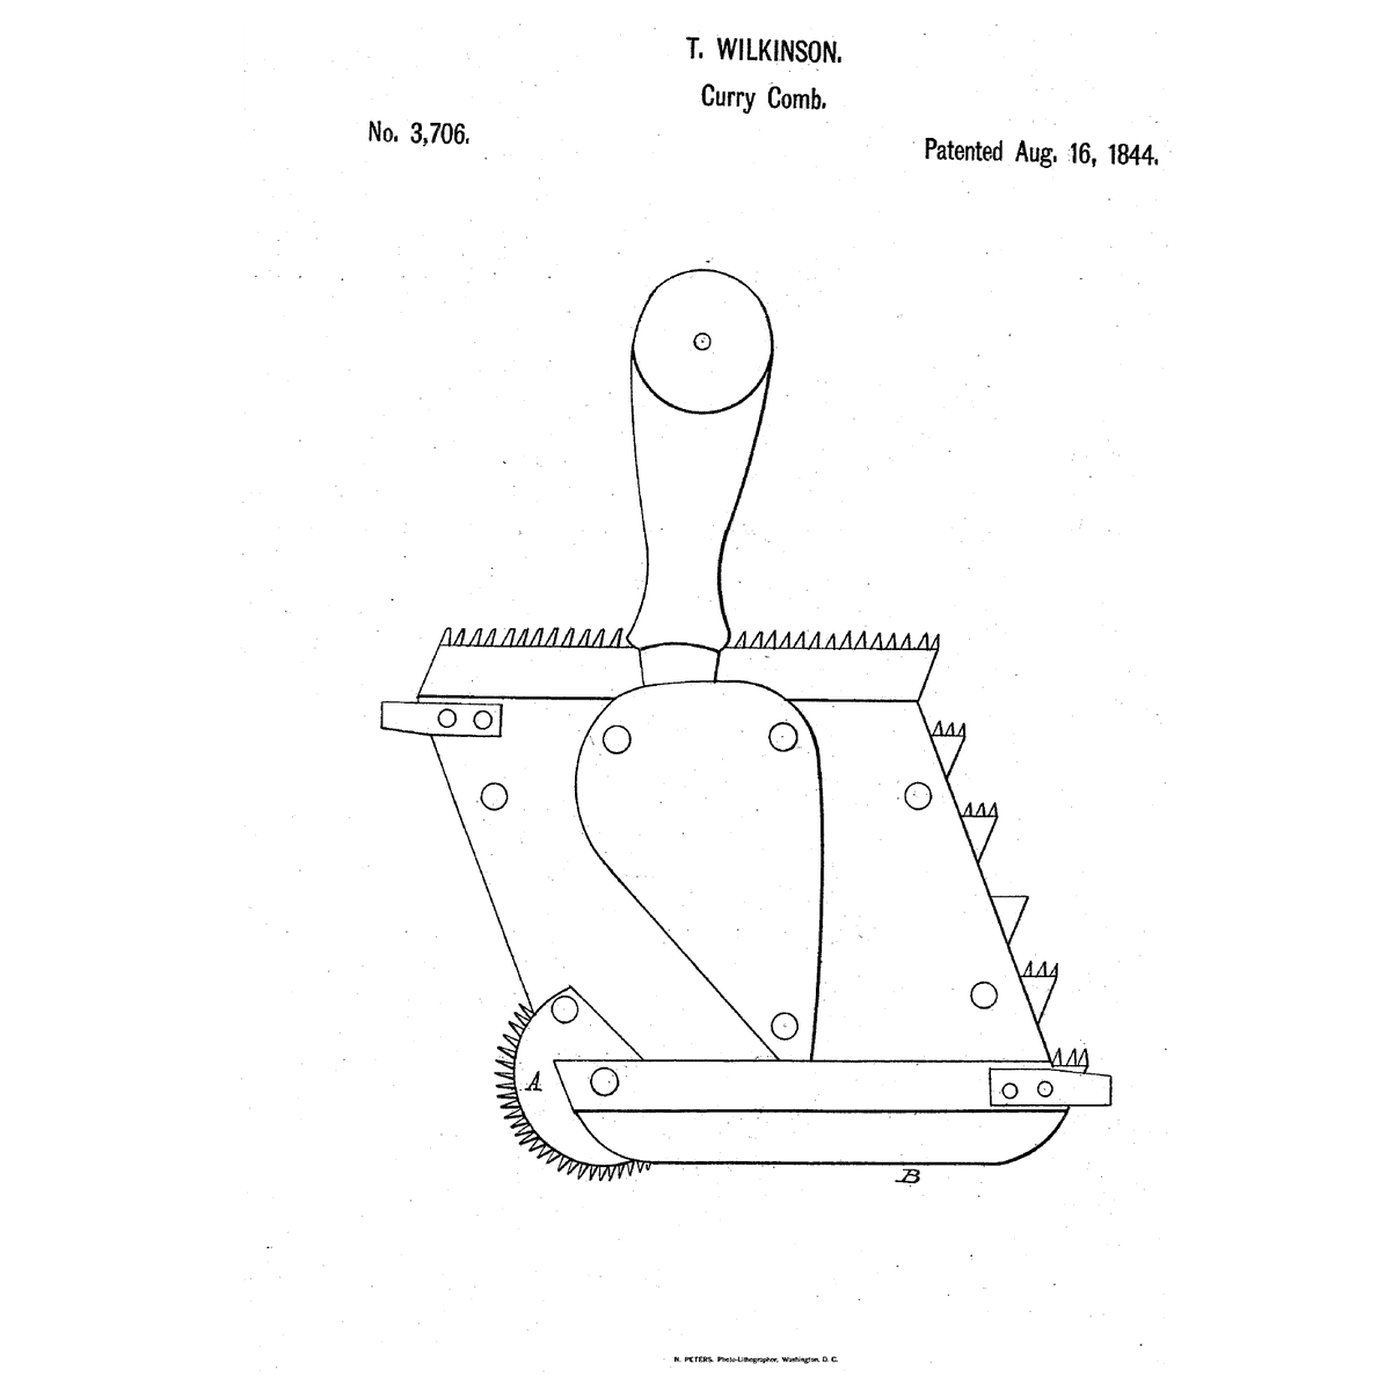
James M. Gardner of Troy, New York, received US 7,986, dated 18 March 1851, for an improvement in the method of casting the backs upon the teeth of curry combs. The teeth are cut in sheet-iron plates with dovetail projections on their other edges; a notched cross-bar in the cope holds the plates while the sand is rammed, and the back is cast onto them, with a ferrule cast onto an iron spike for the wooden handle, so that the plates are "firmly secured in the back by the running of the metal around the dovetail projections."
This rung works out the metal a back takes, then cuts toothed steel plates, holds them in a notched bar in a two-part sand mould and casts a pewter back onto them.
Avancé
About 6 hours
Consignes
1
1
Metal for the back
Metal for the back
Chargement du notebook Jupyter…
2
2
A two-part sand mould before it
A two-part sand mould before it
The embedded blueprint rams sand around a pattern in a two-part flask and pours metal into the space it leaves. Gardner uses the same flask and adds a notched bar in the cope that holds the toothed plates, so the back is cast onto them.
3
3
Read US 7,986
Read US 7,986
"In my improved method of making curry combs the teeth are cut in a series of sheet iron plates, which are arranged in a mold together with an iron spike to be driven into a wooden handle, and the back and ferrule cast on to secure the whole together and complete the comb."
"The cope is made with a cross-bar, h, having slots or notches i cut into it from its under edge, and corresponding with grooves j, made in the face d of the plate a."
"These notches and grooves hold the comb plates l in proper position, and then the cope is rammed full of sand, thus taking the impression of the face d of the plate a, and at the same time securing the comb-plates in the sand."
4
4
Mould the comb and cast the back
Mould the comb and cast the back
**Plates.** From 0.8 mm mild steel sheet cut six strips 9 × 2.5 cm with tin snips. Along one long edge snip V-notches 3 mm deep every 3 mm and file the teeth even. Along the other edge cut two tabs 5 mm deep that widen toward their ends, like dovetails.
**Pattern and bar.** Saw a hardwood pattern 11 × 9 cm and 8 mm thick for the back. Across one face saw six kerfs 5 mm deep and 15 mm apart, so a plate's tabs stand in each. Build a two-part flask from oak board. Across the top of the cope fix a hardwood cross-bar with six notches cut up from its under edge, right above the kerfs.
**Ram.** Sieve and temper the sand. Lay the pattern kerfed face down on a board, set the drag over it and ram it full, then turn it over so the kerfs face up. Stand the plates teeth up with their tabs in the kerfs. Dust with talc, set the cope on so each plate stands in its notch, and ram it full. Lift the cope: the plates come away held in its sand. Draw the pattern. Lay a 6 mm steel rod bent at one end in a groove cut from the cavity out through a hole in the drag frame, as the handle spike. Cut a sprue, a riser and vents, and close the flask.
**Pour.** Weigh out the pewter from the notebook. Melt it in the crucible with the torch, skim it, and pour once, steadily, until the riser stands full. When it has cooled, break it out, saw off the sprue and riser, and try to pull each plate out with pliers. Drill a hardwood handle a little under the spike's size and drive it on.
Matériaux pour cette étape :
 Tôle d'acier doux1 pièce
 Planche de bois dur1 pièce
 Planche de chêne blanc1 pièce
 Bloc de bois dur1 pièce
 Vis à bois16 pièces
 Sable de moulage1 pièce
 Talc1 pièce
 Rond en acier doux0.15 mètre
 Lingot d'étain1 pièce
 Creuset en argile profond1 pièce
Outils nécessaires :
 Cisaille à tôle
 Limes (lime à main)
 Étau d'établi
 Scie égoïne
 Scie à métaux
 Perceuse sans fil
 Jeu de forets
 Jeu de tournevis
 Crible
 Balance de cuisine numérique
 Chalumeau à propane
 Pince à creuset
 Écran facial
 Gants résistants à la chaleur
 Règle
5
5
A back that runs short, blows or lets go
A back that runs short, blows or lets go
Cast-back curry comb troubleshooting.
Flow
Loading...
6
6
History and honest limits
History and honest limits
**James M. Gardner** of Troy, Rensselaer County, New York, received US 7,986, dated 18 March 1851. His pattern plate a had one face b formed like the back of the comb and the other, d, like its under face, with grooves j opposite the ribs k. The plate was rammed face b upward in the nowel, which was turned over, and the cope e was set on with dowel pins f and g. After ramming, the cope came away with the plates; an iron chill or core n with an iron spike o went into the cavity p, the spike pushing out through a hole in the side of the nowel; and molten iron cast the back onto the sheet-iron plates and the ferrule q onto the spike, the chill forming the inside of the ferrule, which binds the wood of the handle r when it is driven on. His claim covers the notched bar with the cope of a two-part flask, holding the plates during the process.
**Honest limits.** Pewter stands in for cast iron, and the back is plain, without Gardner's ribs, ferrule or chill; a pewter back is softer than his. The notebook takes the back as a plain slab; its sizes and allowance are examples. Whether your plates hold is the result.
Matériaux
10- 1 pièceEspace réservé
- 1 pièceEspace réservé
- 1 pièceEspace réservé
- 1 pièceEspace réservé
- 16 piècesEspace réservé
- 1 pièceEspace réservé
- 1 pièceEspace réservé
- 0.15 mètreEspace réservé
- 1 pièceEspace réservé
- 1 pièceEspace réservé
Outils requis
15- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- 1 vendor sell this, none ship to you yetEspace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
Blueprints liés
Ces blueprints partagent des connaissances — techniques, matériaux ou principes
Sand Casting
par Forge
ARTISANAT
39
0
0
0
0
0

Casting Iron in a Cupola Furnace — Re-Melting Pig Iron into Finished Castings
par Piett
Travail des Métaux
44
0
0
0
0
0
The Hock Curry Comb: A Toothed Half-Circle for the Hollows
par Forge
Travail des Métaux
8
0
0
0
0
0
The Open-Back Curry Comb: Three Bent Troughs and No Back to Clog
par Forge
Travail des Métaux
9
0
0
0
0
0

The One-Sheet Curry Comb: Cut, Slit and Fold, With No Rivet and No Waste
par Mary
Travail des Métaux
9
0
0
0
0
0
CC0 Domaine public
Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.
Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.