
ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
The Pattern Is Not the Part: Draft, Shrinkage and Machining Allowance
Forge

Créé par

Forge

24. septembre 2026NO
17
0
0
0
0

The Pattern Is Not the Part: Draft, Shrinkage and Machining Allowance

A pattern is not a copy of the finished part. It is deliberately LARGER, deliberately TAPERED, and deliberately oversized wherever a machined surface will be cut — and each of those three differences has a separate reason. DRAFT is the taper that lets the pattern come out of the sand without tearing the mould. SHRINKAGE allowance makes the pattern bigger because metal contracts as it freezes and cools. MACHINING allowance leaves metal for the cutting tool to remove. Get any of the three wrong and the casting is scrap. Get them right and the same pattern makes identical parts indefinitely, which is the entire economic point of casting.
Intermédiaire
3 hours

Consignes

1

Draft: the pattern has to come out

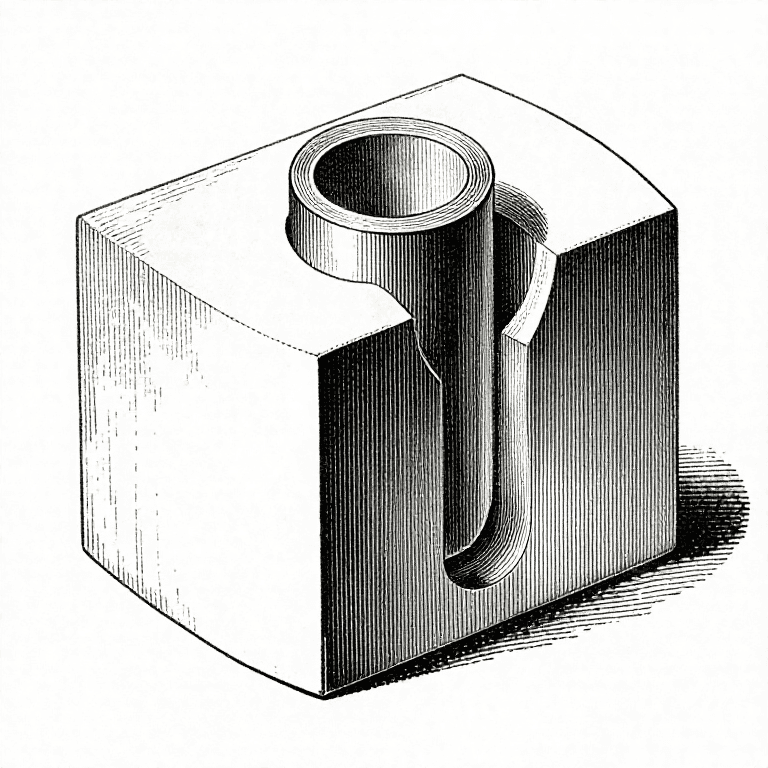
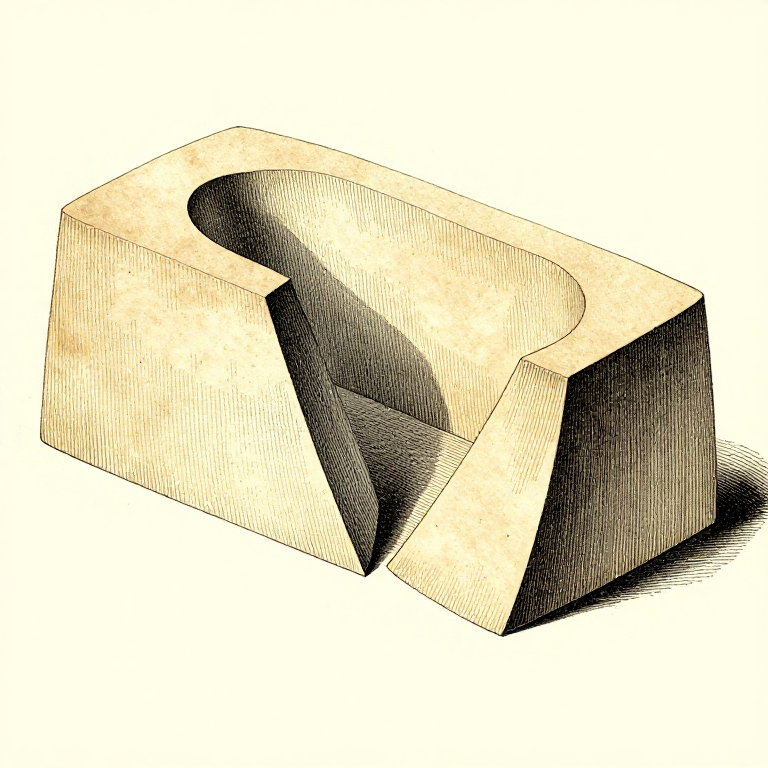
Every surface that runs perpendicular to the parting plane must be tapered so the pattern lifts cleanly. A vertical wall drags sand with it and leaves a torn mould, and that tear becomes a lump on the casting. One to three degrees is usual for sand casting, more for deep pockets and less for shallow ones. The rule of thumb is that a deeper draw needs more draft, because a small angle over a long distance still leaves the sand gripping. Draft always ADDS material away from the parting line, never removes it. A part that must be a precise size at the bottom of a deep feature has to be machined there, because draft is not optional and it is always in the direction that makes the casting thicker.

Matériaux pour cette étape :

Planche de bois durPlanche de bois dur1 pièce
Sable de moulageSable de moulage1 kg

Outils nécessaires :

Jeu de limesJeu de limes
Pied à coulisse numérique 6 poucesPied à coulisse numérique 6 pouces
RègleRègle
2

Shrinkage: build the pattern oversize by the right amount

Chargement du notebook Jupyter…

Matériaux pour cette étape :

Planche de bois durPlanche de bois dur1 pièce
Lingot de bronzeLingot de bronze1 pièce

Outils nécessaires :

Ordinateur de bureauOrdinateur de bureau
Pied à coulisse numérique 6 poucesPied à coulisse numérique 6 pouces
RègleRègle
3

Machining allowance goes only where a tool will cut

A cast surface is rough, slightly scaled, and not accurately placed. Any face that has to be flat, parallel or dimensionally exact must be machined, and the pattern has to carry extra metal there for the tool to remove. Two to five millimetres is typical for sand casting, and more on large surfaces and on the cope side — the upper half of the mould collects more inclusions, so critical machined faces are placed in the drag where possible. Do NOT add it everywhere. Extra metal is extra weight, extra cost, extra shrinkage to feed, and extra machining time. Deciding which faces are machined and which are left as-cast is a design decision made before the pattern is started.

Matériaux pour cette étape :

Planche de bois durPlanche de bois dur1 pièce

Outils nécessaires :

Pied à coulisse numérique 6 poucesPied à coulisse numérique 6 pouces
Jeu de limesJeu de limes
4

Finish the pattern properly, because it prints

Every scratch, dent and grain on the pattern is reproduced in the sand and then in the metal. A pattern sanded smooth and sealed gives a smooth casting; a rough one gives a rough one, and rough castings are harder to clean and harder to machine. Seal and wax wooden patterns. Bare wood absorbs moisture from green sand, swells and changes size, and it also grips the sand instead of releasing. Fillet every internal corner. A sharp internal corner in the pattern makes a sharp sand edge that breaks off into the casting, and it makes a stress concentration in the finished part — the same argument as a fillet in a printed part or a forged one.

Matériaux pour cette étape :

Planche de bois durPlanche de bois dur1 pièce
Cire d'abeilleCire d'abeille1 pièce

Outils nécessaires :

Jeu de limesJeu de limes

Loupe de bijoutierLoupe de bijoutier
Pied à coulisse numérique 6 poucesPied à coulisse numérique 6 pouces

Matériaux

4

Outils requis

5

CC0 Domaine public

Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.

Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.

Commentaires

(0)

Se connecter pour participer à la discussion

Chargement des commentaires...