هنر
زیبایی و سلامت
صنایع دستی
فرهنگ و تاریخ
سرگرمی
محیط زیست
غذا و نوشیدنی
مهندسی معکوس
علوم
ورزش
فناوری
پوشیدنیها

One Die Instead of Two: Forming Sheet Against Rubber
Every forming operation so far has needed two tools that fit each other: a punch and a die, machined to a clearance, in hardened steel. That is fine for a million cans and ruinous for forty aircraft ribs, because cutting the second tool costs as much as cutting the first and neither one makes anything by itself.
Henry Guerin's answer at Douglas Aircraft in the 1930s was to throw one of them away. Put a thick **rubber pad** in a retainer on the press ram; lay the form block on the bed with the sheet on top; close the press. The confined rubber flows round whatever is under it and presses the metal down onto the block.
Now only one tool has to be made, it can be wood or resin instead of tool steel, and it can be altered with a file. This rung builds that, works out what press it needs — honestly, because the answer is inconvenient — and forms a real flange.
پیشرفته
About 5 hours
دستورالعملها
1
1
Read the claim, and the chain of applications behind it
Read the claim, and the chain of applications behind it
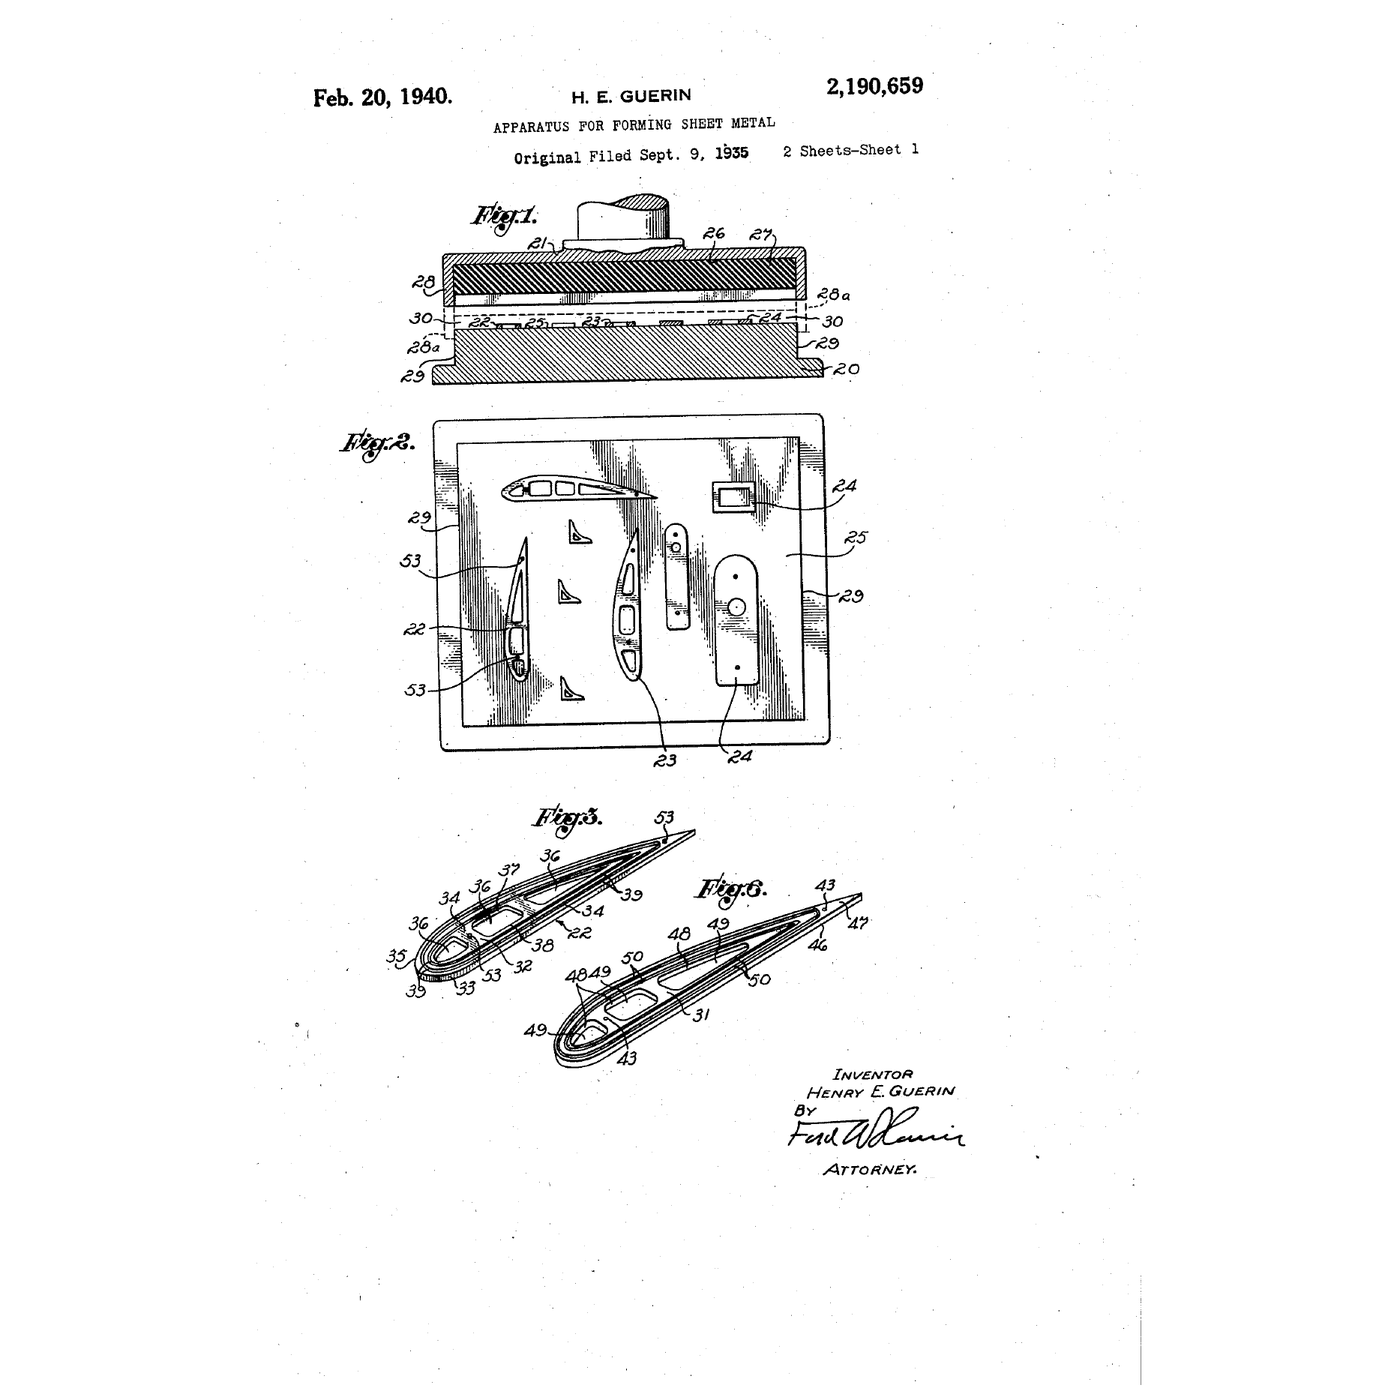
**US 2,190,659**, *Apparatus for forming sheet metal*, **Henry E. Guerin** of Beverly Hills, California, assignor to the **Douglas Aircraft Company** of Santa Monica; granted **20 February 1940**, long expired. The drawing on this page is the patent's own sheet 1.
Its front page is worth reading for the dates alone, because they tell you how long this took: the original application was filed **9 September 1935** and issued as **US 2,055,077** on 22 September 1936; a continuation followed in April 1936; and **this** application, a division, was filed **26 January 1939**. Five years of filings for one idea. When a later rung in some batch says an invention 'appeared in 1940', this is what that usually conceals.
The patent has **one claim**. The specification says what it is for in the first paragraph: forming sheet material into predetermined shape, *particularly to an improved method and apparatus whereby sheet metal may be economically and expeditiously formed into desired shapes*, and it is explicit that the case it cares about is **small quantities of a great many different parts** — *the airplane building industry is necessarily to employ metal members which are made from sheet metal*, in *a relatively few shapes of the same size and configuration*.
That is the economic argument in the patent's own words, and it is the point of the whole rung: *if such ribs are made in accordance with standard practice of making die and punch blocks, there is a considerable investment in such parts since it is well known that a very accurate three-dimensional relationship must be adhered to.* Guerin removes half of that investment.
2
2
Make the form block — and notice what it is made of
Make the form block — and notice what it is made of
The form block is the *only* shaped tool in this process, and the whole saving is that it does not have to be hardened steel.
Make a simple one: a plate about 80 × 60 mm with a rounded profile on one long edge, plus a cut-out or two. Options, and try more than one if you can:
- **MDF or plywood**, cut on the bandsaw and filed. Good for a handful of parts. It will crush at the edges eventually, and you will see exactly where.
- **Cast polyurethane resin**, poured into a mould. Tougher than wood, cheap, and it takes fine detail.
- **Aluminium plate**, filed and sanded. Effectively permanent at this scale.
Whatever you use, the **edge radius matters more than anything else**. A sharp edge on a form block cuts the sheet rather than forming it — the rubber presses the metal hard onto that edge and there is nothing to stop it. Break every edge to at least 1.5 times the sheet thickness and polish it; a scratch on the block prints on every part.
Make the block **thicker than the flange is tall**, so the rubber can wrap the sheet all the way down and still be clear of the bed.
Finally, fix the blank to the block so it cannot move. Two small dowel pins through matching holes in the blank is the classical answer and it is what the patent's figures show. A blank that shifts under the pad makes a part that is the right shape in the wrong place.
مواد مورد نیاز این مرحله:
 ورق امدیاف1 قطعه
 ورق تختهسهلا1 قطعه
 رزین ریختهگری پلییورتان (زودگیر)1 قطعه
 ورق آلومینیوم (6061-T6)1 قطعه
ابزارهای مورد نیاز:
 دریل ستونی
 سوهان (سوهان دستی)
 مجموعه سوهان
 فرز انگشتی
 کولیس دیجیتال ۶ اینچی
 گونیای ترکیبی
 خطکش
 خطکش الماسه
 ماژیک ثابت
 عینک ایمنی شفاف
 دستکش کار چرمی
3
3
Confine the pad, and form something
Confine the pad, and form something
Build the retainer first, because an unconfined pad does nothing. A steel box open on one face, deep enough to hold a stack of rubber sheet 25–40 mm thick, with walls stiff enough not to bulge. Weld it, or bolt it up out of plate. It sits open-face-down on the press ram.
Stack natural rubber sheet — about 50–60 Shore A — into the box until it stands a little proud of the rim. Several thinner sheets work as well as one thick block and are easier to buy.
Then, on the press bed: form block, blank pinned to it, and the retainer lowered over the top. Press **slowly**, and watch the rubber. It should bulge only where the part is, and the box should not visibly deform. If the box is bulging, it is the box that is being formed and not the metal.
Start with 0.8 mm annealed aluminium and a shallow flange. Step 5 says why: a 12 tonne press covers about 77 mm square at the pressure a soft aluminium flange needs, and nothing at all at the pressure a sharp detail needs. **Keep the part small and the detail soft**, and the process works on a bench press; ask for more and you need an aircraft factory.
Look at the result. The face against the block is crisp; the face against the rubber is slightly soft and carries no tool marks at all, which is the process's signature and the reason it was liked for visible skins. Measure the flange height round the part — it will vary, and where it varies tells you where the rubber ran out of pressure.
Keep clear of the press and never reach under a loaded ram. A confined rubber pad stores real energy, and if the retainer lets go it lets go sideways.
مواد مورد نیاز این مرحله:
 ورق لاستیک3 قطعه
 ورق آلومینیوم2 قطعه
 ورق فولاد نرم1 قطعه
ابزارهای مورد نیاز:
 پرس کارگاهی هیدرولیک (۱۲ تن)
 زیرگذار لاستیکی قالبگیری
 گیرهٔ رومیزیکولیس دیجیتال ۶ اینچی
 میکرومترخطکش
 ابزار پلیسهگیری
 سپر صورتعینک ایمنی شفافدستکش کار چرمی
 دفتر آزمایشگاه (با نسخهٔ کپی)
4
4
Try a shrink flange and a stretch flange on the same block
Try a shrink flange and a stretch flange on the same block
Cut a second form block with one **concave** edge and one **convex** edge of the same radius, and form a flange along both in one hit. They will not behave the same, and the difference is the most useful thing in this rung.
**The concave edge** gives a *shrink flange*. Its metal has to fit into a smaller circumference than it started in, so it is in compression, and it **buckles** — a series of small waves along the flange, or one big one.
**The convex edge** gives a *stretch flange*. Its metal has to reach round a larger circumference, so it is in tension, and it **cracks** — starting at the free edge, usually exactly where rung 1's sheared edge left its roughest fracture zone.
Step 5 computes how much shrink or stretch each radius demands. Compare it against the cupping and *n* figures from rung 6, and you can predict which of your blocks is formable before you press it.
Three fixes, all of which the aircraft industry used:
1. **Anneal.** A soft temper takes far more of both. Form soft, then age or heat-treat if the alloy allows it.
2. **Deburr and polish the blank edge.** A stretch flange cracks from the edge, so the quality of rung 1's cut is the dominant variable — this is the most common fix and the cheapest.
3. **Split the job.** Rubber-pad form what you can, then finish the awkward flange by hand over a stake with a mallet, shrinking the waves out. That combination — machine for the bulk, hand for the difficult edge — is exactly how it was done.
مواد مورد نیاز این مرحله:
ورق آلومینیوم2 قطعهورق امدیاف1 قطعهورق لاستیک2 قطعهابزارهای مورد نیاز:
پرس کارگاهی هیدرولیک (۱۲ تن) سندان شکلدهی
 سندان بالاآوری
 چکش لاستیکی
 چکش بیبرگشتسوهان (سوهان دستی)ابزار پلیسهگیری
 میکروسکوپ رقمیکولیس دیجیتال ۶ اینچیعینک ایمنی شفافدستکش کار چرمیدفتر آزمایشگاه (با نسخهٔ کپی)
5
5
Confinement, pressure and the size of part a press can cover
Confinement, pressure and the size of part a press can cover
در حال بارگذاری دفترچهٔ Jupyter…
ابزارهای مورد نیاز:
 کاغذ شطرنجی
6
6
History and context
History and context
**Attribution.** US 2,190,659, *Apparatus for forming sheet metal*, Henry E. Guerin, assignor to Douglas Aircraft Company; original application 9 September 1935 (issued as **US 2,055,077**, 22 September 1936), continuation April 1936, this divisional application 26 January 1939, granted 20 February 1940. Both expired. The drawing on this page is the patent's own.
**Why an aircraft company.** A car maker stamps one body panel a million times and can afford matched steel dies. An aircraft maker in the 1930s needed hundreds of *different* ribs, frames, clips and stiffeners, in runs of dozens. The tooling, not the metal, was the cost — and half of it was the die that mirrors the punch. Guerin's process deletes that half and, more importantly, lets the remaining half be made in wood by a pattern maker rather than in tool steel by a die sinker. When a design changed, you made a new block in an afternoon.
The process ran right through the war and is still in use; later variants — Verson-Wheelon with a rubber bag and hydraulic pressure behind it, and fluid-cell presses — are the same idea with the pressure raised so that deeper parts become possible.
**The principle worth keeping.** Replace one precise tool with an **indifferent medium under pressure**. The rubber does not need to know the shape; it simply has nowhere else to go. The same move turns up in hydroforming, in explosive forming, in vacuum bagging a composite and in an isostatic press, and every time it converts a tooling problem into a pressure problem.
**Honest limits, and they are severe at bench scale.** Pressure has to be applied over the whole plan area at once, so press force scales with part area — step 5's table is the reason a small shop can do a 77 mm flange and not a 300 mm one. Depth is limited: this is a flanging and beading process, not a deep-drawing one, because the rubber cannot hold a blank down and draw it in the way a blank holder does. The rubber wears and takes a permanent set, so pads are consumables. And the face against the pad is never as crisp as a matched-die part — which was a feature for aircraft skins and is a defect if you wanted detail on both sides.
مواد
7- 1 قطعهجایگزین
- 1 قطعهجایگزین
- جایگزین
- 1 قطعهجایگزین
- 3 قطعهجایگزین
- 2 قطعهجایگزین
- 1 قطعهجایگزین
ابزارهای لازم
24- جایگزین
- جایگزین
- جایگزین
- 1 vendor sell this, none ship to you yetجایگزین
- جایگزین
- جایگزین
- جایگزین
- جایگزین
- جایگزین
- جایگزین
- جایگزین
- پرس کارگاهی هیدرولیک (۱۲ تن)10% کمیسیونجایگزین
- جایگزین
- جایگزین
- جایگزین
- جایگزین
- جایگزین
- دفتر آزمایشگاه (با نسخهٔ کپی)10% کمیسیونجایگزین
- جایگزین
- جایگزین
- جایگزین
- چکش بیبرگشت10% کمیسیونجایگزین
- جایگزین
- جایگزین
نقشههای مرتبط
این نقشهها دانش مشترکی دارند — تکنیکها، مواد یا اصول




CC0 مالکیت عمومی
این نقشه تحت مجوز CC0 منتشر شده است. شما آزاد هستید آن را کپی، ویرایش، توزیع و برای هر هدفی بدون نیاز به اجازه استفاده کنید.
با خرید محصولات از طریق نقشه از سازنده حمایت کنید و او کمیسیون سازنده تعیین شده توسط فروشندگان، دریافت میکند یا یک نسخه جدید از این نقشه ایجاد کنید و آن را به عنوان اتصال در نقشه خود قرار دهید تا درآمد به اشتراک گذاشته شود.