هنر
زیبایی و سلامت
صنایع دستی
فرهنگ و تاریخ
سرگرمی
محیط زیست
غذا و نوشیدنی
مهندسی معکوس
علوم
ورزش
فناوری
پوشیدنیها
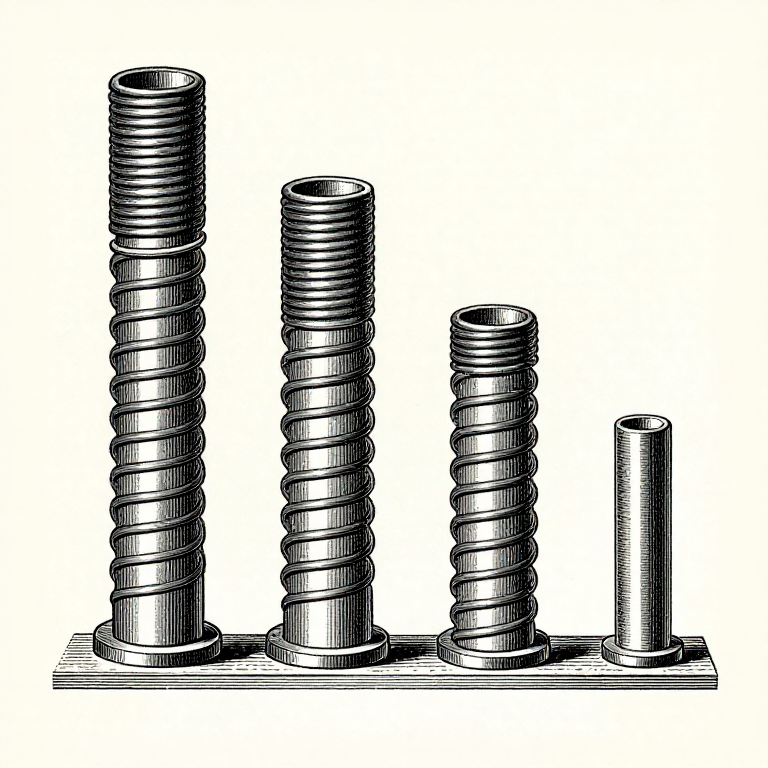

Set and Presetting: Why a Spring Goes Weak Without Getting Softer
'The spring has gone weak' is one of the most common diagnoses in a workshop and one of the most commonly wrong. A spring's rate comes from its wire, its coil diameter and its coil count, and none of those change in service. A spring that gives less force is almost always a spring that has got SHORTER.
That distinction is worth more than it sounds, because it turns a vague complaint into two measurements — free length and rate — whose four possible combinations each name their own cause. And the commonest cause of all turns out not to be the spring at all, but the assembly it sits in.
This rung is set and what it costs, why the same set is far worse on a short-travel spring, and presetting — the trick of deliberately ruining a spring in the factory so it cannot be ruined in service.
متوسط
3 hours
دستورالعملها
1
1
What set is, and where it comes from
What set is, and where it comes from
**Set is permanent deformation from overload.** Push a spring past the point where the wire yields in torsion and the wire does not spring all the way back. The spring is now shorter. Its rate is unchanged, because rate depends on geometry and modulus and neither has moved.
**It happens at the inside of the coil first**, for exactly the reason the index rung gave: that is where the stress is highest. So set begins long before the average stress reaches yield.
**Three ways a spring gets overloaded.**
*Once, hard.* Someone pressed it solid, or the mechanism was assembled with the spring compressed further than the design intended. One event, all the set at once.
*Slowly, at temperature.* Steel relaxes under sustained stress, faster as it gets hotter. A spring held compressed in a hot place loses force over months. This is why spring specifications carry a maximum service temperature, and why an engine valve spring and a door spring are different animals.
*Repeatedly, just below yield.* Many cycles near the limit accumulate a little set each time. The free length drifts down and then stabilises.
**What set is NOT.** It is not fatigue — fatigue cracks and breaks, set just shortens. It is not wear. It is not corrosion, though corrosion makes everything else worse.
**And it is not always bad.** Doing it deliberately, in the factory, is the subject of step 3.
مواد مورد نیاز این مرحله:
 مجموعه فنرهای فشاری1 قطعه
ابزارهای مورد نیاز:
 خطکش
 کولیس ورنیه
 نیروسنج (ترازوی فنری)
2
2
What set costs, and telling the four failures apart
What set costs, and telling the four failures apart
در حال بارگذاری دفترچهٔ Jupyter…
ابزارهای مورد نیاز:
 رایانهٔ رومیزی
3
3
Presetting: taking the set on purpose
Presetting: taking the set on purpose
**The trick.** Make the spring longer than it needs to be, then compress it solid, hold it, and let it go. It takes its set there and then, in the factory, and comes back to the free length that was actually wanted. The trade name for doing it repeatedly is **scragging**.
**What it buys.** Two things. First, the spring can no longer take a set in service, because it has already taken all it is going to at that stress — so its free length is now stable. Second, and less obviously, yielding the surface layers leaves a **residual stress** in the wire of the opposite sign to the working stress. The service load now has to overcome that residual before it does any damage, so the spring can safely carry a higher working stress than an unpreset one of the same material.
**What it costs.** A longer blank, one extra operation, and the fact that the final free length is now a result rather than a setting — so it must be measured and the blank length adjusted until it comes out right. On a production run that is a setup cost; on a one-off it is guesswork.
**When it matters.** Anywhere the spring is highly stressed and must hold its force: valve springs, clutch springs, anything preloaded for the life of the assembly. Catalogue springs for general use are often not preset, which is one reason a catalogue spring drifts where a purpose-made one does not.
**The direction matters.** Presetting only helps in the direction it was done. A compression spring preset by squashing is stronger in compression and no better the other way. So a spring that will be loaded both ways cannot be preset, and that is one reason a spring that is cycled through zero is a harder design problem.
**Do not preset in the field.** Squashing an installed spring solid to 'set it' removes free length you did not intend to lose and gives up force you needed. This is a factory operation on an oversized blank, not a repair.
مواد مورد نیاز این مرحله:
مجموعه فنرهای فشاری1 قطعه مجموعه فنر فشاری1 قطعه
ابزارهای مورد نیاز:
 گیرهٔ رومیزیخطکشکولیس ورنیه
4
4
Designing so it does not happen
Designing so it does not happen
**Work the spring at a low fraction of its allowable stress.** The cheapest insurance there is. A spring at 40% of allowable will hold its length indefinitely at room temperature; one at 80% will drift.
**Give it a long working deflection.** The notebook makes the case: the same absolute set costs far less force when the working deflection is large. Long soft springs hold their force; short stiff ones do not.
**Fit a stop.** If nothing can press the spring solid, it cannot take a set from a single overload event. This is usually a cheaper change than a better spring.
**Check the temperature honestly.** Not the ambient — the temperature of the spring, which may be sitting against something hot. Carbon steel springs are usually limited to around 120 °C for sustained load; above that the material has to change, to a chrome-silicon or chrome-vanadium alloy, or to stainless, or to Inconel for the really hot cases. The rate falls slightly with temperature too, because the modulus does.
**Specify preset springs where it matters**, and say so on the drawing — 'preset to solid' is a manufacturing instruction, not a wish.
**And record the free length at fitting.** Written down, on the machine's record. It converts a future argument about whether the spring has gone weak into one measurement and a subtraction, which is the whole of this rung.
مواد مورد نیاز این مرحله:
مجموعه فنرهای فشاری1 قطعهابزارهای مورد نیاز:
خطکشکولیس ورنیهمواد
2- 1 قطعهجایگزین
- 1 قطعهجایگزین
نقشههای مرتبط
این نقشهها دانش مشترکی دارند — تکنیکها، مواد یا اصول


CC0 مالکیت عمومی
این نقشه تحت مجوز CC0 منتشر شده است. شما آزاد هستید آن را کپی، ویرایش، توزیع و برای هر هدفی بدون نیاز به اجازه استفاده کنید.
با خرید محصولات از طریق نقشه از سازنده حمایت کنید و او کمیسیون سازنده تعیین شده توسط فروشندگان، دریافت میکند یا یک نسخه جدید از این نقشه ایجاد کنید و آن را به عنوان اتصال در نقشه خود قرار دهید تا درآمد به اشتراک گذاشته شود.