هنر
زیبایی و سلامت
صنایع دستی
فرهنگ و تاریخ
سرگرمی
محیط زیست
غذا و نوشیدنی
مهندسی معکوس
علوم
ورزش
فناوری
پوشیدنیها
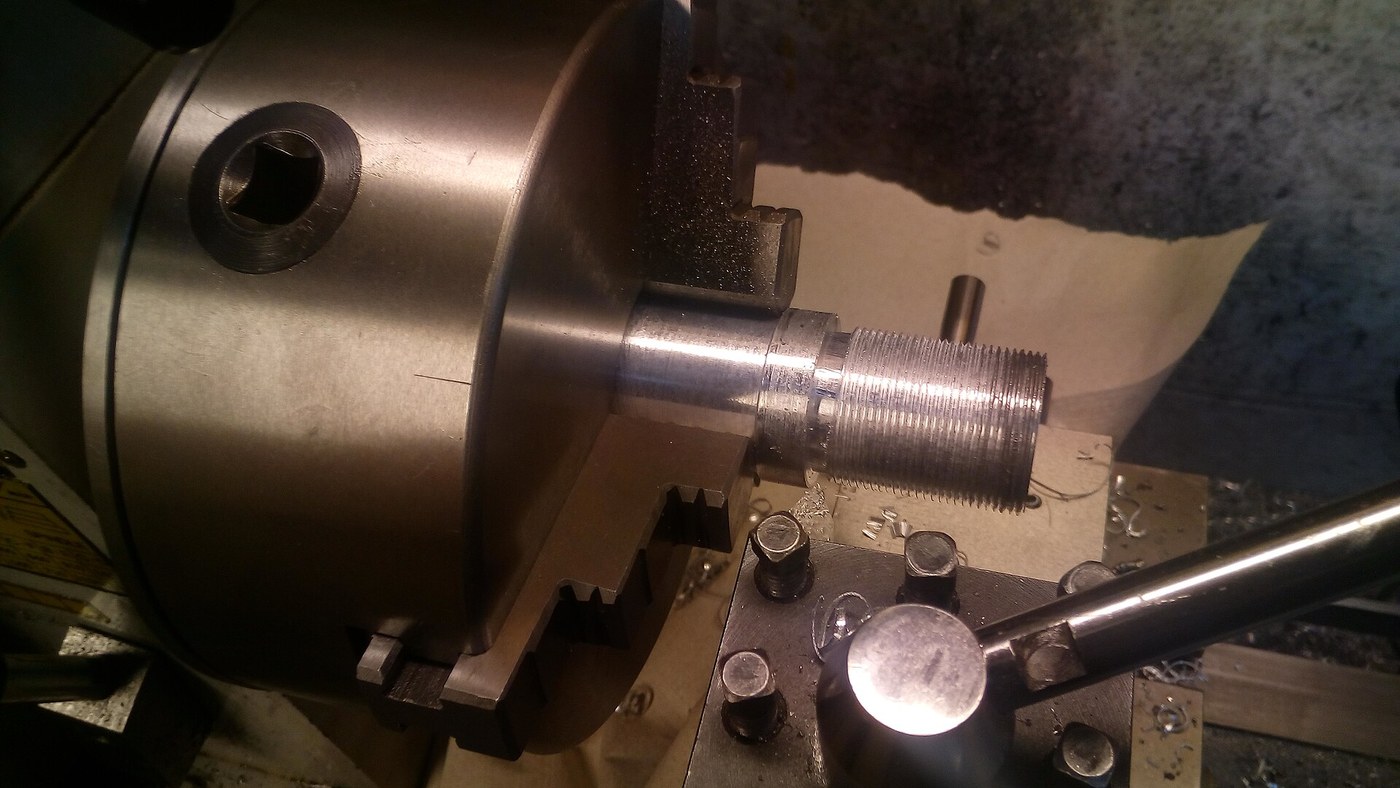

Single-Point Screw Cutting: Making a Thread the Lathe Has Never Seen
A tap and die cut the threads somebody else decided to make. Single-point screw cutting makes any thread at all — a worn imperial size nobody stocks, an oversize repair thread, a left-hand lead screw, a square thread for a vice — from a bar and a ground tool.
The idea is simple and the consequence is enormous. Couple the carriage to the spindle through gears so that the tool advances a fixed distance per revolution, and the tool traces a helix. Choose the gear ratio and you have chosen the pitch.
This is the operation that makes a lathe a machine TOOL rather than a machine: it can produce the lead screws that other lathes are built from, which is why the screw-cutting lathe published here is described as the machine that makes other machines.
پیشرفته
5 hours
دستورالعملها
1
1
Turn the blank, and leave the crest short
Turn the blank, and leave the crest short
Turn the outside diameter to the thread's major diameter, and chamfer the leading end at about 45 degrees down past the thread depth.
Turn it a few hundredths UNDER nominal rather than exactly on. A single-point tool with a sharp point leaves no crest flat, and a thread cut to the full nominal diameter finishes with a thin feather-edged crest that tears and does not gauge properly. The standard form has a flat on the crest, and turning slightly undersize produces it for free.
The chamfer matters for the same practical reason a bolt has one: it starts the nut, and it stops the first thread being a fragile knife-edge that gets knocked off in a drawer.
مواد مورد نیاز این مرحله:
 میلهٔ گرد فولاد نرم1 قطعه
ابزارهای مورد نیاز:
 تراش فلز
 ست ابزار تراش (HSS)
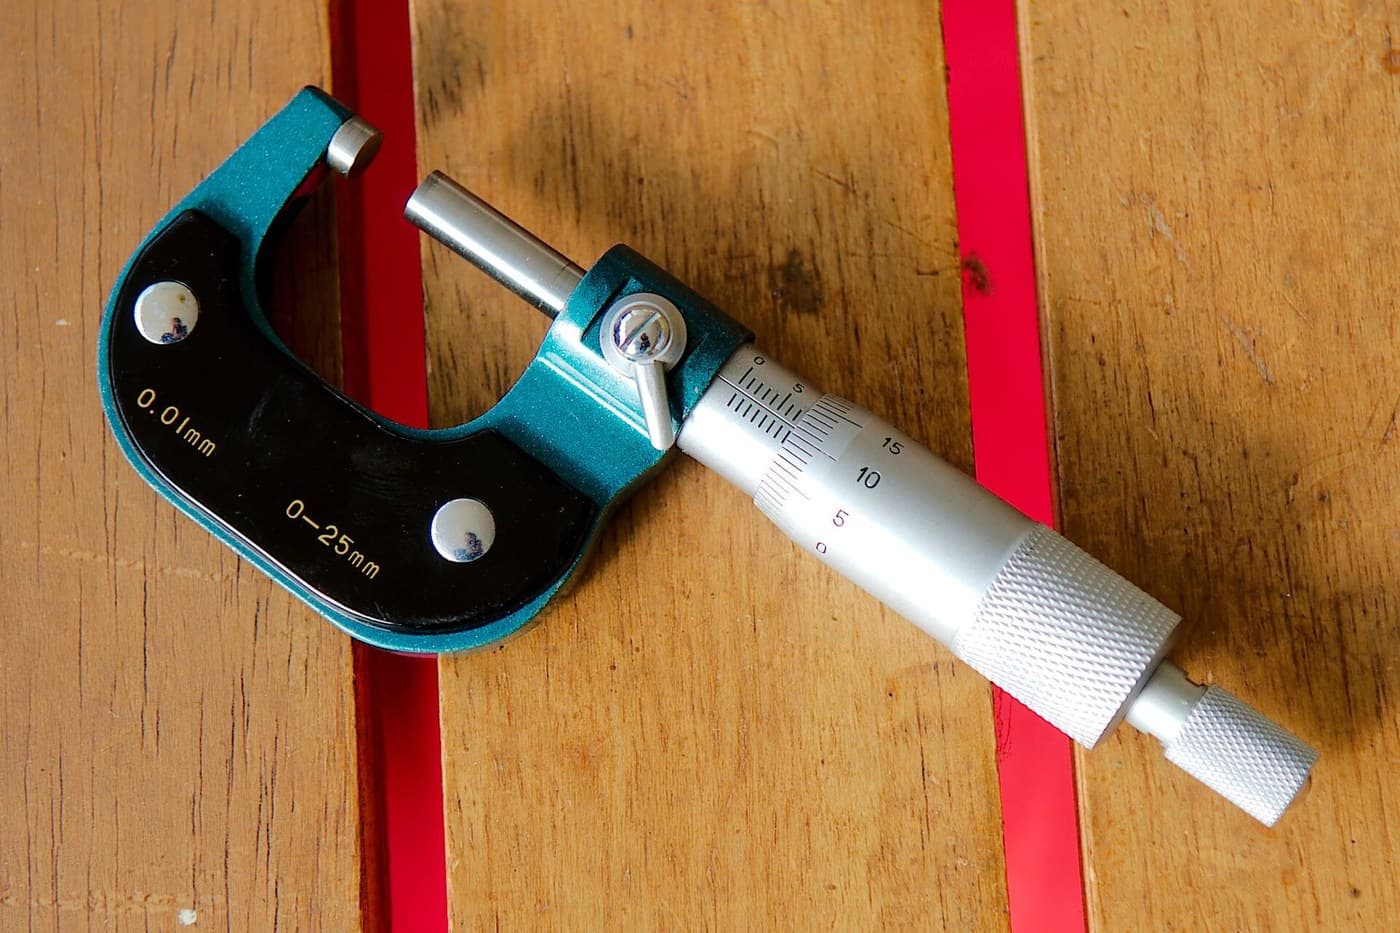
 میکرومتر
2
2
Set the gears, the tool and the compound
Set the gears, the tool and the compound
Set the change gears or the gearbox for the pitch you want, grind or fit a 60 degree tool for a metric or unified thread, and set it SQUARE to the work with a thread gauge against the turned diameter.
A tool set even a degree out of square cuts a thread with unequal flank angles that will not fit a standard nut properly, and no amount of careful infeed fixes it afterwards.
Swing the compound slide to 29.5 degrees from the cross-slide direction and feed in with the COMPOUND rather than straight in. At that angle almost all the cutting is done by the leading flank alone, with the trailing flank just skimming — one edge cutting instead of three, which means less force, less chatter and a far better finish.
ابزارهای مورد نیاز:
تراش فلزست ابزار تراش (HSS) شابلون رزوه
3
3
Pitch, depth and how many passes
Pitch, depth and how many passes
در حال بارگذاری دفترچهٔ Jupyter…
ابزارهای مورد نیاز:
تراش فلز ماشینحساب
 دفترچه
4
4
The first pass is a scratch, and you check it
The first pass is a scratch, and you check it
Take a first pass so light it barely marks the work, then stop and measure the pitch of the scratch with a rule over ten threads, or with a thread gauge.
If the gears are wrong you have lost nothing. If you had gone straight to depth you would have cut a full thread of entirely the wrong pitch, and the blank is scrap. Ten threads measured over their length divides the reading error by ten, which is what makes a steel rule adequate for the check.
Withdraw the tool at the END of every pass before reversing, and return to the same starting point each time. On a metric thread cut with a metric lead screw you can usually use the thread dial; where the pitches are not related, keep the half-nuts engaged and reverse the spindle instead, because disengaging loses the relationship between tool and helix and the next pass cuts a second thread beside the first.
مواد مورد نیاز این مرحله:
میلهٔ گرد فولاد نرم1 قطعهابزارهای مورد نیاز:
تراش فلزشابلون رزوه کولیس ورنیه
5
5
Fit it to the nut that has to go on
Fit it to the nut that has to go on
Cut to the calculated depth, then take the last few thousandths by trying the actual mating nut, cleaning the thread and easing the fit until it runs on freely without slop.
Thread fit is decided by the PITCH diameter, not the outside diameter, and the pitch diameter is what the calculated depth is really setting. Measuring it properly needs thread wires or a thread micrometer; in a workshop without either, the mating part is the gauge — which is exactly the go/no-go logic applied to a thread.
Take a spring pass or two at the final setting before you judge it. The tool deflects under load, so the thread is shallower than the dial says until a pass that removes almost nothing catches up with it.
مواد مورد نیاز این مرحله:
میلهٔ گرد فولاد نرم1 قطعهابزارهای مورد نیاز:
تراش فلزشابلون رزوه روغن برش
نقشههای مرتبط
این نقشهها دانش مشترکی دارند — تکنیکها، مواد یا اصول




CC0 مالکیت عمومی
این نقشه تحت مجوز CC0 منتشر شده است. شما آزاد هستید آن را کپی، ویرایش، توزیع و برای هر هدفی بدون نیاز به اجازه استفاده کنید.
با خرید محصولات از طریق نقشه از سازنده حمایت کنید و او کمیسیون سازنده تعیین شده توسط فروشندگان، دریافت میکند یا یک نسخه جدید از این نقشه ایجاد کنید و آن را به عنوان اتصال در نقشه خود قرار دهید تا درآمد به اشتراک گذاشته شود.