LIST
FEGURÐ OG VELLÍÐAN
HANDVERK
MENNING OG SAGA
SKEMMTUN
UMHVERFI
MATUR OG DRYKKUR
ÖFUGVERKFRÆÐI
VÍSINDI
ÍÞRÓTTIR
TÆKNI
KLÆÐANLEG TÆKNI
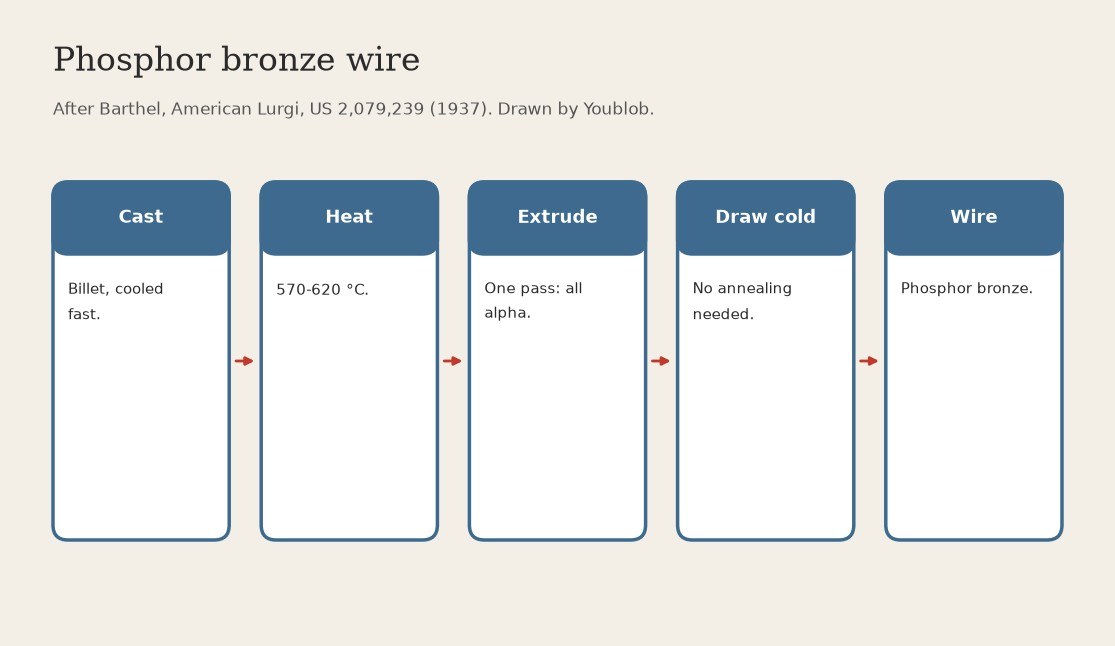

Phosphor Bronze Wire: Cast Billet Extruded at 570-620 °C, then Cold Drawn without Annealing (Barthel, Lurgi, US 2,079,239)
Cast phosphor bronze holds a brittle tin-rich phase that made wire drawing a long round of drawing and annealing. Barthel found that extruding the casting at 570-620 °C kneads it into one soft, even phase, after which it draws straight down to wire.
Result: phosphor bronze wire, drawn without intermediate annealing.
Source: Barthel, US 2,079,239 (American Lurgi, 1937). His temperature is for about 8 % tin; our ingot has about 9 %, so the same range is ours. Not given: extrusion ratio, die sizes. Picture drawn by Youblob.
Lengra kominn
2 days
Leiðbeiningar
1
1
Cast a billet and cool it fast
Cast a billet and cool it fast
Melt the phosphor bronze and cast it into a billet, cooling it rapidly. Ours: cast in an ingot mould and quench.
Efni fyrir þetta skref:
 Fosfórbronsstöng1 as required
Nauðsynleg verkfæri:
 Deigla úr grafíti og leir
 Deigluofn
 Stangamót
 Herslufata
2
2
Heat the billet to 570-620 °C
Heat the billet to 570-620 °C
Heat the billet to between about 570 and 620 °C (Barthel's range for about 8 % tin and 0.3 % phosphorus). Temperature: 500-650 °C overall; the less tin, the hotter (about 650 °C for 6 % tin).
Nauðsynleg verkfæri:
 Múffluofn
 Háhitamælir
3
3
Extrude it in one pass
Extrude it in one pass
Extrude the hot billet in an extrusion press. The kneading makes the metal even all through, practically all alpha. For thick products with little reduction, cold-press the billet 10-20 % first.
Nauðsynleg verkfæri:
 Vökvaþrýstipressa til þrýstimótunar
4
4
Cold draw to wire without annealing
Cold draw to wire without annealing
Draw the extruded rod cold through dies down to wire; Barthel's metal needs no annealing between draws. Ours: a steel drawplate with drawing lubricant, one hole smaller each pass.
Nauðsynleg verkfæri:
 Dráttarplata úr stáli
 Vírdráttarsmurefni
Efni
1- 1 as requiredStaðgengill
Nauðsynleg verkfæri
9- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
Þessi teikning býr til
Tengd Blueprint
Þessi blueprint deila þekkingu — tækni, efni eða meginreglur
CC0 opinbert ríki
Þessi teikning er gefin út undir CC0. Þér er frjálst að afrita, breyta, dreifa og nota þetta verk í hvaða tilgangi sem er, án þess að biðja um leyfi.
Studdu smiðinn með því að kaupa vörur í gegnum teikningu hans þar sem hann fær þóknun smiða sem seljendur ákvarða, eða búðu til nýja endurskoðun á þessari teikningu og tengdu hana sem tengingu í þinni eigin teikningu til að deila tekjum.