LIST
FEGURÐ OG VELLÍÐAN
HANDVERK
MENNING OG SAGA
SKEMMTUN
UMHVERFI
MATUR OG DRYKKUR
ÖFUGVERKFRÆÐI
VÍSINDI
ÍÞRÓTTIR
TÆKNI
KLÆÐANLEG TÆKNI
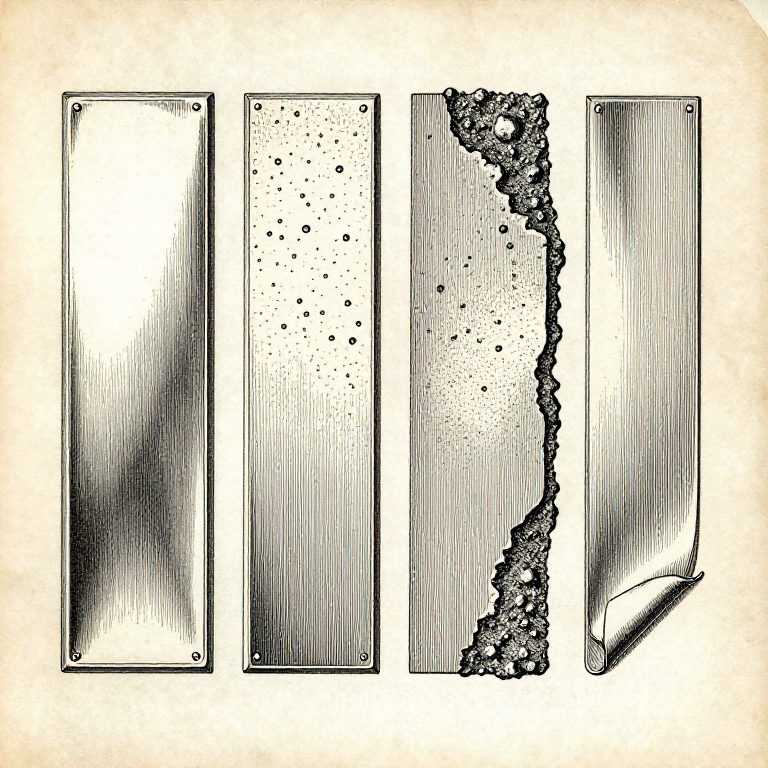

Reading a Plating Fault: Burnt, Pitted, Dull, Peeling
Plating faults have distinct appearances, and each one points at a short list of causes. The diagnosis is quicker than the repair, and it is what stops the same batch being ruined twice.
The first question is always **where** the fault is. A fault at the edges is a current density problem. A fault in a recess is a throwing power problem. A fault in a patch with a defined shape is contamination — and the shape usually says what it was.
A fault over the whole part is the bath.
Miðlungs
2 hours
Leiðbeiningar
1
1
Burning, and roughness
Burning, and roughness
**Burning** is a dark grey, rough, powdery deposit with poor adhesion, always worst at edges, corners and points. It is a dendritic growth: the deposit has grown faster than ions can arrive, so it has branched out into the solution rather than filling in.
*Causes, in order:* current density too high — either the current was set too high or the area was underestimated; too little agitation; the bath too cold; the metal concentration too low.
*The fix at the edges specifically:* a thief, a shield, or a lower current. The racking rung covers these.
**Roughness** is different — gritty or nodular over the whole surface, with good adhesion. It is particles in the bath being plated over.
*Causes:* particles falling from the anodes, which is why anodes go in bags; precipitated basic salts from a pH that drifted high; dust; filter failure.
*The fix:* filter the bath continuously, bag the anodes, check the pH.
**The two are told apart by adhesion and by location.** Burning is at the extremities and lifts; roughness is everywhere and sticks.
Efni fyrir þetta skref:
 Plata úr mjúku stáli2 stykki
 Nikkelsúlfat sexhýdrat1 stykki
Nauðsynleg verkfæri:
 Stækkunarlúpa
 Stafrænn margmælir — sjálfvirkt svið, raunverulegt RMS
2
2
Pitting, and why hydrogen causes it
Pitting, and why hydrogen causes it
**Pitting** is small round holes or craters in the deposit, often in trails running upwards, and it has one dominant cause: **a hydrogen bubble stuck to the surface**. Where a bubble sits, no metal deposits, and the deposit grows around it into a pit.
The trails happen because the bubble slides upwards as it grows.
*Causes and fixes:*
**Poor wetting** — the commonest. A wetting agent in the bath lowers the surface tension so bubbles release instead of clinging. Its exhaustion is the usual reason a bath starts pitting after months of working.
**Too little agitation** — bubbles are not swept away.
**Organic contamination** — oil in the bath, often from a part that was not properly degreased, stabilises the bubbles. Carbon treatment removes it.
**Low current efficiency** — more hydrogen produced in the first place, which is why chrome pits so readily.
**A horizontal surface facing upwards pits worst**, because bubbles settle on it. Rotating or tilting the work during plating is a genuine fix and costs nothing.
Efni fyrir þetta skref:
Plata úr mjúku stáli2 stykkiNauðsynleg verkfæri:
Stækkunarlúpa Hitaplata með seglhræru
3
3
Dullness, cloudiness and staining
Dullness, cloudiness and staining
**Dullness where brightness was expected.** The brightener is exhausted, the current density is below the bright range, the temperature is wrong, or the substrate was not polished — a bright bath does not make a dull surface bright unless it is a levelling bath, and even then only up to a point.
**Cloudiness or haze**, especially in low current density areas. Usually organic contamination, and carbon treatment is the answer.
**A milky or smutty grey film** that wipes off. Often a metallic contaminant co-depositing — zinc in a nickel bath, for instance. Dummy plating at low current density for several hours removes it onto a scrap cathode.
**Staining after drying.** Solution not rinsed out, or a hole that weeped after the part was dry, or tap water in the last rinse.
**A rainbow or iridescent sheen on zinc** is the passivation film and is normal — that one is a feature.
**Brown or black streaks running down from a hole** are trapped solution finding its way out after plating. Blow the holes out before drying.
Efni fyrir þetta skref:
Nikkelsúlfat sexhýdrat1 stykki Eimað vatn1 stykki
Nauðsynleg verkfæri:
Stækkunarlúpa Bikarglas úr bórsílíkati
4
4
The diagnostic sequence, and the log
The diagnostic sequence, and the log
**Start with where.** Edges and points say current density. Recesses and blind areas say throwing power. A patch with a shape — a thumb print, a run mark, a line where the solution level sat — says contamination or handling. Everywhere at once says the bath.
**Then ask when it started.** A fault that appeared suddenly between two otherwise identical runs points at a single change: a new bottle of something, a topped-up bath, a different part, a colder day. A fault that has crept in over weeks points at consumption — brightener, wetting agent, anode area.
**Then run a Hull cell.** One small panel shows the whole current density range at once: where it burns, where it goes dull, where it is bright. It is the single most informative half hour available, and it uses a few hundred millilitres.
**Then treat in the standard order:** filter, carbon treat for organics, dummy plate for metallics, correct the pH, correct the temperature, and only then add brightener. Adding brightener first is the usual instinct and it usually makes things worse, because the additive is rarely the cause.
**Keep the log.** Date, part, area, current, time, temperature, pH, weight gain, and what the deposit looked like. Every diagnosis above is a comparison against a previous run, and without the log there is nothing to compare with.
Nauðsynleg verkfæri:
 Stillanlegur aflgjafi fyrir vinnubekkStafrænn margmælir — sjálfvirkt svið, raunverulegt RMS
 Rannsóknastofuhitamælir
 Rafhúðunarsett
Efni
3- 2 stykkiStaðgengill
- 1 stykkiStaðgengill
- 1 stykkiStaðgengill
Nauðsynleg verkfæri
7- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
Tengd Blueprint
Þessi blueprint deila þekkingu — tækni, efni eða meginreglur

CC0 opinbert ríki
Þessi teikning er gefin út undir CC0. Þér er frjálst að afrita, breyta, dreifa og nota þetta verk í hvaða tilgangi sem er, án þess að biðja um leyfi.
Studdu smiðinn með því að kaupa vörur í gegnum teikningu hans þar sem hann fær þóknun smiða sem seljendur ákvarða, eða búðu til nýja endurskoðun á þessari teikningu og tengdu hana sem tengingu í þinni eigin teikningu til að deila tekjum.