Collaborazione
ARTE
BELLEZZA E BENESSERE
MESTIERE
CULTURA E STORIA
DIVERTIMENTO
AMBIENTE
CIBO E BEVANDE
INGEGNERIA INVERSA
SCIENZE
SPORT
TECNOLOGIA
INDOSSABILI
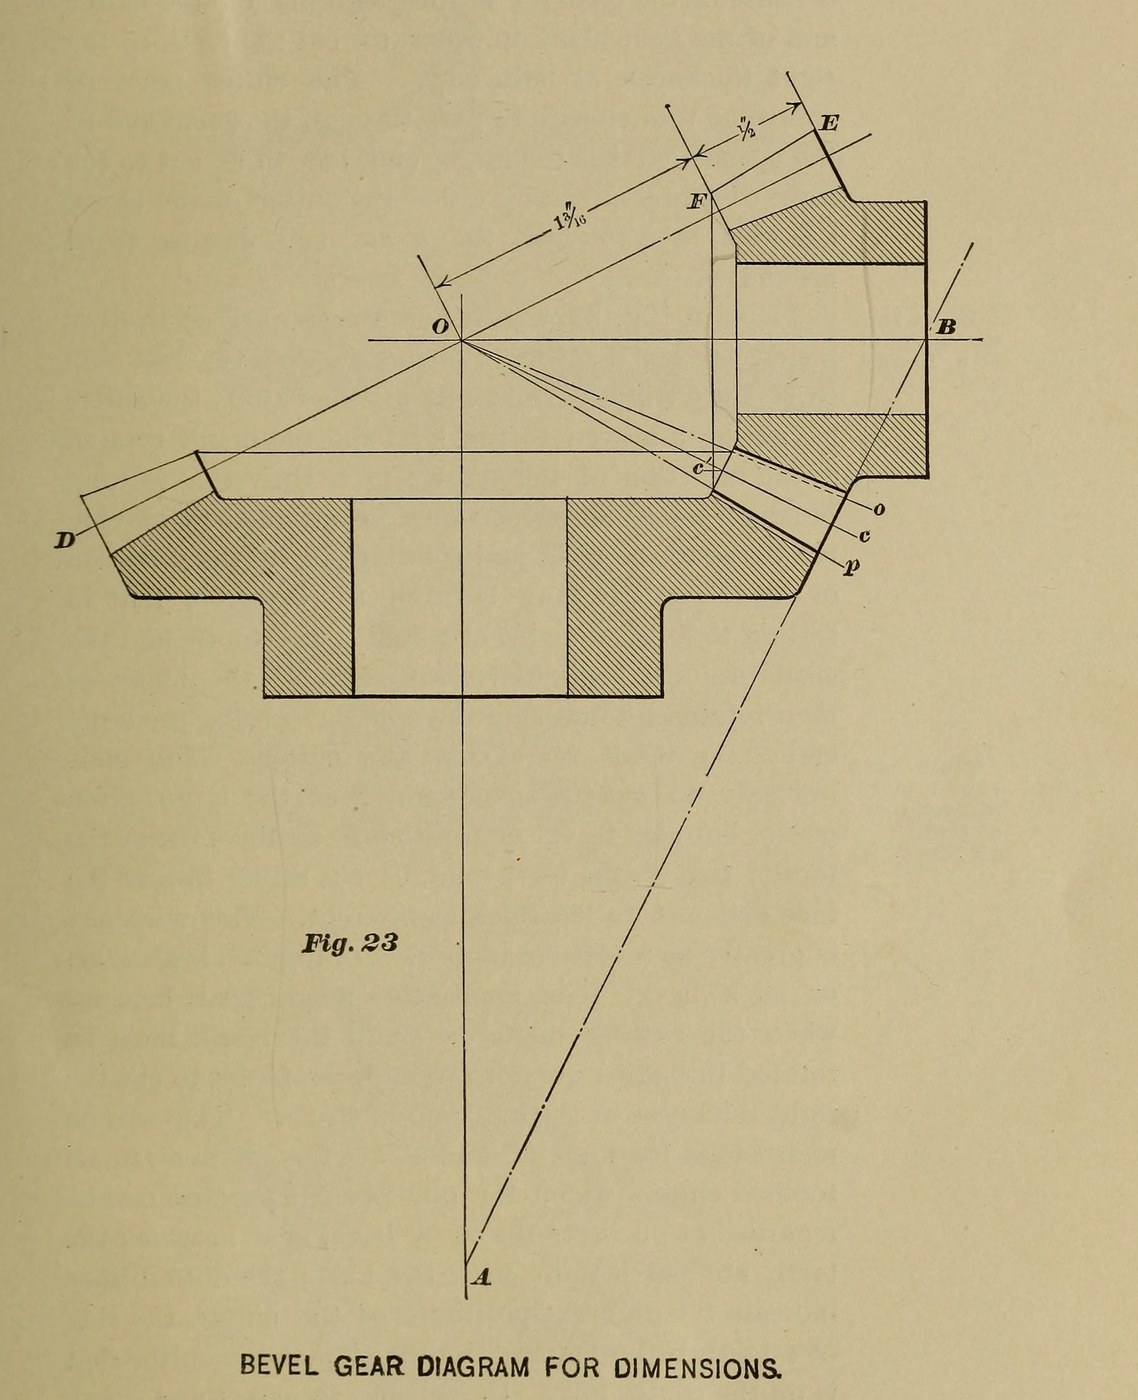


Bevel Pinion: 12 Teeth, 8 Pitch, for a 24-Tooth Gear (Brown & Sharpe 1911)
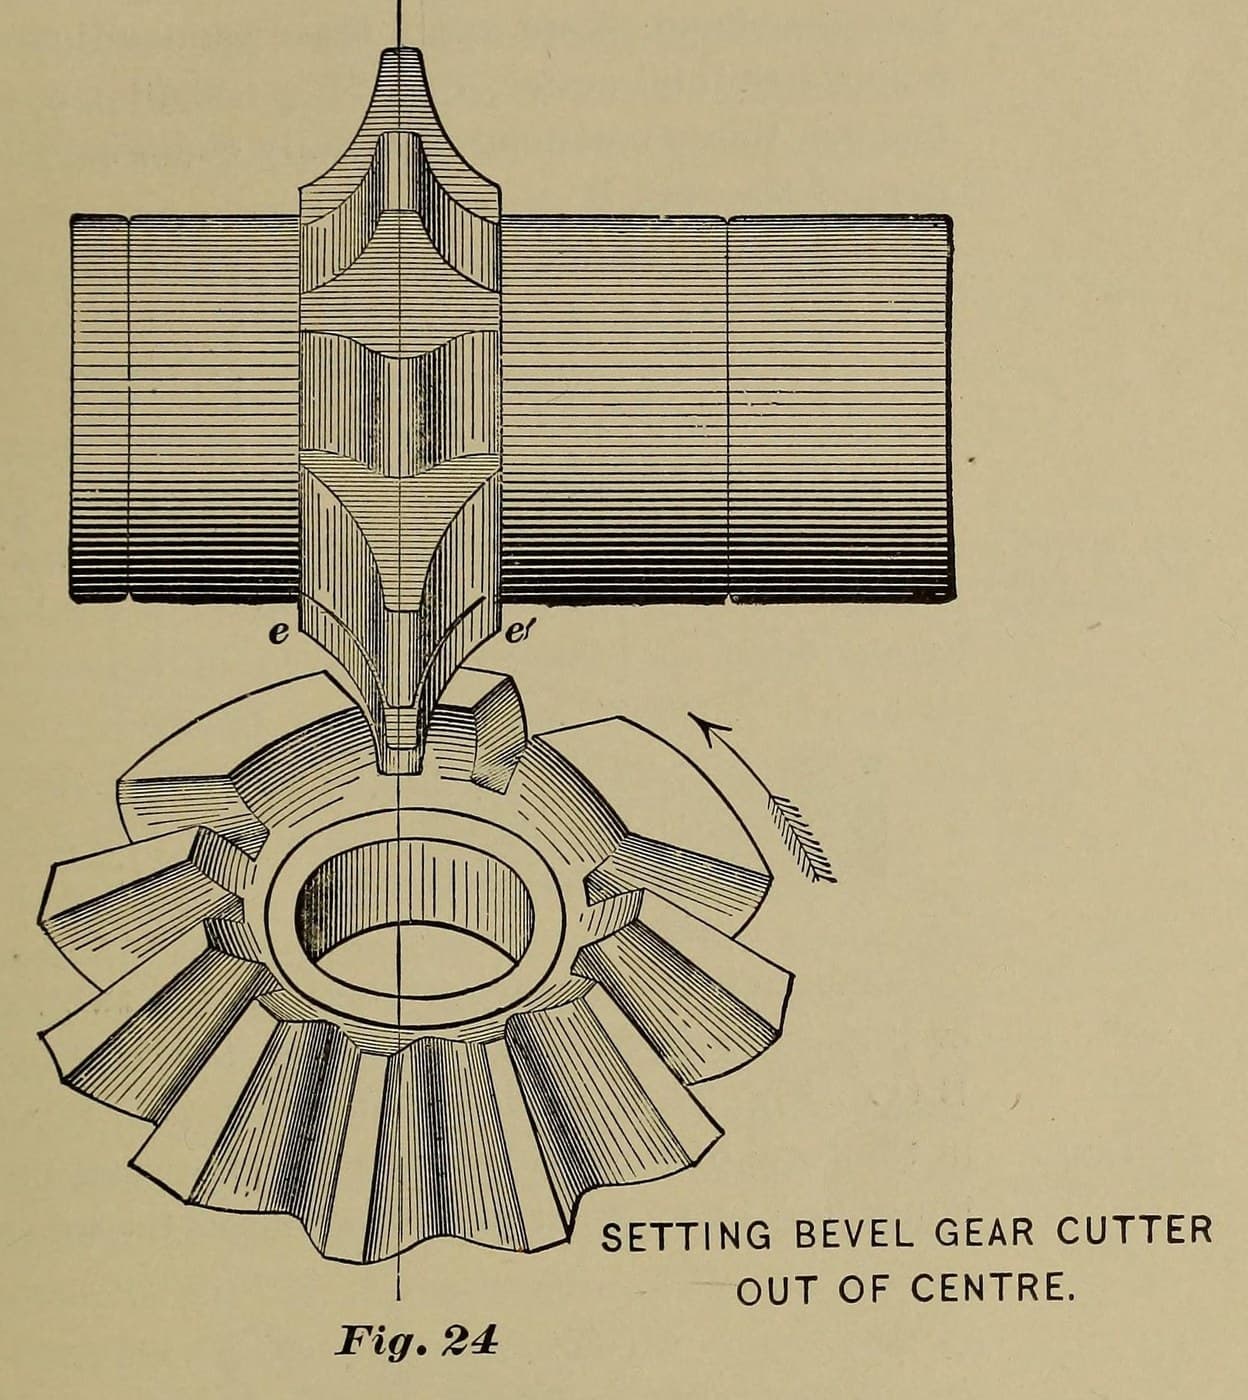
Brown & Sharpe's own worked example: the small gear of a 12 and 24 tooth bevel pair, 8 pitch, shafts at right angles, cut with the No. 8 cutter they send to anyone who orders one for this pinion. The method is the same as for mitre gears: set off centre, cut each side, file the small ends.
Source: Brown & Sharpe, Practical Treatise on Gearing (1911), Fig. 23 example, Part I ch. IX–X, Part II ch. III and the set-over table p. 58. The blank sizes are our arithmetic with their rules; the steel and bore are ours. Picture: their Fig. 23.
Avanzato
1 day
Istruzioni
1
1
Work out and turn the blank
Work out and turn the blank
Pitch diameter 12 ÷ 8 = 1.500 in. Angle of edge 26° 34′ and angle of face 59° 11′ (Brown & Sharpe's figures for every 12 and 24 tooth pair). Diameter increment = cos 26° 34′ × 0.250 = 0.224 in, so turn the steel blank to 1.72 in outside diameter. Face ½ in long. Try both angles with a protractor against the end of the hub.
Materiali per questo passaggio:
 Barra di acciaio dolce1 length for one blank
Strumenti necessari:
 Tornio per metalli
 Utensile da taglio per tornio
 Goniometro
 Micrometro
2
2
Choose the cutter
Choose the cutter
Twice the back cone radius × 8 comes to about 13, so a No. 8, 8-pitch bevel gear cutter. Measure its thickness Tc at the pitch line, 0.145 in from its tip.
Strumenti necessari:
 Fresa per ingranaggi conici
 Calibro a nonio per denti di ingranaggio
3
3
Set the head at 22° 18′
Set the head at 22° 18′
Apex distance = sec 26° 34′ × 1.5 = 1.677 in. Angle increment: tan = sin 26° 34′ ÷ 6, giving 4° 16′. Set the dividing head to the cutting angle 26° 34′ − 4° 16′ = 22° 18′ and index 12 spaces. Depth at the large end 0.270 in.
Strumenti necessari:
 Fresatrice
 Testa a dividereFresa per ingranaggi conici
4
4
Set over and cut one side
Set over and cut one side
Apex distance ÷ face = 3.35; we take the nearest column, 3¼, where a No. 8 cutter has the factor .286. Set-over = Tc ÷ 2 − .286 ÷ 8 = Tc ÷ 2 − 0.036 in. Set off centre by that amount, take up backlash, and cut round all 12 spaces.
Strumenti necessari:
FresatriceTesta a dividereFresa per ingranaggi conici5
5
Set over the other way and trim
Set over the other way and trim
Set over the same amount the other side, line the cutter up with the space at the small end, take a trial cut, and rotate toward the cutter until the tooth is 0.196 in thick at the large end and 0.138 in at the small end. Check with the gear tooth vernier, then cut round.
Strumenti necessari:
FresatriceTesta a dividereFresa per ingranaggi coniciCalibro a nonio per denti di ingranaggio6
6
File the small ends
File the small ends
File the teeth rounder at the small ends, where the cutter could not, without filing them thinner at the pitch line. The cutting angle is under 30°, so the spaces may come out narrower at the face than the cutter suggests; Brown & Sharpe's own shop used a No. 6 cutter here instead.
Strumenti necessari:
 Lima fine
Materiali
1- 1 length for one blankSegnaposto
Strumenti richiesti
9- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
Questo progetto realizza
Blueprint correlati
Questi blueprint condividono conoscenze — tecniche, materiali o principi
CC0 Pubblico dominio
Questo progetto è rilasciato sotto CC0. Sei libero di copiare, modificare, distribuire e utilizzare quest'opera per qualsiasi scopo, senza chiedere permesso.
Supporta il Maker acquistando prodotti tramite il suo progetto dove guadagna una Commissione Maker stabilita dai venditori, oppure crea una nuova iterazione di questo progetto e includilo come collegamento nel tuo progetto per condividere i ricavi.