コラボレーション
アート
美容とウェルネス
工芸
文化と歴史
エンターテインメント
環境
食品と飲料
リバースエンジニアリング
科学
スポーツ
テクノロジー
ウェアラブル
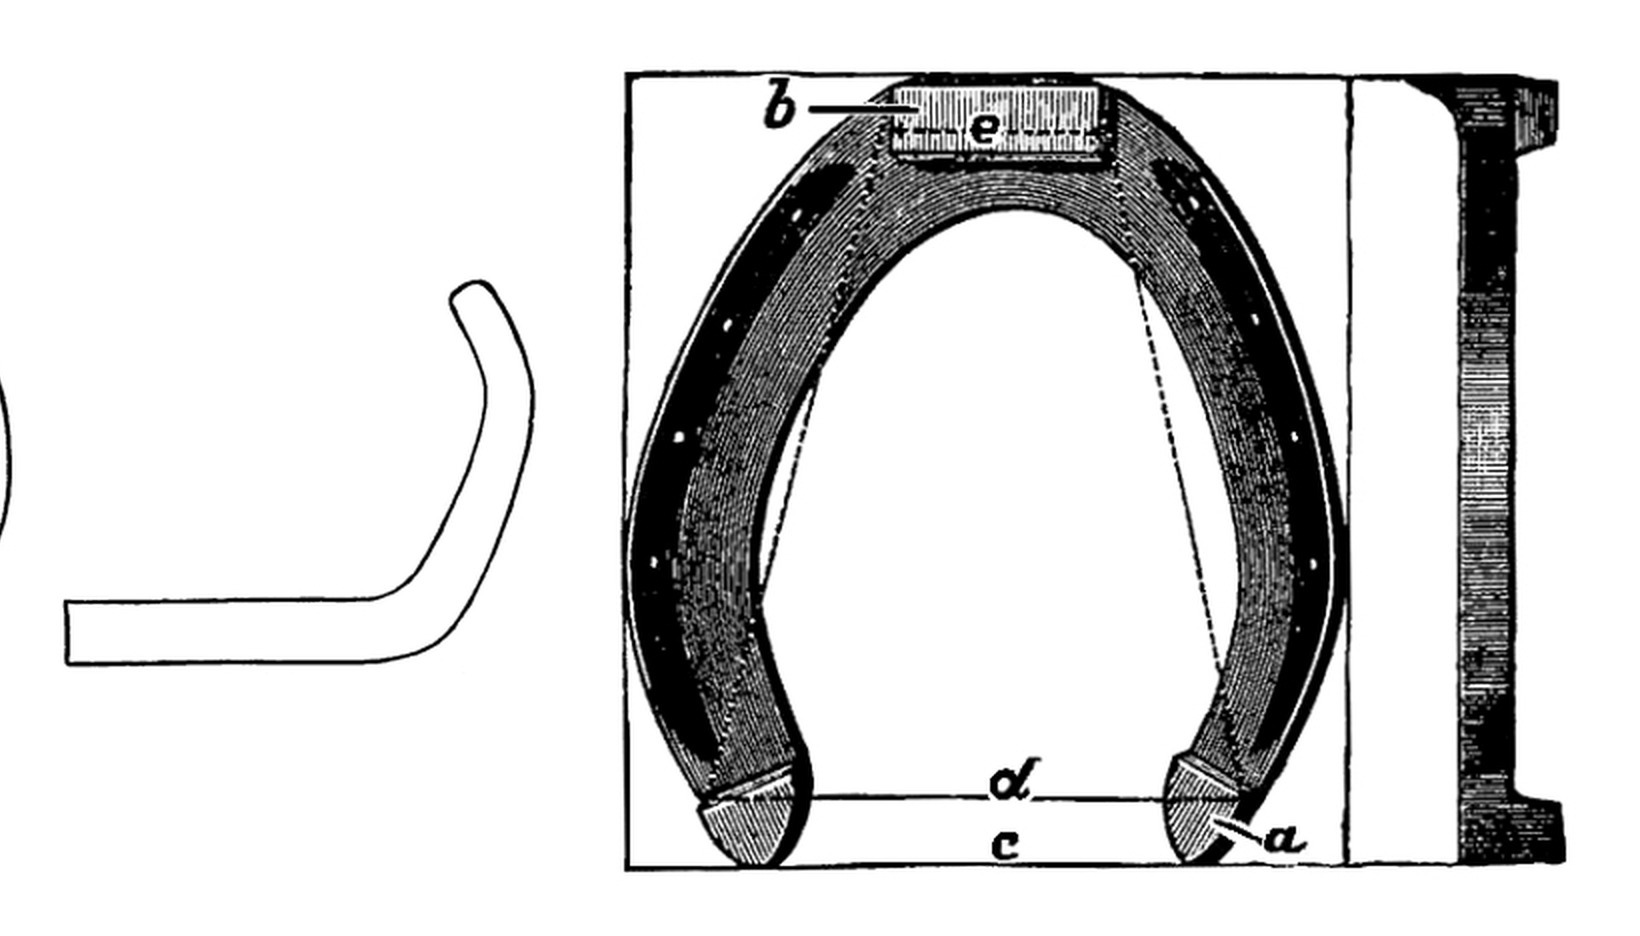


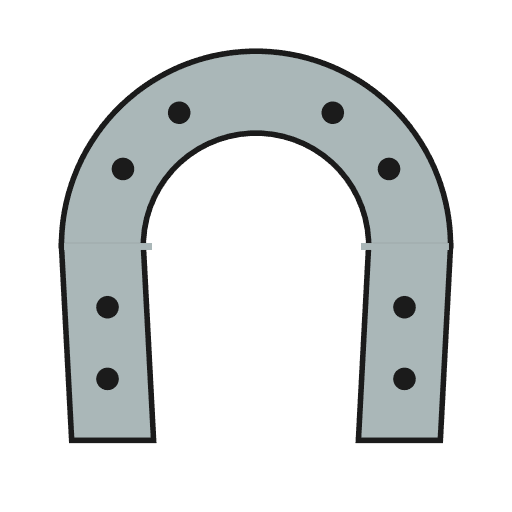
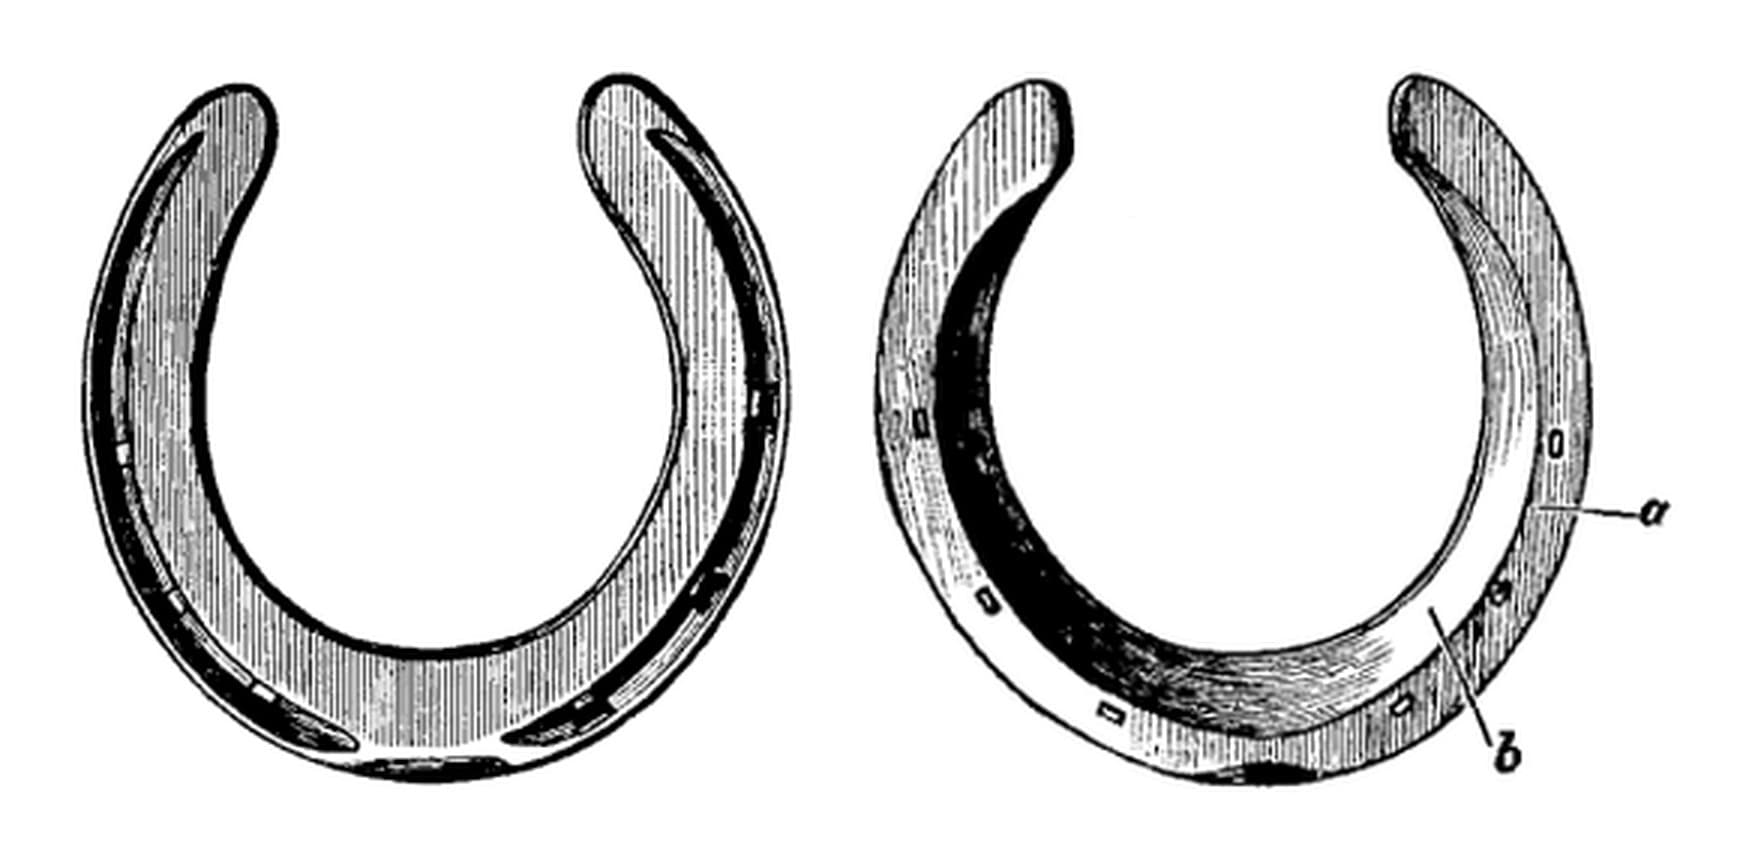
Hind Horseshoe: Round-Pointed Toe, No Seating, Nail Holes in the Front Two-Thirds (Lungwitz and Adams, Text-Book of Horseshoeing, 1913)
A flat hind horseshoe from Lungwitz and Adams, A Text-Book of Horseshoeing (1913). It is made "in like manner" as the front shoe, but the branches are bent to a different curve, giving a round-pointed toe, the hoof side is not concaved, and the nail holes run further back.
Fitting and nailing the shoe to the horse, calks and clips are not covered here.
中級者
8-15 minutes a pair, once practised
手順
1
1
Bar length and sizes
Bar length and sizes
Jupyter ノートブックを読み込み中…
2
2
Read Lungwitz and Adams
Read Lungwitz and Adams
"The hind shoe is made in like manner, but the branches are not bent in a circle but given that form shown in Fig. 106."
3
3
Measure and cut the bar
Measure and cut the bar
Measure the hoof from the point of the toe to the buttress and its greatest width; add them for the bar length. Trace the outline on stiff paper if you want to keep it. Cut the bar.
このステップの材料:
 錬鉄の棒1 個
必要な工具:
 メジャー(巻尺)
 鉛筆
 厚紙のシート
 鍛冶炉
 金床用たがね
 鍛冶ばさみ(やっとこ)
4
4
Bend the outer branch to the hind curve
Bend the outer branch to the hind curve
Heat the bar white-hot just beyond its middle and bend it over the sledge head on the anvil face with the turning hammer, as for the front shoe, but bend the branch to the flatter, angled curve of his Fig. 106, not to a circle. The outer branch is made first, the right shoe first in a pair. Draw out the end with the sledge.
必要な工具:
鍛冶炉 嘴付き小金床
 そり
 丸め鎚鍛冶ばさみ(やっとこ)
5
5
Bevel, flatten and shape
Bevel, flatten and shape
Bevel the branch on the horn, then flatten it. Bending the toe of a hind shoe backs up the inner edge and thins the outer, so hammer the shoe smooth and even. Shape it so the toe is round-pointed, "yet not too much so", as in his Fig. 116.
必要な工具:
嘴付き小金床丸め鎚鍛冶ばさみ(やっとこ)6
6
Round the inner edge and fuller
Round the inner edge and fuller
Concaving is not necessary: just round the inner edge of the web. Fuller the ground side as for the front shoe, to about two-thirds of the thickness.
必要な工具:
嘴付き小金床 フラー(溝切り鉄)そり丸め鎚鍛冶ばさみ(やっとこ)
7
7
Stamp the nail holes
Stamp the nail holes
Stamp and pritchel the nail holes in the front two-thirds of the shoe, none at the toe: usually one more than a front shoe, seldom more than eight. Set each as far from the outer edge as the wall is thick; on a hind hoof the wall is nearly as thick at the quarters as at the toe.
必要な工具:
嘴付き小金床 熱間ポンチ
 釘穴用のたがね丸め鎚鍛冶ばさみ(やっとこ)
8
8
Make the second branch and finish
Make the second branch and finish
Make the inner branch the same way, turned to the left. Go over the outer edge on the horn and hammer the bearing surface smooth and level. Rough it out in two heats if you can.
必要な工具:
鍛冶炉嘴付き小金床丸め鎚フラー(溝切り鉄)熱間ポンチ釘穴用のたがね鍛冶ばさみ(やっとこ)9
9
Troubleshooting
Troubleshooting
Hind shoe troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
From **A Text-Book of Horseshoeing**, by A. Lungwitz and John W. Adams, 11th edition, J. B. Lippincott, 1913 (Project Gutenberg 66786), chapter III F. His Fig. 116 shows a hind shoe with toe- and heel-calks; the calks and the toe-clip are not made here, as this chapter gives no method for forging heel-calks or drawing clips. Fitting and nailing are not covered. The metric figures are ours.
必要な工具
12- 1 vendor sell this, none ship to you yetプレースホルダー
- 1 vendor sell this, none ship to you yetプレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
この設計図で作るもの
関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理
CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。