コラボレーション
アート
美容とウェルネス
工芸
文化と歴史
エンターテインメント
環境
食品と飲料
リバースエンジニアリング
科学
スポーツ
テクノロジー
ウェアラブル
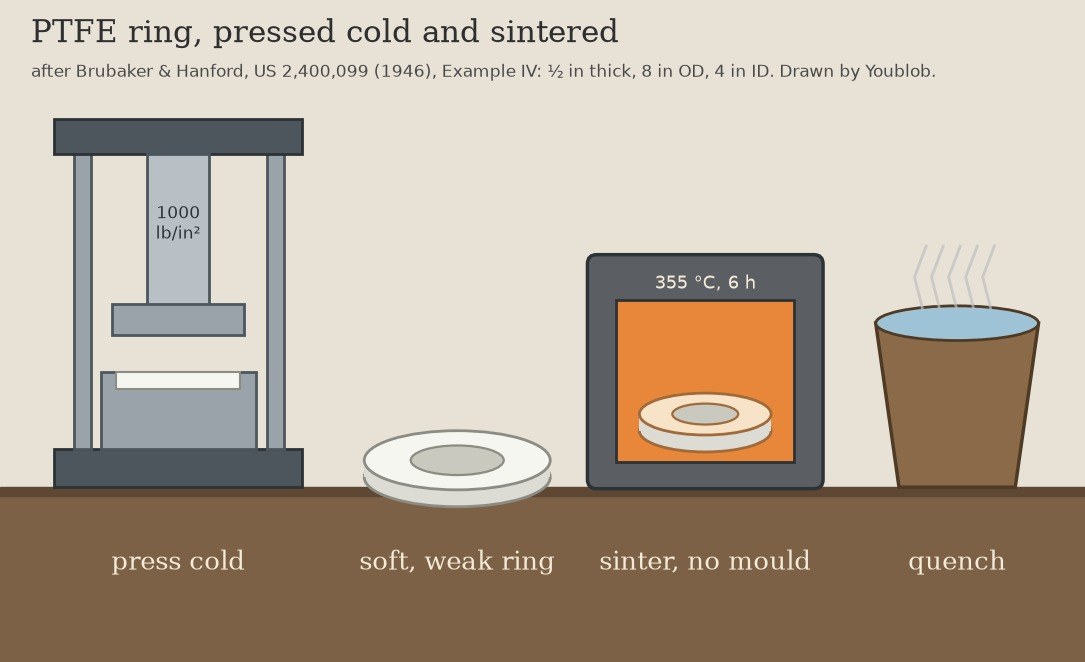


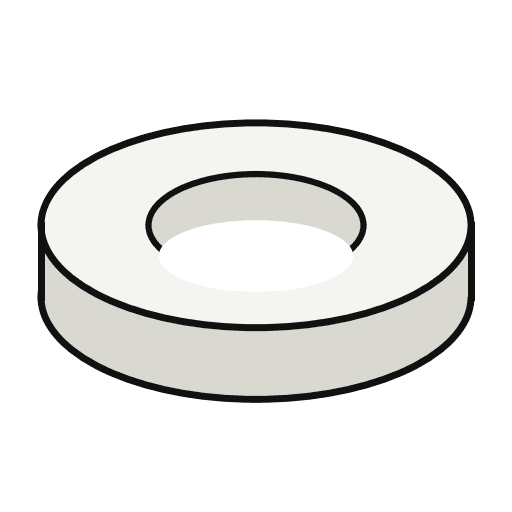
PTFE Ring: Pressed Cold, Sintered Out of the Mould (Brubaker & Hanford 1946)
PTFE will not flow like other plastics, so it cannot be injection moulded. Du Pont's answer was to press the powder cold into shape, take it out of the mould, and only then heat it above 327 °C. The soft, weak pressing keeps its shape in the furnace and comes out tough. This is their Example IV: a ring 8 in across.
Source: M. M. Brubaker and W. E. Hanford (du Pont), US 2,400,099 (1946), Example IV. The press, die and furnace are ours. Picture drawn by Youblob.
中級者
1 day
手順
1
1
Fill the ring mould with powder
Fill the ring mould with powder
At room temperature, fill a ring mould with powdered PTFE. The finer the powder, the better the result (the patent).
このステップの材料:
 PTFE 樹脂粉末1 as required to fill the mould
必要な工具:
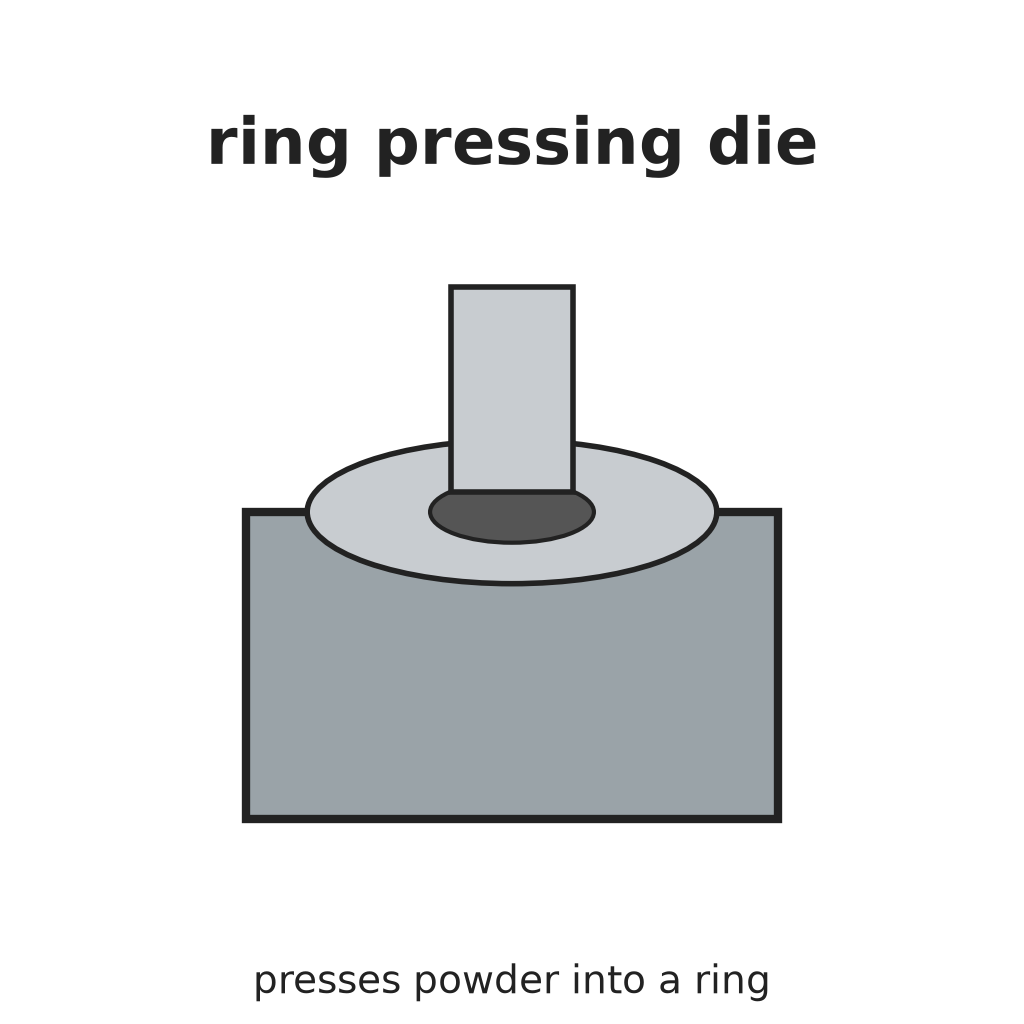 リング成形ダイス
2
2
Press at 1000 psi
Press at 1000 psi
Press it at 1000 lb/sq in into a ring ½ in thick, 8 in outside and 4 in inside diameter. The pressed ring is soft and weak: handle it gently.
必要な工具:
 油圧プレスリング成形ダイス
 定規
3
3
Sinter at 355 °C for 6 hours
Sinter at 355 °C for 6 hours
Take the ring out of the mould and heat it, free-standing, in a furnace at 355 °C for 6 hours. Air is fine; no mould is needed to hold its shape.
必要な工具:
 マッフル炉
 表示器付き熱電対
4
4
Quench in cold water
Quench in cold water
Lift the hot ring out and quench it in cold water. It comes out hard and tough. It shrinks a little but stays symmetrical.
必要な工具:
 火ばさみ
 焼き入れ桶
この設計図で作るもの
関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理

CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。