アート
美容とウェルネス
工芸
文化と歴史
エンターテインメント
環境
食品と飲料
リバースエンジニアリング
科学
スポーツ
テクノロジー
ウェアラブル
The Bin That Stops Flowing: Arching, Ratholing, and the Gate That Causes It
Every machine in this batch needs to be fed steadily. The jaw and the cone want to be choke fed; the hammer mill tells you audibly when it is starved; the screen's efficiency collapses if the bed depth wanders. So the last rung is the one that decides whether any of them work: getting material out of a bin at a rate you chose.
A bin that has stopped looks the same whatever the cause, and there are two causes with nothing in common. Coarse lumps can jam mechanically across a small opening. Fine or damp material can develop real strength and stand up as an arch — and that strength grows while the bin sits full, which is why the bin that ran all week blocks on Monday morning.
There is also a third cause, and it is the commonest of all: somebody fitted a gate and used it to control the rate. Throttling a gate makes the outlet smaller, and a smaller outlet is exactly what arching needs.
中級者
About 3 hours
手順
1
1
Make an arch on the bench, twice
Make an arch on the bench, twice
Cut a cone from sheet — or use a large funnel, or a bucket with a hole in it — and stand it over a tray.
**Mechanical interlocking first.** Fill it with coarse aggregate whose largest pieces are about a third the size of the outlet. It will jam, and if you look up into the outlet you will see three or four stones wedged against each other in a ring. Enlarge the outlet in stages and find the size at which it stops jamming. Compare with the six-to-eight-times rule in step 4.
**Cohesive arching second.** Empty it and fill it with crusher fines or damp sand. Poke a hole through and let it drain. Now watch what is left: a vertical pipe through the middle with the material standing untouched against the walls. That is a **rathole**, and the bin is still nominally half full.
Do the second test again after leaving the material sitting for a day. It will be noticeably harder to start, and the arch it forms will span further. That is the time-consolidation in step 4, and it is the whole reason bins are emptied at the end of a shift rather than left standing.
Never clear a blocked bin from underneath, and never reach into an outlet. A bulk solid that lets go does so all at once, and it does not have to be a large bin to kill someone.
このステップの材料:
 骨材の石1 bucket
 粗砂(建築・陶芸用)1 bucket
 軟鋼板1 個
必要な工具:
 左官ごて
 スコップ
 メジャー(巻尺)
 定規
 バケツ
 革の作業用手袋
 透明保護メガネ
 防じんマスク
2
2
Measure the wall friction, because everything depends on it
Measure the wall friction, because everything depends on it
Whether a hopper flows at the wall is decided by one number and the number is easy to get.
Take a flat plate of the material the hopper is actually made of — not 'steel', but the steel it is made of, in the condition it is in: rusty, painted, lined, polished. Put a shallow open-bottomed ring of your bulk solid on it. Tilt the plate slowly until the material slides.
The tangent of that angle is the wall friction coefficient. Write down the angle, the material, the surface and the moisture — all four, because changing any one of them changes the answer.
Now do it again with a different surface. A sheet of polished stainless or a scrap of UHMW polyethylene beside a piece of rusty mild steel is an education: the same material that will not move on one will run off the other. Lining a hopper is not a coating job, it is a change to the mechanics.
And do it again after the sample has been standing wetted overnight. Wall friction is the least constant 'constant' in the rung.
このステップの材料:
 軟鋼板1 個
 アルミ板1 個粗砂(建築・陶芸用)1 つかみ
必要な工具:
 分度器
 水準器定規
 デジタルスケール革の作業用手袋
3
3
Fit a feeder, not a gate
Fit a feeder, not a gate
This is the sentence that matters most in the rung: **a gate turns flow on and off; a feeder controls the rate.** They are not interchangeable and using one for the other is what blocks most bins.
The reason is in step 5's arithmetic. A part-closed slide gate is a small outlet, and a small outlet arches. The operator throttles it because the flow is too fast, the bin blocks, somebody hits it with a hammer, and the conclusion drawn is that the material is difficult.
A feeder sits under the **full** outlet and withdraws material across all of it. A belt feeder, a screw with a tapered flight or a variable pitch, a vibrating tray — each meters what leaves while the whole opening stays open.
The detail that is easy to get wrong: a feeder must draw from the whole outlet, not just from one end of it. A plain constant-pitch screw under a long slot fills up at the back end and then conveys without drawing any more, so the bin empties through a rathole above the first few flights and the rest stands still. Taper the flight, or step the pitch, so the screw's capacity increases along its length.
And build an interlock: the feeder starts before the bin is filled and stops after it, so the bin is never left standing full over a shutdown. That single piece of sequencing prevents more blockages than any vibrator ever fitted.
このステップの材料:
 振動モーター1 個
 産業用ベルトコンベヤー1 個
 軟鋼の山形鋼1 個
 小ねじ8 個
必要な工具:
 ギヤードモーター
 スパナセット
 コードレスドリル
 ドリルビットセット水準器メジャー(巻尺)透明保護メガネ革の作業用手袋
 聴覚保護具
4
4
The minimum outlet, and why it changes over a weekend
The minimum outlet, and why it changes over a weekend
Jupyter ノートブックを読み込み中…
5
5
Mass flow, funnel flow, and what the gate does
Mass flow, funnel flow, and what the gate does
Jupyter ノートブックを読み込み中…
6
6
History and context
History and context
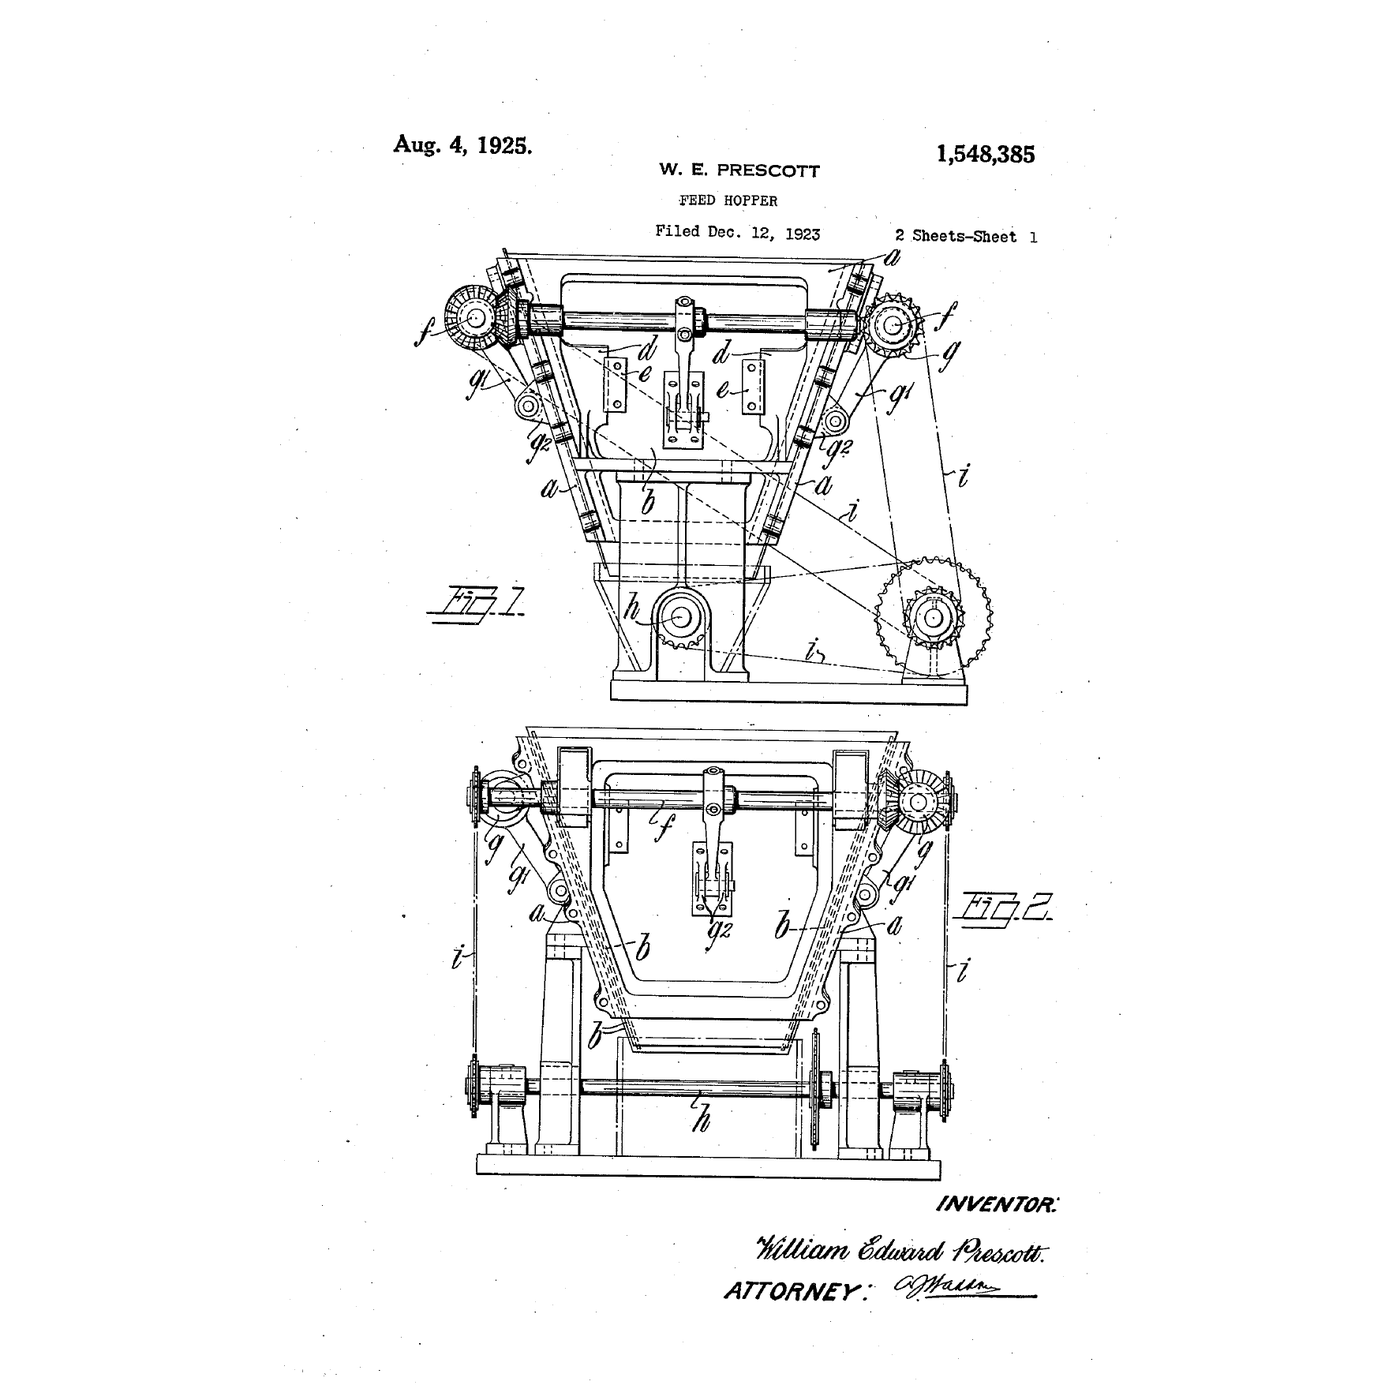
**US 1,548,385, 'Feed Hopper', William Edward Prescott of London, assignor to Baker-Perkins Company Incorporated of New York, application filed 12 December 1923, granted 4 August 1925.** The specification states its own purpose plainly: hoppers for feeding *'semi-liquid, plastic, powdered or granulated substances'* to machines such as mixers, with *'improved means for agitating or keeping in movement the contents in order to facilitate the discharge or feed.'*
The mechanism is worth the visit. Prescott builds the hopper's sides as a skeleton framework and completes the walls with plates that **slide**, reciprocated in sequence by eccentrics on shafts along each side. The wall itself keeps moving, so material at the wall cannot come to rest and an arch has nothing to spring from. It is the mass-flow problem attacked from the other end — instead of making the wall slippery enough for the material to slide on, make the wall slide under the material.
The systematic theory came later. **Andrew Jenike's work at the University of Utah, published in 1961 as Bulletin 108, 'Gravity Flow of Bulk Solids'**, turned hopper design from craft into engineering: the flow-function measurement, the mass-flow and funnel-flow distinction, and the arching calculation in step 4 are all his. No patent number is asserted for that work, because it was published rather than patented.
**Honest limits.** The arching calculation needs the material's unconfined yield strength, and that has to be measured on a shear tester at the consolidation and moisture the bin will actually see — a number taken from a handbook is a guess. Mass flow costs headroom and it costs wall wear, because all the material now slides on the wall instead of on itself. Lined hoppers wear their liners. And no amount of hopper design helps a material that changes: the bin that was designed for dry fines will block on wet ones, and the weather is not a design parameter anyone gets to fix.
材料
9- 1 bucketプレースホルダー
- 1 つかみプレースホルダー
- 1 個プレースホルダー
- 1 個プレースホルダー
- 1 個プレースホルダー
- 1 個プレースホルダー
- 1 個プレースホルダー
- 8 個プレースホルダー
必要な工具
16- プレースホルダー
- プレースホルダー
- 1 vendor sell this, none ship to you yetプレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- プレースホルダー
- 1 vendor sell this, none ship to you yetプレースホルダー
- プレースホルダー
- 聴覚保護具10%コミッションプレースホルダー
関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理

The Troughed Belt: Two Tipped Rollers That Doubled What a Conveyor Carries
Emma 作
力学
9
0
0
0
0
0
Breaking by Impact: The Swing Hammer and the Grate That Sets the Size
Martin 作
金属加工
7
0
0
0
0
0
The Cone Crusher: A Parallel Zone Nothing Gets Past
Martin 作
金属加工
11
0
0
0
0
0

Sorting by Size: Why a Screen Never Makes a Clean Cut
Emma 作
力学
10
0
0
0
0
0
CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。