アート
美容とウェルネス
工芸
文化と歴史
エンターテインメント
環境
食品と飲料
リバースエンジニアリング
科学
スポーツ
テクノロジー
ウェアラブル

Tolerance and Clearance: Printed Holes Come Out Small, Every Time
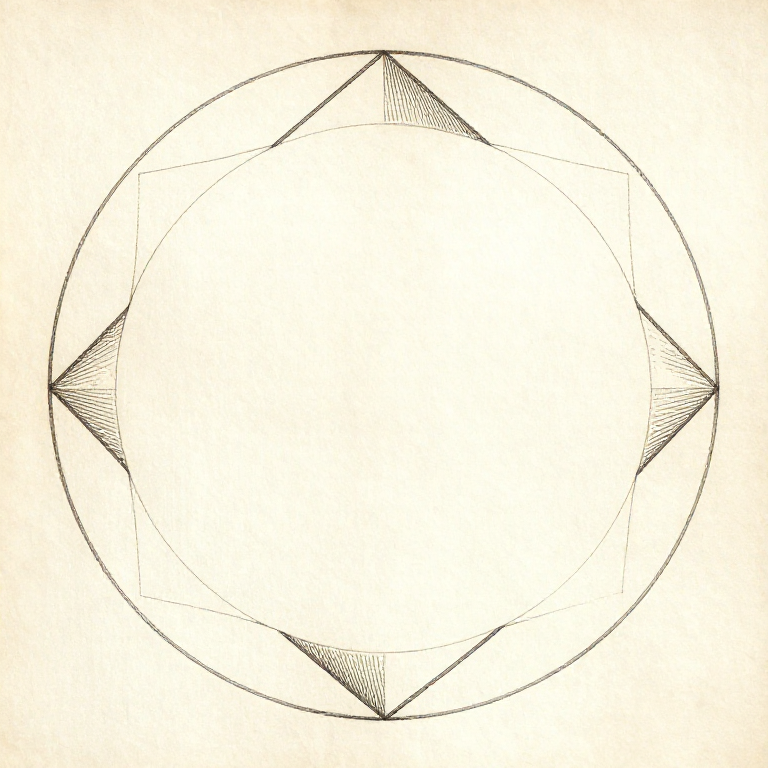
Model a 5 mm hole, print it, and a 5 mm pin will not go in. That is not a fault in the printer: it is what happens when a round hole is approximated by straight line segments laid inside its circumference, and when hot plastic shrinks as it cools.
Both effects run the same way, so printed holes come out SMALL and printed pegs come out LARGE. The error is a few tenths of a millimetre, consistently, in a predictable direction — which makes it correctable rather than annoying.
Which is the whole point: measure your printer's error once, on a test piece, and then design every hole and peg with it already allowed for.
中級者
3 hours
手順
1
1
Why it happens, and which way
Why it happens, and which way
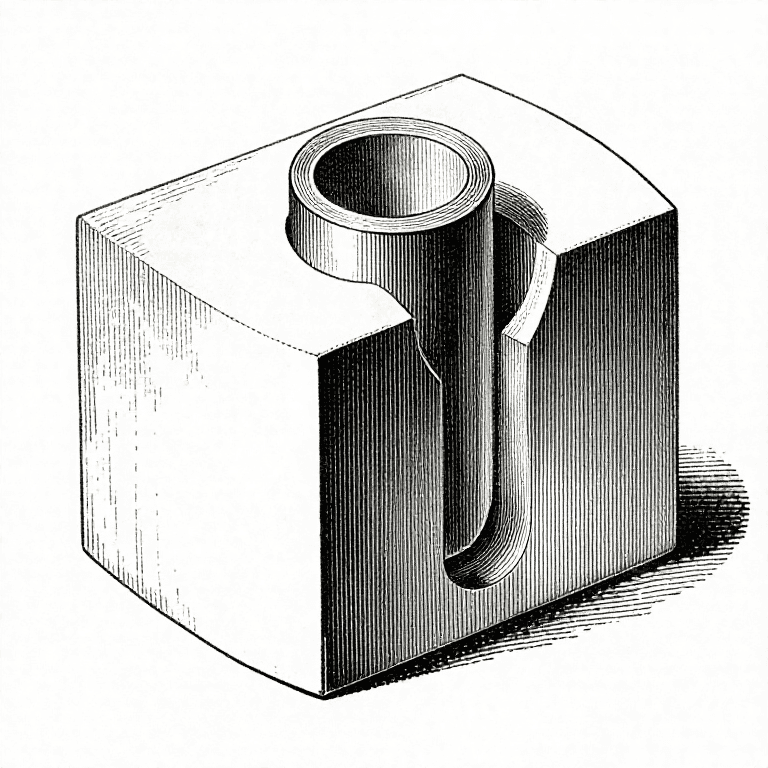
A circular hole is printed as a many-sided polygon whose corners touch the circle, so the flats fall INSIDE it. The smaller the hole, the fewer segments and the worse the effect.
On top of that the nozzle pushes a line of plastic that spreads slightly, and the plastic shrinks as it cools. Both add material where the hole should be and remove it from outside surfaces — so holes shrink and pegs grow.
That means an interference fit and a clearance fit are not symmetrical on a printer, unlike on a lathe. A peg and hole modelled the same size will always be an interference fit, and usually a very tight one.
このステップの材料:
 3D プリント用フィラメント(PLA)1 個
必要な工具:
 デジタルノギス 6インチ
 拡大ルーペ
2
2
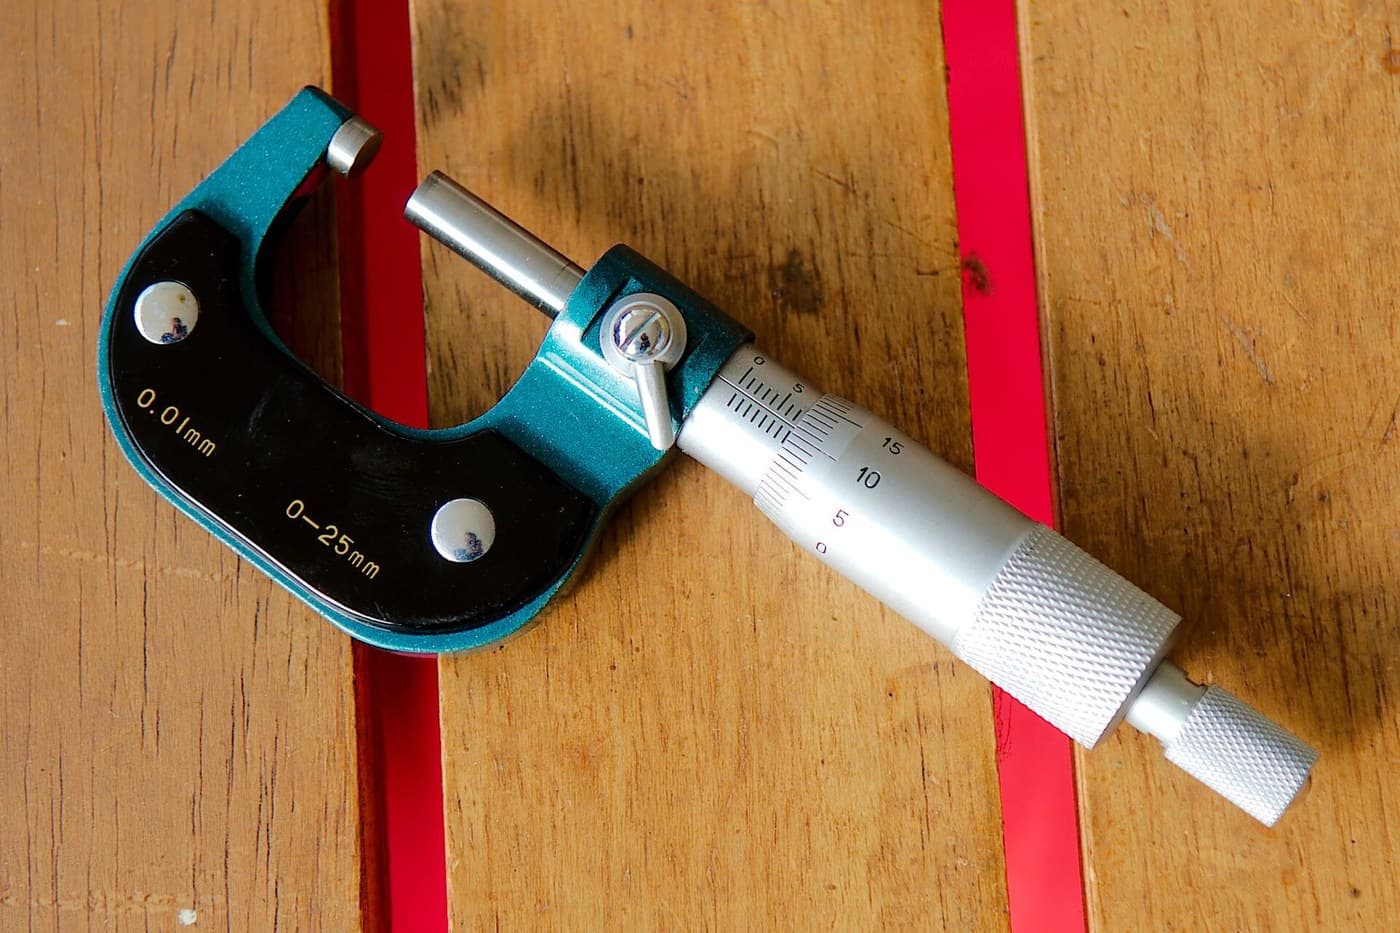
Measure your own printer's offset
Measure your own printer's offset
Jupyter ノートブックを読み込み中…
このステップの材料:
3D プリント用フィラメント(PLA)1 個 ABS フィラメント1 個
必要な工具:
デジタルノギス 6インチ デスクトップパソコン
 FDM 3D プリンター
3
3
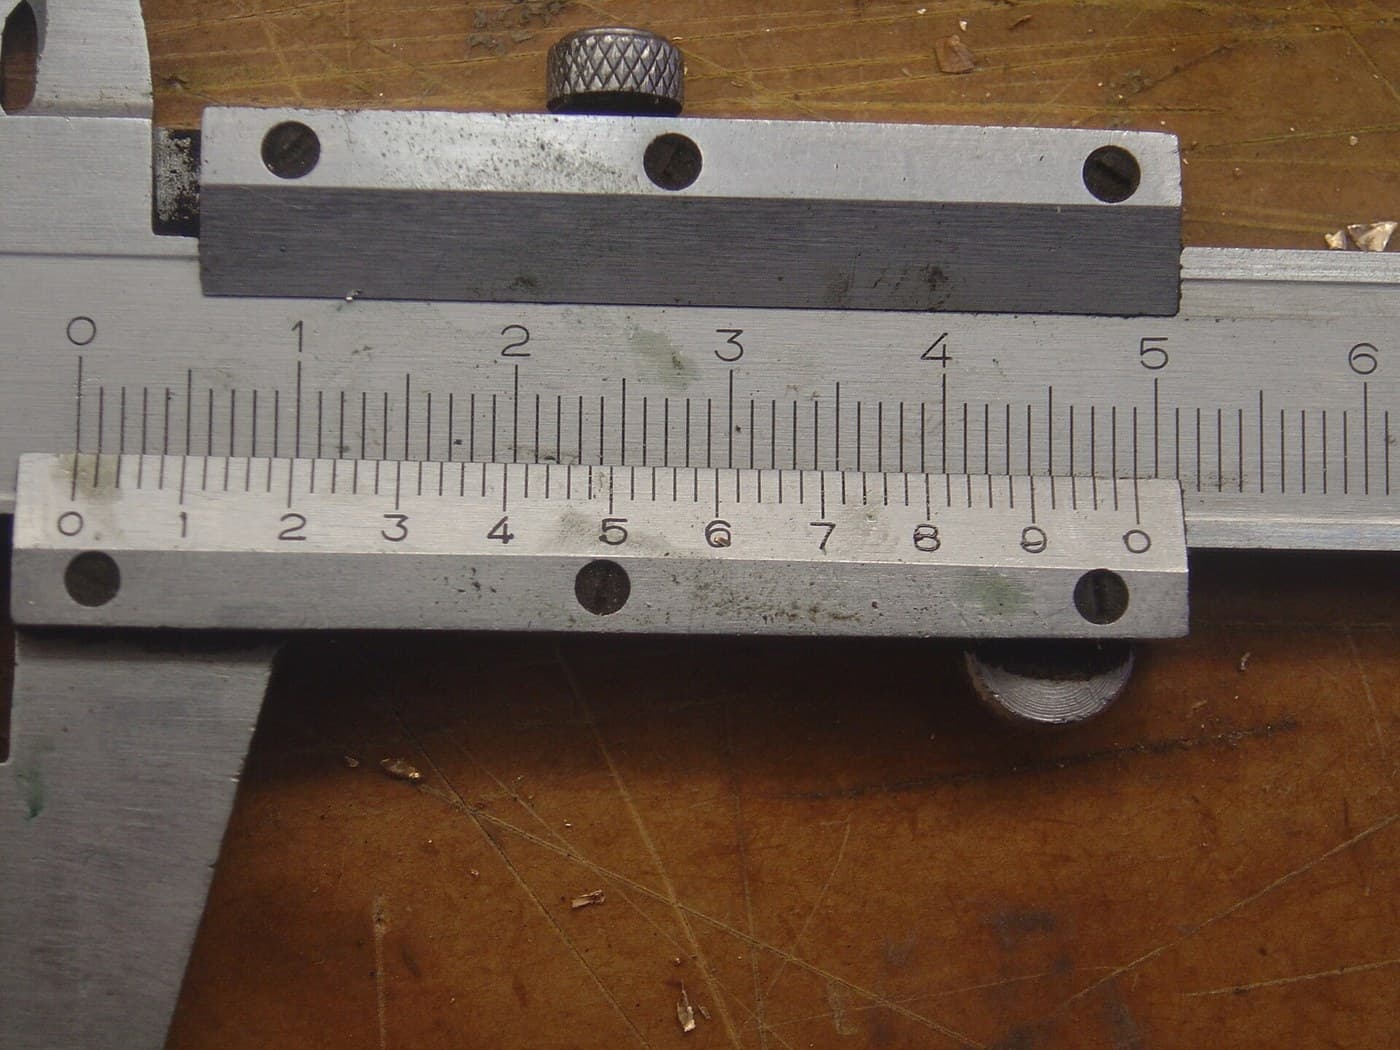
Measure the same way every time
Measure the same way every time
Measure across several diameters and at several heights. A printed hole is not round and not the same size top to bottom — the first layers are squashed wider and the seam where each layer starts leaves a small bump.
Take the smallest reading for a hole and the largest for a peg. Those are what actually decide whether the parts go together, and averaging hides exactly the feature that will stop them.
Deburr before measuring. The small ridge left where each layer starts, and the elephant-foot bulge on the bottom layers, both read as material that is not really in the way — and both come off in seconds with a deburring tool.
このステップの材料:
3D プリント用フィラメント(PLA)1 個必要な工具:
デジタルノギス 6インチ バリ取り工具拡大ルーペ
4
4
Design so the fit does not have to be perfect
Design so the fit does not have to be perfect
The best answer to a tight tolerance is usually to remove the need for it. A slot instead of a hole, a chamfer at the entry, a split collar with a screw, a deliberate flexure — all of them turn a precise dimension into an adjustable one.
A CHAMFER on every hole and peg entry is nearly free and makes an imperfect fit assemble anyway. It also prints better, because the chamfer at the bottom removes the elephant-foot problem from the part that has to enter.
And where a real fit is needed, use a real part: a brass insert for a thread, a steel pin in a printed housing, a bearing pressed into a printed seat. Printing everything is a constraint nobody imposed.
このステップの材料:
3D プリント用フィラメント(PLA)1 個必要な工具:
デスクトップパソコンデジタルノギス 6インチバリ取り工具関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理


CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。