SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI
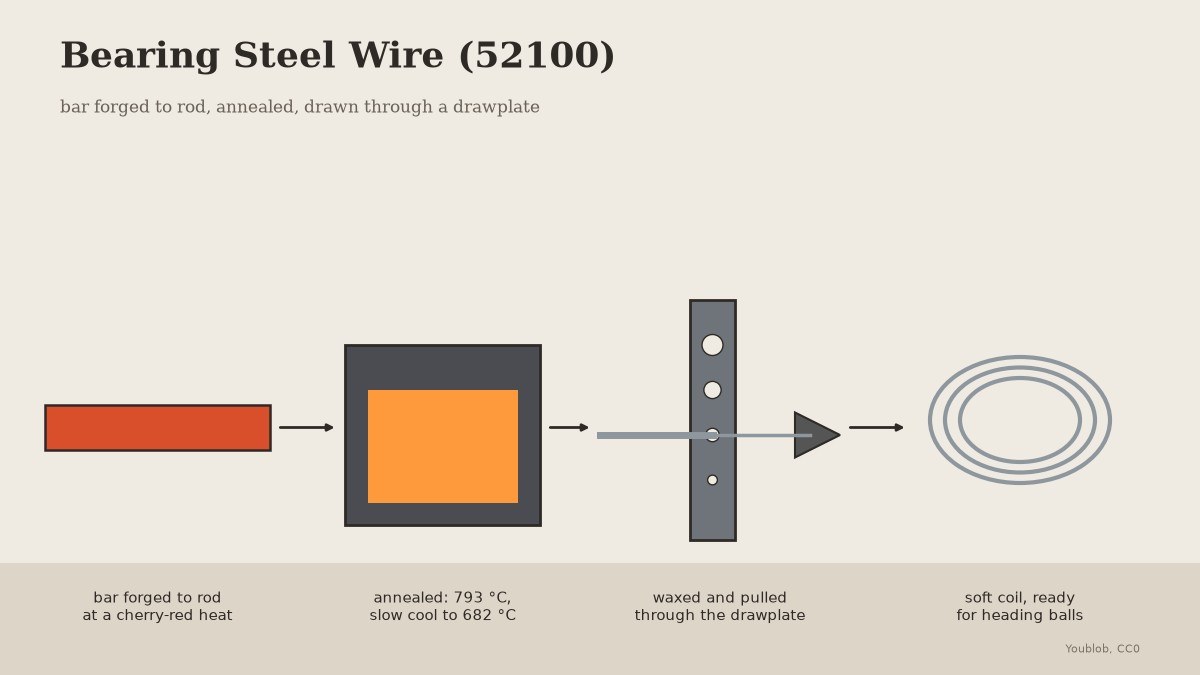


Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
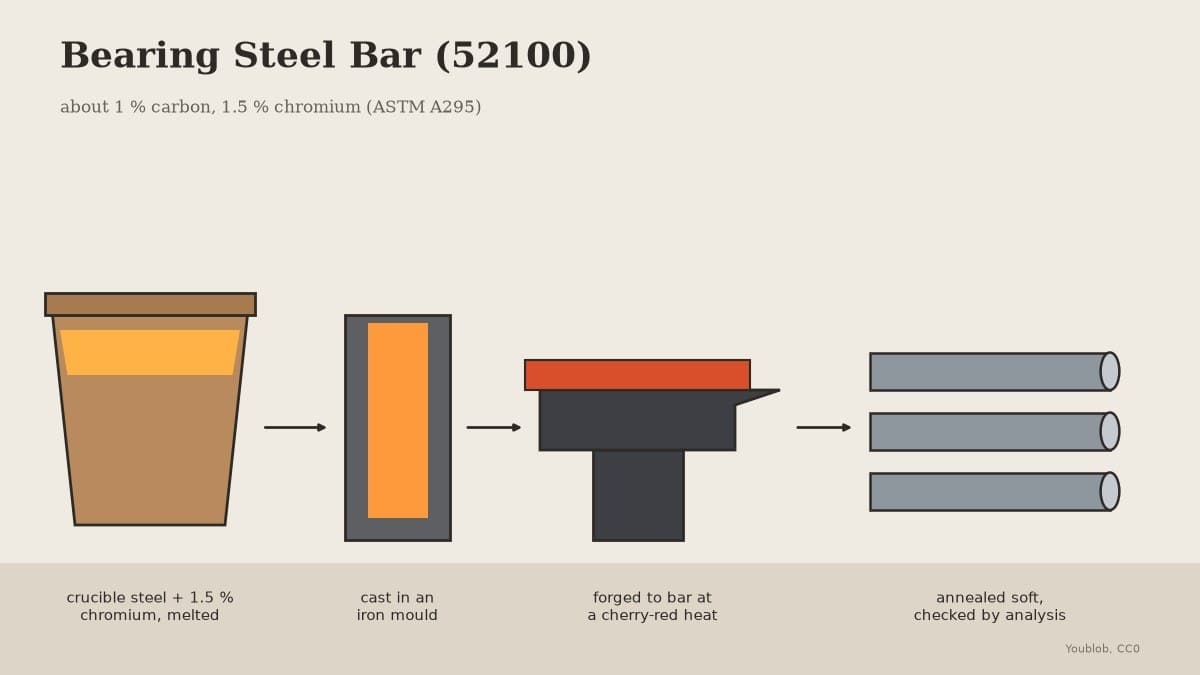
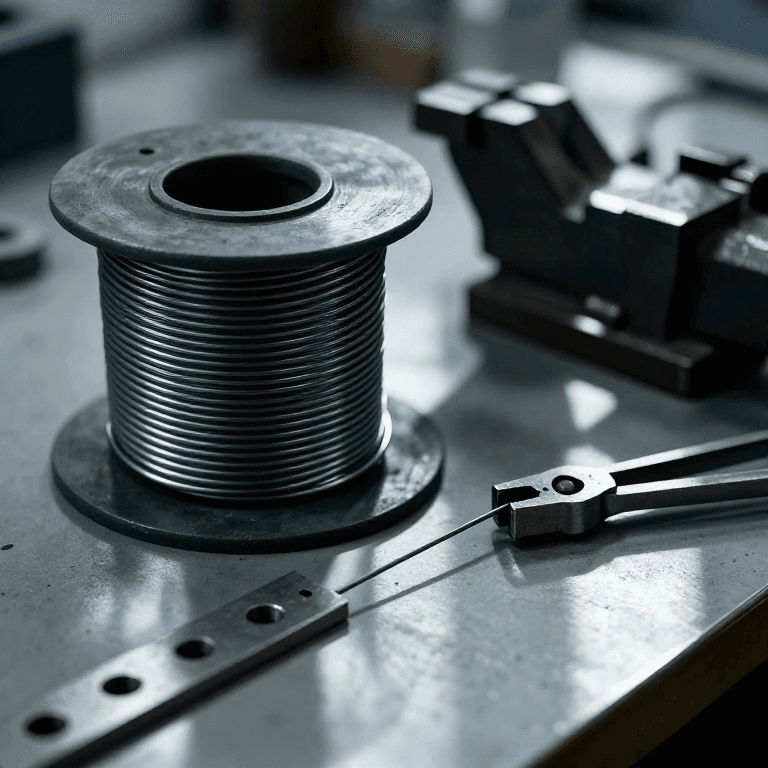
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
The picture: our drawing, bar to coil.
Juu
2 days
Maagizo
1
1
Forge to rod
Forge to rod
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
Vifaa kwa hatua hii:
 Fimbo ya chuma cha beringi (52100)1 kg
 Mkaa1 as required
Zana zinazohitajika:
 Fua ya mhunzi
 Fuawe
 Nyundo yenye kichwa cha msalaba
 Koleo za mhunzi
 Glavu za kulehemu
 Miwani ya usalama
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Zana zinazohitajika:
 Tanuri ya kutibu kwa joto
 Themokapo yenye kionyeshiKoleo za mhunziGlavu za kulehemu
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
Zana zinazohitajika:
 Seti ya brashi za waya
 Seti ya tupa
 Kibano cha meza ya kazi
4
4
Wax and draw
Wax and draw
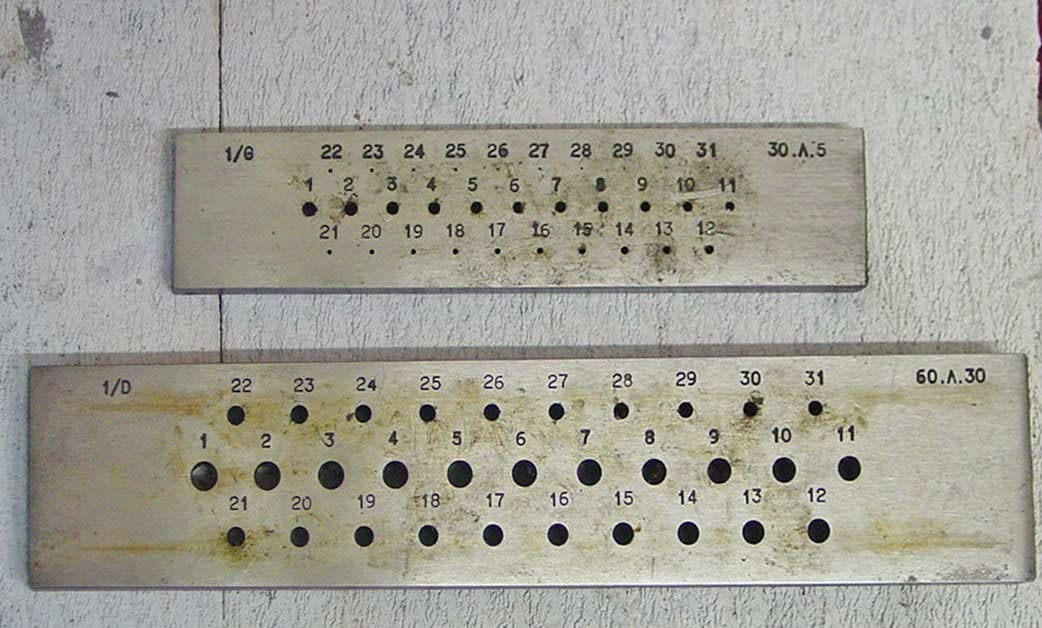
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
Vifaa kwa hatua hii:
 Nta ya Nyuki20 g
Zana zinazohitajika:
 Bamba la chuma la kuvuta waya
 Koleo la kuvutaKibano cha meza ya kazi
 Glavu za Kazi za Ngozi
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Vifaa kwa hatua hii:
Nta ya Nyuki1 kipandeZana zinazohitajika:
Bamba la chuma la kuvuta wayaKoleo la kuvutaTanuri ya kutibu kwa jotoThemokapo yenye kionyeshi6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
Zana zinazohitajika:
 Kipima-unene cha dijitali cha inchi 6Tanuri ya kutibu kwa jotoThemokapo yenye kionyeshi
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
Vifaa
3- Kishikilia Nafasi
- 1 as requiredKishikilia Nafasi
- 1 kipandeKishikilia Nafasi
Zana Zinazohitajika
15- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
Mchoro huu unatengeneza
Blueprint zinazohusiana
Blueprint hizi zinashiriki maarifa — mbinu, vifaa au kanuni
CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.