SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI
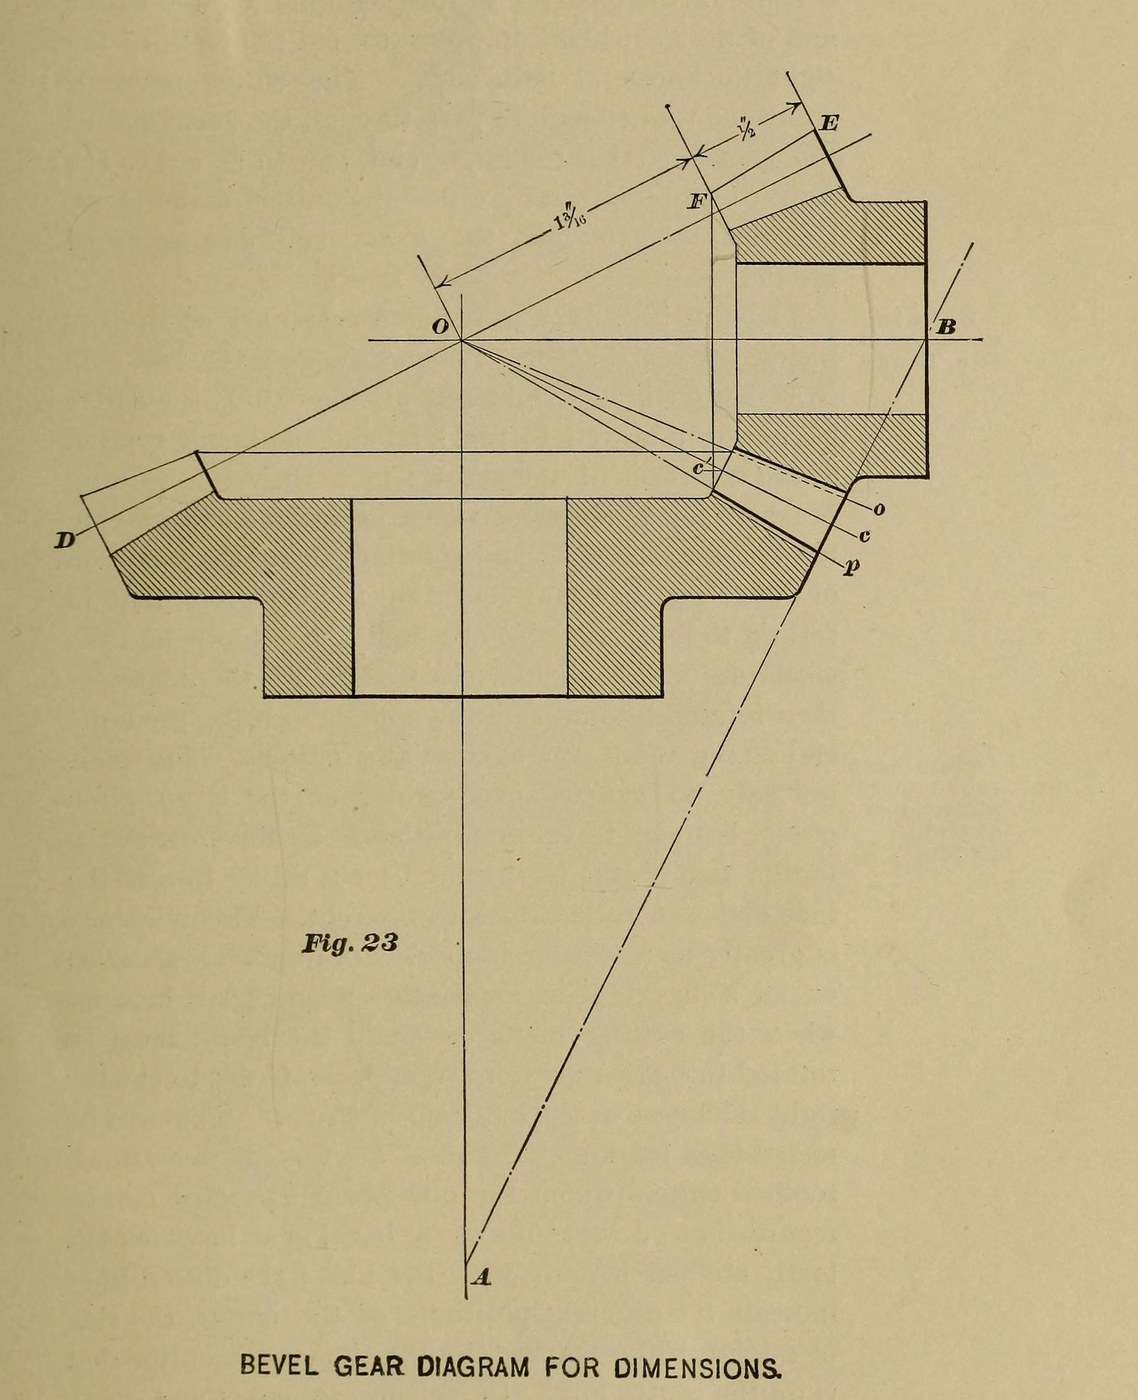


Bevel Pinion with a No. 6 Cutter, Filed at the Small End (Brown & Sharpe 1911)
The same 12-tooth, 8-pitch pinion as Brown & Sharpe's worked example, but cut the way their own shop did it: with a No. 6 cutter instead of the No. 8 they sell for it, cut to the right thickness at the large end, then filed well round at the small end. They did this only for a 12-tooth pinion running with a gear two or three times its size.
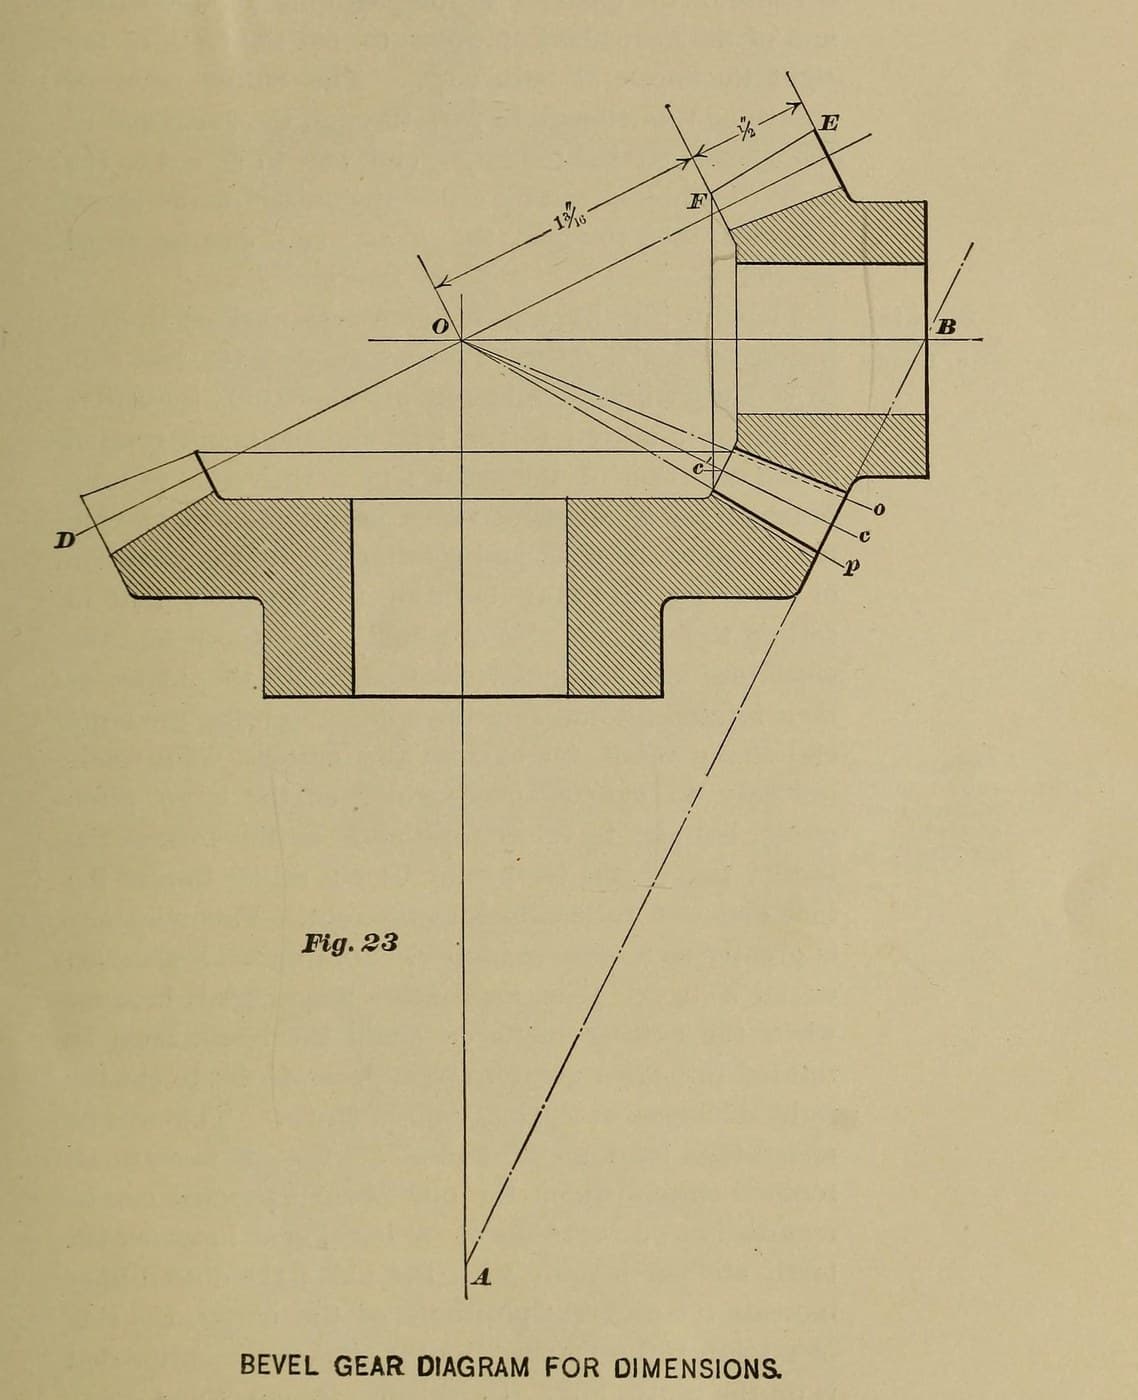
Source: Brown & Sharpe, Practical Treatise on Gearing (1911), Fig. 23 example, Part I ch. IX–X, Part II ch. III and the set-over table p. 58. The blank sizes are our arithmetic with their rules; the steel and bore are ours. Picture: their Fig. 23.
Juu
1 day
Maagizo
1
1
Work out and turn the blank
Work out and turn the blank
Pitch diameter 12 ÷ 8 = 1.500 in. Angle of edge 26° 34′ and angle of face 59° 11′ (Brown & Sharpe's figures for every 12 and 24 tooth pair). Diameter increment = cos 26° 34′ × 0.250 = 0.224 in, so turn the steel blank to 1.72 in outside diameter. Face ½ in long. Try both angles with a protractor against the end of the hub.
Vifaa kwa hatua hii:
 Fito ya chuma laini1 length for one blank
Zana zinazohitajika:
 Kereza ya Chuma
 Chombo cha kukata cha lathe
 Kipima-pembe
 Maikromita
2
2
Choose the cutter
Choose the cutter
Twice the back cone radius × 8 comes to about 13, which would call for a No. 8, but take a No. 6, 8-pitch bevel gear cutter (17 to 20 teeth), as Brown & Sharpe's own shop did for this pinion. Measure its thickness Tc at the pitch line, 0.145 in from its tip.
Zana zinazohitajika:
 Kikata gia pia
 Kalipa ya verinia ya meno ya gia
3
3
Set the head at 22° 18′
Set the head at 22° 18′
Apex distance = sec 26° 34′ × 1.5 = 1.677 in. Angle increment: tan = sin 26° 34′ ÷ 6, giving 4° 16′. Set the dividing head to the cutting angle 26° 34′ − 4° 16′ = 22° 18′ and index 12 spaces. Depth at the large end 0.270 in.
Zana zinazohitajika:
 Mashine ya kusaga chuma
 Kichwa cha KugawanyaKikata gia pia
4
4
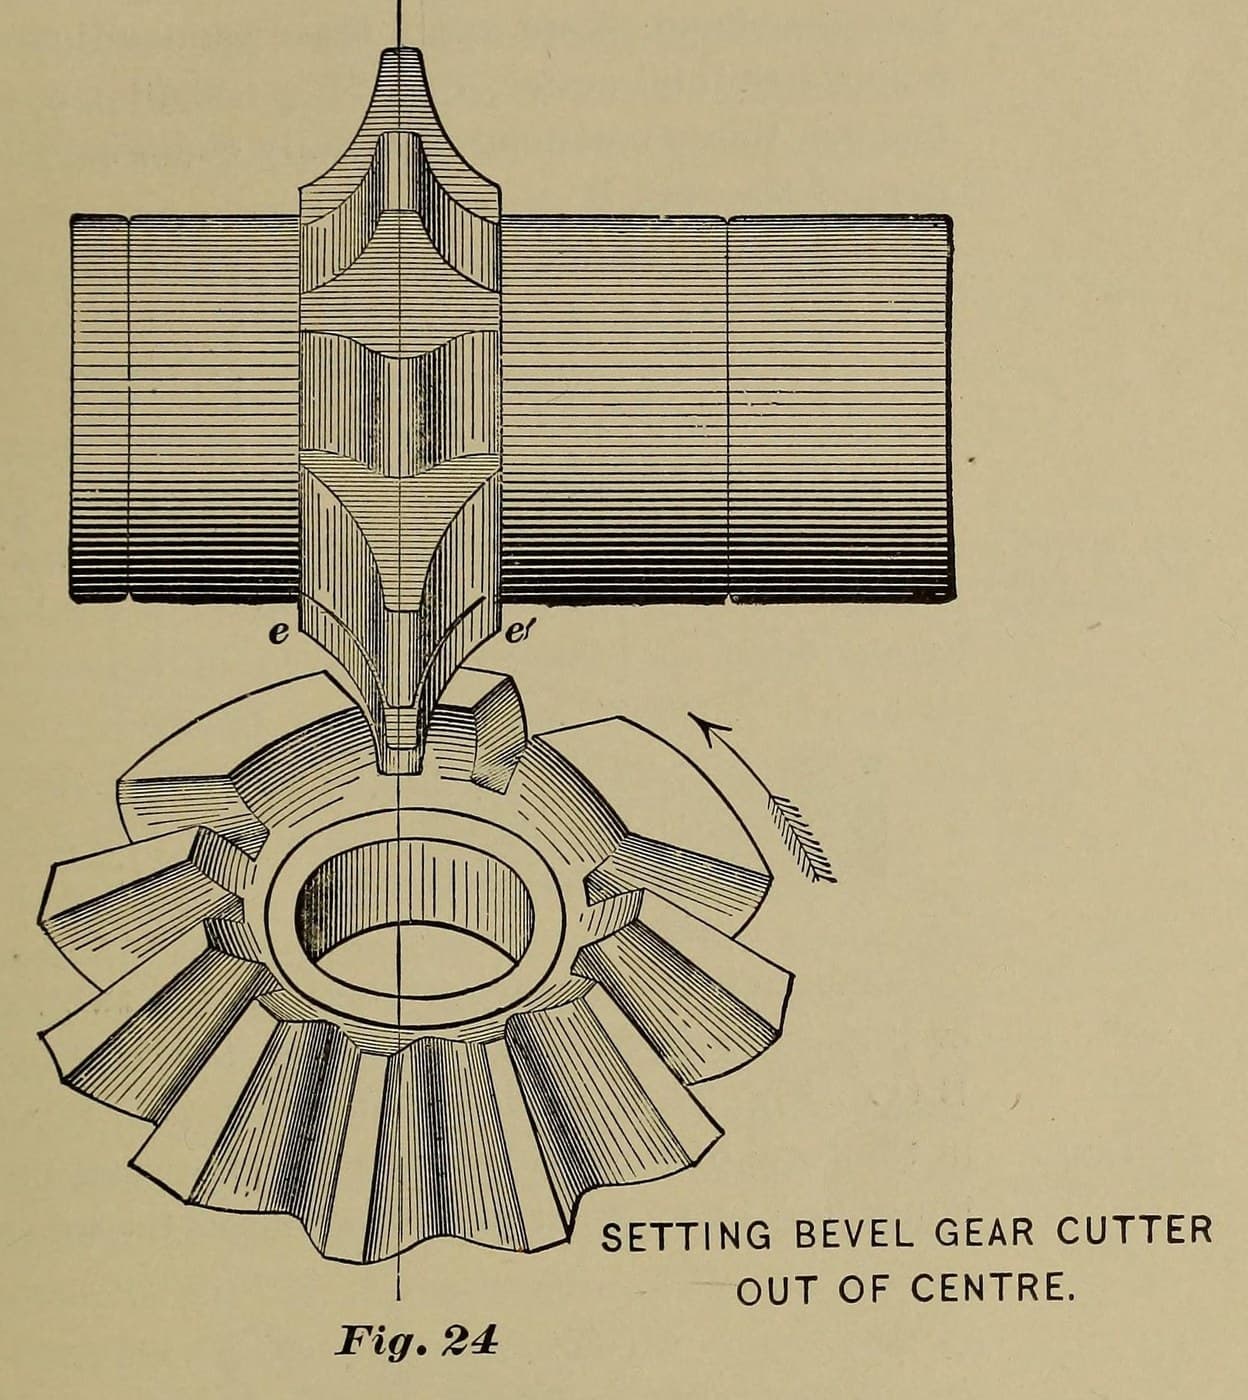
Set over and cut one side
Set over and cut one side
Apex distance ÷ face = 3.35; we take the nearest column, 3¼, where a No. 6 cutter has the factor .318. Set-over = Tc ÷ 2 − .318 ÷ 8 = Tc ÷ 2 − 0.040 in. Set off centre by that amount, take up backlash, and cut round all 12 spaces.
Zana zinazohitajika:
Mashine ya kusaga chumaKichwa cha KugawanyaKikata gia pia5
5
Set over the other way and trim
Set over the other way and trim
Set over the same amount the other side, line the cutter up with the space at the small end, take a trial cut, and rotate toward the cutter until the tooth is right at the faces of the large end: 0.196 in at the pitch line (0.138 in at the small end). Check with the gear tooth vernier, then cut round.
Zana zinazohitajika:
Mashine ya kusaga chumaKichwa cha KugawanyaKikata gia piaKalipa ya verinia ya meno ya gia6
6
File the small ends
File the small ends
The No. 6 cuts the tooth sides with a longer curve than the No. 8, so expect considerable filing: round the teeth over at the small ends, without filing them thinner at the pitch line.
Zana zinazohitajika:
 Tupa laini
Vifaa
1- 1 length for one blankKishikilia Nafasi
Zana Zinazohitajika
9- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
Mchoro huu unatengeneza
Blueprint zinazohusiana
Blueprint hizi zinashiriki maarifa — mbinu, vifaa au kanuni
CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.