SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI
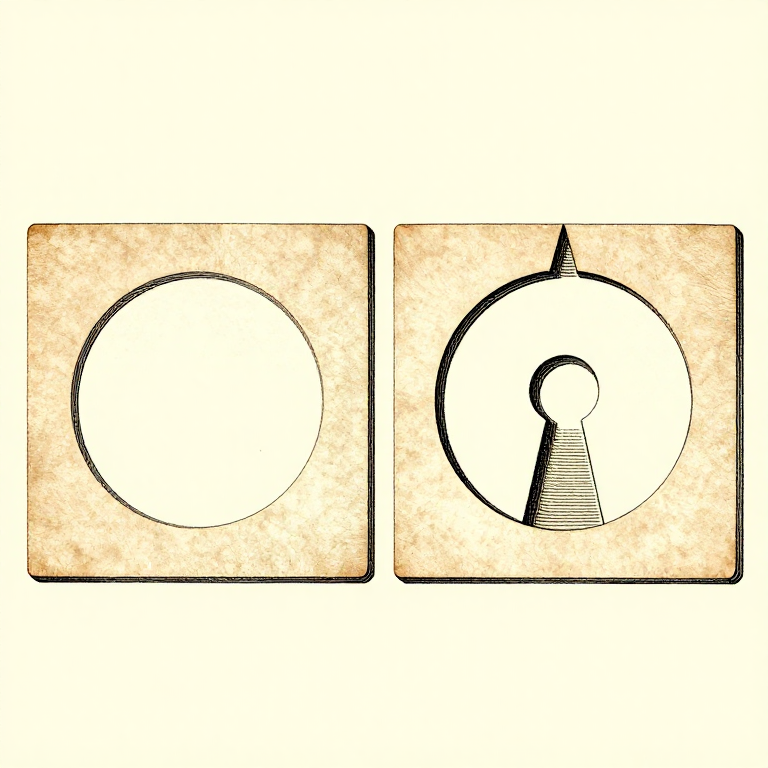

Designing For the Process: A Printable Part Is a Different Shape
A model drawn without thinking about printing can usually be printed. A model drawn WITH the process in mind prints faster, stronger, with no supports and a better surface — from the same amount of design effort.
Every rung before this one is a constraint: layers are weak in one direction, overhangs have a limit, holes come out small, corners warp, walls carry the load. Design is where those stop being problems to work around and become the rules the shape is drawn to.
That is the same move as designing a casting with draft angles, or a timber frame with wood movement allowed for. The process has a grain, and a good design runs with it.
Juu
4 hours
Maagizo
1
1
Chamfer the bottom, fillet the rest
Chamfer the bottom, fillet the rest
A 45-degree CHAMFER on the bottom edge of a part is self-supporting, removes the elephant-foot bulge, and makes the part easier to insert into anything. It is close to free and almost always an improvement.
Fillets elsewhere reduce stress concentration and warping, exactly as a radiused corner does on any other part. Internal corners especially: a sharp internal corner is where a printed part cracks.
But do NOT fillet the bottom edge — a bottom fillet is an overhang that starts at 90 degrees, which is the one angle nothing can print. Chamfer at the bottom, fillet above it, and that single rule removes a lot of support material.
Vifaa kwa hatua hii:
 Uzi wa uchapishaji 3D (PLA)1 kipande
Zana zinazohitajika:
 Kompyuta ya mezani
 Programu ya kukata faili za 3MF
 Kifaa cha kuondoa ukingo
2
2
Turn overhangs into bridges and teardrops
Turn overhangs into bridges and teardrops
A horizontal hole printed round has an unsupported arch at the top that sags. Printed as a TEARDROP — a circle with a 45-degree point on top — it is entirely self-supporting and needs no support at all.
A hexagonal hole does the same job and takes a nut. So does simply making the top of the hole a flat bridge rather than a curve, which prints well for the reasons the overhang rung gives.
The general form: wherever the model has a surface between 45 and 90 degrees, ask whether it can become a chamfer, a bridge, or a shape with a point on top. Nearly always it can, and nearly always the result is better than supporting it.
Vifaa kwa hatua hii:
Uzi wa uchapishaji 3D (PLA)1 kipandeZana zinazohitajika:
Kompyuta ya mezaniProgramu ya kukata faili za 3MF Kipima-unene cha dijitali cha inchi 6
3
3
Split the part where splitting helps
Split the part where splitting helps
A part that needs supports, or warps, or is too tall to be stable, can often be cut into two pieces that each print flat and are then glued or bolted.
Put the split where a joint is natural — at a change of section, behind a flange — and add a locating feature, a peg and socket or a dovetail, so the two halves cannot be assembled wrong. Design the clearance into one side only, as the tolerance rung sets out.
Splitting also lets each half be oriented for its own load path, which the orientation rung says is the highest-leverage decision available. A part split into two well-oriented halves can be stronger than the same part printed whole.
Vifaa kwa hatua hii:
Uzi wa uchapishaji 3D (PLA)1 kipandeZana zinazohitajika:
Kompyuta ya mezaniProgramu ya kukata faili za 3MFKipima-unene cha dijitali cha inchi 6Kifaa cha kuondoa ukingo4
4
Use real hardware where it belongs
Use real hardware where it belongs
Printed threads are weak, printed bearings wear, and printed springs creep. Heat-set brass inserts, steel pins, real bearings and real fasteners cost very little and remove the weakest parts of a printed assembly.
Design the pocket for them from the start: a straight bore for an insert, a captive hex pocket for a nut, a shoulder for a bearing to seat against. A pocket designed in prints perfectly; one drilled afterwards splits the part along a layer.
Which is the whole argument of this batch. The printer is one process among several, it has specific strengths and specific limits, and the best results come from using it for what it is good at and something else for the rest.
Vifaa kwa hatua hii:
Uzi wa uchapishaji 3D (PLA)1 kipande Filamenti ya PETG yenye nyuzi za kaboni1 kipande
Zana zinazohitajika:
Kompyuta ya mezaniKipima-unene cha dijitali cha inchi 6 Seti ya zana za printa ya 3D
Vifaa
2- 4 vipandeKishikilia Nafasi
- Filamenti ya PETG yenye nyuzi za kaboniKamisheni 10%1 kipandeKishikilia Nafasi
Blueprint zinazohusiana
Blueprint hizi zinashiriki maarifa — mbinu, vifaa au kanuni
Tolerance and Clearance: Printed Holes Come Out Small, Every Time
na 3DBonanza
Utengenezaji wa nyongeza
23
0
0
0
0
0
Orientation: A Printed Part Is Weakest Between Its Layers
na 3DBonanza
Utengenezaji wa nyongeza
18
0
0
0
0
0
Overhangs, Bridges and Support: What the Machine Can Print Over Thin Air
na 3DBonanza
Utengenezaji wa nyongeza
19
0
0
0
0
0
CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.