Ushirikiano
SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI
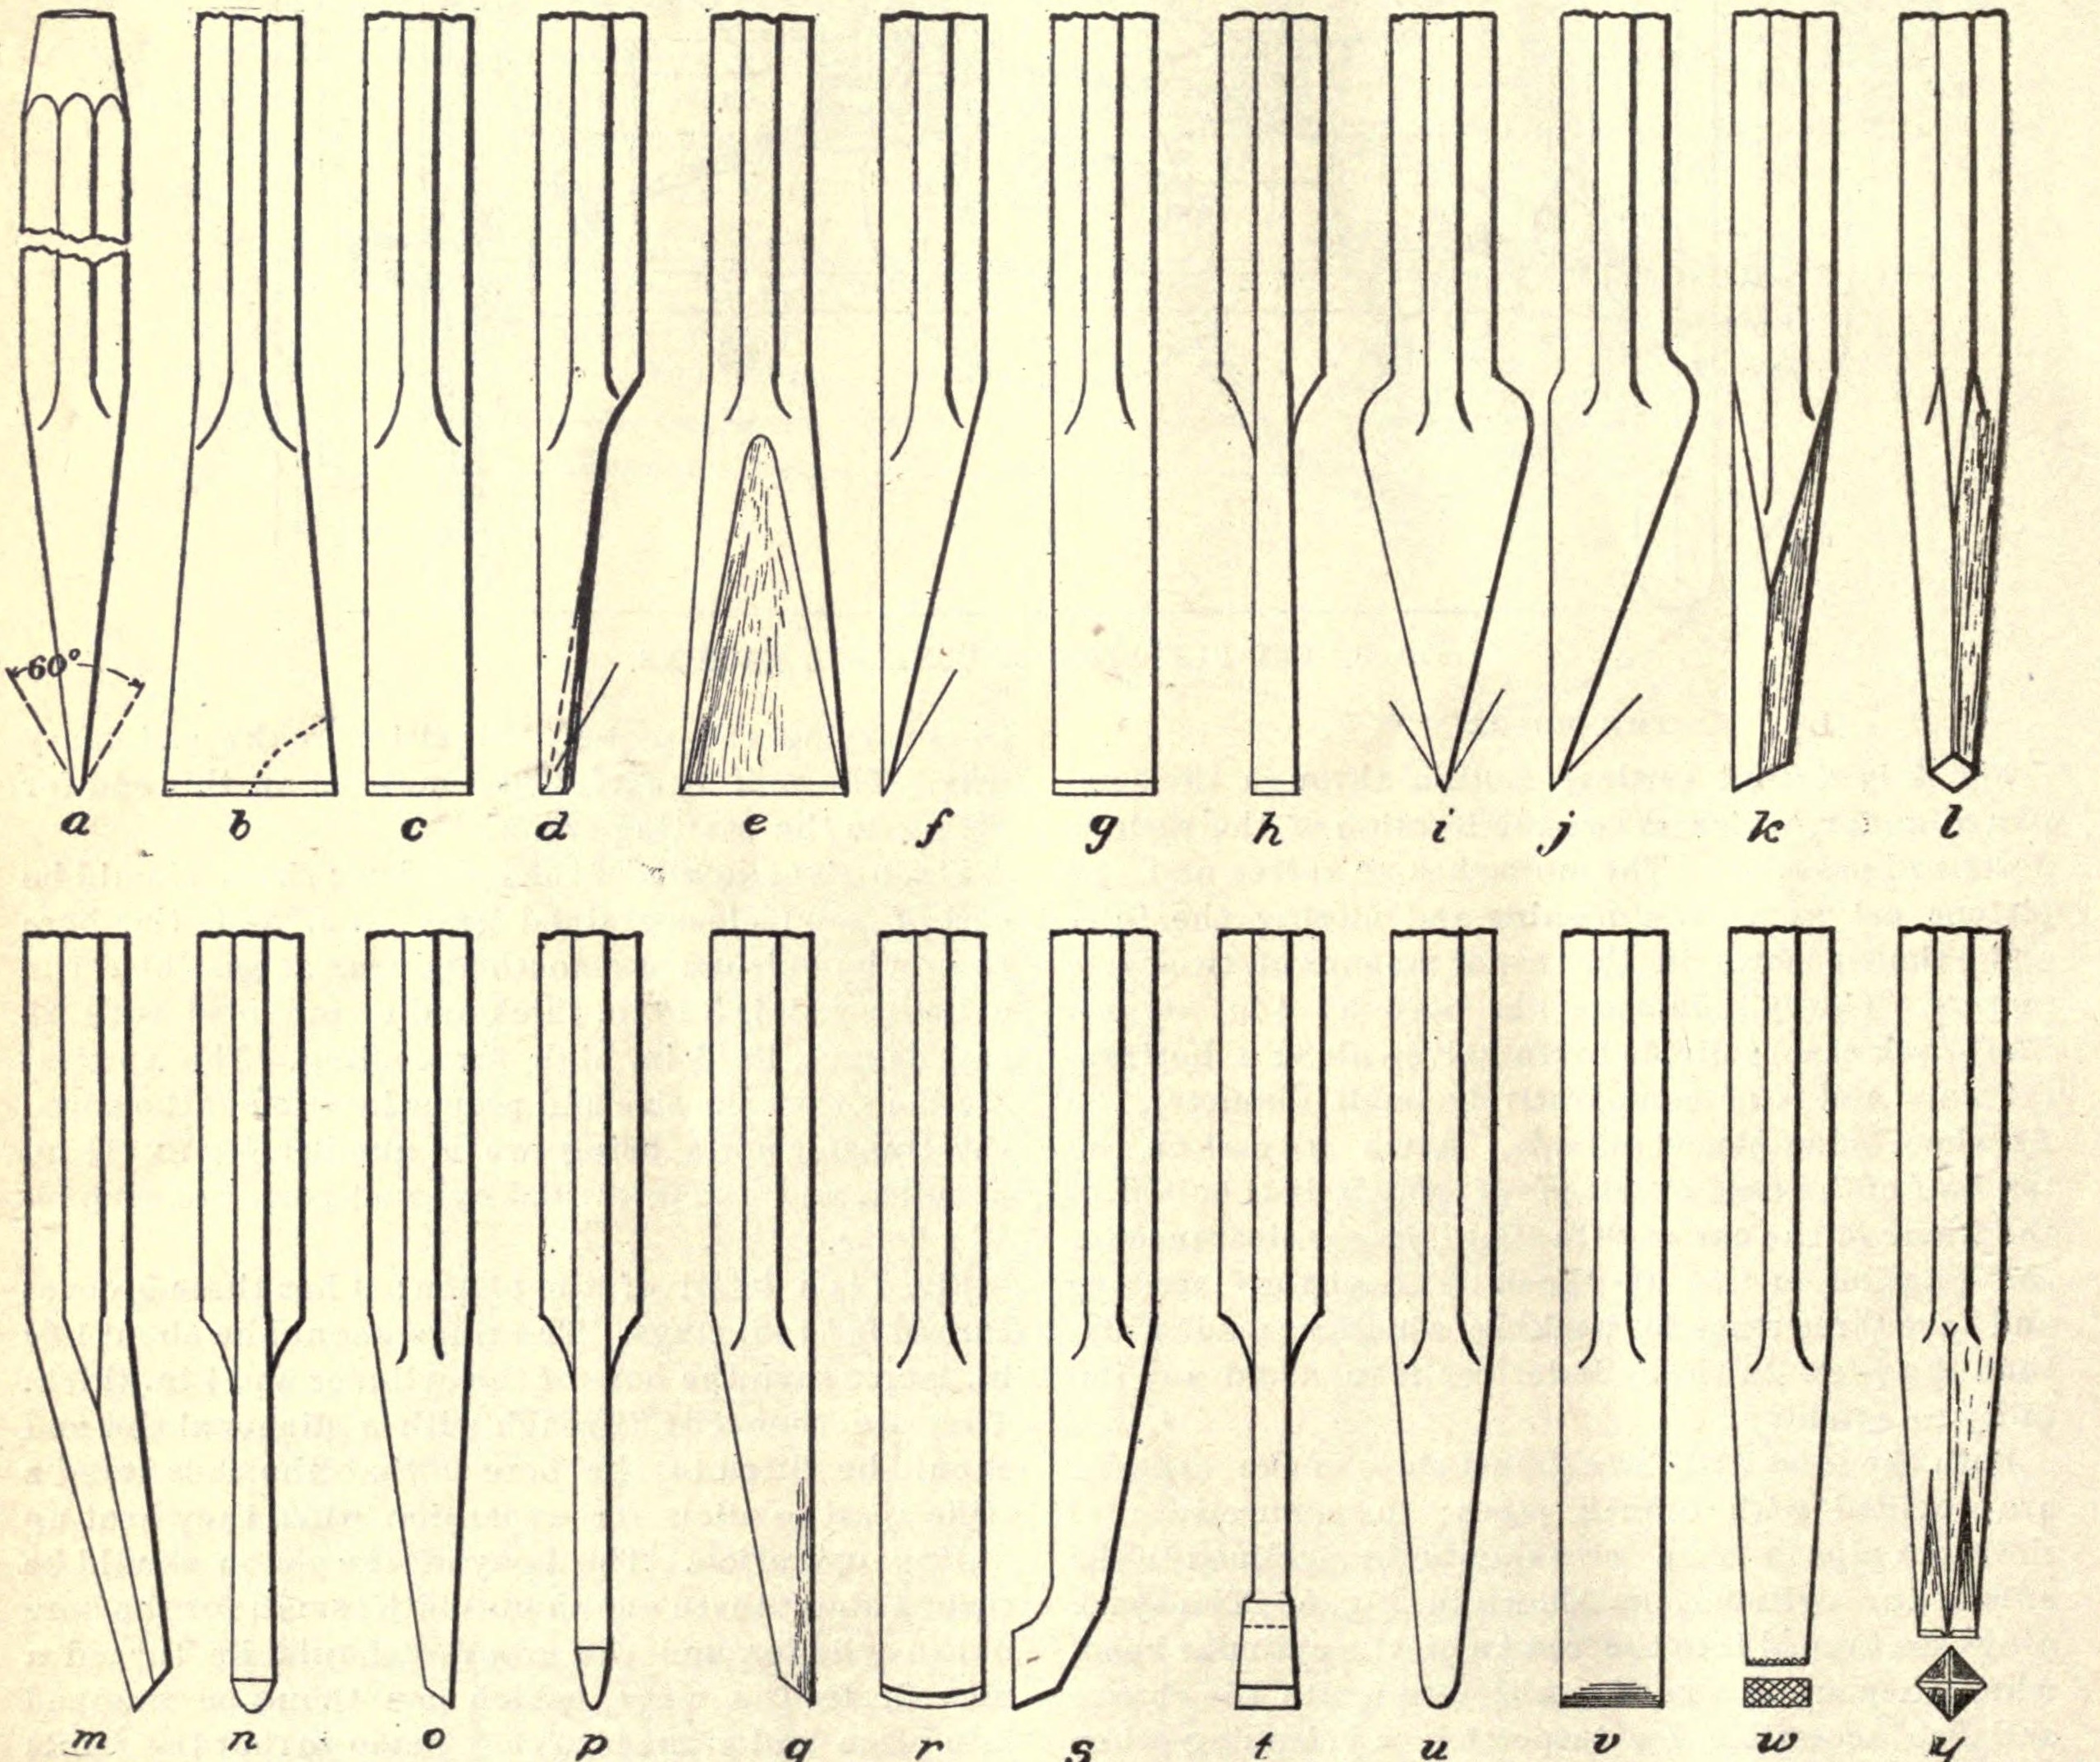


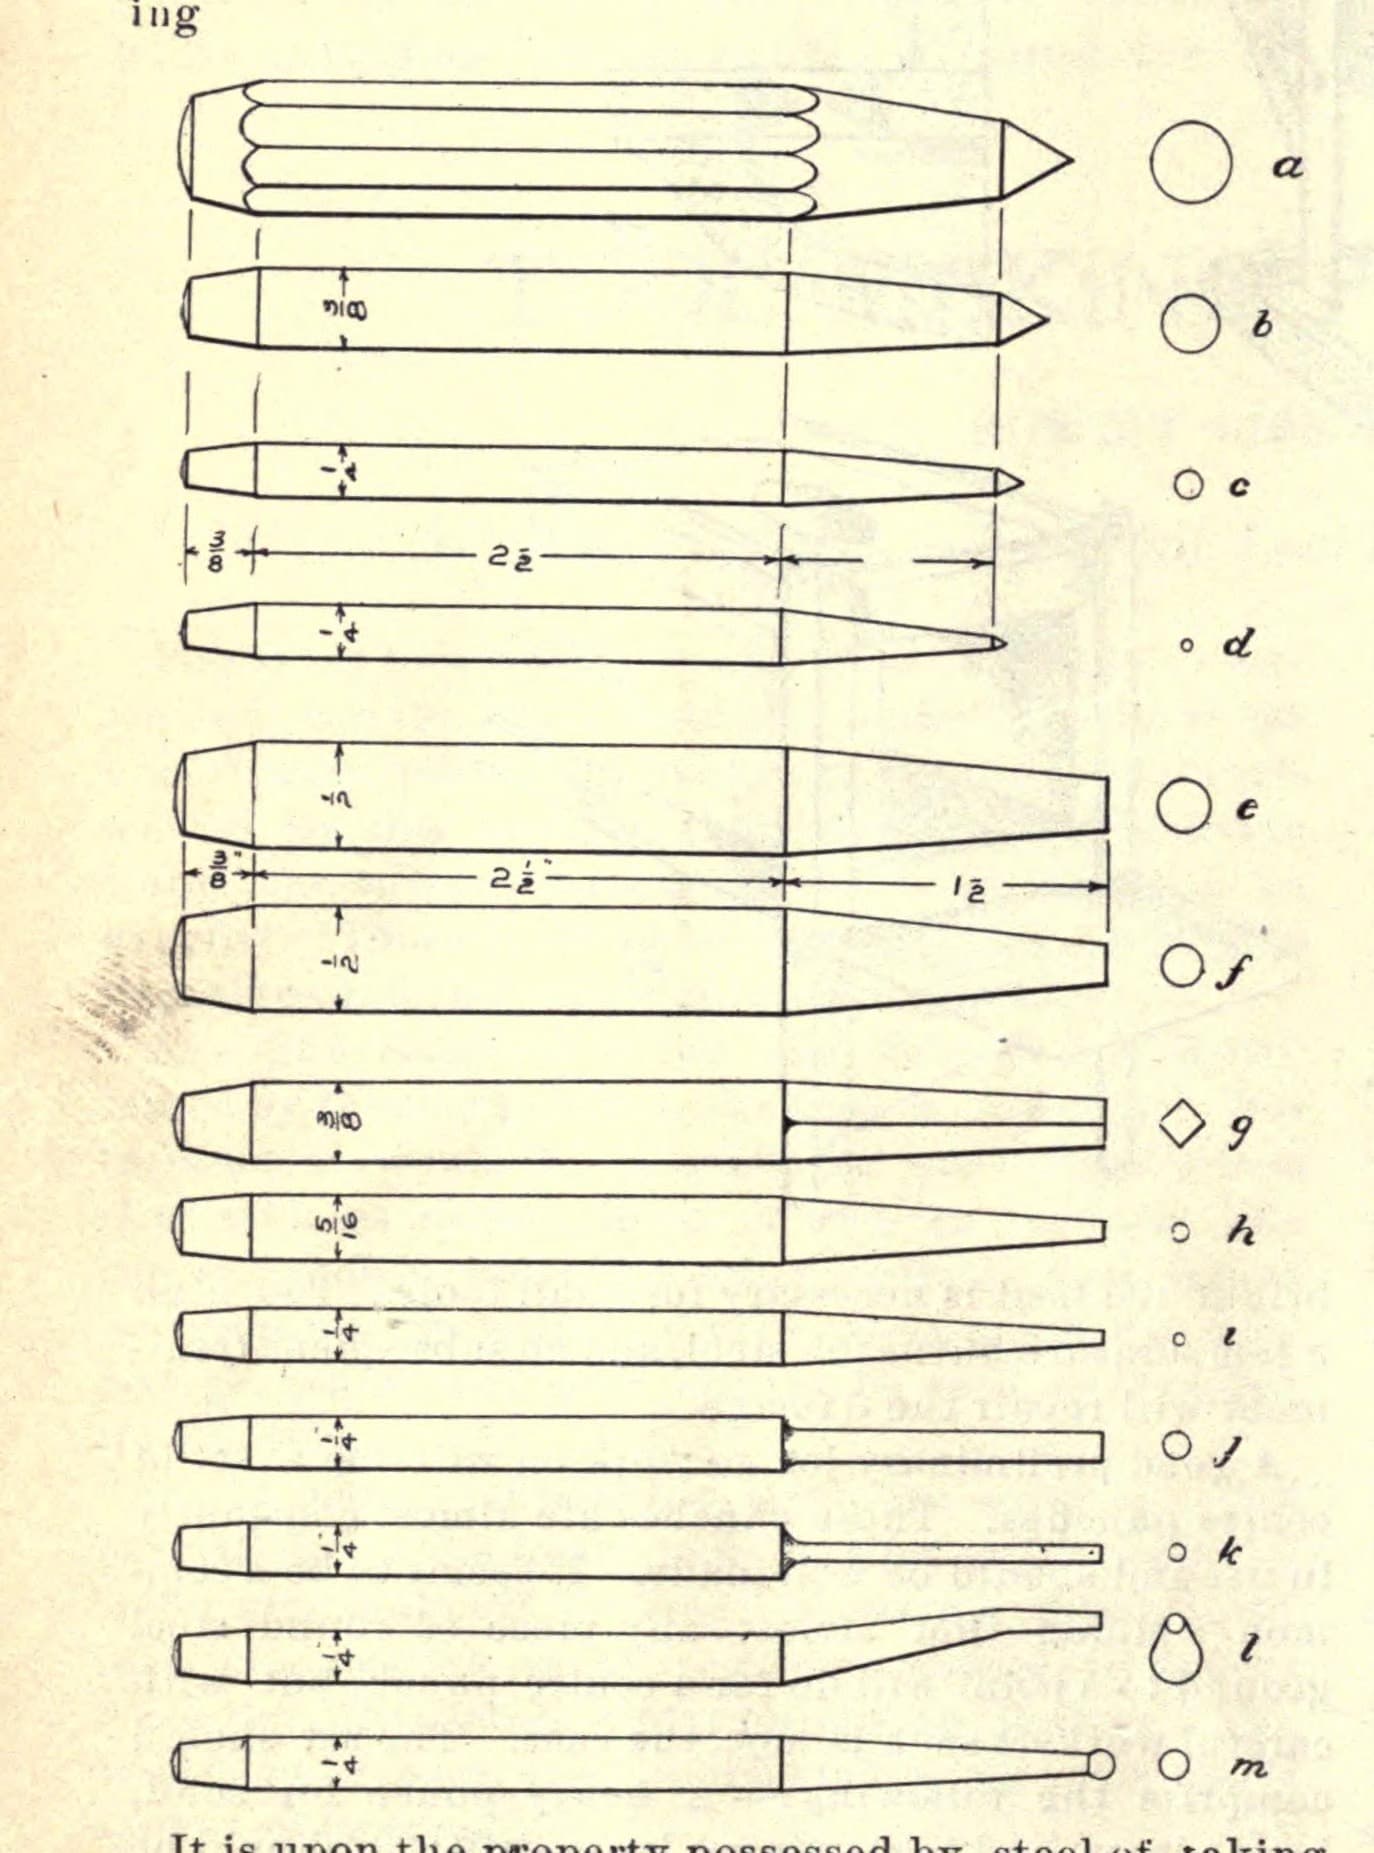
A Set of Cold Chisels: Flat, Gouge, Side, Cape, Diamond-Point and Round-Nose, Edge Hardened Only, Tempered Purple (Griswold, 1904)
Robert Gibson Griswold's working set of cold chisels from Amateur Work (Boston, 1904): octagonal tool steel or old files forged about 5 in. long, flat chisels 3/8 to 1 in. with a 60 degree edge, plus gouges, side, cape, diamond-point and round-nose chisels; only the last 1/8 in. of the edge hardened, tempered light purple for steel or dark purple for iron.
Kati
Two or three days for the set
Maagizo
1
1
His sizes
His sizes
Inapakia daftari la Jupyter…
2
2
Read Griswold
Read Griswold
"When the tool is forged the edge only must be hardened for about 1/8 in., the metal above being left softer to withstand the shock."
3
3
Forge the blanks
Forge the blanks
From octagonal tool steel (or old files) forge each chisel about 5 in. (127 mm) from head to edge with a gradual taper to the edge, and forge the head down so it does not broom. Forging steps are ours: forge at a bright red only, as in his part I.
Vifaa kwa hatua hii:
 Kipande cha pembe nane cha feleji ya zana1 kipande
Zana zinazohitajika:
 Fua ya mhunzi
 Fuawe
 Nyundo
 Koleo za mhunzi
4
4
Shape the edges
Shape the edges
Flat chisels 3/8, 1/2, 5/8 and 1 in. wide; gouges 1/4-5/8 in. with the bevel inside; side chisels 1/4, 3/8, 1/2 in. with the edge in one flat side; cape chisels 3/16 and 1/4 in. with the stock behind slightly thinner; a diamond point about 1/8 in. on the square (bent version for flat work); round-nose chisels, heavy and a long-tapered drawing chisel (his fig. 1).
Zana zinazohitajika:
Fua ya mhunziFuaweNyundo Tupa (Tupa ya Mkono)
5
5
Harden the edge only
Harden the edge only
Heat the edge and harden only about 1/8 in. (3 mm) of it in water, leaving the body softer: a chisel hard too far up cracks off on a line under a heavy blow.
Vifaa kwa hatua hii:
 Maji1 kipande
Zana zinazohitajika:
Fua ya mhunziKoleo za mhunzi Ndoo
6
6
Temper purple
Temper purple
Brighten the edge with emery cloth and let the heat run the colour down: light purple (530 F) for chisels used on steel, dark purple (550 F) for cast and wrought iron; then cool.
Vifaa kwa hatua hii:
 Kitambaa cha emeri1 kipandeMaji1 kipande
Zana zinazohitajika:
Ndoo7
7
Grind
Grind
Grind the flat chisel edges to about 60 degrees (45-75: blunter for heavy work), keeping the edge from blueing.
Zana zinazohitajika:
 Kisagia cha meza
8
8
Troubleshooting
Troubleshooting
Cold chisel troubleshooting.
Flow
Loading...
9
9
History and honest limits
History and honest limits
From Robert Gibson Griswold, "Tool Making for Amateurs" II, **Amateur Work** (Boston), vol. III (1903-04), pp. 304-305 and fig. 1 (checked on the archive.org scan amateurwork03bostrich); temper temperatures from his part I table. Forging heats, metric figures and tools are ours.
Vifaa
3- Kishikilia Nafasi
- 2 vipandeKishikilia Nafasi
- 1 kipandeKishikilia Nafasi
Mchoro huu unatengeneza

Blueprint zinazohusiana
Blueprint hizi zinashiriki maarifa — mbinu, vifaa au kanuni

CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.