Ushirikiano
SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI
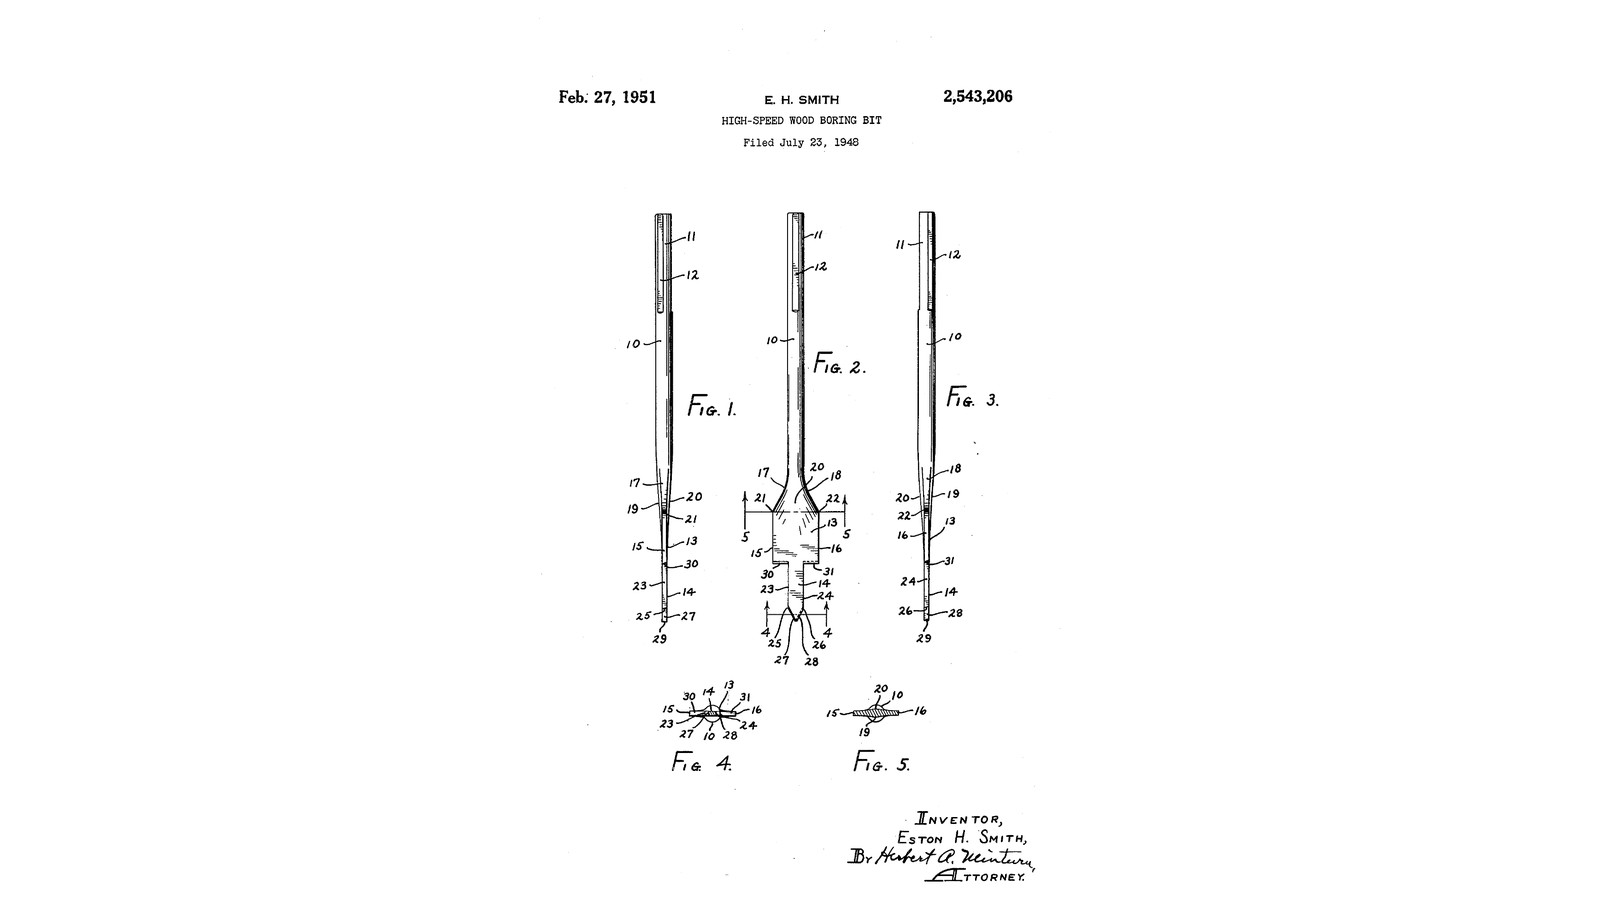


Long-Pilot High-Speed Wood Bits: A Flat Plate and a Long Square-Edged Pilot, No Screw Feed (Smith, 1951)
Eston H. Smith of Indianapolis received US 2,543,206, dated 27 February 1951, for a flat wood-boring bit made for the high speeds of an electric drill, 2,000 to 3,500 revolutions a minute. A flat plate on a thin stem has edges square to its faces and exactly the same width all the way down. A long flat pilot below it keeps the bit centred until it is through. With no screw feed it can bore at an angle, into another hole, or overlapping one, without splitting the wood. The thin stem leaves room for the shavings to come out.
We forge his 3/4 inch bit to his figures, with 1/2 and 1 inch bits beside it.
Kati
About 1 day
Maagizo
1
1
His figures in millimetres
His figures in millimetres
Inapakia daftari la Jupyter…
2
2
Read US 2,543,206
Read US 2,543,206
"It is extremely important however that these edges 15 and 16 be of exactly constant width from top to bottom, else the holes will not be bored true, and chattering and heating might develop."
3
3
Forge the blades
Forge the blades
Cut three 170 mm lengths of 10 mm octagonal tool steel. Heat 50 mm of one end to a bright orange in the forge and flatten it on the anvil to about 3 mm thick, centred on the bar. Hammer across it with the peen to spread it wider than the bit, about 2 mm over its size: 15, 21 and 27 mm. Draw the neck down smoothly where the blade meets the bar and keep the blade in line with it. Reheat as soon as the colour fades to red. Finally heat each one to a cherry red and let it cool slowly in the air, to soften it for filing.
Vifaa kwa hatua hii:
 Kipande cha pembe nane cha feleji ya zana3 vipande
Zana zinazohitajika:
 Msumeno wa chuma
 Kibano cha meza ya kazi
 Jiko la Kufua
 Fuawe
 Nyundo ya Kufua
 Koleo la forji
 Glavu za kulehemu
 Miwani ya usalama
4
4
Print the grinding template
Print the grinding template
Full-size A4 template: the outlines of the 1/2, 3/4 and 1 inch bits with the long flat pilot. Print at 100 %; its 50 mm bar must measure 50 mm.
5
5
Grind the outline
Grind the outline
Glue each outline on its blade, centred on the bar, and grind to the lines on the bench grinder, dipping the steel in water often. Grind the faces flat and parallel to 2.4 mm (3/32 inch). Grind the plate's two side edges and the pilot's two side edges square to the faces and exactly parallel; check the plate's width with the caliper at the top and the bottom, it must not change. Grind three flats on the end of the stem, 20 mm long, for the chuck's jaws.
Zana zinazohitajika:
 Printa ya kupuliza wino
 Gundi
 Kisagia cha meza
 Ndoo ya kupoza chuma
 Maji
 Seti ya tupaKibano cha meza ya kazi
 Kipima-unene cha dijitali cha inchi 6Miwani ya usalama
6
6
Grind the clearances
Grind the clearances
The bit turns clockwise seen from the stem. Grind each cutting edge either side of the pilot square to the axis, with no top rake, and a clearance of 15 degrees behind it, on the face that trails. Grind the pilot's two point edges to 58 degrees included and give each a clearance of 9 degrees the same way. Leave a 1 mm flat at the tip, square to the axis.
Zana zinazohitajika:
Kisagia cha mezaNdoo ya kupoza chumaMajiSeti ya tupaKibano cha meza ya kazi7
7
Harden and temper
Harden and temper
Heat the blade and the neck evenly to a cherry red, until a magnet no longer sticks to it, and quench it straight down in water, moving it up and down. Rub the faces bright with a stone. Heat the shank gently 30 mm behind the blade and watch the colours run down; quench again as soon as a dark straw colour reaches the shoulders and the point. Do the other two.
Zana zinazohitajika:
Jiko la KufuaKoleo la forji Sumaku NdogoNdoo ya kupoza chumaMaji
 Jiwe la KunoleaGlavu za kulehemuMiwani ya usalama
8
8
Sharpen and test
Sharpen and test
Hone the cutting edges on the shoulders and the point with the stone, keeping their angles, and take the burr off. Chuck a bit by its flats and bore a scrap of hardwood: it should start on the point without wandering, cut two clean shavings from the shoulders and leave a round hole of its own size; check it with the caliper.
Zana zinazohitajika:
Jiwe la Kunolea Kekee cha Betri
 Ubao wa Mti MgumuKipima-unene cha dijitali cha inchi 6Miwani ya usalama
9
9
Troubleshooting
Troubleshooting
Long-pilot bit troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
**Eston H. Smith** of Indianapolis, assignor to Benjamin B. Aufderheide, US 2,543,206, dated 27 February 1951, filed 23 July 1948. He claimed a flat plate on a stem with a flat pilot, their edge faces at ninety degrees to their faces, a pilot point of 55 to 60 degrees with 8 to 10 degree clearances, and cutting edges square to the pilot with a clearance of between 15 and 20 degrees (his text says 10 to 20). His figures are for the 3/4 inch bit; the 1/2 and 1 inch bits are ours, with his pilot and edge height. His stem is about 1/4 inch with flats; ours is octagonal tool steel with three ground flats. He gives no material or heat treatment; those are ours.
Vifaa
1- Kishikilia Nafasi
Zana Zinazohitajika
19- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- 1 vendor sell this, none ship to you yetKishikilia Nafasi
- Kishikilia Nafasi
Faili za muundo
1Mchoro huu unatengeneza

Blueprint zinazohusiana
Blueprint hizi zinashiriki maarifa — mbinu, vifaa au kanuni
CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.