
Continuous Casting
안내
Build the bottomless water-cooled mould
Build the bottomless water-cooled mould
A short copper tube with water around it and nothing underneath.
- Make a mould 40 mm square in section and only 150 mm long, from copper or thick aluminium.
- Build a water jacket around its outside with inlet at the bottom and outlet at the top.
- Taper the bore very slightly, wider at the top, to allow for the strand shrinking as it cools.
- Leave both ends fully open.
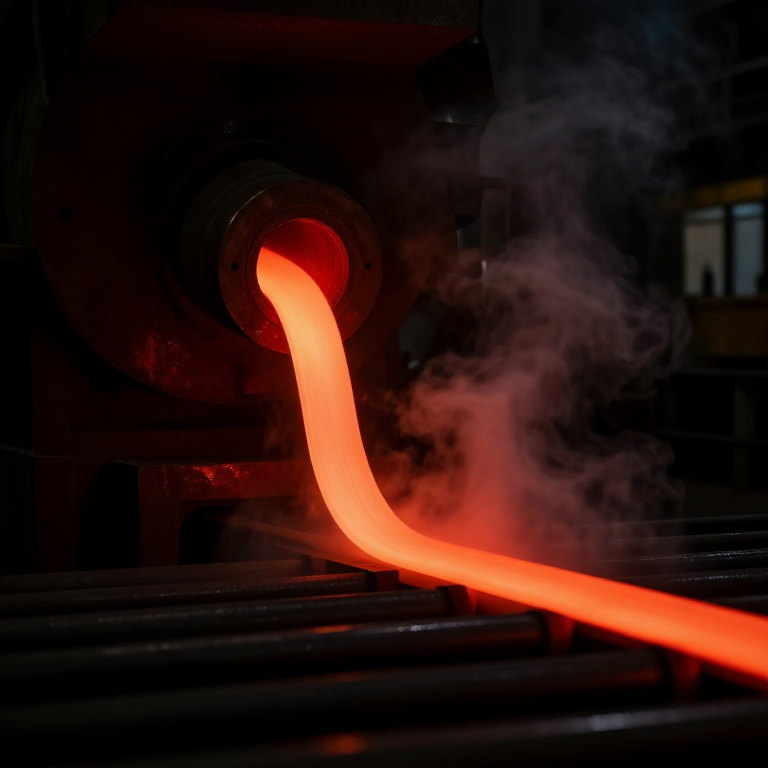
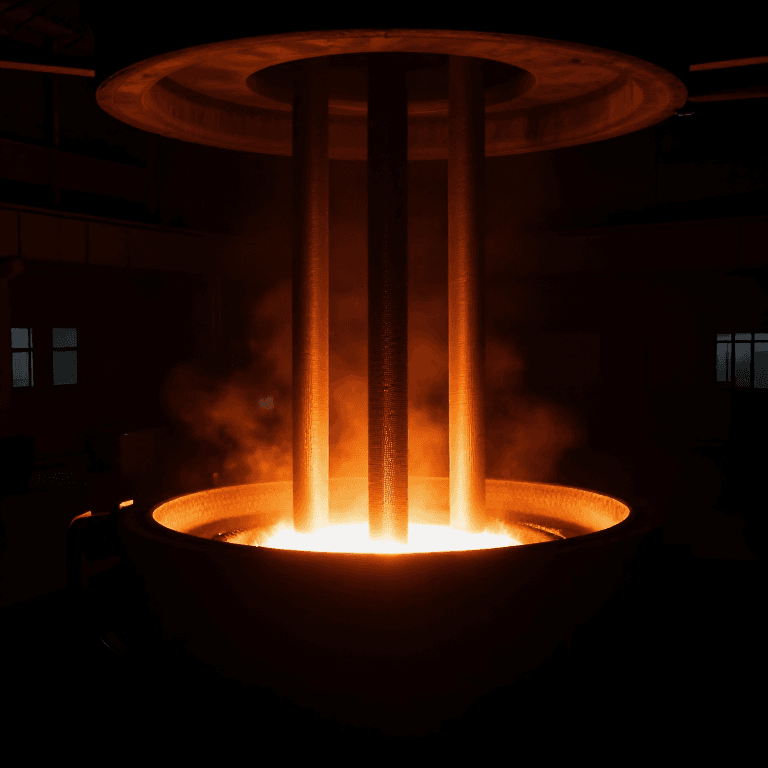
The mould is short on purpose. Its only job is to freeze a shell strong enough to contain the liquid core — not to solidify the whole section. The strand leaves the mould with a solid skin and a molten centre, and finishes freezing in the spray chamber below. Understanding that the mould makes a SHELL, not a casting, is the key to the whole process.
The taper matters: steel shrinks as it freezes and would otherwise pull away from the mould wall, losing heat transfer exactly where it is needed, or jam against a parallel wall. A degree or so of taper keeps contact without binding.이 단계의 재료:
 구리 환봉1 개
 알루미늄 판1 개
 평와셔8 개
 육각 너트4 개
필요한 도구:
 쇠톱 프레임과 톱날
 무선 드릴
 드릴 비트 세트
 줄 세트
 바이스(만력)
 디지털 캘리퍼스 6인치
Add the oscillation — Junghans' contribution
Add the oscillation — Junghans' contribution
The mould must move up and down, and this is the invention.
- Mount the mould on vertical slides so it can travel 5 to 10 mm.
- Drive it from an eccentric on a shaft, giving smooth reciprocation at a few cycles per second.
- Arrange the motion so that on the DOWN stroke the mould briefly moves faster than the strand is being withdrawn.
- Fix the drive with M6 × 40 hex bolts × 4, M6 flat washers × 8 and M6 hex nuts × 4.
Why oscillation solves the fundamental problem. A freezing shell sticks to a stationary mould wall, and a stuck shell tears as it is pulled — the shell ruptures and liquid steel escapes, which is called a breakout and is the catastrophic failure of this process. Moving the mould downward faster than the strand for part of each cycle pushes the shell back into compression and breaks the adhesion before it can grip. That period is called negative strip, and it is what made continuous casting industrially possible.
This is a beautiful example of solving a sticking problem with motion rather than with lubricant or coating — though casting powder is used as well, and does the lubricating job.이 단계의 재료:
 알루미늄 평각봉1 개
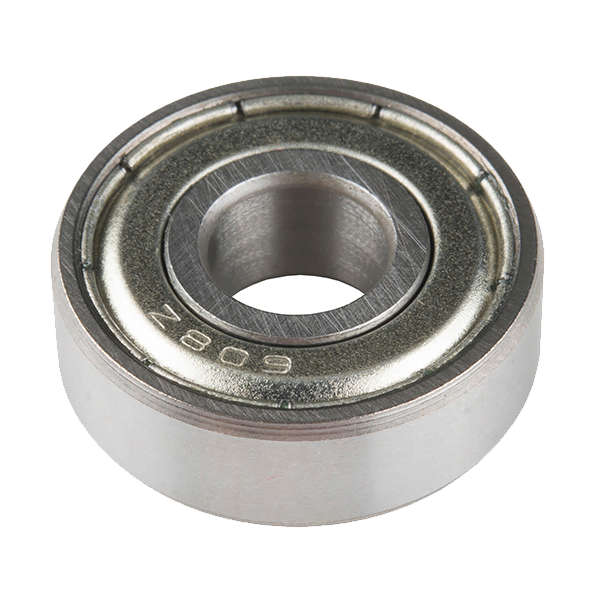 Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)2 개평와셔8 개육각 너트4 개
필요한 도구:
무선 드릴드릴 비트 세트 육각 렌치 세트줄 세트디지털 캘리퍼스 6인치
 조합 직각자
Build the withdrawal rolls and dummy bar
Build the withdrawal rolls and dummy bar
Something must pull the strand down at a controlled rate, and something must start it.
- Fit two driven rolls below the mould, gripping the strand between them.
- Gear them to a hand crank or a slow motor with a measurable speed.
- Make a dummy bar — a stub that plugs the mould's bottom at the start and is gripped by the rolls.
- Give the dummy bar's head a shape the first metal will freeze onto and grip.
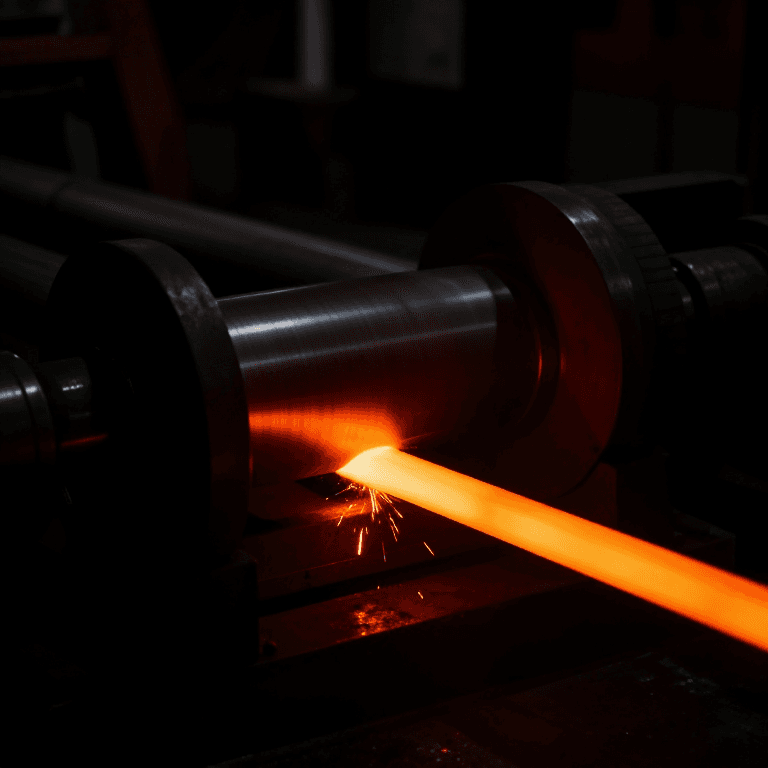
The dummy bar solves the starting problem. A bottomless mould has nothing to hold the first metal, so before pouring you plug it from below. The first steel freezes onto the dummy bar head, the rolls pull it down, and once a strand is established the dummy bar is disconnected and the process runs continuously. Every start-up on every caster in the world begins this way.
Withdrawal rate must match the rate at which a strong enough shell forms. Pull too fast and the shell is thin and bursts below the mould; too slow and the strand freezes solid in the mould and jams.이 단계의 재료:
 알루미늄 환봉1 개Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)4 개
 발트 자작나무 합판1 장평와셔8 개육각 너트4 개
필요한 도구:
무선 드릴드릴 비트 세트 직소육각 렌치 세트줄 세트디지털 캘리퍼스 6인치
Cast a strand and account for the metal saved
Cast a strand and account for the metal saved
The economic case is arithmetic, and it is worth doing.
- Melt a low-temperature alloy and cast a continuous strand, withdrawing steadily.
- Section the strand and look for the shrinkage cavity along its axis.
- Now cast an ingot of the same alloy in a closed mould and section that.
- Measure the shrinkage pipe at the ingot's top and estimate what fraction must be cropped.
- Compare the yield of usable metal from each route.
이 단계의 재료:
 납 잉곳1 ingot
 흑연 점토 도가니1 개
필요한 도구:
 도가니 집게쇠톱 프레임과 톱날디지털 캘리퍼스 6인치
 스톱워치
Abolishing the batch, and history
Abolishing the batch, and history
Henry Bessemer proposed casting steel continuously between rolls in 1857, long before it could be made to work. The obstacles were the sticking shell and the difficulty of controlling solidification, and they took most of a century to solve. Siegfried Junghans developed the oscillating mould in the 1930s, first for non-ferrous metals, and continuous casting of steel spread through the 1950s and 60s until it became near-universal.
The pattern is batch to continuous, and it is one of the great themes of industrial history. Puddling was a batch process and the open hearth was too; the Bessemer converter was a fast batch; continuous casting is the point where steelmaking's output stops being a series of objects and becomes a flow. The same transition happened in glass with the float process, in paper with the Fourdrinier machine already in this catalogue, and in chemicals with continuous reactors. Continuous processes are steadier, more uniform and more efficient — and far less forgiving, because there is no pause between units in which to correct anything.
How it closes this batch. The chain opened in 1783 with Cort's rolling mill, which needed a heated bloom to work on. Every process since has been about getting metal into a useful shape. Continuous casting feeds that same rolling mill directly, hot, in a strand of the right section — eliminating the ingot that every intermediate step existed to handle. The end of the chain connects straight back to its beginning.
Its honest limits: only simple sections — slabs, blooms and billets — since complex shapes still come from rolling or forging afterwards; a breakout is a serious and expensive failure; and the capital cost only makes sense at large scale. It is a process for making a great deal of one thing, which is exactly what modern steelmaking is.
재료
10- 1 개플레이스홀더
- 1 개플레이스홀더
- 8 개플레이스홀더
- 4 개플레이스홀더
- 1 개플레이스홀더
- ₩17
- 1 개플레이스홀더
- 1 장플레이스홀더
- 1 ingot플레이스홀더
- 1 개플레이스홀더
필요 도구
11- 플레이스홀더
- 1 vendor sell this, none ship to you yet플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 1 vendor sell this, none ship to you yet플레이스홀더
- 플레이스홀더
- 플레이스홀더
관련 블루프린트
이 블루프린트들은 지식을 공유합니다 — 기술, 재료 또는 원리

CC0 퍼블릭 도메인
이 블루프린트는 CC0로 공개되었습니다. 어떤 목적으로든 자유롭게 복사, 수정, 배포 및 사용할 수 있습니다.
제품 구매를 통해 메이커를 지원하세요. 판매자가 설정한 메이커 커미션 을 받거나, 이 블루프린트의 새로운 반복을 만들어 연결로 포함시킬 수 있습니다.