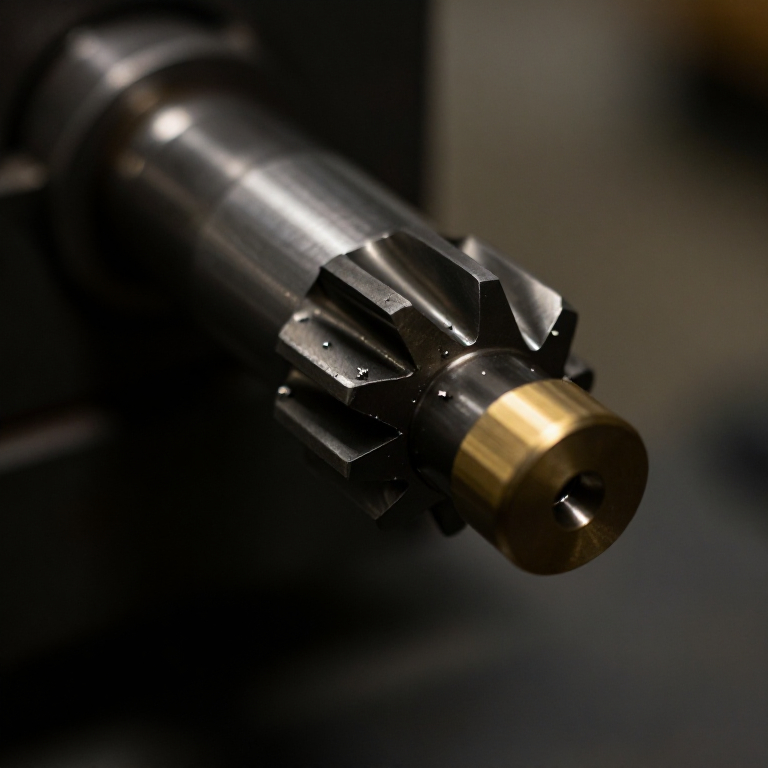

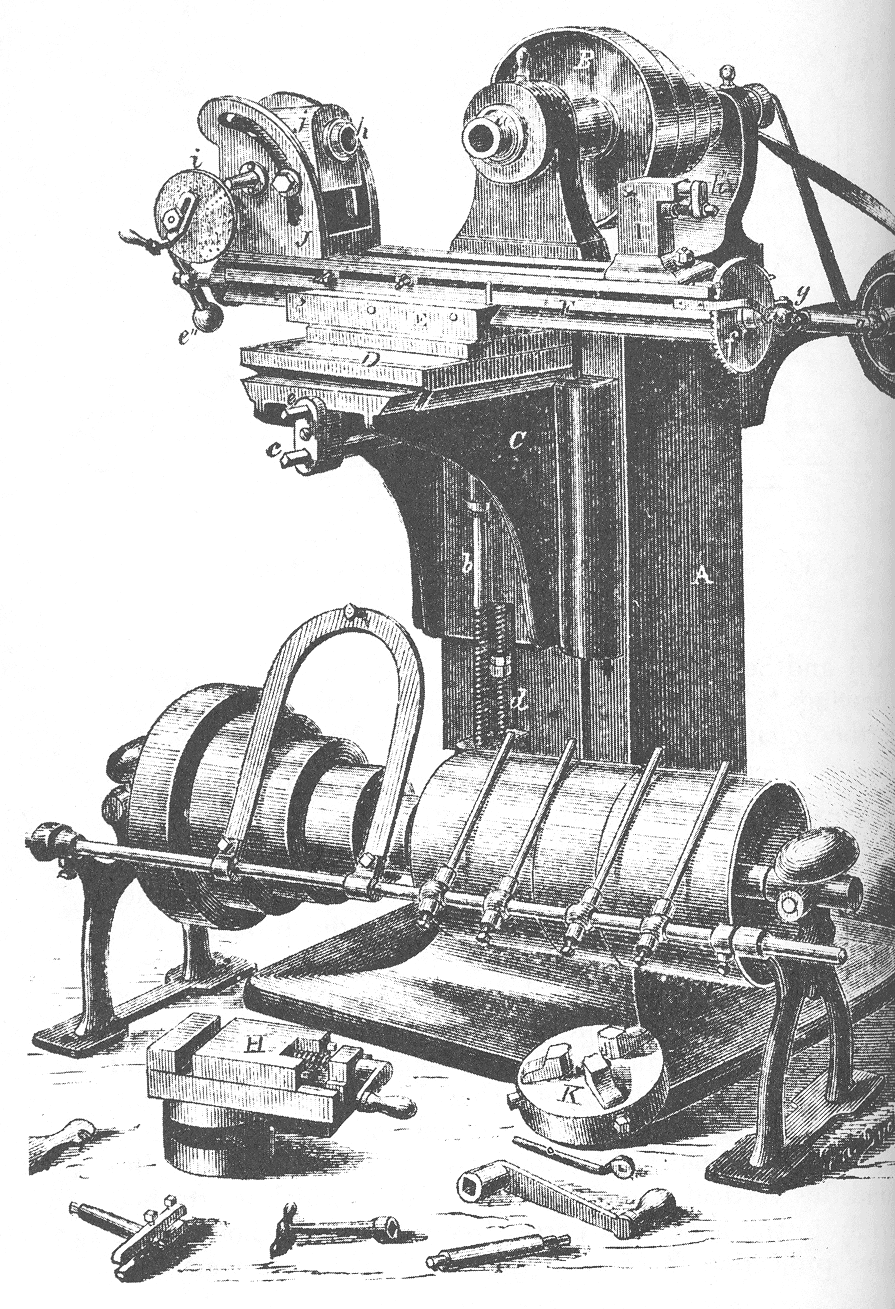
Gear Hobbing Machine
안내
Understand generation before building anything
Understand generation before building anything
Prove to yourself that a curved tooth can be made by straight cuts.
- Cut a card disc as a gear blank and mark its centre.
- Cut a card strip with straight-sided rack teeth — this represents the hob.
- Roll the rack along the disc's edge without slipping, marking the rack's outline on the disc at each small step.
- Look at the envelope of all those straight lines.
The curve appears without anyone drawing it. The involute tooth form is the envelope of a straight-sided rack rolled against the blank, which is why a hob with straight-sided teeth can cut a correctly curved gear. This is generation rather than copying, and it is why one hob serves every tooth count of its module: the form comes from the ROLLING RELATIONSHIP, not from the cutter's shape.
Do this exercise in card before cutting metal. Most of the difficulty in understanding hobbing dissolves once the envelope appears on the disc in front of you.이 단계의 재료:
 색상 카드지 모음1 팩
 모눈종이1 pad
필요한 도구:
 디지털 캘리퍼스 6인치
 조합 직각자
 실톱(코핑 소)
Make a single-start hob
Make a single-start hob
A worm with flutes cut across it, so each thread crest becomes a row of teeth.
- Start from a length of M12 threaded rod — a ready-made single-start worm of known pitch.
- Cut three or four straight flutes along its length with a hacksaw, at 90 degrees to each other.
- File a relief behind each cutting edge so only the edge contacts.
- Mount it on an arbor in two 608 bearings.
Modern build spec (derived). A real hob is a hardened, precisely relieved and ground cutter with a defined pressure angle. Threaded rod flutted by hand will cut soft material and demonstrate the geometry exactly, at a fraction of the work. What it will not do is hold form after a few cuts.
The flutes must be straight and evenly spaced, because each becomes a cutting row. Uneven flutes mean some rows cut more than others, which shows up as a periodic error around the finished gear.이 단계의 재료:
 알루미늄 환봉1 개
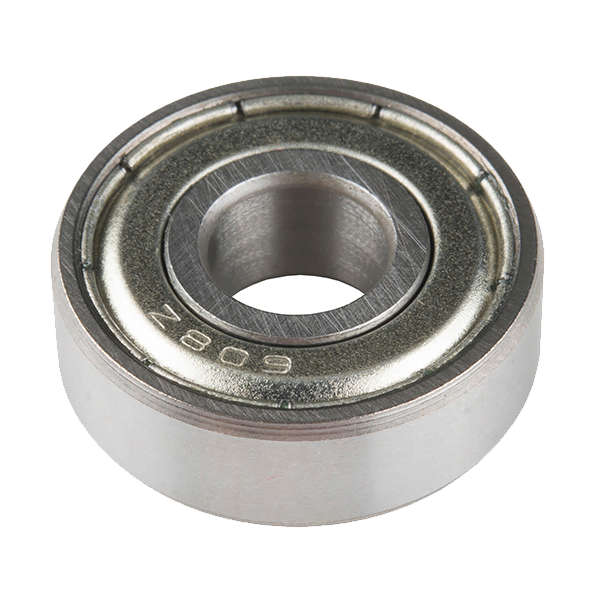 Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)2 개
 컵 포인트 멈춤 나사2 개
필요한 도구:
 쇠톱 프레임과 톱날
 바이스(만력)
 줄 세트
 무선 드릴
 드릴 비트 세트디지털 캘리퍼스 6인치
Gear the hob to the blank in a fixed ratio
Gear the hob to the blank in a fixed ratio
This is the machine. Everything else is a frame to hold it.
- Mount the blank on a vertical spindle in 608 bearings.
- Connect the hob spindle to the blank spindle through a train of change gears.
- For a single-start hob cutting N teeth, the blank must turn once for every N turns of the hob.
- Fit the change gears to give that ratio and check it by counting turns by hand.
- Secure everything with M6 × 50 hex bolts × 4, M6 flat washers × 8 and M6 hex nuts × 4.
The ratio is the tooth count. Change the gearing to 1:37 and you cut a 37-tooth gear with the same hob; 1:38 gives 38 teeth. Nothing about the cutter changes. That is the whole economic argument for hobbing — one cutter, every tooth count, and prime numbers are no harder than round ones.
Count the turns by hand before cutting. A gearing error produces a gear with the wrong tooth count and a mangled last tooth, and it is not visible until the cut is nearly finished.이 단계의 재료:
 발트 자작나무 합판1 장Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)2 개
 평와셔8 개
 육각 너트4 개
 알루미늄 평각봉1 개
필요한 도구:
무선 드릴드릴 비트 세트 육각 렌치 세트
 직소조합 직각자디지털 캘리퍼스 6인치
Set the hob's lead angle and cut a gear
Set the hob's lead angle and cut a gear
The hob must be tilted, or its teeth cut at an angle to the gear's axis.
- Measure the hob's lead angle — the helix angle of its thread.
- Swivel the hob head by that angle so its teeth run parallel to the gear's tooth direction.
- Feed the hob into the blank to full tooth depth.
- Feed it slowly along the blank's axis while both rotate, and let the teeth generate.
- Inspect the finished teeth for the characteristic faceted flanks.
이 단계의 재료:
알루미늄 평각봉1 개필요한 도구:
조합 직각자디지털 캘리퍼스 6인치육각 렌치 세트줄 세트Generation versus forming, and history
Generation versus forming, and history
Hermann Pfauter patented a universal gear hobbing machine in 1897 in Chemnitz, and the firm he founded still makes hobbing machines. The same year, Edwin Fellows patented the gear shaper already in this catalogue — two different generating machines arriving simultaneously, which is a good indication that gear cutting was the bottleneck everyone was pushing at.
Generating versus forming, stated plainly. A form cutter is shaped like the space between two teeth, so it copies its own profile and is strictly correct for only one tooth count — which is why form cutters are sold in numbered sets, each covering a range approximately. A generating process rolls a simple cutter against the blank and lets the correct curve emerge from the motion. Generation gives better accuracy from simpler tooling, at the cost of a machine that must hold an exact ratio between two rotations.
What it inherited from this chain: the milling machine's rigid three-axis frame, the dividing head's principle of exact angular relation — here made continuous rather than stepped — and the change-gear train that Maudslay's screw-cutting lathe introduced for connecting rotation to rotation. Hobbing is those three ideas combined and pointed at one job.
Where each still wins: hobbing for spur, helical and worm gears in quantity; shaping for internal gears and for gears with a shoulder close by, where a hob cannot run out; form milling for one-off repairs where setting up a hobber is not worth it. Three approaches to one goal, all still in use — and the choice is about quantity and geometry, not about which is better.
재료
9- 1 팩플레이스홀더
- 1 pad플레이스홀더
- 1 개플레이스홀더
- ₩17
- 2 개플레이스홀더
- 1 장플레이스홀더
- 8 개플레이스홀더
- 4 개플레이스홀더
- 1 개플레이스홀더
필요 도구
10- 플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 1 vendor sell this, none ship to you yet플레이스홀더
- 플레이스홀더
- 플레이스홀더
- 1 vendor sell this, none ship to you yet플레이스홀더
관련 블루프린트
이 블루프린트들은 지식을 공유합니다 — 기술, 재료 또는 원리
CC0 퍼블릭 도메인
이 블루프린트는 CC0로 공개되었습니다. 어떤 목적으로든 자유롭게 복사, 수정, 배포 및 사용할 수 있습니다.
제품 구매를 통해 메이커를 지원하세요. 판매자가 설정한 메이커 커미션 을 받거나, 이 블루프린트의 새로운 반복을 만들어 연결로 포함시킬 수 있습니다.