예술
뷰티 및 웰니스
공예
문화 및 역사
엔터테인먼트
환경
음식 및 음료
역공학
과학
스포츠
기술
웨어러블
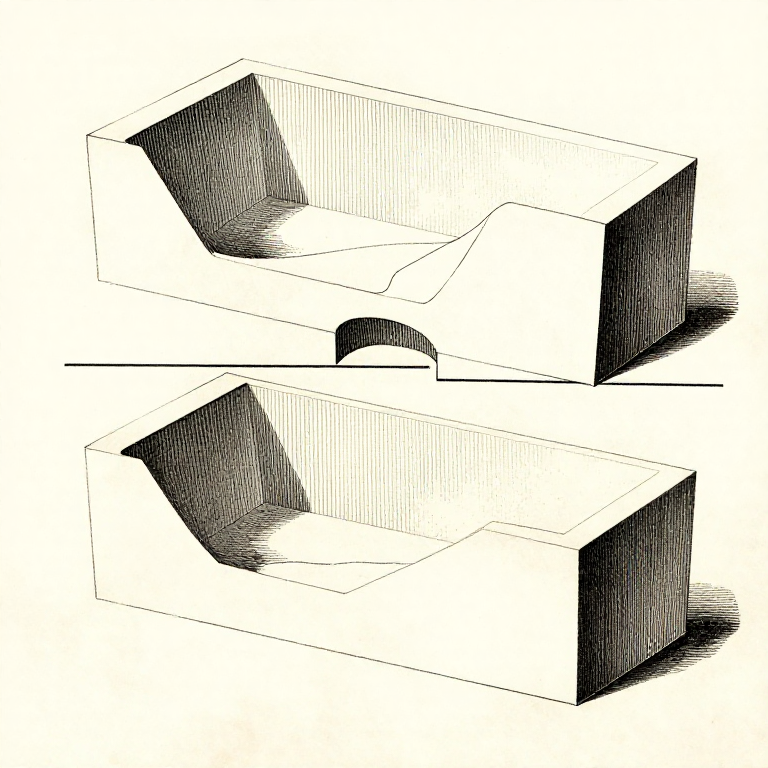

The Parting Line: Where the Mould Splits Decides Everything Else
A two-part mould has to come apart, so the pattern has to be able to leave both halves. Choosing where the split runs is the first real design decision in casting, and it constrains every decision after it.
Draft is measured FROM the parting line, so moving it changes which surfaces are tapered and in which direction. The gating usually enters at it. And the split always leaves a visible flash line on the finished part, so it also decides where the casting looks worst.
The rule that solves most cases: put the parting line at the LARGEST cross-section, so that both halves of the pattern taper away from it and neither has an undercut.
고급
3 hours
안내
1
1
Find the largest section and split there
Find the largest section and split there
Imagine drawing the pattern upward out of the drag and downward out of the cope. Any surface that overhangs — any UNDERCUT — makes that impossible, and the parting line must be placed so there are none.
At the widest cross-section, everything above tapers up and everything below tapers down, which is exactly the condition for a clean draw. That is why a sphere is parted at its equator and a cone at its base.
Where one parting line cannot avoid every undercut, the answers are a CORE, a loose piece in the pattern that stays behind and is removed separately, or a three-part mould. All three cost time, which is why the geometry is worth rearranging first.
이 단계의 재료:
 경목 판재1 개
필요한 도구:
 디지털 캘리퍼스 6인치
 자
2
2
Cores make internal shapes, and they have to be held and vented
Cores make internal shapes, and they have to be held and vented
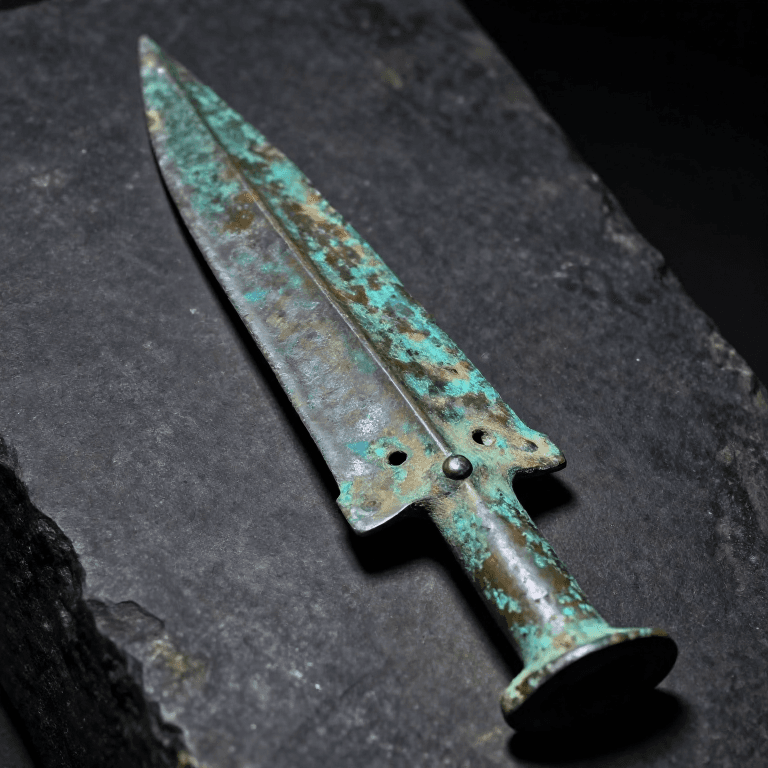
A CORE is a separate piece of bonded sand placed in the mould to make a hole or a hollow. The socket of a bronze spearhead, the inside of a kettle and the bore of a pipe are all cores.
It has to be LOCATED, by core prints — extensions on the pattern that leave sockets for the core's ends to sit in. A core that floats on molten metal moves, and a moved core gives a wall thick on one side and thin on the other.
It also has to VENT and to COLLAPSE. Gas generated inside a core has only one way out, through the core prints; and a core too strong to break down afterwards cannot be got out of the casting, which is why core binders are designed to lose strength at temperature.
이 단계의 재료:
 주물사1 kg
 벤토나이트 점토1 kg
필요한 도구:
 주형틀(상형과 하형)디지털 캘리퍼스 6인치
 확대 루페
3
3
Put the important surfaces in the drag
Put the important surfaces in the drag
Slag, dross and any sand washed loose float upward and collect at the top of the casting — which is the cope. So the surfaces that matter go in the DRAG, the lower half, where the metal is cleanest.
Thick sections also want to be high, because the feeding has to come from above: metal contracting as it freezes is fed by gravity from the riser, and a thick section at the bottom cannot be fed by one at the top.
Those two rules sometimes conflict, and then the decision is which matters more — a sound thick section or a clean visible surface. Recognising that it IS a conflict, rather than looking for a layout that satisfies both, is the useful step.
이 단계의 재료:
주물사1 kg필요한 도구:
주형틀(상형과 하형)자4
4
The flash line is permanent, so put it where it belongs
The flash line is permanent, so put it where it belongs
A thin fin of metal always forms where the two mould halves meet, however well they are clamped. It is ground off in fettling and it leaves a line that never quite disappears.
So put the parting line on an edge, a corner, or a face that will be machined — somewhere the line is expected — rather than across a visible curved surface where it will be obvious for ever.
And align the halves positively. Pins and sockets on the flask, or a moulded register, stop the cope shifting sideways relative to the drag. A shifted mould gives a casting with a visible step all the way round, and that one is not recoverable by fettling.
이 단계의 재료:
주물사1 kg필요한 도구:
주형틀(상형과 하형) 줄 세트디지털 캘리퍼스 6인치
관련 블루프린트
이 블루프린트들은 지식을 공유합니다 — 기술, 재료 또는 원리
CC0 퍼블릭 도메인
이 블루프린트는 CC0로 공개되었습니다. 어떤 목적으로든 자유롭게 복사, 수정, 배포 및 사용할 수 있습니다.
제품 구매를 통해 메이커를 지원하세요. 판매자가 설정한 메이커 커미션 을 받거나, 이 블루프린트의 새로운 반복을 만들어 연결로 포함시킬 수 있습니다.