සහයෝගීතාව
කලාව
රූපලාවණ්ය සහ සුවතාව
ශිල්පය
සංස්කෘතිය සහ ඉතිහාසය
විනෝදාස්වාදය
පරිසරය
ආහාර සහ පාන
ප්රතිලෝම ඉංජිනේරු
විද්යාවන්
ක්රීඩා
තාක්ෂණය
පැළඳිය හැකි
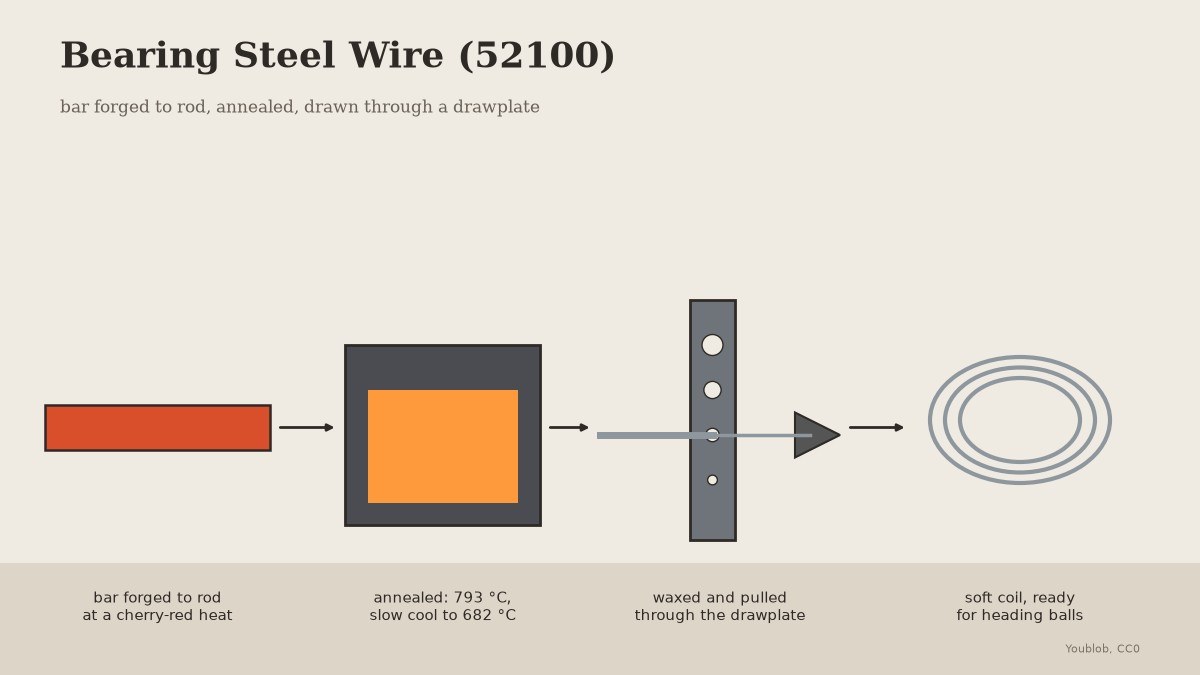


Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
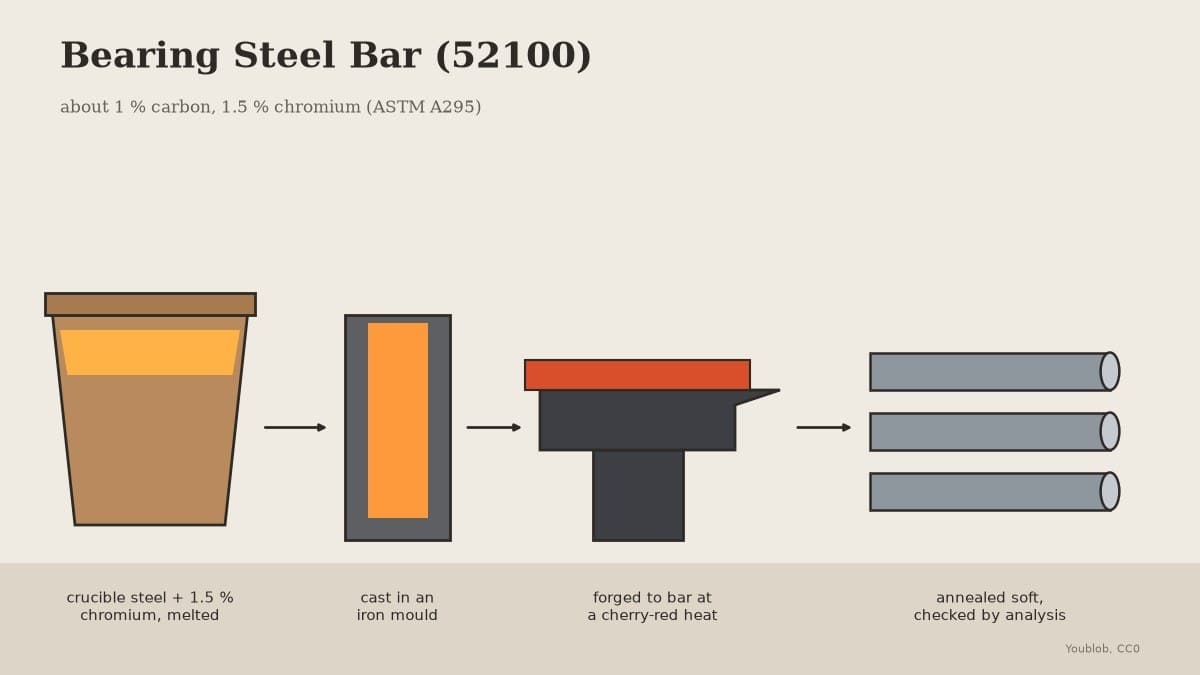
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
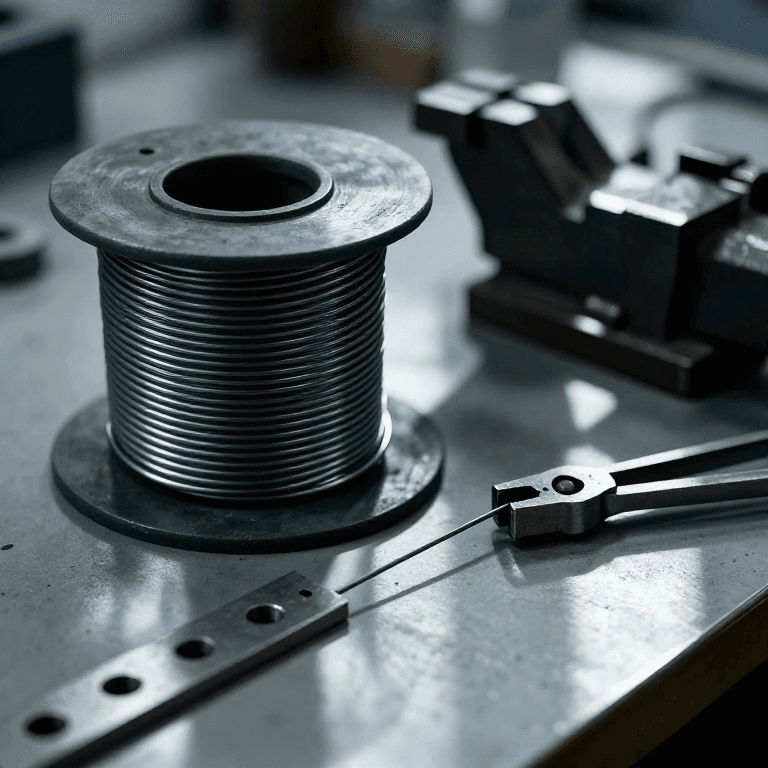
The picture: our drawing, bar to coil.
උසස්
2 days
උපදෙස්
1
1
Forge to rod
Forge to rod
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
මෙම පියවර සඳහා ද්රව්ය:
 බෙයාරිං වානේ දණ්ඩ (52100)1 කිග්රෑ
 අඟුරු1 as required
අවශ්ය මෙවලම්:
 කම්මල් උදුන
 නියන (ඇන්විලය)
 හරස් කුඤ්ඤ හිසක් සහිත මිටිය
 කම්මල්කරුගේ අඬුව
 වෑල්ඩින් අත්වැසුම්
 ආරක්ෂිත කණ්ණාඩි
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
අවශ්ය මෙවලම්:
 තාප පිරියම් උදුන
 කියවීමක් සහිත තාපයුග්මයකම්මල්කරුගේ අඬුවවෑල්ඩින් අත්වැසුම්
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
අවශ්ය මෙවලම්:
 කම්බි බුරුසු කට්ටලය
 කටු කට්ටලය
 බංකු තද කරන්නා
4
4
Wax and draw
Wax and draw
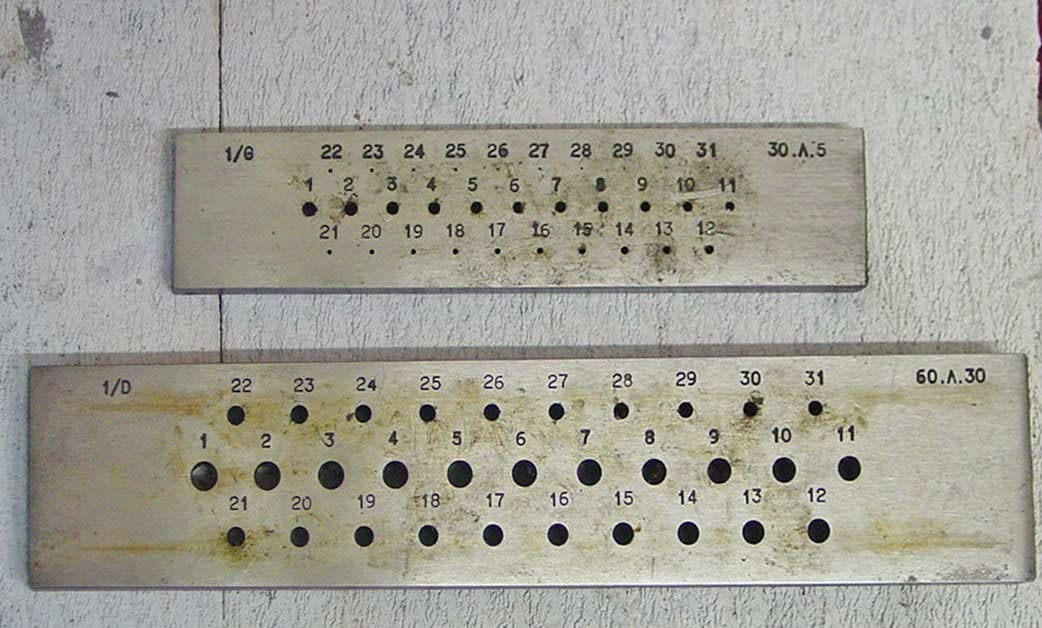
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
මෙම පියවර සඳහා ද්රව්ය:
 මී ඉටි20 ග්රෑ
අවශ්ය මෙවලම්:
 වානේ කම්බි ඇදීමේ තැටිය
 ඇදීමේ අඬුබංකු තද කරන්නා
 සම් වැඩ අත්වැසුම්
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
මෙම පියවර සඳහා ද්රව්ය:
මී ඉටි1 කැබැල්ලඅවශ්ය මෙවලම්:
වානේ කම්බි ඇදීමේ තැටියඇදීමේ අඬුතාප පිරියම් උදුනකියවීමක් සහිත තාපයුග්මය6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
අවශ්ය මෙවලම්:
 ඩිජිටල් කැලිපරය අඟල් 6තාප පිරියම් උදුනකියවීමක් සහිත තාපයුග්මය
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
ද්රව්ය
3- 1 කිග්රෑස්ථානගත
- 1 as requiredස්ථානගත
- 1 කැබැල්ලස්ථානගත
අවශ්ය මෙවලම්
15- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
- ස්ථානගත
මෙම සැලසුම සාදන්නේ
සම්බන්ධ බ්ලූප්රින්ට්
මෙම බ්ලූප්රින්ට් දැනුම බෙදා ගනී — ශිල්ප ක්රම, ද්රව්ය හෝ මූලධර්ම
CC0 පොදු වසම
මෙම බ්ලූප්රින්ට් CC0 යටතේ නිකුත් කර ඇත. ඔබට අවසර නොමැතිව පිටපත් කිරීම, වෙනස් කිරීම, බෙදා හැරීම සහ භාවිතා කිරීම කළ හැක.
බ්ලූප්රින්ට් හරහා නිෂ්පාදන මිලදී ගැනීමෙන් නිර්මාතෘට සහාය වන්න නිර්මාතෘ කොමිසම විකුණුම්කරුවන් විසින් නියම කළ, හෝ මෙම බ්ලූප්රින්ට්හි නව අනුවාදයක් සාදා ආදායම බෙදා ගැනීමට ඔබේ බ්ලූප්රින්ට්හි සම්බන්ධතාවයක් ලෙස ඇතුළත් කරන්න.