Хамтын ажиллагаа
УРЛАГ
ГОО САЙХАН БА ЭРҮҮЛ МЭНД
ГАРААР ХИЙСЭН
СОЁЛ БА ТҮҮХ
ҮЗВЭР НААДАМ
БАЙГАЛЬ ОРЧИН
ХООЛ БА УНДАА
УРВУУ ИНЖЕНЕРЧЛЭЛ
ШИНЖЛЭХ УХААН
СПОРТ
ТЕХНОЛОГИ
ӨМСДӨГ ХЭРЭГСЭЛ
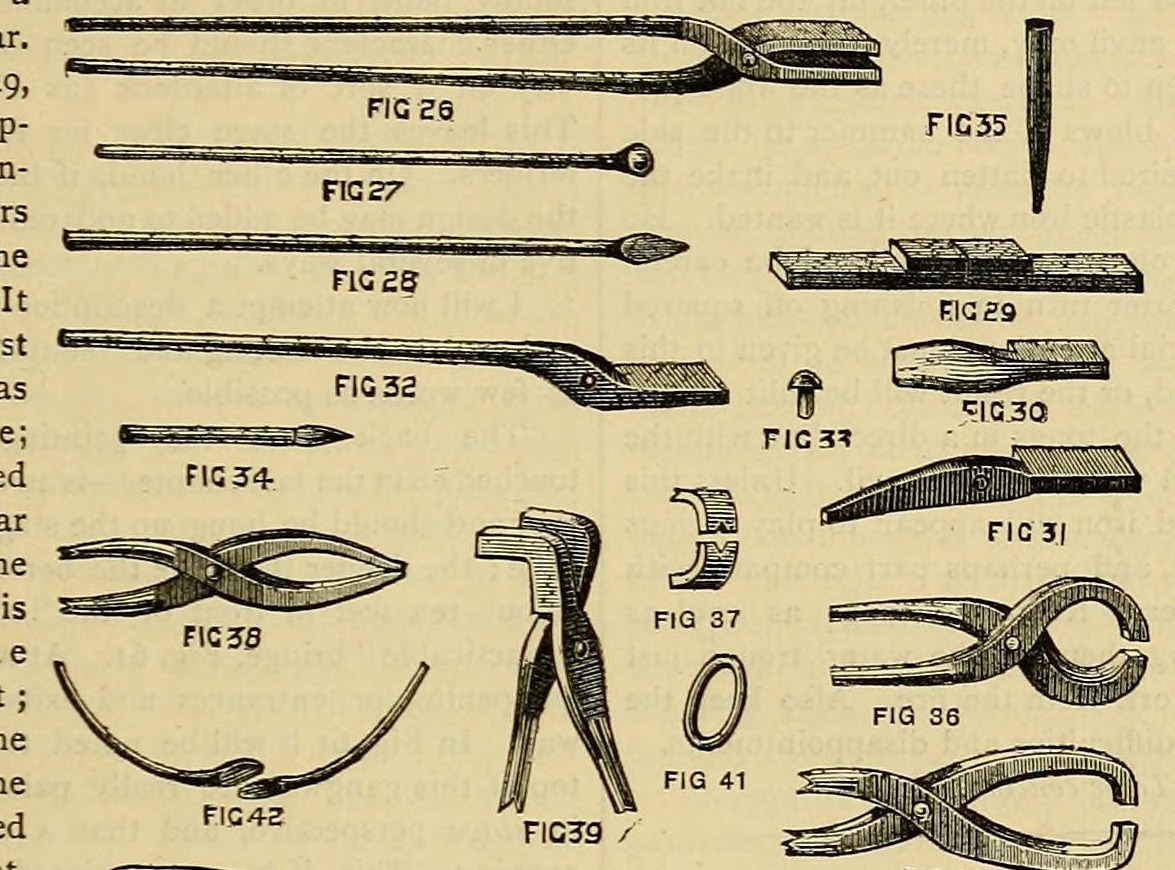


Flat-Bit Tongs and the Tongs Made from Them, down to Crucible Tongs: Welded Reins, Riveted Joint (Edwinson, 1886)
George Edwinson's tong-making lesson from Amateur Work (1886): jaws forged from inch-square iron, reins of 5/8 in. rod scarfed and welded on, the halves riveted with a hot iron pin. The same flat-bit tongs are then reshaped into pincer, hammer and crook-bit tongs, light smith's pliers, and thinned and curved into crucible tongs.
Дээд шат
A day at the forge
Зааварчилгаа
1
1
His sizes
His sizes
Jupyter дэвтэр ачаалж байна…
2
2
Read Edwinson
Read Edwinson
"Indeed, the man who can turn out a good pair of tongs may be trusted with almost any job in the smithy."
3
3
Forge the reins
Forge the reins
Cut two pieces of 5/8 in. (16 mm) iron rod, each 2 ft (0.6 m) long, with a cold chisel. Bring one end of each to a white welding heat and draw 3-4 in. down to a taper from 5/8 to 1/2 in., rounded for the hand. Upset the other ends at a white heat and scarf them (his figs. 27-28).
Энэ алхмын материал:
 Давтсан төмөр гулдмай1 ширхэг
Шаардлагатай багаж:
 Хүйтэн цүүц
 Дархны зуух
 Дөш
 Алх
 Дархны хавчаар
4
4
Forge the jaws
Forge the jaws
Cut two 6 in. pieces of 1 in. square iron (or one 12 in. bar, worked from each end before cutting, fig. 29). Forge each jaw end 4 in. long, 1 1/4 in. wide and 3/8 in. thick. Flatten the other end to 1/4 in. thick, round it for the joint (fig. 30) and draw it to a slightly rounded taper (fig. 31).
Энэ алхмын материал:
 Зөөлөн ган дөрвөлжин саваа1 ширхэг
Шаардлагатай багаж:
Дархны зуухДөшАлхДархны хавчаар5
5
Punch the joint
Punch the joint
Mark the hole with a centre punch, heat, and punch a 3/8 in. hole over the anvil's heel hole with an iron punch tapering 1/4 to 1/2 in. (fig. 35), or a steel punch of 5/8 in. tool steel.
Энэ алхмын материал:
 Багажийн ган саваа1 ширхэг
Шаардлагатай багаж:
 Төвлүүлэх цүүцДархны зуухДөшАлх
6
6
Weld jaw to rein
Weld jaw to rein
Scarf the taper end of each jaw to fit a rein. Heat both to a welding heat in a clear fire, throw on clean fine fresh-water sand and heat until pasty. Tap the scarfs together lightly, return to the fire a moment, and finish the weld. At a red heat forge the square part to blend into the round rein (fig. 32).
Энэ алхмын материал:
 Элс1 ширхэг
Шаардлагатай багаж:
Дархны зуухДөшАлхДархны хавчаар7
7
Rivet the joint
Rivet the joint
Smiths' way: nick a 3/8 in. round iron rod to rivet length, put the halves together, insert the hot end, twist it off, let 1/4 in. stand below, and rivet both sides. (Or make a 3/4 x 3/8 in. button-headed rivet in a 3/8 in. hole in a flat iron.) If the joint locks, reheat jaws and pin to bright red and work them free.
Энэ алхмын материал:
Давтсан төмөр гулдмай1 ширхэгШаардлагатай багаж:
Дархны зуухДөшАлх Хадаасны толгой хийх хавтан
8
8
Set the jaws
Set the jaws
Heat the jaws and set them to the width of the stock to be held. Spring them wider with a piece of cold iron between and a few light blows.
Шаардлагатай багаж:
Дархны зуухДөшАлх9
9
Crucible tongs and other forms
Crucible tongs and other forms
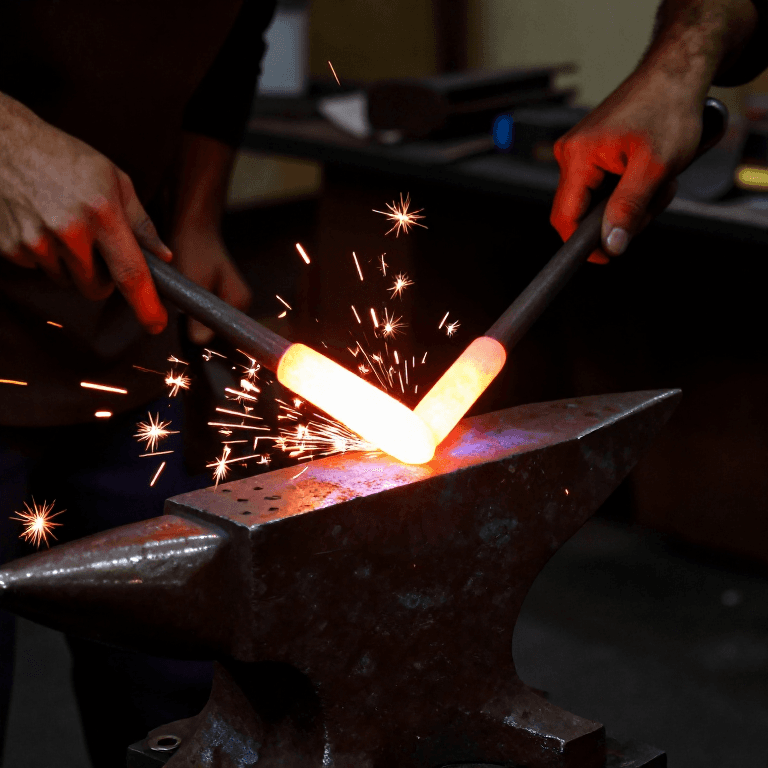
From flat-bit tongs at the fig. 32 stage: lengthen and curve the bits for pincer tongs (angular notches hold round or square bars), more for hammer tongs, bend them sideways for crook-bit tongs. Small flat-bit tongs with lengthened, shaped bits are smith's pliers; thin those out further and curve them like pincers to make crucible tongs for hot crucibles and pots of molten metal. Heavy tongs 2-5 ft long need stouter iron.
Шаардлагатай багаж:
Дархны зуухДөшАлхДархны хавчаар10
10
Troubleshooting
Troubleshooting
Tongs troubleshooting.
Flow
Loading...
11
11
History and honest limits
History and honest limits
From George Edwinson, "Smithing and Forging" III, **Amateur Work, Illustrated**, vol. V (1886), pp. 266-269 (checked on the archive.org scan amateurworkillus05lond). He gives full sizes only for the flat-bit tongs; crucible tong sizes and curvature are left to the work. Metric figures and tools are ours.
Материал
4- 1 ширхэгТүр орлуулагч
- 1 ширхэгТүр орлуулагч
- 1 ширхэгТүр орлуулагч
- 1 ширхэгТүр орлуулагч
Энэ загвараар хийдэг

Холбоотой загварууд
Эдгээр загварууд мэдлэг хуваалцдаг — арга техник, материал эсвэл зарчим
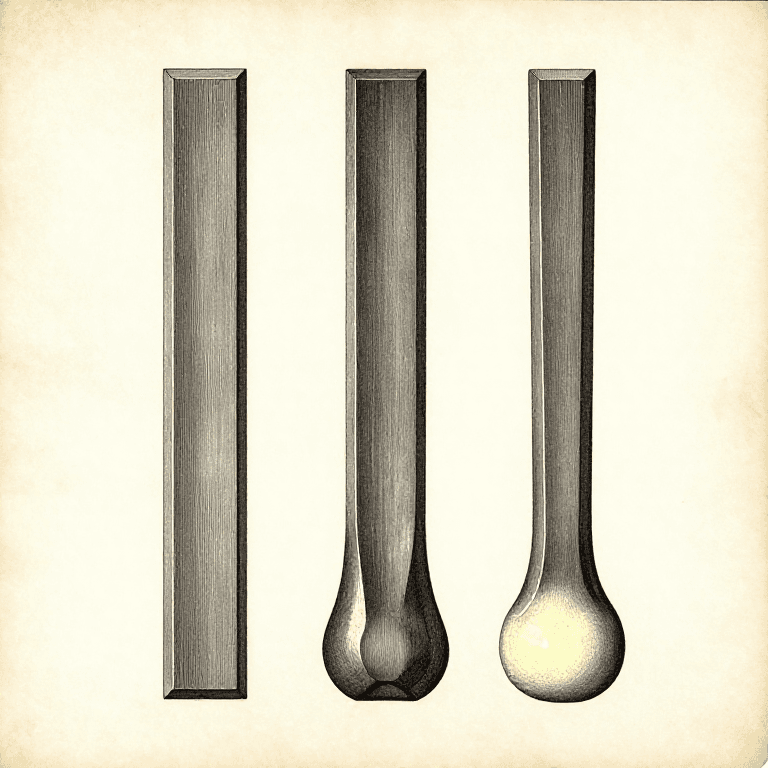
CC0 Нийтийн домэйн
Энэ загвар CC0 дор гаргагдсан. Та зөвшөөрөл авахгүйгээр хуулах, өөрчлөх, түгээх, ашиглах боломжтой.
Загвараар дамжуулан бүтээгдэхүүн худалдаж авч Бүтээгчийг дэмжээрэй Бүтээгчийн шимтгэл Борлуулагчаар тогтоосон, эсвэл энэ загварын шинэ хувилбар үүсгэж орлогоо хуваахын тулд өөрийн загварт холбоос болгон оруулна уу.