
Grooved Rolling Mill
Instrucciones
Make the roll pair and their housing
Make the roll pair and their housing
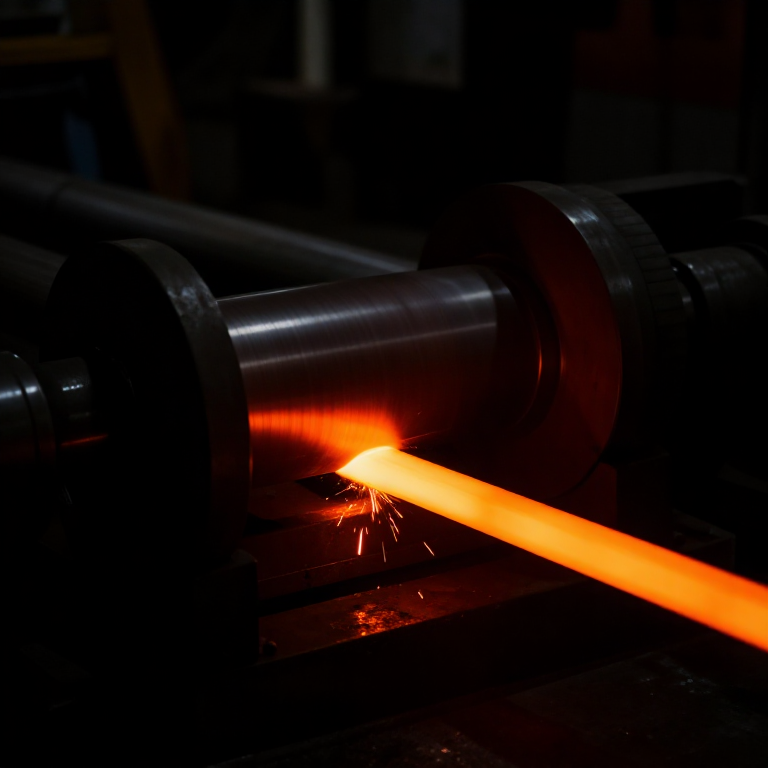
Two rolls, geared together, in a frame stiff enough to resist being pushed apart.
- Turn two rolls 80 mm diameter, 120 mm long, from aluminium round bar.
- Mount each in two 608 bearings in a plywood housing.
- Set the roll axes parallel and in the same vertical plane, checked with the caliper at both ends.
- Fix the housing with M6 × 50 hex bolts × 6, M6 flat washers × 12 and M6 hex nuts × 6.
- Gear the rolls together so they counter-rotate at equal speed.
Roll separating force is the reason mill housings are massive. The work pushes the rolls apart with enormous force, so any flex in the frame lets the gap open and the bar comes out thicker than set — and thicker in the middle than at the ends, because the frame flexes most where the load is. Every rolling mill ever built is mostly frame for this reason.
Equal speed matters. If one roll turns faster than the other it skids on the work, marks the surface and pulls the bar sideways out of the groove.Materiales para este paso:
 Redondo de aluminio2 piezas
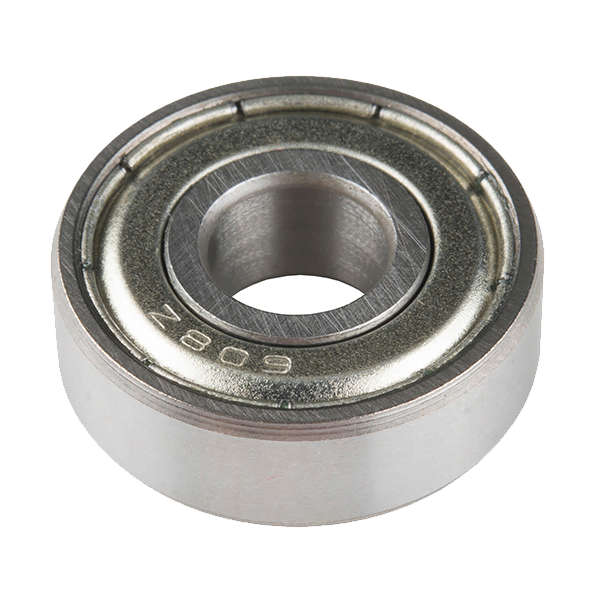 Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)4 piezas
 Contrachapado de abedul báltico1 hoja
 Arandela plana12 piezas
 Tuerca hexagonal6 piezas
Herramientas necesarias:
 Arco de sierra para metales con hojas
 Taladro atornillador sin cable
 Juego de brocas
 Juego de limas
 Juego de llaves Allen
 Calibre digital de 6 pulgadas
Cut a sequence of grooves, not just one
Cut a sequence of grooves, not just one
A pass schedule: each groove takes the bar one step closer to size.
- Cut matching semicircular grooves in both rolls so they form closed apertures when the rolls meet.
- Make a series: 20 mm, 16 mm, 13 mm, 10 mm and 8 mm across the roll faces.
- Align each pair of grooves exactly — a mismatch shows as a fin on the finished bar.
- Round the groove edges slightly so the bar enters without shearing.
Reduction per pass is a real constraint. Take too much in one pass and the rolls simply refuse to bite — the bar skids instead of being drawn in — and the metal cracks at its surface. Take too little and you waste passes and lose heat. Roughly 20 to 30 per cent area reduction per pass is the practical band, which is why the schedule steps down rather than jumping.
Groove alignment is the commonest fault. Offset the two halves by a millimetre and every bar carries a longitudinal fin exactly at the parting line, which must then be removed by hand — losing all the advantage the mill was built for.Herramientas necesarias:
Juego de limas Tornillo de bancoCalibre digital de 6 pulgadas
 Escuadra combinada
 Granete
Add screw-down adjustment
Add screw-down adjustment
The gap must be settable, and it must hold against the separating force.
- Mount the top roll's bearings in vertical slides within the housing.
- Fit two M10 screws bearing down on those slides, one at each end.
- Fit locknuts so a setting holds.
- Set the gap with feeler gauges or shim stock at both ends and confirm they match.
Two screws, set independently, and this is why. If one end of the gap is tighter than the other, the bar is squeezed harder on one side, comes out thicker on the other, and — because the longer side must go somewhere — the bar curves as it leaves. Rolling a banana instead of a bar is nearly always an unequal gap rather than a bad groove.
Set the gap with the mill loaded if you can. Frame flex means the running gap is always larger than the static one, and the difference is exactly the error you will measure in step 4.Materiales para este paso:
 Pletina de aluminio1 piezaArandela plana8 piezasTuerca hexagonal4 piezas
Herramientas necesarias:
Taladro atornillador sin cableJuego de brocasJuego de llaves AllenJuego de limasCalibre digital de 6 pulgadasRoll a bar down the schedule and measure consistency
Roll a bar down the schedule and measure consistency
The claim is uniform section along the whole length. Test it.
- Take an annealed aluminium bar and roll it through the largest groove.
- Measure its section at five points along its length.
- Pass it through each successive groove, rotating it 90 degrees between passes.
- Measure again at five points after the final pass.
- Compare against a bar of the same reduction produced by hammering.
Materiales para este paso:
Redondo de aluminio1 piezaHerramientas necesarias:
Calibre digital de 6 pulgadas CronómetroTornillo de banco
Why it was patented with puddling, and history
Why it was patented with puddling, and history
Henry Cort patented grooved rolls in 1783 and the puddling process in 1784, and the two belong together. Puddling produced wrought iron as a spongy bloom full of slag; that bloom had to be worked to expel the slag and consolidate the metal, and rolling did it in minutes where hammering took hours. Neither invention is as valuable alone: puddling made the iron, rolling made it usable, and together they multiplied British wrought iron output enormously.
This is why chronological order matters for reading the catalogue. Puddling appears earlier here as a smelting process; without the rolling mill it is an interesting furnace. With it, it is the foundation of the railway age — rails, plate, angle and bar all came off grooved rolls, in sections a hammer could never hold consistently.
The deeper shift is from craft to stock. Before rolling, iron came in whatever sections a particular smith made. Afterwards it came in catalogued sections, repeatable between mills, so a structure could be designed on paper from standard parts before any metal was ordered. That is the same transition the Whitworth thread brought to fasteners and gauge blocks brought to measurement — the industrial habit of agreeing on a standard first.
Its honest limits: rolling makes long constant sections and nothing else. It cannot make a shape that varies along its length, cannot make a closed hollow without a mandrel — which is what the Mannesmann process later in this batch solves — and the tooling is a set of rolls that must be re-cut for every new section. High volume of one profile is where it wins, and that has not changed.
Materiales
6- 3 piezasMarcador de posición
- Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)10% de comisión4 piezasMX$21.86
- Marcador de posición
- 20 piezasMarcador de posición
- 10 piezasMarcador de posición
- 1 piezaMarcador de posición
Herramientas requeridas
10- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
Blueprints relacionados
Estos blueprints comparten conocimiento — técnicas, materiales o principios


CC0 Dominio público
Este Blueprint se publica bajo CC0. Eres libre de copiar, modificar, distribuir y usar este trabajo para cualquier propósito, sin pedir permiso.
Apoya al Maker comprando productos a través de su Blueprint, donde gana una Comisión del Maker establecida por los vendedores, o crea una nueva iteración de este Blueprint e inclúyela como conexión en tu propio Blueprint para compartir ingresos.