Kerjasama
SENI
KECANTIKAN & KESEJAHTERAAN
KRAFTANGAN
BUDAYA & SEJARAH
HIBURAN
ALAM SEKITAR
MAKANAN & MINUMAN
KEJURUTERAAN TERBALIK
SAINS
SUKAN
TEKNOLOGI
BOLEH PAKAI
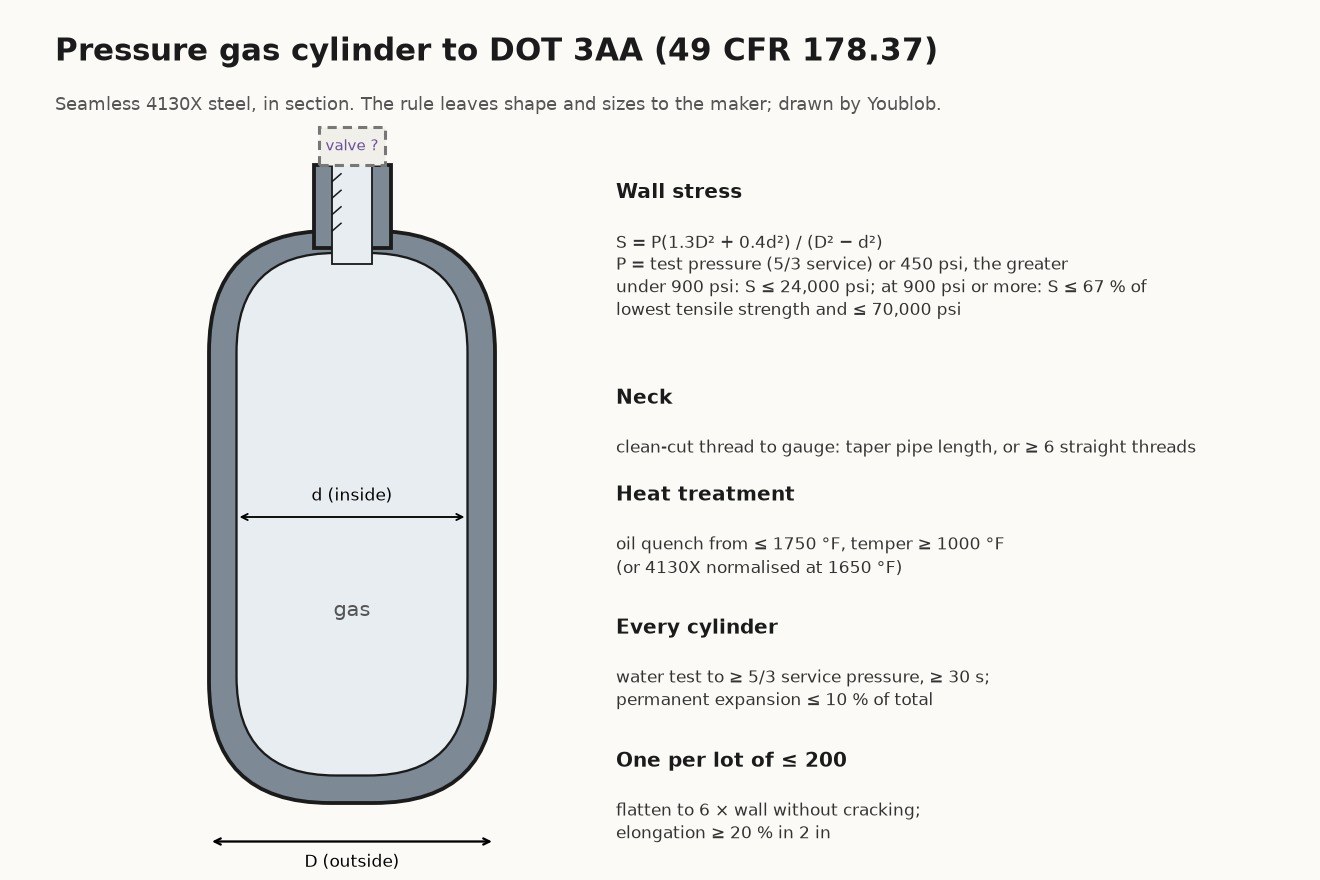


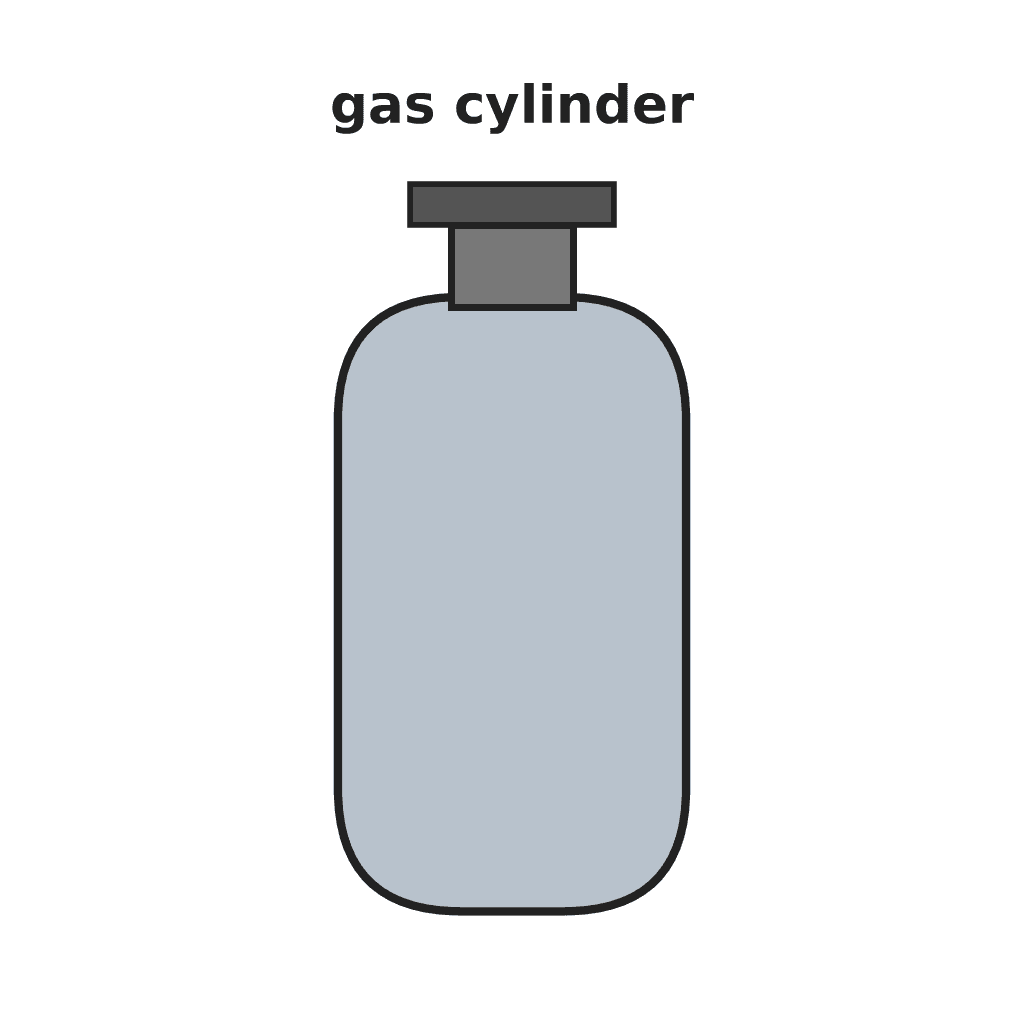
Pressure Gas Cylinder: Seamless 4130X Steel to DOT 3AA (49 CFR 178.37)
A seamless steel cylinder for compressed or liquefied gas, made to the US rule DOT 3AA: at least 150 psi service pressure, up to 1,000 lb of water capacity. The rule gives the steel, a formula for the wall, the heat treatment and the tests every cylinder or lot must pass. It does not say how the shell is formed.
Result: a seamless 4130X steel cylinder, heat-treated and proof-tested to 5/3 of its service pressure, with a threaded neck for its valve.
Source: 49 CFR 178.37, Specification 3AA. Unknown: how the shell is formed, the valve, the test apparatus. Picture drawn by Youblob.
Lanjutan
Unknown
Arahan
1
1
Size the wall
Size the wall
Pick the service pressure (at least 150 psi) and the diameter. Find the wall stress S = P(1.3D² + 0.4d²) / (D² − d²), with D and d the outside and inside diameters in inches and P the test pressure (5/3 of service pressure) or 450 psi, whichever is greater. Below 900 psi service, S may not pass 24,000 psi, and a cylinder over 5 in across needs a wall of at least 0.100 in. At 900 psi or more, S may not pass 67 % of the steel's lowest tensile strength, nor 70,000 psi.
Alatan diperlukan:
 Dimensi tidak diketahui
2
2
Get the steel
Get the steel
Use open-hearth, basic oxygen or electric steel of uniform quality, here 4130X: carbon 0.25-0.35 %, manganese 0.40-0.90 %, silicon 0.15-0.35 %, chromium 0.80-1.10 %, molybdenum 0.15-0.25 %, phosphorus 0.04 % and sulphur 0.05 % at most. For hot-drawn cylinders, mark each billet with its heat number.
Bahan untuk langkah ini:
 Bilet keluli 41301 per cylinder
Alatan diperlukan:
Dimensi tidak diketahui3
3
Form the seamless shell
Form the seamless shell
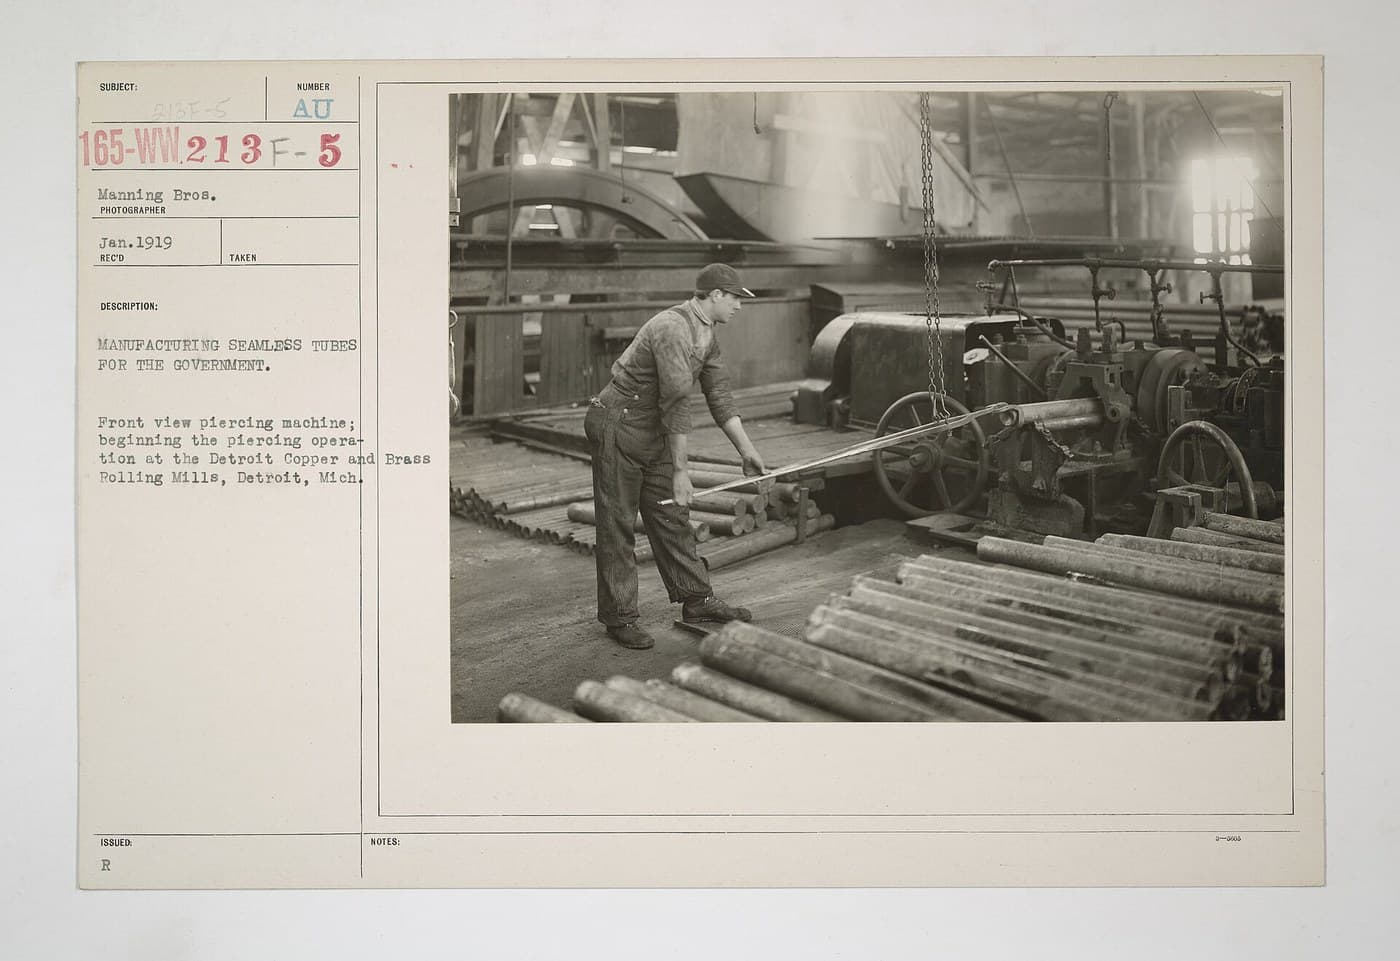
Form the billet into a seamless cylinder with no fissures and a smooth, even surface; machine away any defects. A bottom closed by welding or spinning must be at least twice the minimum wall thick. Do not weld anything else, except neck and foot rings on cylinders of 500 psi or less. Not given: how the shell is formed (the rule names hot drawing from billet or plate, and spinning).
Alatan diperlukan:
 Kaedah pembentukan tidak diketahuiDimensi tidak diketahui
4
4
Thread the neck
Thread the neck
Cut a clean, even thread in the neck opening, to gauge. A taper thread must be at least as long as an American Standard taper pipe thread. A straight thread needs at least six engaged threads, a tight fit, a gasket, and a shear strength of at least ten times the test pressure.
Alatan diperlukan:
 Set pemotong ulir
5
5
Heat-treat
Heat-treat
Heat-treat each finished cylinder evenly before testing. Quench it in oil or another suitable medium from the temperature right for the steel, no higher than 1750 °F, then temper at 1000 °F or more. Or normalise 4130X at 1650 °F instead, with no tempering. A cylinder quenched in water, or in anything cooling more than 80 % as fast, must be checked for quench cracks by magnetic particle, dye penetrant or ultrasound; a cracked one is scrapped.
Alatan diperlukan:
 Ketuhar rawatan haba
 Tangki lindap kejut berminyak
 Ketuhar sepuh lindap
6
6
Pressure-test every cylinder
Pressure-test every cylinder
Test each cylinder with water by the water-jacket or direct-expansion method of CGA C-1, to at least 5/3 of service pressure, held for at least 30 seconds and until it stops expanding. Between heat treatment and this test, never go above 90 % of test pressure. The permanent expansion may not pass 10 % of the total expansion. Not given: the CGA C-1 apparatus.
Alatan diperlukan:
 Kit ujian tekanan hidraulik
7
7
Test one from each lot
Test one from each lot
From each lot of 200 or fewer, take one cylinder. Flatten it between two 60° knife edges rounded to ½ in radius, set across its axis: it must reach six times the wall thickness without cracking. Cut two tensile specimens from it: find the yield at 0.2 % offset, moving the cross-head no faster than ⅛ in per minute, and the tensile strength; elongation must be at least 20 % over 2 in (10 % on other gauge lengths). A rejected cylinder may be heat-treated again and retested, never repaired by welding or spinning.
Alatan diperlukan:
 Mesin tekan hidraulik
 Mesin ujian bahan
8
8
Fit the valve
Fit the valve
Screw the valve into the threaded neck. A cylinder whose bottom was closed by spinning or by a plug must also pass a gas leak test: apply at least service pressure to one side of the clean, dry bottom for at least a minute, with the other side under water, and reject it at any leak. Not given: the valve.
Bahan untuk langkah ini:
 Injap tidak diketahui1 keping
Alatan diperlukan:
 Sepana boleh laras
Bahan
2- 1 per cylinderPemegang Tempat
- 1 kepingPemegang Tempat
Alatan Diperlukan
10- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
Bahan Blueprint Bersambung


Blueprint ini membuat
Blueprint berkaitan
Blueprint ini berkongsi pengetahuan — teknik, bahan atau prinsip
CC0 Domain Awam
Blueprint ini dikeluarkan di bawah CC0. Anda bebas menyalin, mengubah, mengedar, dan menggunakan karya ini untuk sebarang tujuan, tanpa meminta kebenaran.
Sokong Pembuat dengan membeli produk melalui Blueprint mereka di mana mereka memperoleh Komisen Pembuat ditetapkan oleh Penjual, atau cipta iterasi baru Blueprint ini dan sertakan ia sebagai sambungan dalam Blueprint anda sendiri untuk berkongsi hasil.