SENI
KECANTIKAN & KESEJAHTERAAN
KRAFTANGAN
BUDAYA & SEJARAH
HIBURAN
ALAM SEKITAR
MAKANAN & MINUMAN
KEJURUTERAAN TERBALIK
SAINS
SUKAN
TEKNOLOGI
BOLEH PAKAI

Walls and Infill: Strength Comes From the Outside, Not the Middle
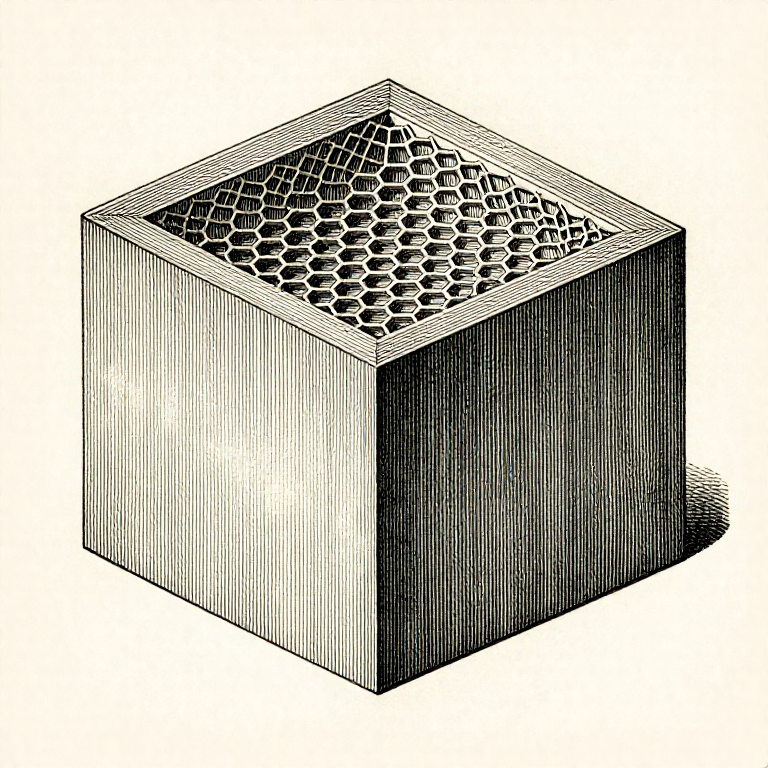
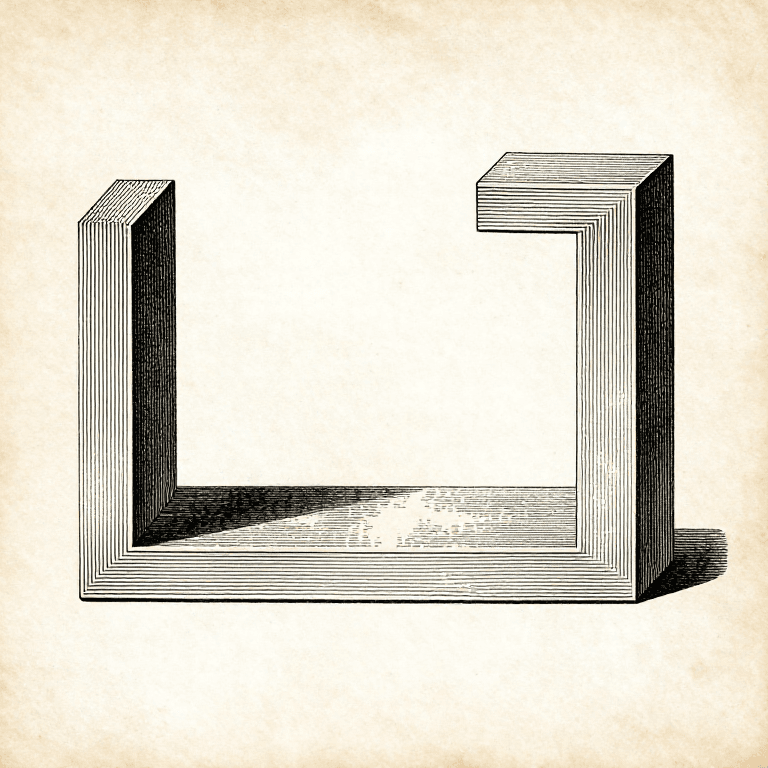
The usual response to a part that broke is to raise the infill. It is almost always the wrong lever: for a part in bending, the material near the surface does most of the work and the material in the middle does almost none.
That is not a printing fact, it is geometry. Bending stiffness depends on how far the material sits from the neutral axis — so a wall at the outside is worth many times an equal weight of plastic in the centre.
Which makes WALL COUNT the setting that matters. Going from two walls to four typically does more for strength than going from 20% infill to 60%, and costs less time and less filament.
Pertengahan
3 hours
Arahan
1
1
Walls against infill, in numbers
Walls against infill, in numbers
Memuatkan buku nota Jupyter…
Bahan untuk langkah ini:
 Filamen cetakan 3D (PLA)1 keping
Alatan diperlukan:
 Komputer Meja
 Perisian penghiris fail 3MF
 Angkup Digital 6 Inci
2
2
Make wall thickness a multiple of the line width
Make wall thickness a multiple of the line width
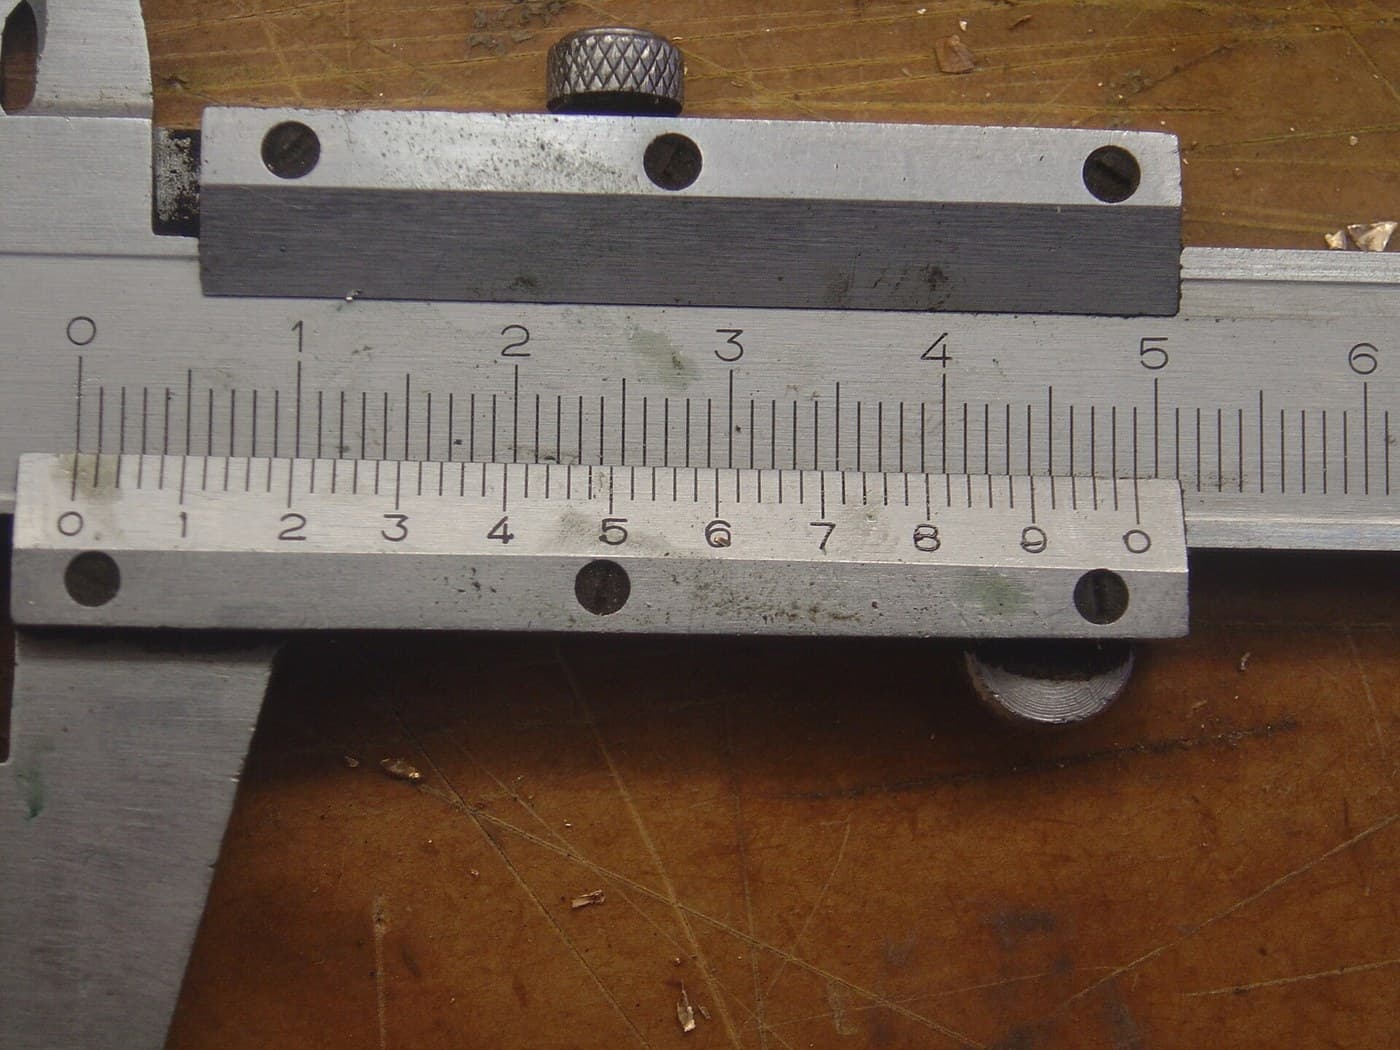
A wall 1.0 mm thick printed with a 0.42 mm line cannot be made of whole lines. The slicer either leaves a gap in the middle or over-extrudes to fill it, and both are weaker than a wall that is an exact number of lines.
So design walls at multiples of the line width: 0.84 mm for two lines, 1.26 for three, 1.68 for four. It is not fussiness — it is the difference between a wall that is solid and one with a void running through it.
Modern slicers handle odd thicknesses much better than they used to, varying the line width to suit. It is still worth designing to the grid where you can, and it is worth knowing this is why a 1 mm wall sometimes prints badly.
Bahan untuk langkah ini:
Filamen cetakan 3D (PLA)1 kepingAlatan diperlukan:
Perisian penghiris fail 3MFKomputer Meja Set muncung pencetak 3D
3
3
Top and bottom layers, and why the top looks rough
Top and bottom layers, and why the top looks rough
The top surface is printed over infill, which is mostly air. Too few solid layers and the top sags into the gaps — the 'pillowing' that makes a top face look dimpled.
Four to five solid top layers is a normal starting point, and more infill helps by giving them less distance to bridge. That is one of the few cases where raising infill is the right answer, and it is about surface quality rather than strength.
The bottom needs solid layers too, and for a different reason: they are what the part stands on and what a screw head bears against. A part with one bottom layer tears through if anything is bolted to it.
Bahan untuk langkah ini:
Filamen cetakan 3D (PLA)1 kepingAlatan diperlukan:
Perisian penghiris fail 3MF Kanta Pembesar Tukang Emas
 Pencetak 3D filamen (FDM)
4
4
Infill pattern matters less than people think
Infill pattern matters less than people think
Gyroid, cubic, grid, triangular — the differences between patterns at the same percentage are small compared with the difference between two walls and four. Choosing a pattern is a late optimisation.
Where it does matter: GYROID is isotropic and prints without the nozzle crossing its own path, which makes it quiet and good for flexible parts. GRID is fast but the nozzle crosses itself every layer, which can knock the part. TRIANGULAR is strong in plane and used where the load is known.
Pick one, use it consistently, and change the wall count instead. That is the change-one-thing-at-a-time rule applied to a slicer: a hundred settings are available and about four of them matter.
Bahan untuk langkah ini:
Filamen cetakan 3D (PLA)1 kepingAlatan diperlukan:
Perisian penghiris fail 3MFKomputer MejaAlatan Diperlukan
6- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
- Pemegang Tempat
Blueprint berkaitan
Blueprint ini berkongsi pengetahuan — teknik, bahan atau prinsip

CC0 Domain Awam
Blueprint ini dikeluarkan di bawah CC0. Anda bebas menyalin, mengubah, mengedar, dan menggunakan karya ini untuk sebarang tujuan, tanpa meminta kebenaran.
Sokong Pembuat dengan membeli produk melalui Blueprint mereka di mana mereka memperoleh Komisen Pembuat ditetapkan oleh Penjual, atau cipta iterasi baru Blueprint ini dan sertakan ia sebagai sambungan dalam Blueprint anda sendiri untuk berkongsi hasil.