IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
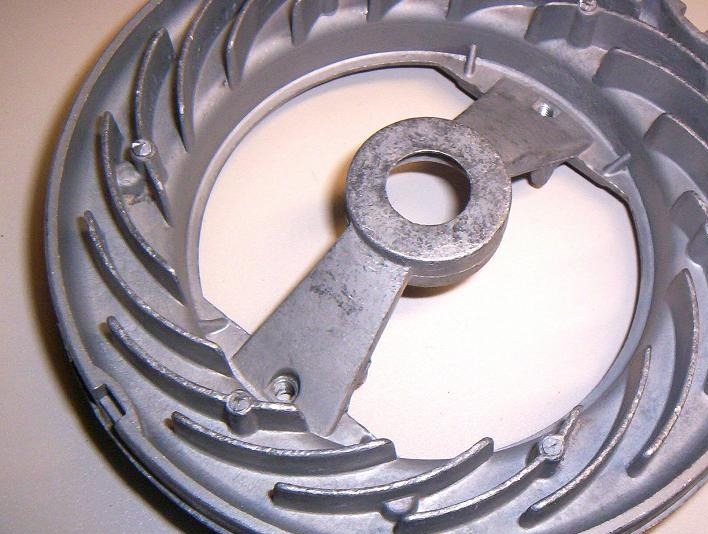

Aluminium Die Casting
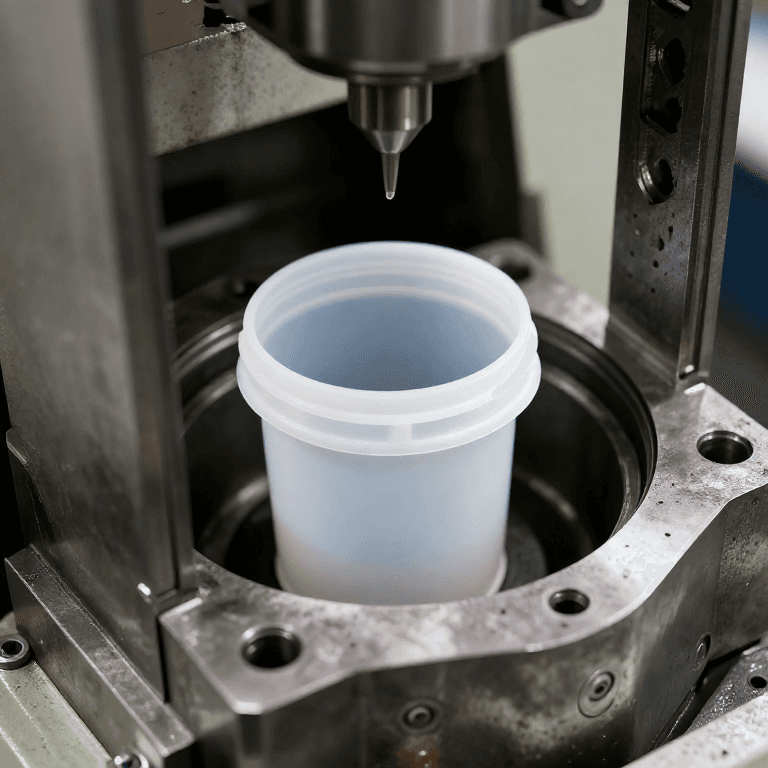
Die casting is injection moulding for metal: molten metal is forced at high pressure, about 10–175 MPa, into a steel die, held until it freezes, and pushed out by ejector pins. Aluminium needs a cold-chamber machine, where each shot is ladled in from a separate furnace, because molten aluminium would pick up iron from a submerged pump. The gate, runners and flash are broken off afterwards. Enclosures, housings and brackets come out with fine detail and little machining.
Ilọsíwájú
Seconds per casting (industrial)
Ìlànà
1
1
Melt
Melt
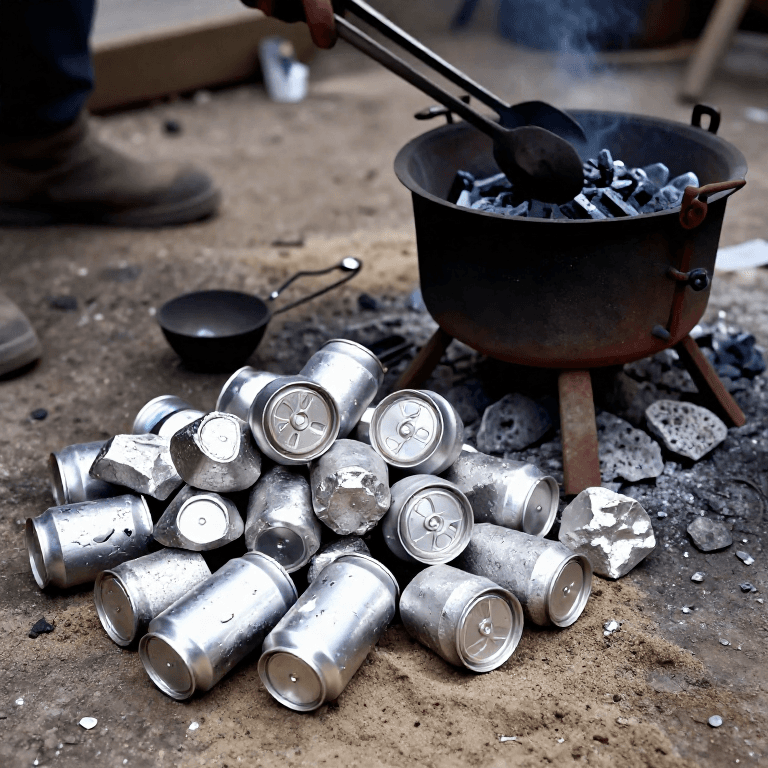
Aluminium ingots are melted in a holding furnace beside the machine.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ìṣù aluminiọ̀mù50 kg
2
2
Prepare the die
Prepare the die
The two die halves are sprayed with release lubricant and closed.
Àwọn irinṣẹ́ tí a nílò:
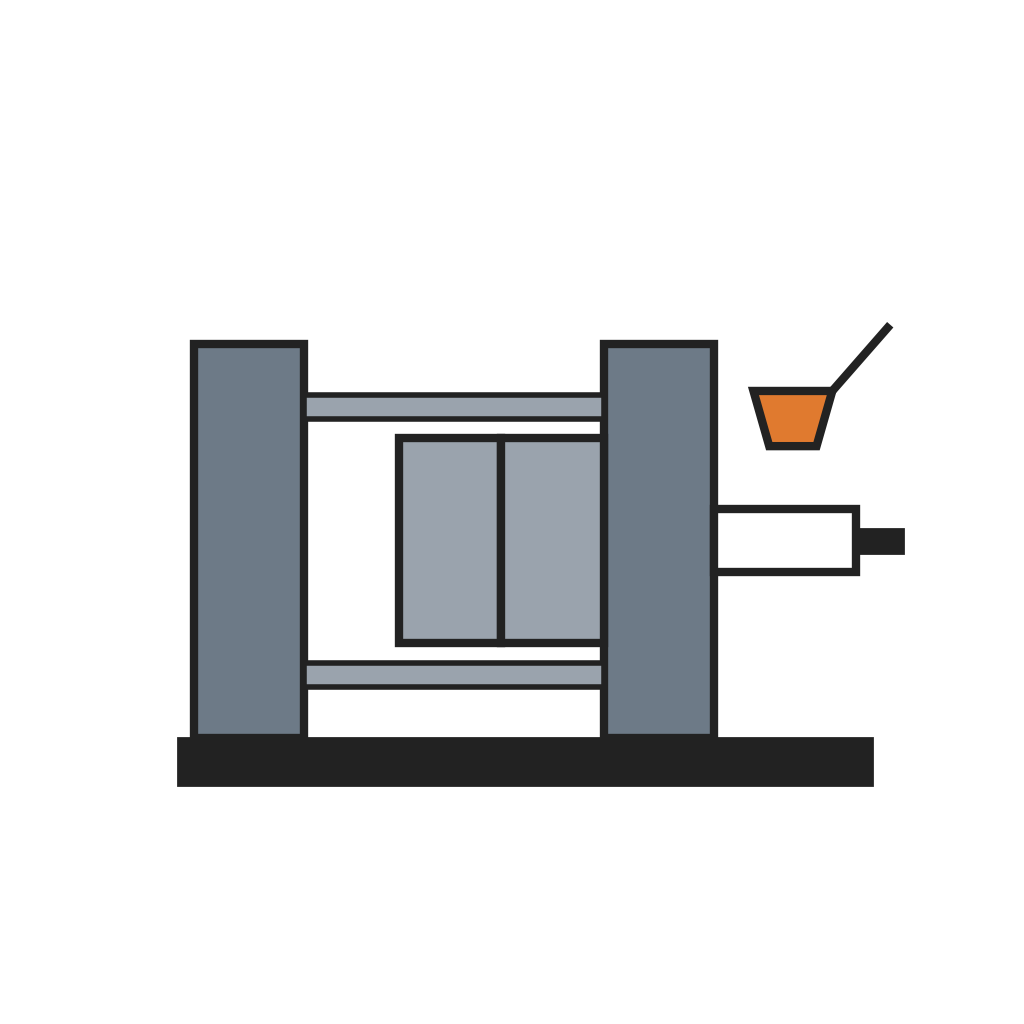 Ẹ̀rọ ìdà onípá
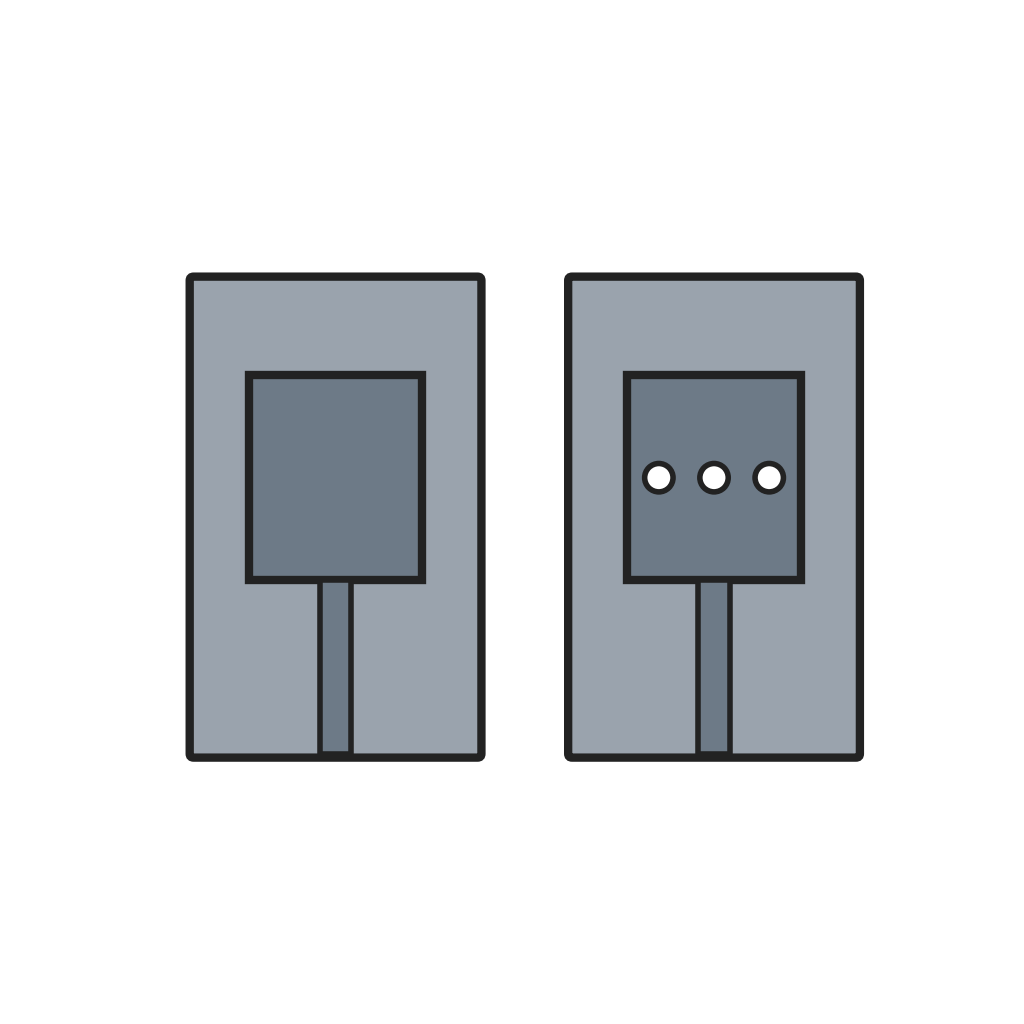 Àwòṣe ìdà onípá
3
3
Shot
Shot
A measured ladle of metal goes into the shot sleeve and a plunger drives it into the die at high pressure.
Àwọn irinṣẹ́ tí a nílò:
Ẹ̀rọ ìdà onípá4
4
Freeze and eject
Freeze and eject
Pressure is held while the metal freezes; the die opens and ejector pins push the casting out.
Àwọn irinṣẹ́ tí a nílò:
Ẹ̀rọ ìdà onípáÀwòṣe ìdà onípá5
5
Trim and check
Trim and check
Gate, runners and flash are removed and the casting is checked against the drawing.
Àwọn irinṣẹ́ tí a nílò:
 Òṣùwọ̀n Kálípà Díjítà Ìnṣì 6
Àwọn ohun-èlò
1- 50 kgÀyè
Àwọn irinṣẹ́ tó nílò
3Ìtọ́nisọ́nà yìí ń ṣe
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà

CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.