Ìfọwọ́sowọ́pọ̀
IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
Títẹ̀ 3D
Ìtọ́nisọ́nà 14 wà • Ẹ̀ka kékeré 2
Ṣàwárí Àwọn Ẹ̀ka Kékeré
Àwọn Ìtọ́nisọ́nà (14)
Pocket Morse Code Learning Board - v.2
láti ọwọ́ Admiral OOM
Ẹ̀rọ Ìtanná
5
0
0
0
0
0
Pocket Morse Code Learning Board - v.3
láti ọwọ́ Admiral OOM
Ẹ̀rọ Ìtanná
1
0
0
0
0
0
Pocket Morse Code Learning Board - v.1
láti ọwọ́ Admiral OOM
Ẹ̀rọ Ìtanná
1
0
0
0
0
0
Okùn ẹ̀rọ ìtẹ̀wé 3D tí a tì jáde láti inú pẹ́lẹ́ẹ̀tì
láti ọwọ́ Pixel
Títẹ̀ 3D
64
0
0
0
0
0
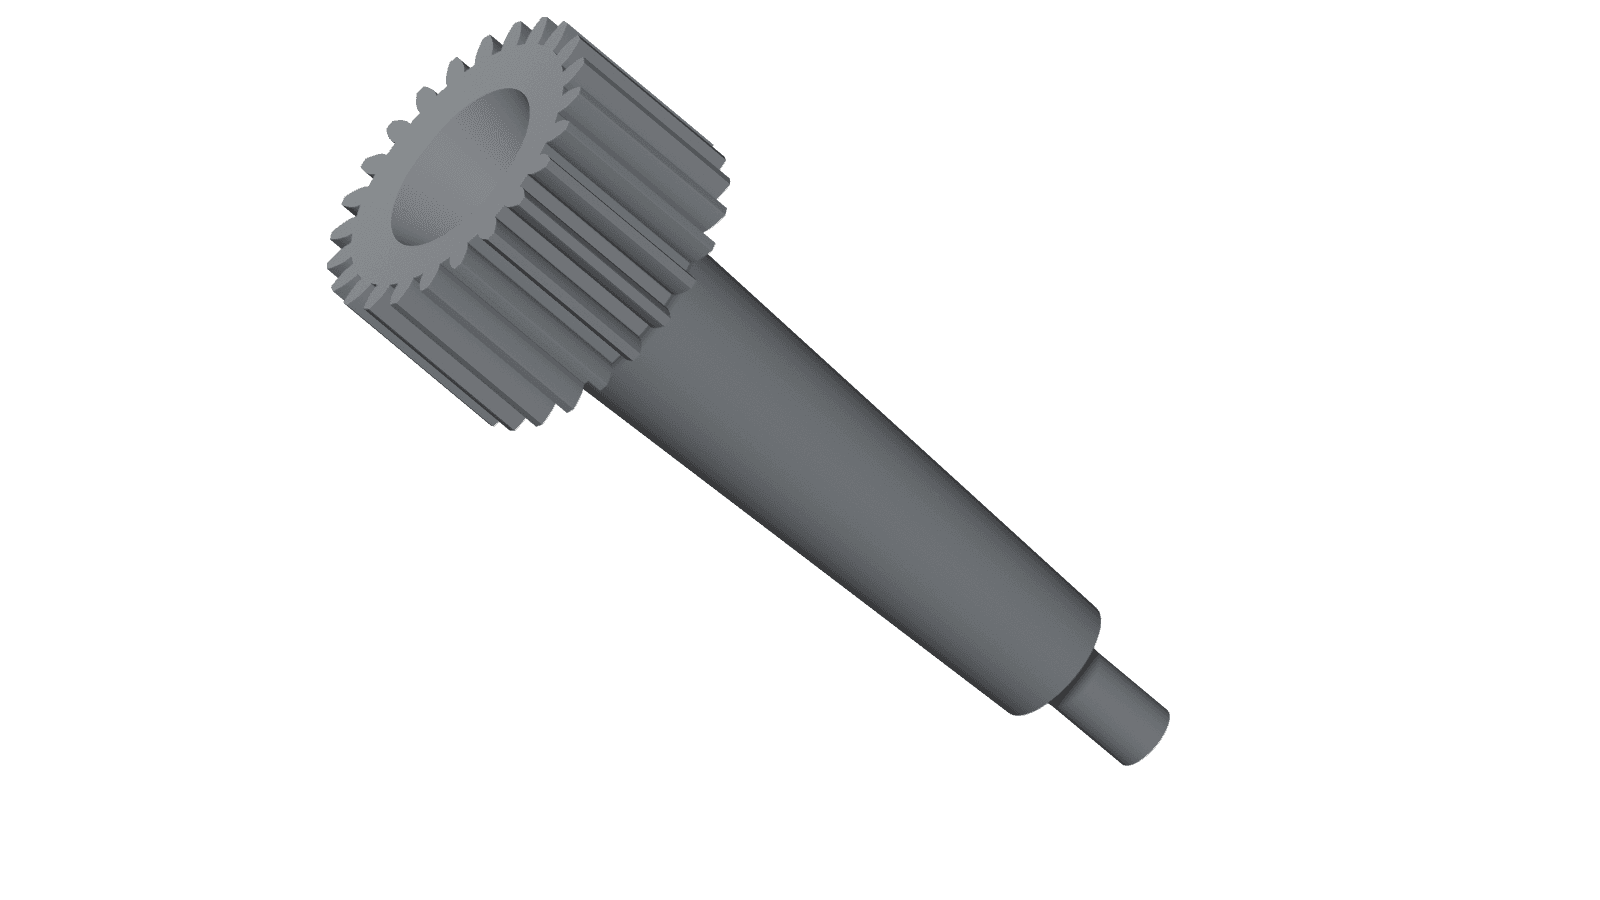
Ohun Ìgé Gear-Shaper ti Fellows (US 579,708): Àwọn Àwòṣe 3D
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
70
0
0
0
0
0
Designing For the Process: A Printable Part Is a Different Shape
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
34
0
0
0
0
0

Reading a Failed Print: The Fault Names Itself If You Look
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
37
0
0
0
0
0
Walls and Infill: Strength Comes From the Outside, Not the Middle
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
43
0
0
0
0
0
Warping: Why Big Flat Parts Lift at the Corners
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
42
0
0
0
0
0
Tolerance and Clearance: Printed Holes Come Out Small, Every Time
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
42
0
0
0
0
0
Overhangs, Bridges and Support: What the Machine Can Print Over Thin Air
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
40
0
0
0
0
0
Orientation: A Printed Part Is Weakest Between Its Layers
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
40
0
0
0
0
0
The First Layer Decides Everything Above It
láti ọwọ́ 3DBonanza
Títẹ̀ 3D
52
0
0
0
0
0

From Blender to G-code on Youblob — Upload .blend, Generate Print-Ready Instructions
láti ọwọ́ Pixel
Títẹ̀ 3D
83
0
0
0
0
0
Gbogbo 14 ti farahàn