IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
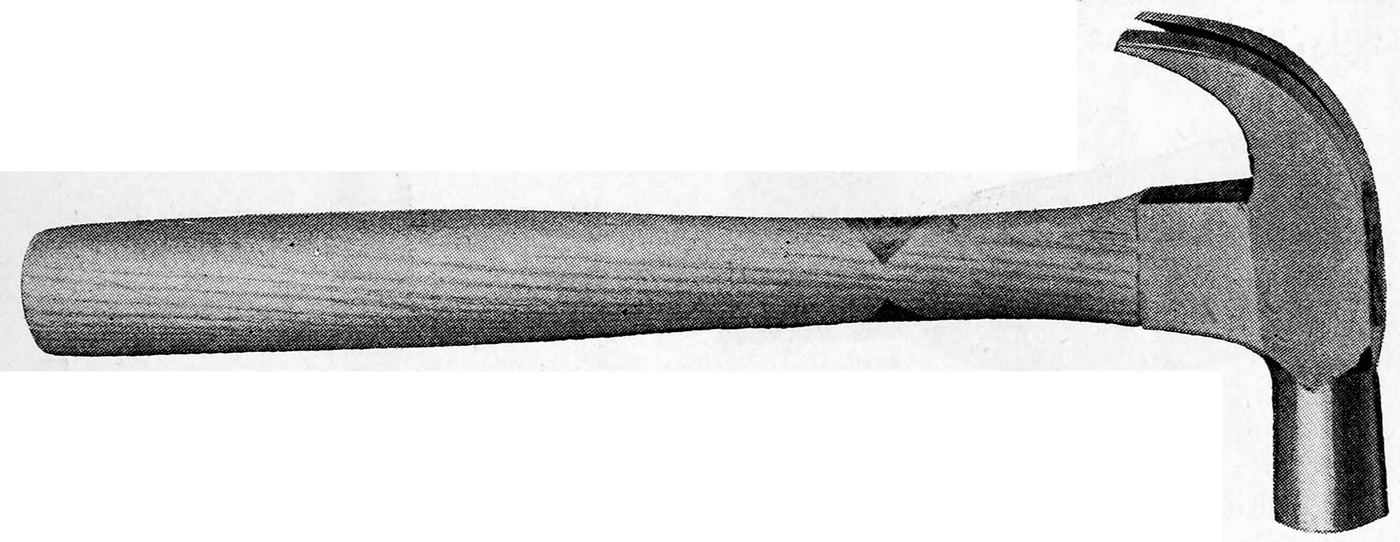

Claw Hammer: Drop-Forged Head, Turned Wooden Handle
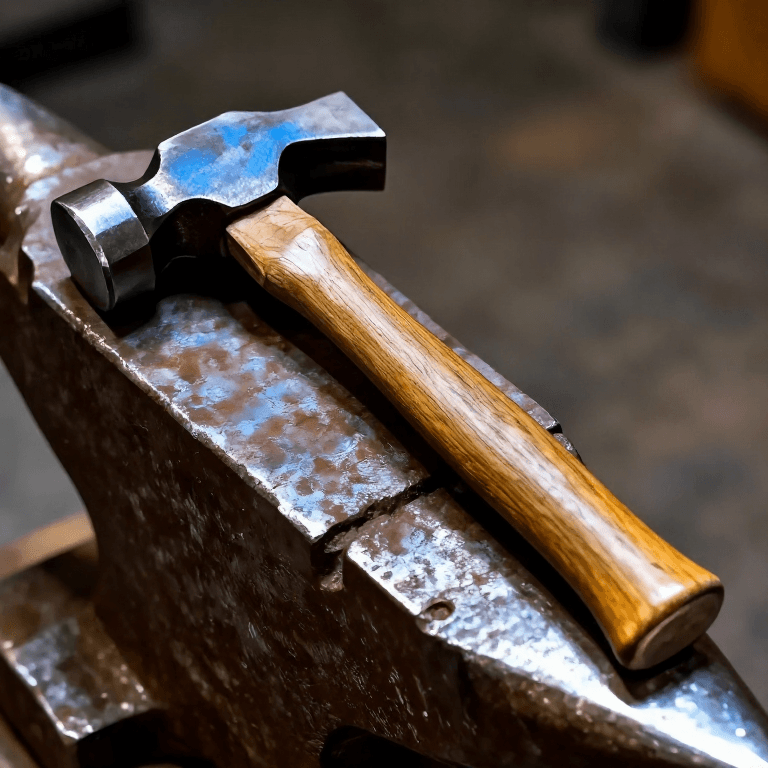
A claw hammer's head is high-carbon steel, hot forged between dies and then hardened only where it takes the blows: the face, the poll and the claws. The handle is straight-grained ash or hickory, woods with good strength, durability and enough give to absorb the shock of repeated blows. It is turned on a lathe that copies a cam, pushed up through the head's eye and wedged: one thin wooden wedge driven diagonally into a slot, then two steel wedges driven through it crossways.
Ilọsíwájú
Factory process
Ìlànà
1
1
Heat the bar
Heat the bar
Heat a length of steel bar to about 1,200–1,300 °C (2,200–2,350 °F) with open flame torches or by passing it through an induction coil.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀pá onígun mẹ́rin irin irinṣẹ́1 as required
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìmúgbóná induction
2
2
Forge the head
Forge the head
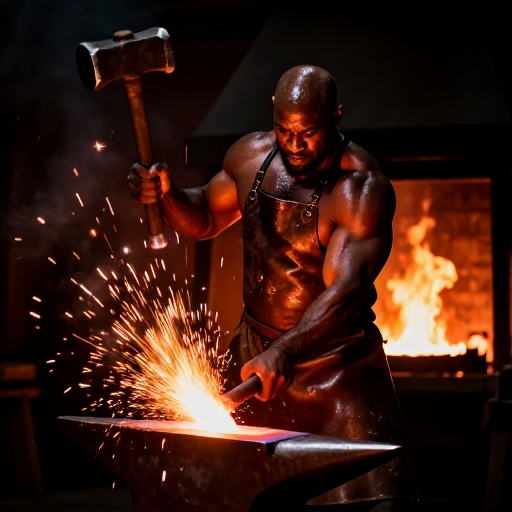
Put the hot bar or a cut blank between the dies. The ram forces them together and squeezes the steel into the die cavities; repeat in several dies to form the head step by step.
Àwọn irinṣẹ́ tí a nílò:
 Òòlù ìjánilẹ̀ pẹ̀lú àwòṣe ìrọ
3
3
Trim the flash
Trim the flash
Cut off the flash, the steel squeezed out between the dies, with trimming dies. Cool the head and grind off rough spots.
Àwọn irinṣẹ́ tí a nílò:
 Àwòṣe ìgé etí àṣẹ́kù
 Ẹ̀rọ ìfá orí tábìlì
4
4
Harden the face, poll and claws
Harden the face, poll and claws
Heat those areas with a flame or an induction coil and cool them quickly, so the steel near the surface becomes much harder than the rest of the head.
Àwọn irinṣẹ́ tí a nílò:
Ẹ̀rọ ìmúgbóná induction5
5
Clean and polish
Clean and polish
Shot blast the head (a stream of air carrying small steel particles), paint it if wanted, then polish the face, poll, claws and cheeks. Smooth the V-slot of the claws with an abrasive disc.
Àwọn irinṣẹ́ tí a nílò:
 Kọ́bọ́ọ̀dù ìfọ́n ọta
 Àgbá ìdán
6
6
Turn the handle
Turn the handle
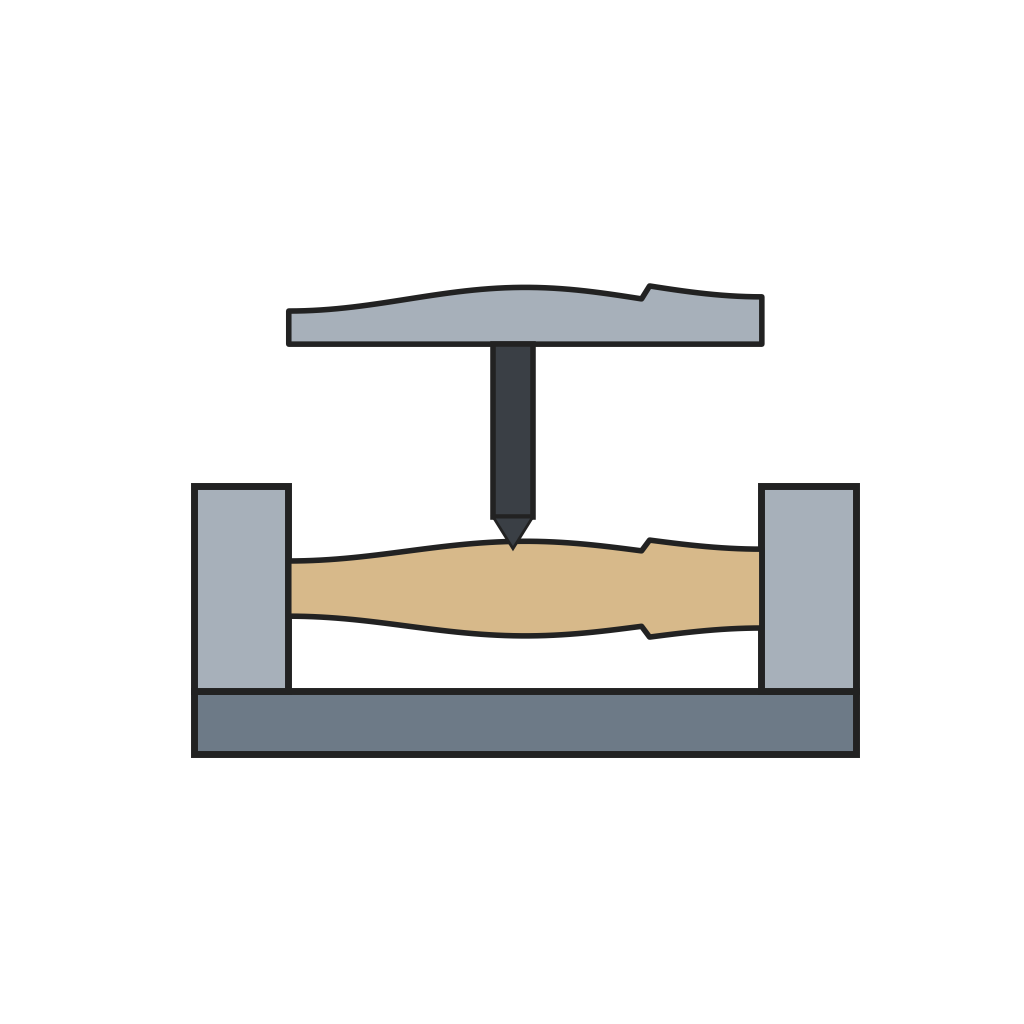
Cut ash or hickory to length and hold it at both ends in the lathe. As it spins, the cutting tool follows a cam with the handle's shape. Cut a slot diagonally across the top and sand the handle smooth.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Igi Líle Fún Ìdìmú1 ẹyọ
 Bébà Ìfá1 as required
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìgbẹ́ ọwọ́ irinṣẹ́ tí kámù ń darí
7
7
Hang the head
Hang the head
Push the handle up through the eye of the head. Tap the wooden wedge into the diagonal slot to spread the handle against the head, then drive two small steel wedges through it crossways.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Gọ̀gọ̀ igi líle1 ẹyọ
 Ìgèrè irin oníkọjá2 ẹyọ
Àwọn ohun-èlò
5- 1 as requiredÀyè
- 1 ẹyọÀyè
- 1 as requiredÀyè
- 1 ẹyọÀyè
- 2 ẹyọÀyè
Ìtọ́nisọ́nà yìí ń ṣe
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà
CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.