IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
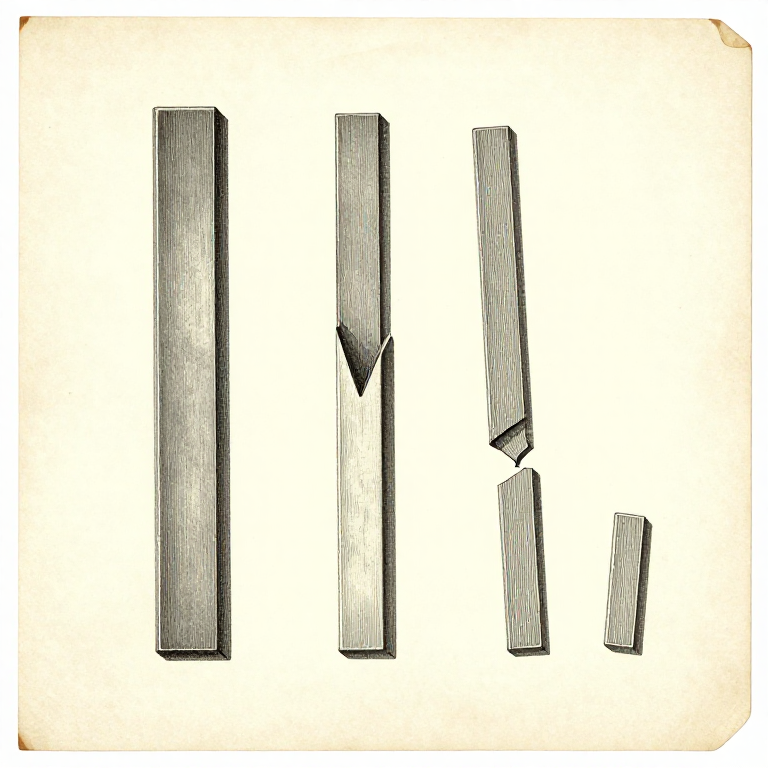


Cutting Hot Metal: The Hardy, the Chisel, and Never Through to the Face
Hot steel cuts like hard cheese. A chisel that would barely mark a cold bar sinks through a bright orange one in a few blows, which makes cutting to length a forge operation rather than a saw one.
The rule that governs all of it: never cut all the way through onto the anvil FACE. The face is hardened and a chisel driven into it leaves a permanent notch that prints into everything you forge afterwards.
So you cut nearly through, then break — or you cut over the soft step, or over the hardy hole, where going through costs nothing.
Àárín
2 hours
Ìlànà
1
1
The hot cut hardy: the chisel that points up
The hot cut hardy: the chisel that points up
Drop a hot cut hardy into the hardy hole and it becomes an upward-facing chisel. Lay the hot bar on it and hammer from above, and the bar is cut between the hammer and the hardy edge.
Rotate the bar as you go, cutting a groove all the way round rather than driving straight through one side. A bar cut from one side only ends up with a long drawn-out tail rather than a square end.
Stop before you go right through — leave a thin web — and break the piece off by bending it. Driving the last of the cut through drives the bar down onto the hardy's edge, and a hardy is much easier to damage than to replace.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀pá irin rírọ̀1 ẹyọ
 Èédú Ìṣùu1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Ọ̀bẹ ìgé lórí ìdí alágbẹ̀dẹ
 Ìdí Alágbẹ̀dẹ
 Òòlù alágbẹ̀dẹ
 Ẹmú alágbẹ̀dẹ
2
2
A hot chisel from above, over the step
A hot chisel from above, over the step
A hand-held hot chisel does the same job from the top, which suits cutting part way in — a shoulder, a slit for a joint, a decorative line.
Work over the soft STEP of the anvil, not the face, wherever the chisel might go through. That is what the step is for, and it is why it is deliberately left unhardened.
Keep the hot chisel cool: dip it every few blows exactly as with a punch. A hot chisel is not hardened as far as a cold chisel — it relies on the work being softer than it is — so letting it get hot ruins the edge quickly.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Ọ̀pá irin rírọ̀1 ẹyọ Omi1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
Ìdí Alágbẹ̀dẹÒòlù alágbẹ̀dẹẸmú alágbẹ̀dẹ Ìbọ̀wọ́ Awọ Apá Gígùn
3
3
Hot chisel and cold chisel are different tools
Hot chisel and cold chisel are different tools
A COLD chisel is ground to a stout angle — around 60 degrees — because it has to survive cutting metal that is not giving way. A HOT chisel is ground much thinner, around 30 degrees, because hot steel offers little resistance and a thin edge cuts far better.
Use them the wrong way round and both fail: a cold chisel in hot steel is slow and leaves a rough cut, and a hot chisel in cold steel chips its edge off immediately.
Mark them so you cannot confuse them — a band of paint, a different handle, separate racks. The angle rung in the sharpening batch is where those numbers come from, and it is the same logic: the angle follows the job.
Àwọn irinṣẹ́ tí a nílò:
 Lúpù ÌgbégaỌ̀bẹ ìgé lórí ìdí alágbẹ̀dẹ
 Ìṣètò búrọ́ọ̀ṣì okùn
4
4
Mind where the offcut goes
Mind where the offcut goes
A short hot offcut breaks free suddenly and flies. It is at forging heat, it is sharp, and it lands somewhere you were not looking.
Cut so the offcut falls away from you and downward, keep the floor clear of anything that will burn, and know where it went before you take the next heat. A hot offcut on the floor looks exactly like a cold one after a minute.
The same habit as the cooling rung: anything that has been in the fire is hot until proved otherwise, and it goes in one designated place. None of this makes the work risky — it is the small set of habits that makes it ordinary.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Ọ̀pá irin rírọ̀1 ẹyọÀwọn irinṣẹ́ tí a nílò:
Ẹmú alágbẹ̀dẹ Gílásì Ààbò Tí Ó Mọ́Ìbọ̀wọ́ Awọ Apá Gígùn
Àwọn irinṣẹ́ tó nílò
8- Àyè
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà

CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.