
Cylindrical Grinding Machine
Measuring to a thousandth is useless if nothing can be made to a thousandth. Grinding is how metrology stopped being a laboratory exercise and became manufacturing.
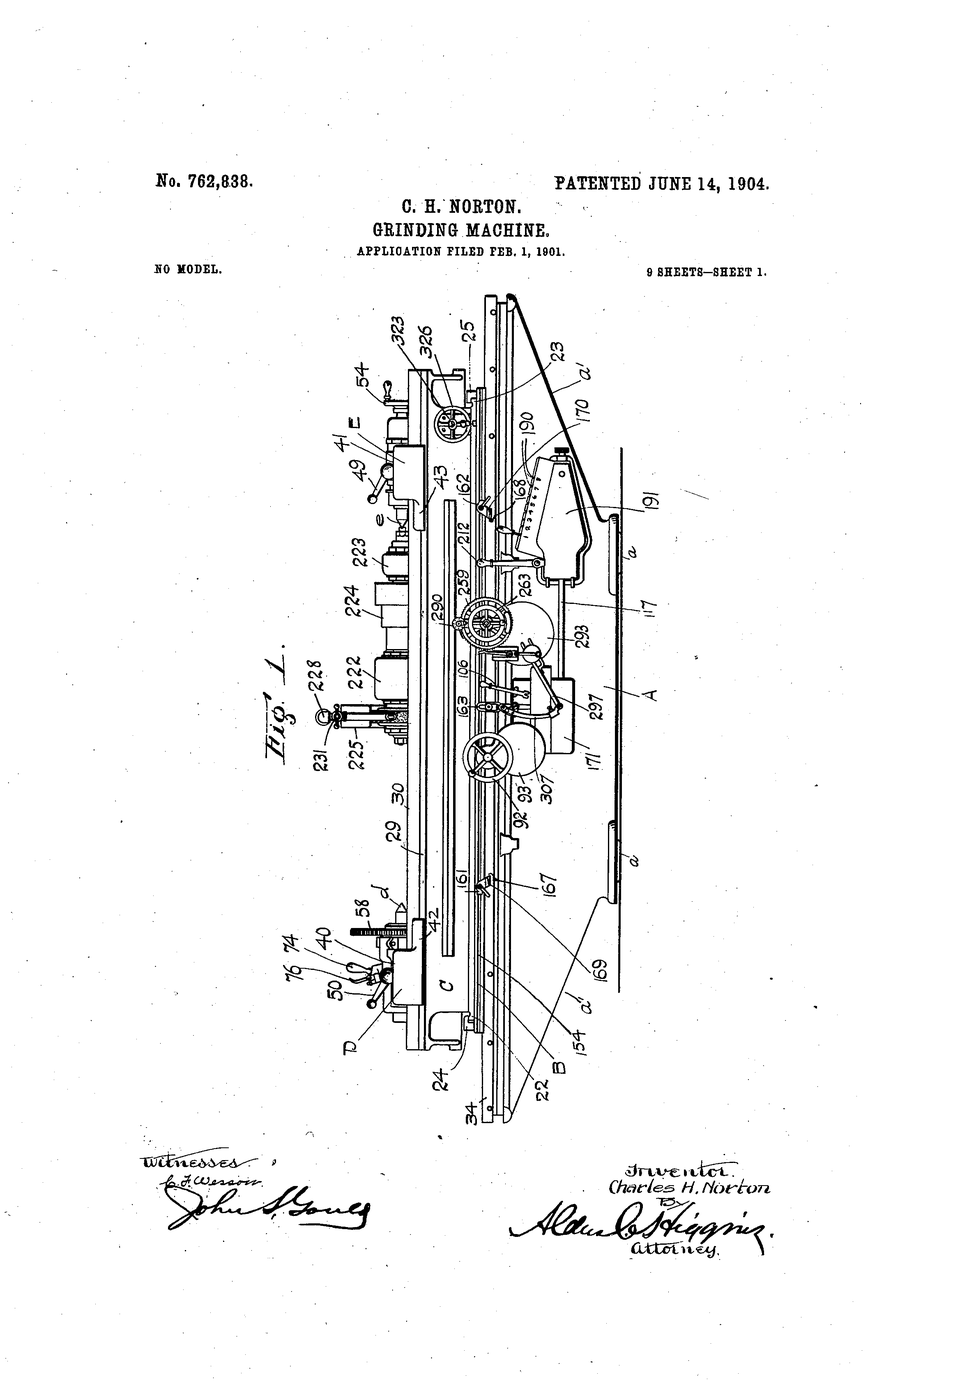
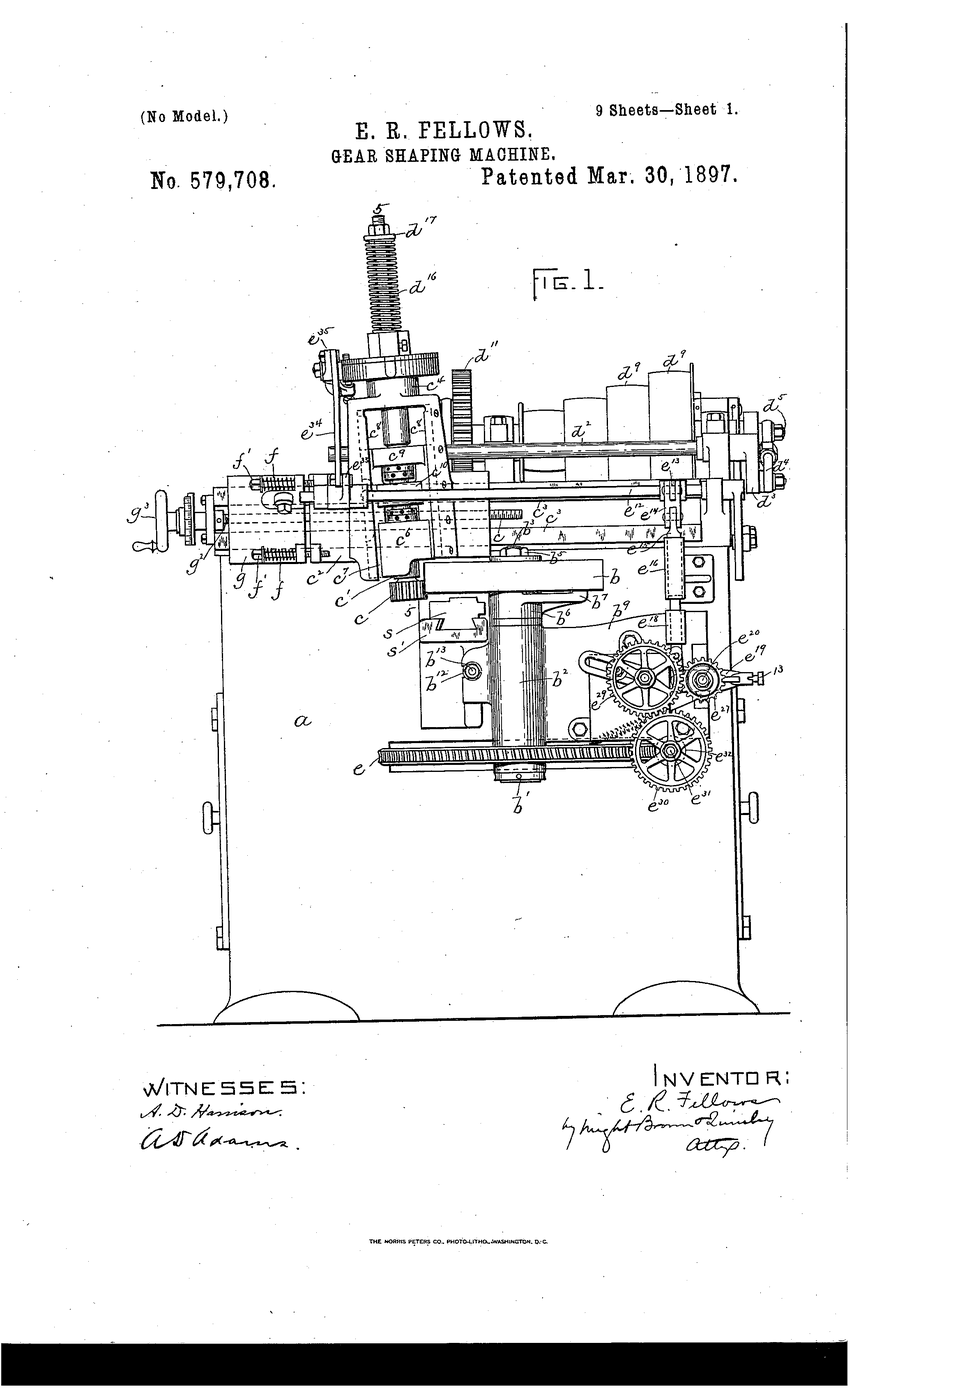
US 762,838, “Grinding-Machine”, Charles H. Norton of Worcester, Massachusetts, filed 1 February 1901 and granted 14 June 1904, assigned to the Norton Grinding Company. Norton's argument, in his own words, was “great rigidity of parts, minute accuracy in grinding heavy work, simplicity and cheapness of construction”.
Rigidity is the insight. Everyone before him built grinders light, because grinding was thought of as delicate finishing. Norton built a machine weighing over 6,800 kg with a wide wheel and took heavy cuts — and got better accuracy, not worse, because a rigid machine does not flex away from the work.
Ìlànà
Read the claim before you build
Read the claim before you build
Norton claims rigidity as the route to accuracy — the opposite of the intuition that delicate work needs a delicate machine. Write down why you would expect the opposite.
Feel flex in a thin beam
Feel flex in a thin beam
Hold the steel ruler flat, press its end sideways. It bends easily. Now turn it on edge and press again. Same steel, far stiffer. Shape beats material.
Àwọn irinṣẹ́ tí a nílò:
 Steel Ruler (30cm)
Measure the deflection
Measure the deflection
Clamp the ruler flat over the board's edge and press with a known steady push; measure the deflection with the dial indicator.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Flat Wooden Board1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Dial IndicatorSteel Ruler (30cm)
Repeat on edge
Repeat on edge
Repeat with the ruler on edge. Record the much smaller deflection. This ratio is why Norton's machine was heavy.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Graph Paper1 ewé
Àwọn irinṣẹ́ tí a nílò:
Dial IndicatorSand a rod by hand
Sand a rod by hand
Sand the brass rod by hand for one minute, turning as you go.
Àwọn irinṣẹ́ tí a nílò:
 Brass Rod
Measure what hand work achieved
Measure what hand work achieved
Measure the rod at four points around and along with the micrometer. Record the spread.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Graph Paper1 ewéÀwọn irinṣẹ́ tí a nílò:
 MicrometerBrass Rod
Build a rigid rest
Build a rigid rest
Glue two blocks to the board so the rod is supported close to where it is being worked. Support near the cut is the whole trick.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Flat Wooden Board1 ẹyọ Wood Glue5 ml
Work the rod again with support
Work the rod again with support
Sand again, this time with the rod held in the rest and rotated steadily.
Àwọn irinṣẹ́ tí a nílò:
Brass RodMeasure and compare
Measure and compare
Measure the four points again. Compare the spread with step 6. Same abrasive, same hand, better geometry.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Graph Paper1 ewéÀwọn irinṣẹ́ tí a nílò:
MicrometerCheck roundness with the indicator
Check roundness with the indicator
Roll the rod under the dial indicator on the surface plate. The needle sweep is out-of-roundness.
Àwọn irinṣẹ́ tí a nílò:
Dial Indicator Surface PlateBrass Rod
Deliberately support it badly
Deliberately support it badly
Remove one support and work the rod again. Measure. Chatter and taper appear immediately.
Àwọn irinṣẹ́ tí a nílò:
Brass RodMicrometerCheck against a gauge
Check against a gauge
Set a feeler stack to your target and test whether the rod passes. Grinding without a gauge is just polishing.
Àwọn irinṣẹ́ tí a nílò:
 Feeler Gauge Set
Grind to a stated tolerance
Grind to a stated tolerance
Set a target such as ±0.05 mm and work until every measured point falls inside it. Record how many attempts it took.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Graph Paper1 ewéÀwọn irinṣẹ́ tí a nílò:
MicrometerBrass RodHistory & Context
History & Context
US 762,838, “Grinding-Machine”, Charles H. Norton, Worcester, Massachusetts, filed 1 February 1901, granted 14 June 1904, assigned to the Norton Grinding Company.
A date correction. Popular accounts date this machine to 1900 and often imply the patent is contemporaneous. 1900 is when Norton designed it; the application was filed in February 1901 and took more than three years to issue.
What it did to industry. Norton's grinder could finish a cylindrical part far faster than anything before it while holding about a quarter of a thousandth of an inch. Henry Ford bought them in quantity for Model T production. Grinding a crankshaft or a bearing race to a repeatable diameter is precisely what makes engines mass-producible — the Timken tapered roller bearing linked here is one of the parts that depends on it.
Why rigidity beats delicacy. A cutting force pushes the tool away from the work. If the machine flexes, the cut is shallower than commanded, and worse, the flex varies as the force varies, so the error is not even constant. A heavy machine deflects less, so what you command is what you get. This is one of the genuinely counter-intuitive results in engineering, and it is why precision machine tools are massive lumps of cast iron rather than elegant frames.
Where it sits. Johansson's blocks, linked here, define the size. Norton's machine produces it. Without both, a tolerance on a drawing is a wish.
Àwọn Ohun Èlò Ìtọ́nisọ́nà Tí A So Pọ̀
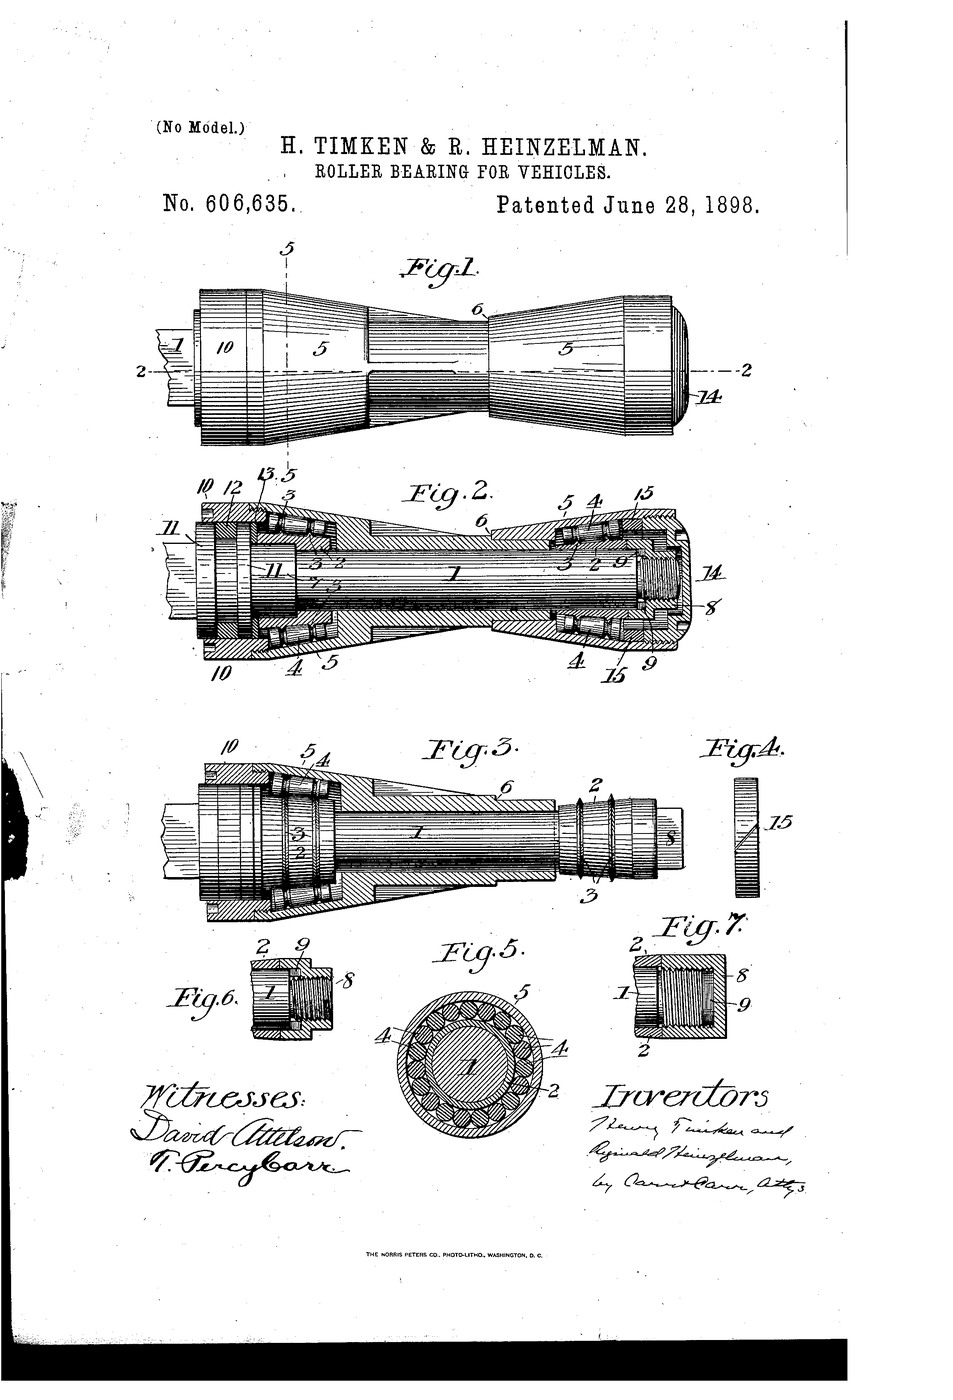

Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà
CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.