IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
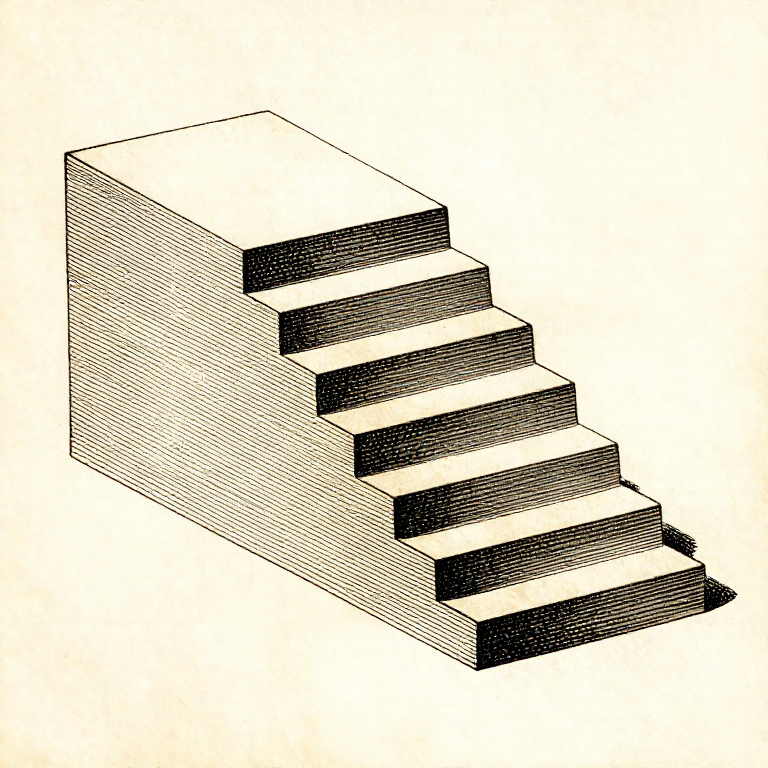


Overhangs, Bridges and Support: What the Machine Can Print Over Thin Air
Each layer is laid on the one below it. Where there is no layer below, the plastic has nothing to sit on — so the question for every sloping surface is how much of each line is still supported by the line under it.
The rule of thumb is 45 degrees, and it is not arbitrary: at 45 degrees each line overhangs the one below by exactly half its width, and half a line is enough to hold. Past that the overhang grows quickly and the plastic droops.
A BRIDGE is the other case: a flat span between two supported ends, printed as a stretched thread across the gap. Bridges work far better than most people expect, and designing to use them is how supports get avoided.
Àárín
3 hours
Ìlànà
1
1
Why 45 degrees, in numbers
Why 45 degrees, in numbers
Ń ṣí ìwé Jupyter…
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Okùn ìtẹ̀wé 3D (PLA)1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Kọ̀ǹpútà Tábìlì
 Sọ́fítíwéà pípín fáìlì 3MF
 Ìdìpọ̀ ẹnu ẹ̀rọ ìtẹ̀wé 3D
2
2
Bridges: flat spans print better than slopes
Bridges: flat spans print better than slopes
A bridge is printed as a single stretched line pulled tight between two anchored ends. Because it is in tension it stays straight, and a well-cooled bridge of 50 mm or more comes out flat.
The first bridging layer is printed FAST and with full cooling, so the line is drawn thin and sets before it can sag. Slicers detect bridges and do this automatically, which is why a bridge often succeeds where a gentler slope fails.
So a square hole printed with a flat top is often better than one with an arch, and a teardrop-shaped horizontal hole is better than a round one because it turns the unsupported top into a self-supporting point. Designing the shape to suit the process is the last rung of this batch.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Okùn ìtẹ̀wé 3D (PLA)1 ẹyọÀwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìtẹ̀ 3D oníwàyà (FDM)Sọ́fítíwéà pípín fáìlì 3MF
 Òṣùwọ̀n Kálípà Díjítà Ìnṣì 6
3
3
Support is a cost, so spend it deliberately
Support is a cost, so spend it deliberately
Support material is printed, then thrown away, and it leaves a rough scar on every surface it touched. So it costs time, filament and finish — three things at once.
Use SUPPORT ON BUILD PLATE ONLY where possible. Support that grows from the part itself marks the part; support that rises from the plate marks nothing except where it meets the overhang.
Increase the Z gap between support and part until it releases by hand. A gap of one layer height is usually right: smaller and it fuses on, larger and the overhang above it droops into the gap. It is worth finding your printer's number once and writing it down.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Okùn ìtẹ̀wé 3D (PLA)1 ẹyọÀwọn irinṣẹ́ tí a nílò:
Sọ́fítíwéà pípín fáìlì 3MF Ohun èlò ìmúkúrò èèpo
 Ìdìpọ̀ ohun èlò ẹ̀rọ ìtẹ̀wé 3D
4
4
Print a test tower before trusting a part
Print a test tower before trusting a part
An overhang test is a small model with faces at a range of angles, printed once per filament and per layer height. Twenty minutes, and it tells you exactly where your machine stops coping.
Keep them, labelled with the filament and settings. A drawer of test prints is the same thing as a shelf of glaze test tiles: a physical record that answers questions faster than any table.
Re-test when anything changes — a new filament, a new nozzle, a different cooling duct. Overhang performance is one of the most machine-specific things in printing, and a number from somebody else's printer is a starting guess.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Okùn ìtẹ̀wé 3D (PLA)1 ẹyọ Okùn ABS1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
Ẹ̀rọ ìtẹ̀ 3D oníwàyà (FDM) Lúpù Ìgbéga
Àwọn irinṣẹ́ tó nílò
8- Àyè
- Àyè
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà

Designing and 3D-Printing a Self-Watering Planter — FDM Printing with PLA
láti ọwọ́ Pixel
Títẹ̀ 3D
59
0
0
0
2
0
Change One Thing at a Time: Grow the Control, and the Confounded Jar Too
láti ọwọ́ Penny
Ìtúpalẹ̀
8
0
0
0
0
0
One Reading Is Not a Measurement: Repeat It, and Look at the Spread
láti ọwọ́ Penny
Ìmọ̀-ẹ̀rọ
20
0
0
0
0
0
CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.