IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
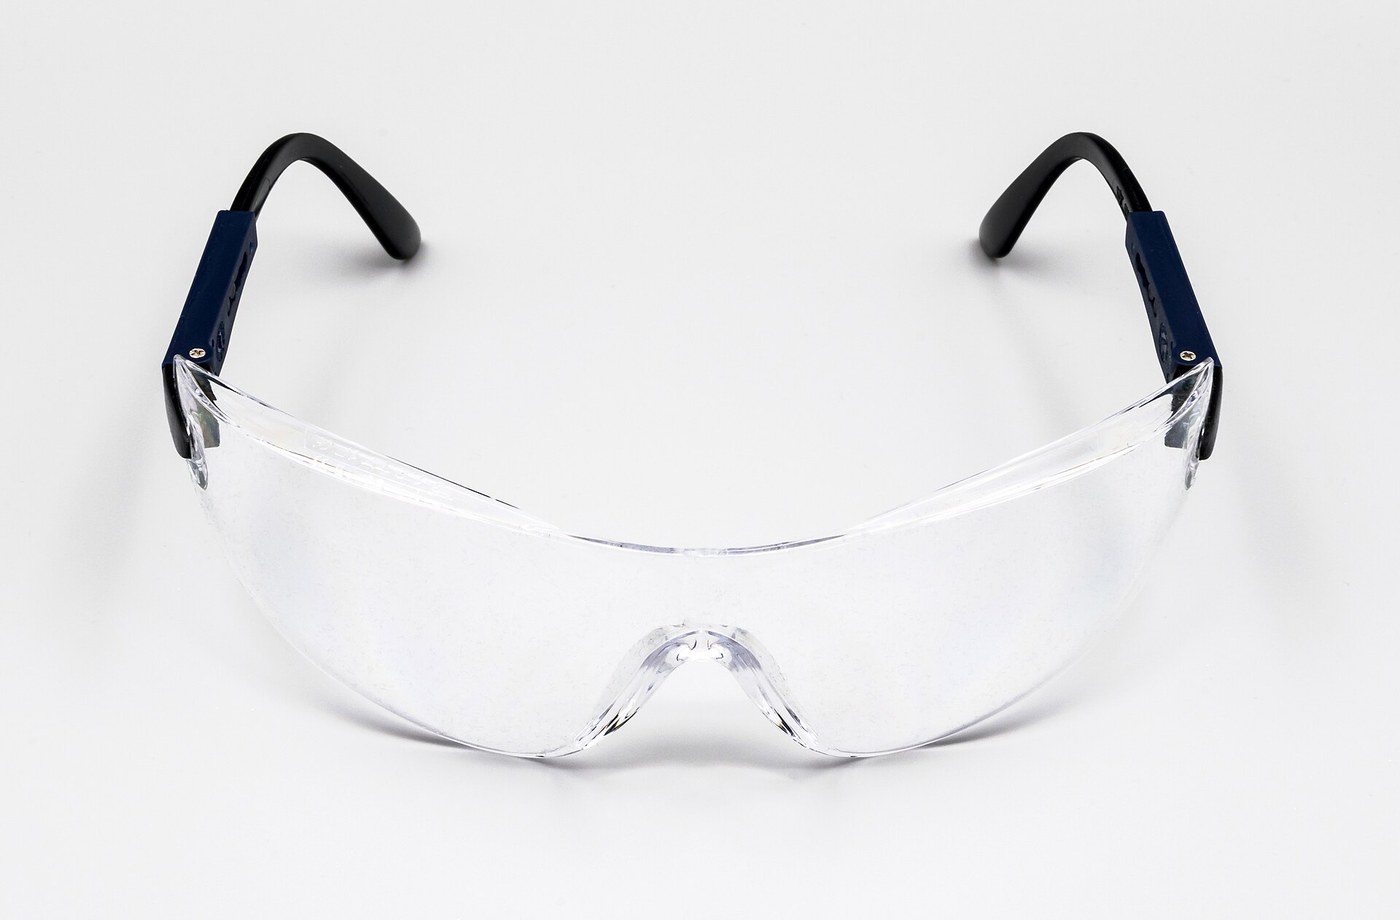

Safety Spectacles: Moulded Polycarbonate with a Hard Coat
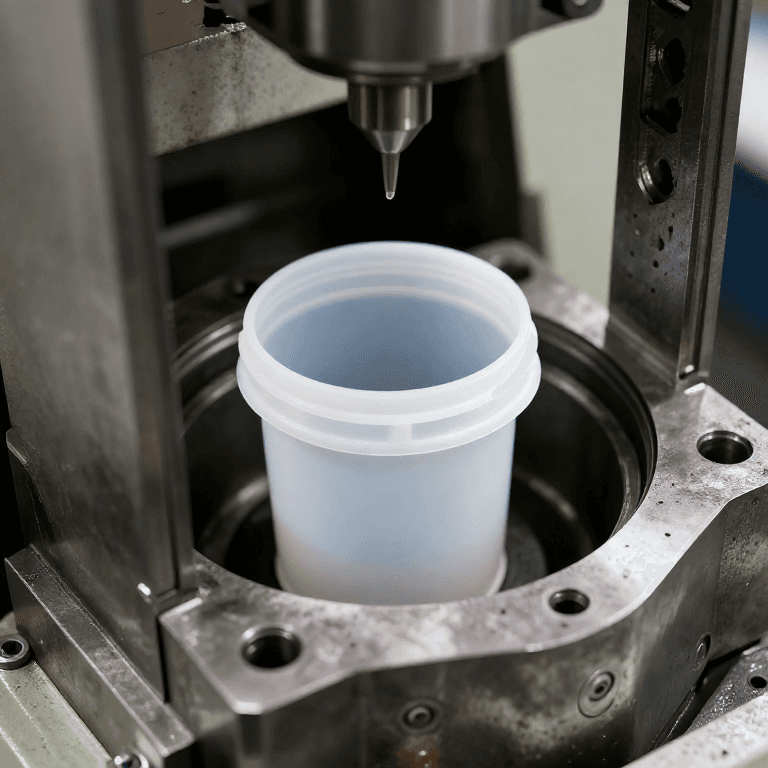
Industrial safety spectacles are injection-moulded from tough, transparent polycarbonate, often as a single front piece with the lenses, hinged to moulded temple arms; one design meeting the ANSI Z87.1 impact standard uses a lens 0.080 inch thick. Polycarbonate scratches easily, so the lenses get a thin, clear, abrasion-resistant coat of about 3–5 micrometres. Hard coats are applied by dipping or spinning after moulding: acrylate coats are cured by UV, siloxane coats by heat. Frames may be moulded in nylon.
Ilọsíwájú
Factory process
Ìlànà
1
1
Mould the front
Mould the front
Injection-mould the lens or one-piece front in polycarbonate.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Àwọn kóró polycarbonate0.05 kg
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìtẹ̀ ṣíṣu
2
2
Hard-coat
Hard-coat
Wash and dry the lens, dip it in the hard-coat solution and lift it out at an even speed.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Omi ìbora líle lẹ́ńsì1 lítà
Àwọn irinṣẹ́ tí a nílò:
 Táńkì ìbora ìrìbọmi
3
3
Cure
Cure
Dry the coat and cure it: UV for acrylate coats, heat for siloxane coats.
Àwọn irinṣẹ́ tí a nílò:
 Ààrò ìjinná
4
4
Mould the temples and assemble
Mould the temples and assemble
Mould the temple arms and hinge them to the front.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Àwọn kóró nylon0.02 kg
Àwọn irinṣẹ́ tí a nílò:
Ẹ̀rọ ìtẹ̀ ṣíṣuÀwọn ohun-èlò
3- 0.05 kgÀyè
- 1 lítàÀyè
- 0.02 kgÀyè
Àwọn irinṣẹ́ tó nílò
3- Àyè
Ìtọ́nisọ́nà yìí ń ṣe

Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà
CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.