IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
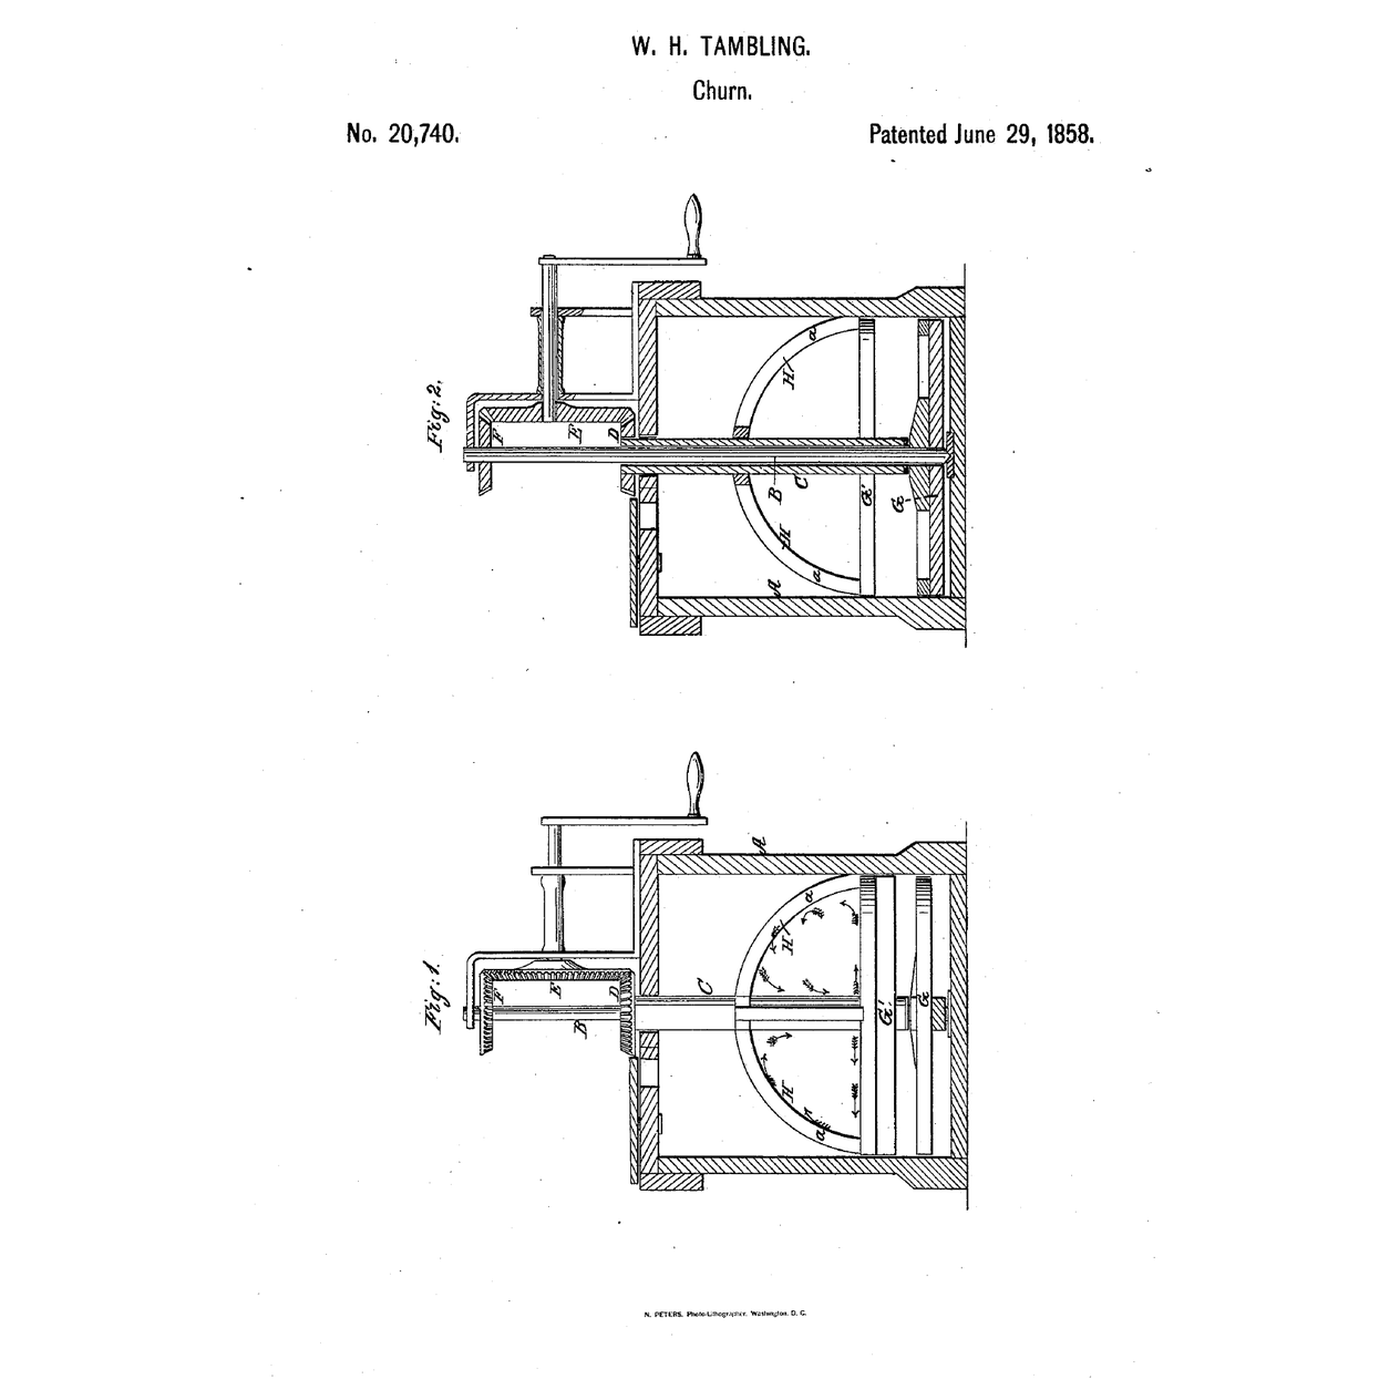


Skeleton-Semisphere Dasher Churn: Arched Ribs Over the Upper Dasher Roll the Cream Back to the Centre
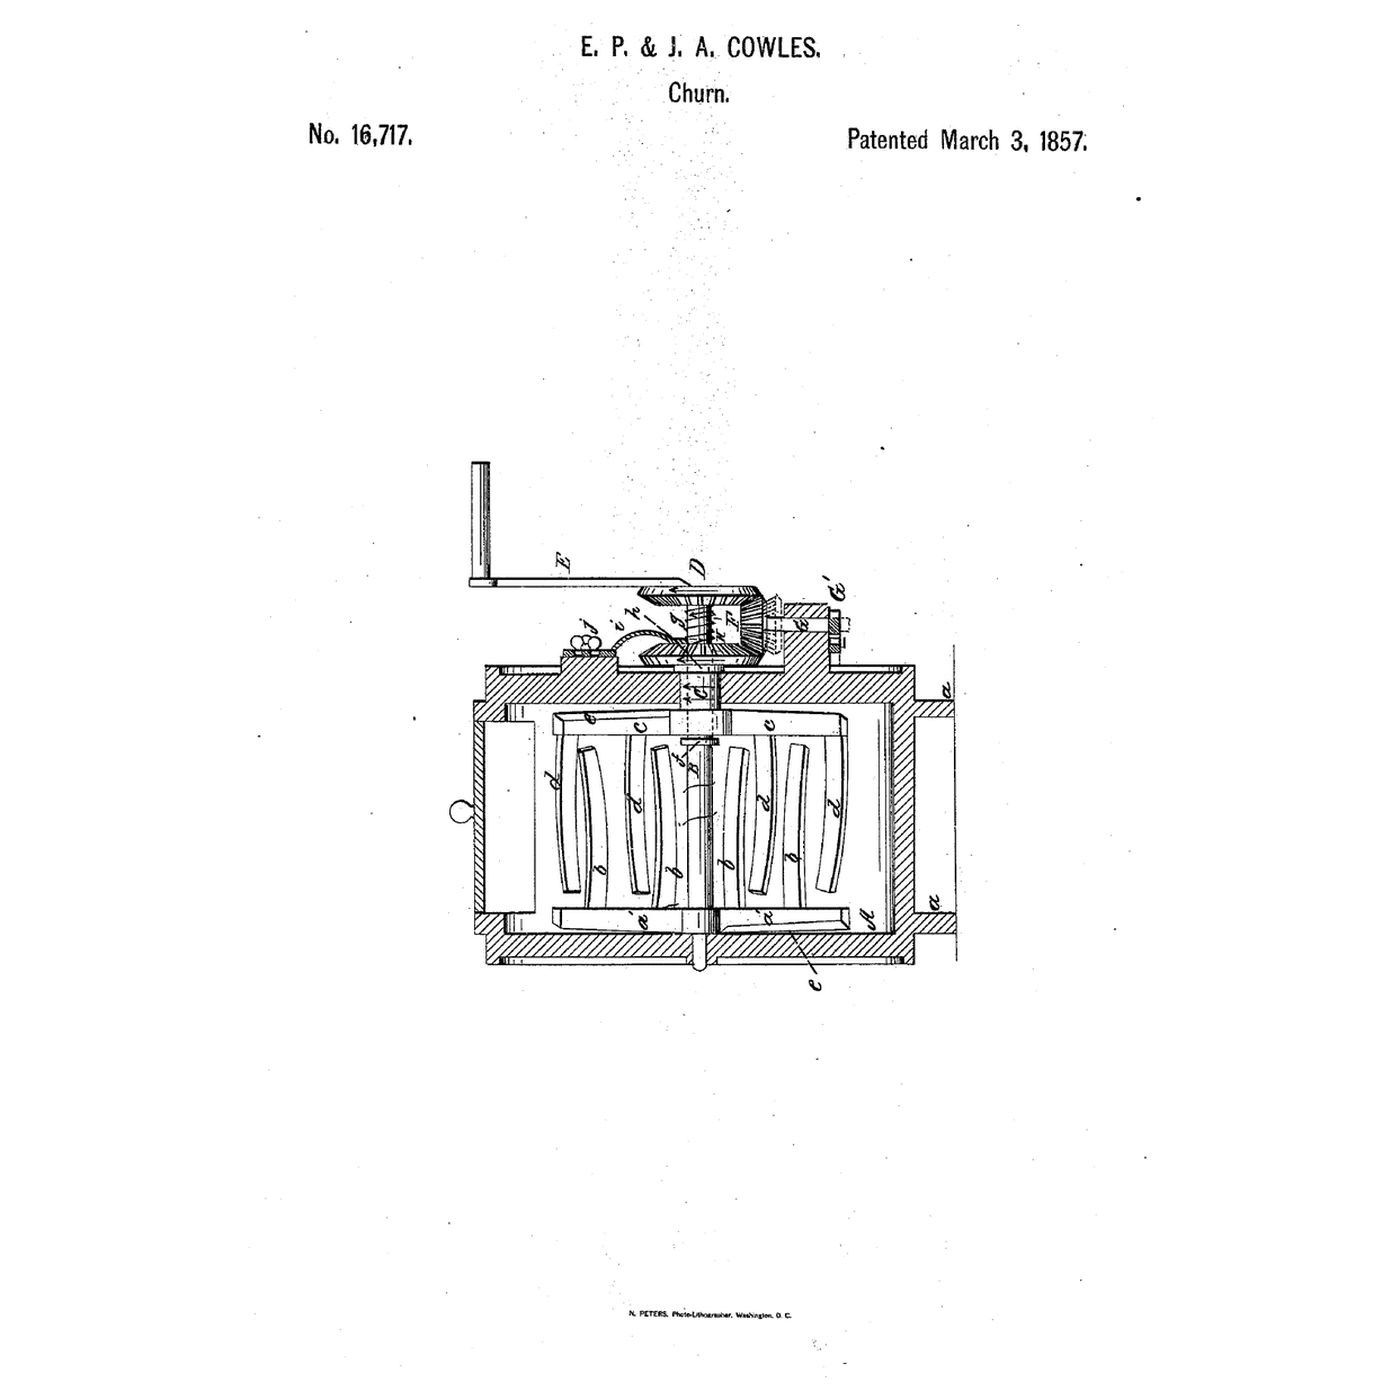
W. H. Tambling of Berlin, Wisconsin, received US 20,740, dated 29 June 1858, for a skeleton semisphere of ribs on the upper of two disk dashers turning opposite ways: cream thrown outward rises under its arched ribs and falls back at the centre, so no part of it is left undisturbed.
This rung prints the dashers, the ribs and the bevel gearing at tabletop scale, in a stock pot.
Ilọsíwájú
About 6 hours, plus printing
Ìlànà
1
1
Gearing and heights
Gearing and heights
Ń ṣí ìwé Jupyter…
2
2
Counter-turning churns, before it
Counter-turning churns, before it
Tambling kept two dashers turning opposite ways, as churns then did, and arched ribs over the upper one.
3
3
Read US 20,740
Read US 20,740
"The office of the circular disk form dashers is to agitate the cream near the bottom of the churn, while that of the skeleton semisphere is to agitate it near the center of the height of the churn."
4
4
Print the parts
Print the parts
Print the lower dasher (/uploads/blueprints/skeleton-semisphere-dasher-churn-lower-dasher.stl), the upper dasher with its tube (/uploads/blueprints/skeleton-semisphere-dasher-churn-upper-dasher.stl) disk down, four ribs (/uploads/blueprints/skeleton-semisphere-dasher-churn-rib.stl) flat, pinions D (/uploads/blueprints/skeleton-semisphere-dasher-churn-pinion-d.stl) and E (/uploads/blueprints/skeleton-semisphere-dasher-churn-pinion-e.stl), the wheel F (/uploads/blueprints/skeleton-semisphere-dasher-churn-wheel-f.stl), the step (/uploads/blueprints/skeleton-semisphere-dasher-churn-step.stl), the cover (/uploads/blueprints/skeleton-semisphere-dasher-churn-cover.stl), the standard (/uploads/blueprints/skeleton-semisphere-dasher-churn-standard.stl) and the crank (/uploads/blueprints/skeleton-semisphere-dasher-churn-crank.stl). Print in PETG at 0.2 mm layers, 30 % infill, 4 walls; wash before first use.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Okùn PETG1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìtẹ̀ 3D oníwàyà (FDM)
5
5
Shaft and dashers
Shaft and dashers
Cut a 10 mm square hardwood strip 320 mm long as the solid shaft and sand it. Set the step in the bottom of the pot and stand the shaft in it. Slide the lower dasher on, its boss 4 mm above the step, and fix it with an M3 screw drilled through the shaft. Press the four ribs' feet into the upper dasher's rim and their heads into the collar, then lower the upper dasher's tube over the shaft.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ìkòkò Ọbẹ̀ Ńlá1 ẹyọ
 Tẹ́ẹ́rẹ́ igi líle1 ẹyọ
 Skurú ẹ̀rọ1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Ayùn Ọwọ́
 Bébà Ìfá
 Ìlù ọwọ́
 Ìṣù àwọn ohun ìyí skurú
6
6
Cover and gears
Cover and gears
Lay the cover on the pot with the tube through its centre and a washer over it. Slide pinion D onto the flat at the tube's top, so the upper dasher hangs from it. Fix pinion E on the shaft above it with an M3 screw drilled through the shaft. Screw the standard to the cover from below with two M4 screws, push a 10 mm dowel through it as the axle, press wheel F tight onto its inner end so it meshes with D below and E above, and fix the crank on its outer end with an M3 screw drilled through the dowel.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Àwọn dowel igi líle1 ẹyọSkurú ẹ̀rọ1 ẹyọ
 Wáṣà Pẹrẹsẹ1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
Ayùn Ọwọ́Ìlù ọwọ́Ìṣù àwọn ohun ìyí skurú7
7
The build in 3D
The build in 3D
FreeCAD model of this build: the pot, the step, the square solid shaft with the lower disk dasher, the upper disk dasher on its tube with four arched ribs, the cover, bevel pinions D and E driven opposite ways by wheel F, the standard and the crank.
8
8
Churn
Churn
Pour in 3 litres of heavy cream at about 15 °C, checked with the thermometer. Turn the crank steadily and time it with the stopwatch: the disks turn opposite ways and the ribs roll the rising cream back toward the centre. When the butter comes, lift out the cover and dashers, pour off the buttermilk, wash the butter in cold water until it runs clear, work in a pinch of salt and weigh it.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀rá wàrà tó nípọn3 l
 Iyọ̀ Òkun Rúkèrúdò1 ẹyọ
 Omi1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìwọ̀n ooru oníhun tí ó dúró sí inú
 Aago Ìdúró
 Òṣùwọ̀n Díjítà Ilé Ìdáná
 Àwo ìdàpọ̀ ńlá ti irin tí kò ń yá
9
9
Troubleshooting
Troubleshooting
Skeleton-semisphere churn troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
**W. H. Tambling** of Berlin, Marquette County, Wisconsin, US 20,740, 29 June 1858, signed 8 June 1858, assigned to Aaron Hilton. He drew four ribs but would use six, eight or more as needed, smaller semispheres of fine wire ribs inside them, or the semisphere made like a coarse wire screen. He also suggested a complete skeleton sphere, the lower dasher made semispherical to match. He claimed only the semisphere on the upper dasher of a reverse-acting churn. Our pot, sizes, gear counts and printed parts are ours. FDM prints hold food in their layer lines, so wash well and replace when worn.
Àwọn ohun-èlò
9- 1 ẹyọÀyè
- 1 ẹyọÀyè
- 1 ẹyọÀyè
- 2 ẹyọÀyè
- 1 ẹyọÀyè
- 1 ẹyọÀyè
- Àyè
- 1 ẹyọÀyè
- 1 ẹyọÀyè
Àwọn irinṣẹ́ tó nílò
9- Àyè
- Àyè
- Àyè
- Àyè
Àwọn fáìlì àpẹrẹ
1Ìtọ́nisọ́nà yìí ń ṣe
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà


CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.