
Submerged Arc Welding
Kjellberg's coating protects the pool with a thin shell carried on the electrode. It works, but it limits how much current you can push: crank the amps up and the coating burns off ahead of the arc, spatter goes everywhere, and the operator is standing in front of a small sun.
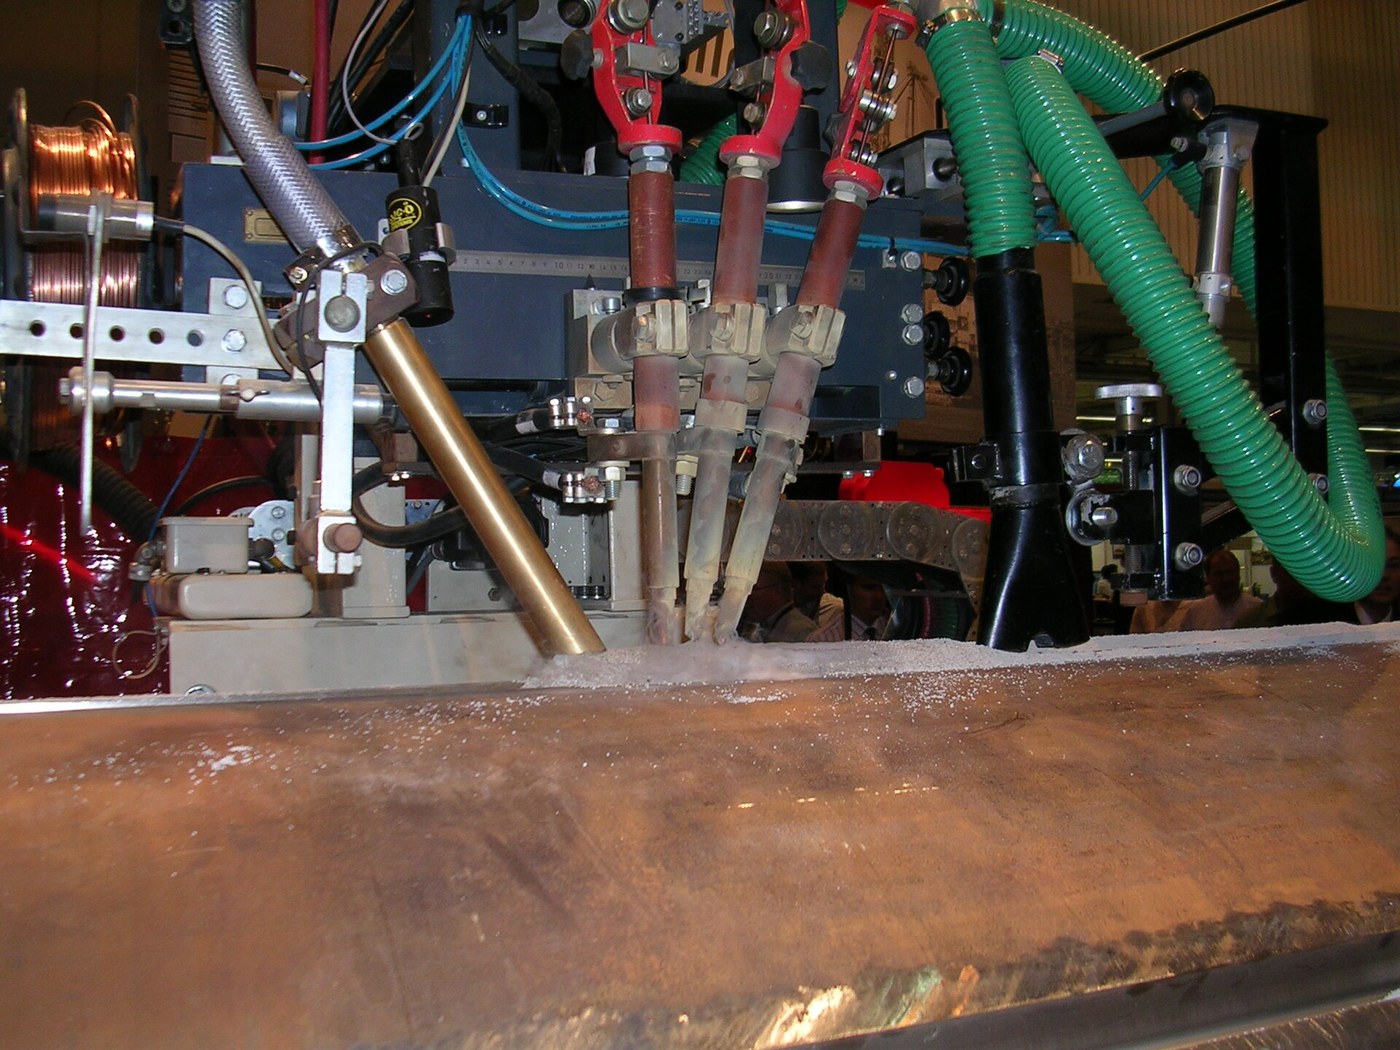
Submerged arc welding takes the idea to its conclusion. Instead of coating the electrode, pour a deep blanket of granular flux over the joint and run a bare wire down into it. The arc burns underneath the powder, completely buried. There is no visible light, almost no spatter, no fume escaping, and no radiated heat — and because the flux blanket also traps the heat, far more of the energy goes into melting metal instead of warming the room.
US 2,043,960, “Electric Welding”, filed 9 October 1935 and granted 9 June 1936. Three inventors are named — Lloyd T. Jones, Harry E. Kennedy and Maynard A. Rotermund, assigned to Union Carbide and Carbon. Note the spelling: Rotermund, not Rothermund, and three men rather than the one the process is usually credited to.
The experiment below buries a heat source under granular material and measures what the blanket does to the energy — the principle, at a temperature you can put a thermometer on.
Ìlànà
State the two claims you are testing
State the two claims you are testing
Write both down: a granular blanket blocks radiation, and a granular blanket keeps heat in the joint. They are separate claims.
Set up two identical steel coupons
Set up two identical steel coupons
Cut two matched coupons from the steel flat bar and sand both bright. They must start identical for the comparison to mean anything.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀pá Pẹrẹsẹ Irin Pẹ́lẹ́2 ẹyọ
 Bébà Ìfá1 ewé
Àwọn irinṣẹ́ tí a nílò:
 Ìwọ̀n Irin
 Kálípà Fáníà
Heat the open coupon and start timing
Heat the open coupon and start timing
Heat coupon A to about 400 °C with the torch, then remove the flame and start the clock. Record temperature every 30 seconds.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Ọ̀pá Pẹrẹsẹ Irin Pẹ́lẹ́1 ẹyọ Bíríkì Tí Ń Kojú Iná2 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Ọ̀pá Iná Pùróféènì
 Ẹ̀rọ Ìwọ̀n Ooru Infurarẹ́dì
 Ìbọ̀wọ́ Awọ
Heat the second coupon and bury it
Heat the second coupon and bury it
Heat coupon B the same way, then immediately cover it with 30 mm of clean dry sand. Start the clock again.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Ọ̀pá Pẹrẹsẹ Irin Pẹ́lẹ́1 ẹyọ Iyanrìn2 kg
Àwọn irinṣẹ́ tí a nílò:
Ọ̀pá Iná PùróféènìÌbọ̀wọ́ AwọTrack the buried coupon with the thermocouple
Track the buried coupon with the thermocouple
The infrared thermometer cannot see through sand. Use the thermocouple probe placed against the coupon before burying, and read every 30 seconds.
Àwọn irinṣẹ́ tí a nílò:
 Thermocouple irú K pẹ̀lú modulu MAX6675
Plot both cooling curves on one chart
Plot both cooling curves on one chart
Plot temperature against time for A and B together. The buried coupon holds heat markedly longer — that is the thermal-efficiency claim, confirmed.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Bébà Àwòrán1 ewé
Measure the radiation the blanket blocks
Measure the radiation the blanket blocks
Point the infrared thermometer at each coupon's surface from 300 mm. The sand surface reads far cooler than the bare coupon. That is why no helmet is needed.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Bébà Àwòrán1 ewéÀwọn irinṣẹ́ tí a nílò:
Ẹ̀rọ Ìwọ̀n Ooru Infurarẹ́dìÌwọ̀n IrinTest whether the blanket excludes air
Test whether the blanket excludes air
Uncover coupon B once cold and compare its surface with coupon A's. The buried one carries much less scale — the sand kept oxygen out too.
Àwọn irinṣẹ́ tí a nílò:
 Dígí Ìgbéga
Weigh the scale loss on both
Weigh the scale loss on both
Brush both coupons and weigh. Quantify what you saw in step 8 rather than trusting the eye.
Àwọn irinṣẹ́ tí a nílò:
 Òṣùwọ̀n Díjítà
 Àkójọ Ìfá
Note what real flux does that sand cannot
Note what real flux does that sand cannot
Record the difference: welding flux melts to a slag, deoxidises the pool and can carry alloying elements. Sand is inert — it models the blanket, not the chemistry.
Work out why the process must be mechanised
Work out why the process must be mechanised
The operator cannot see the arc. Write down what that implies: the travel speed, wire feed and current must be set by machine, not judged by eye.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Bébà Àwòrán1 ewéList where the geometry limits it
List where the geometry limits it
Loose powder falls off anything that is not roughly flat. Note the consequence: submerged arc welds flat and horizontal joints only — no overhead, no vertical.
Safety awareness — the hazard you cannot see
Safety awareness — the hazard you cannot see
An invisible arc is still an arc. Submerged arc welding is famous for needing no helmet, and that breeds carelessness: if the flux blanket thins or breaks — at the start of a run, at a joint edge, or when the hopper empties — the arc flashes through and the ultraviolet is as damaging as any other. Operators keep eye protection to hand precisely because the exposure is unexpected.
Hot flux looks exactly like cold flux. Fused slag and unfused powder are the same colour and sit side by side at wildly different temperatures. Recovered flux is handled with tools, and slag is chipped only behind eye protection — it detaches under tension and flies.
In this blueprint the sand is the hazard. Sand heated against a 400 °C coupon holds that heat for a long time and gives no visual warning at all. Leave it to cool fully and check with the thermometer before putting a hand near it.
Àwọn irinṣẹ́ tí a nílò:
 Gílásì Ààbò Tí Ó Mọ́Ìbọ̀wọ́ AwọẸ̀rọ Ìwọ̀n Ooru Infurarẹ́dì
History & Context
History & Context
US 2,043,960, “Electric Welding”, filed 9 October 1935, granted 9 June 1936, assigned to Union Carbide and Carbon Corporation. The named inventors are Lloyd Theodore Jones, Harry Edward Kennedy and Maynard Arthur Rotermund — three men. The process is habitually credited to one, and the third name is regularly misspelled Rothermund. The document settles both points.
Slavyanov got there first, sort of. In the 1890s at Perm he covered the weld pool with a molten slag blanket, for the same reason. The 1936 patent is the industrialised, granular, machine-fed form of an idea that had been floating around since arc welding began — which is a fair description of a good many welding patents.
Why the numbers are so different. Because none of the energy escapes as light or radiated heat, submerged arc welding runs at currents that would be unusable in the open — commonly 300 to 1000 A and, on multi-wire installations, far more. Thermal efficiency approaches 90 per cent against roughly 60 to 70 for open-arc processes, and deposition rates are several times higher than manual stick welding. On thick plate it is not a little faster; it is a different order of magnitude.
Where you have seen it without knowing. Pressure vessels, shipbuilding, wind-turbine towers, structural I-beams and large-diameter pipe are almost all submerged arc welded, usually with the work rotating under a fixed head. It arrived just in time for the Second World War, where it welded ship hulls and armour plate at rates riveting could not approach.
The strange consequence. This is the only common welding process where the operator's protection is not equipment but the process itself. The arc is not shielded from the welder; the welder is shielded from the arc — by the same blanket that shields the weld.
Àwọn ohun-èlò
5- Àyè
- 1 ewéÀyè
- 2 ẹyọÀyè
- 2 kgÀyè
- 1 ewéÀyè
Àwọn Ohun Èlò Ìtọ́nisọ́nà Tí A So Pọ̀

Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà

CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.