IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
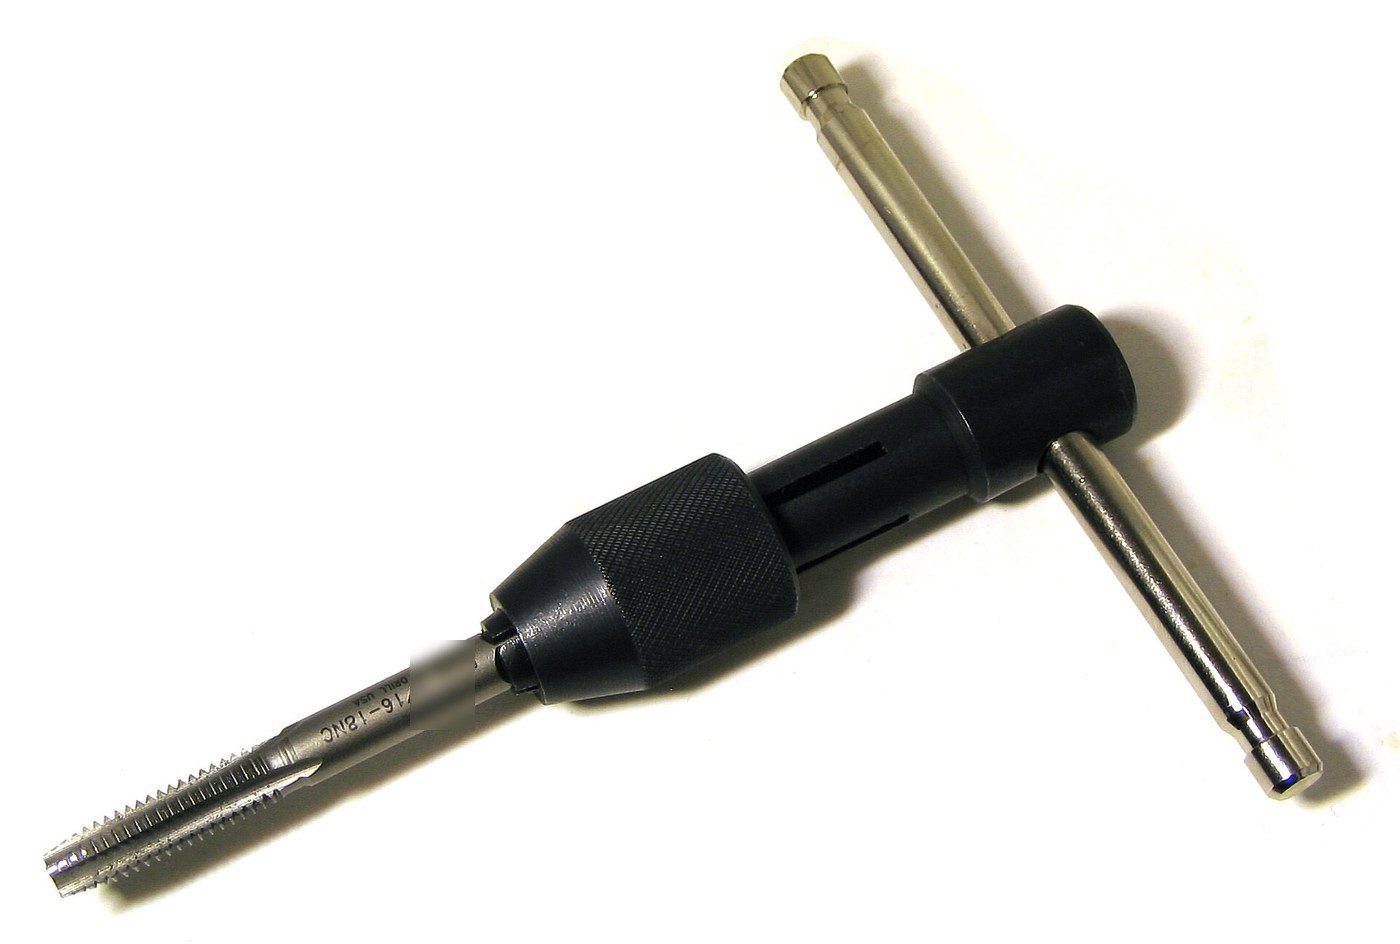

Taps and Dies Cut on the Lathe, with Wrench and Stock
A tap cuts the thread inside a hole; a die cuts it on a rod. Makers made their own in the 16th and 17th centuries. Cut the thread on tool steel in the screw-cutting lathe, file flutes so it cuts, harden it, and use the finished tap to cut the thread in a steel blank that becomes the matching die. A T-wrench turns the tap, a stock holds the die.
The picture: a tap held in a T-wrench.
Ilọsíwájú
Two days for a few sizes
Ìlànà
1
1
Turn and thread the tap
Turn and thread the tap
Turn tool steel to the thread's major diameter with a square on the end for the wrench. Cut the thread in the lathe at the right pitch and check it with the gauge. Taper the first 8–10 threads for a taper tap, or 3–5 for a plug tap.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀pá onígun mẹ́jọ irin irinṣẹ́1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ Ìyí Irin
 Àkójọ Irinṣẹ́ Yíyí Igi HSS
 Ìwọ̀n ihá
 Òṣùwọ̀n Kálípà Díjítà Ìnṣì 6
 Òróró gígé
2
2
Flute and harden the tap
Flute and harden the tap
File three or four lengthwise flutes along the thread so it has cutting edges and room for chips. Harden in water from cherry red and temper to brown.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Omi10 lítà
 Èédú1 as required
Àwọn irinṣẹ́ tí a nílò:
 Ìfá Irin
 Ìdìmú Tábìlì
 Ìléru alágbẹ̀dẹ
 Àpótí ìtutù
 Ẹmú alágbẹ̀dẹ
 Gíláàsì ààbò
3
3
Cut the die with the tap
Cut the die with the tap
Drill a flat tool-steel blank to the tap drill size and run the finished tap through it with oil. Drill clearance holes round the thread so it cuts, saw one side open so it can be set, then harden and temper it to brown.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀pá pẹlẹbẹ irin irinṣẹ́1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
 Ìlù ọwọ́Ìdìmú TábìlìÌfá IrinÌléru alágbẹ̀dẹÀpótí ìtutù
4
4
Wrench and stock
Wrench and stock
Forge and file a T-wrench with a square hole for the tap, and a die stock from flat bar with a round recess for the die, two handles and a set screw.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀pá Pẹrẹsẹ Irin Pẹ́lẹ́1 ẹyọ
Àwọn irinṣẹ́ tí a nílò:
Ìléru alágbẹ̀dẹÌfá IrinÌlù ọwọ́Ìdìmú Tábìlì5
5
Tap drill sizes
Tap drill sizes
Ń ṣí ìwé Jupyter…
Àwọn ohun-èlò
5- Àyè
- 10 lítàÀyè
- 1 as requiredÀyè
- Àyè
- Àyè
Ìtọ́nisọ́nà yìí ń ṣe
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà


CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.