SINING
BEAUTY AT WELLNESS
CRAFTS
KULTURA AT KASAYSAYAN
LIBANGAN
KAPALIGIRAN
PAGKAIN AT INUMIN
REVERSE ENGINEERING
AGHAM
ISPORTS
TEKNOLOHIYA
MGA WEARABLE

Striking and Holding an Arc: Four Things Under Your Hand at Once
An arc is a conducting column of ionised gas. It will not start across a gap on its own at welding voltages, so it is started by touching the electrode to the work and lifting away — the short circuit heats the tip enough to ionise the air above it.
Once lit, four things are under the welder's hand at the same time: the current set on the machine, the length of the arc, the angle the electrode is held at, and how fast it travels. Everything that goes right or wrong in a bead comes out of those four.
This rung is about lighting the arc and holding it steady. Laying a bead with it is the next rung.
Baguhan
3 hours
Mga Tagubilin
1
1
Set the current before you touch the work
Set the current before you touch the work
Current is set by the electrode, not by the plate. The rule of thumb that holds for general-purpose mild steel rods is roughly 30 to 40 amps per millimetre of core diameter:
* 2.0 mm rod — 50 to 80 A
* 2.5 mm rod — 70 to 110 A
* 3.2 mm rod — 100 to 140 A
* 4.0 mm rod — 140 to 190 A
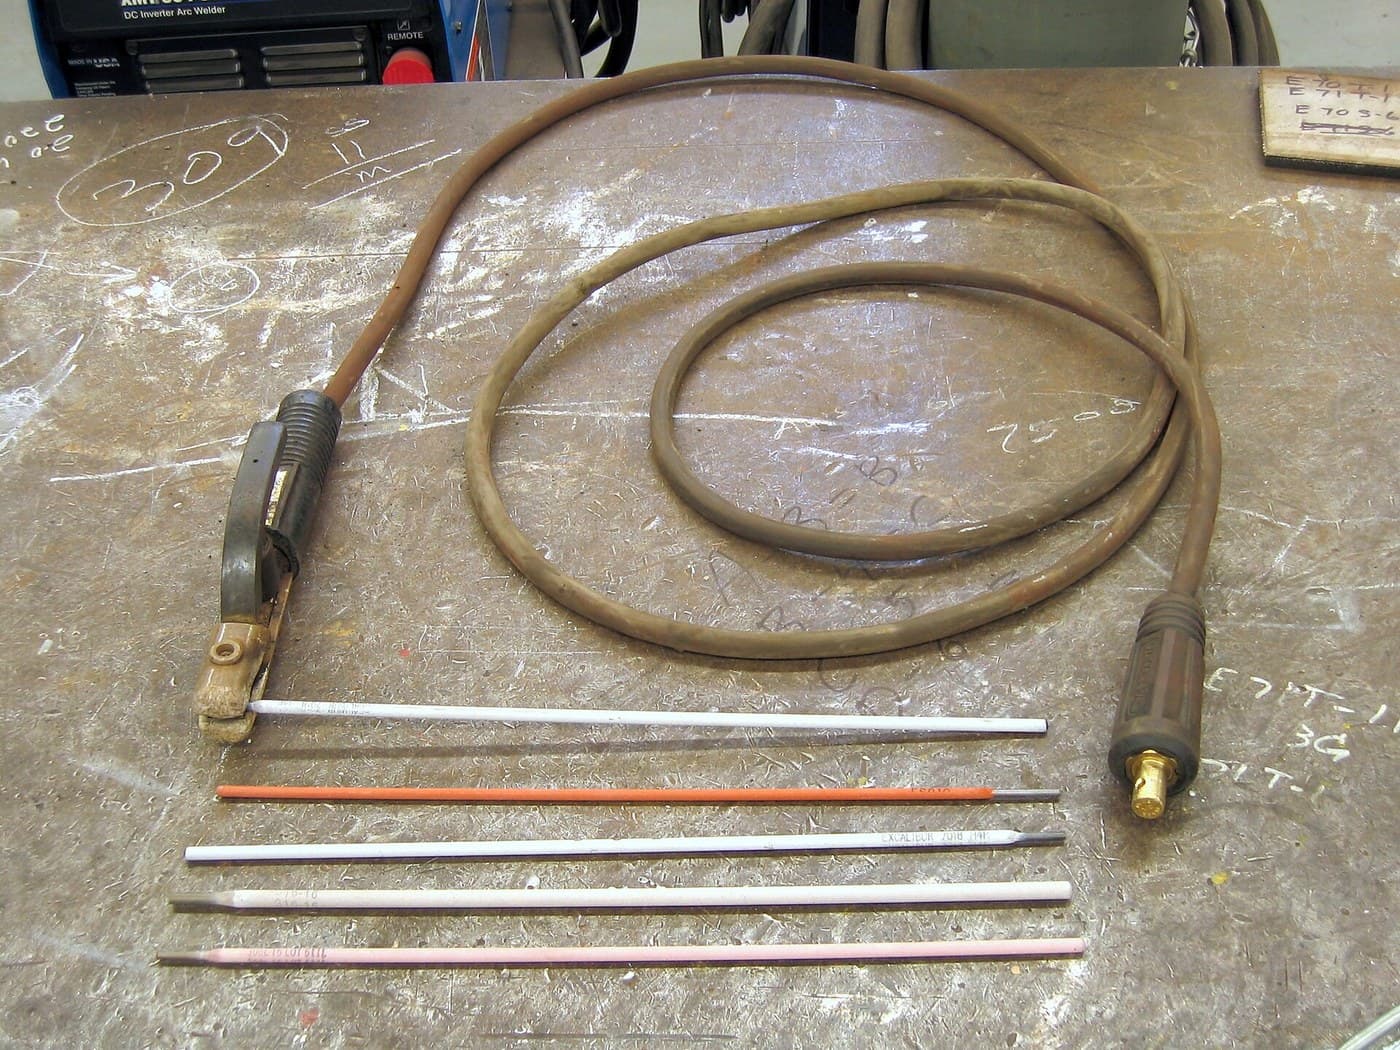
Every box of electrodes prints its own range and that printed range beats the rule of thumb every time.
Start in the middle. Too low and the rod sticks and the arc keeps going out; too high and the rod glows red before it is half used, the pool runs, and the edges of the joint are undercut.
Mga materyales para sa hakbang na ito:
 Elektrodo sa paghihinang1 pakete
Mga kailangang kasangkapan:
 Makinang panghinang na arko
 Helmet sa hinang na kusang nagdidilim
 Mga guwantes sa paghihinang
 Delantal na Katad
2
2
Two ways to strike, and what to do when it sticks
Two ways to strike, and what to do when it sticks
**Scratch start.** Drag the tip across the plate like striking a match, then lift about 3 mm the moment it lights. It is the easier of the two to learn and it leaves a scratch outside the joint, so scratch where the weld will later cover, or on scrap.
**Tap start.** Bring the tip straight down onto the spot, touch, and lift. It starts exactly where you want it, which matters when the bead must begin at a line, but it sticks more often.
It will stick. The rod welds itself to the plate and the machine goes into short circuit. Twist the holder sharply sideways and it usually breaks free. If it does not, release the rod from the holder first — do not stand there pulling while the machine pours current into a dead short — then snap the stuck rod off and chip the stub away.
Sticking on nearly every strike means the current is too low.
Mga materyales para sa hakbang na ito:
Elektrodo sa paghihinang1 pakete Plantsang asero na malambot1 piraso
Mga kailangang kasangkapan:
Makinang panghinang na arkoHelmet sa hinang na kusang nagdidilimMga guwantes sa paghihinang Martilyo
 Set ng brotsang kawad
3
3
Arc length is the one you cannot see yourself getting wrong
Arc length is the one you cannot see yourself getting wrong
Hold the arc about as long as the core wire is thick — 3.2 mm of gap for a 3.2 mm rod. That is the single most useful number in stick welding.
The reason it matters is that arc voltage rises with arc length, so a long arc puts more heat in at the same current, spreads it wider, and lets air at the pool. A long arc sounds hollow and fluttery, throws spatter everywhere, and leaves a wide flat bead with porosity in it.
A correct arc has a sharp continuous crackle, like frying bacon. Learn the sound, because behind a helmet the sound tells you about the arc length faster than the view does.
As the rod burns down, the hand has to feed it in at exactly the rate it is consumed. That is the actual skill, and it is why the first hour is spent running beads on scrap with no joint at all.
Mga materyales para sa hakbang na ito:
Elektrodo sa paghihinang1 paketePlantsang asero na malambot1 pirasoMga kailangang kasangkapan:
Makinang panghinang na arkoHelmet sa hinang na kusang nagdidilimMga guwantes sa paghihinang Pananggalang sa pandinig (earmuff, SNR 30 dB)
4
4
Angle: along the joint, and across it
Angle: along the joint, and across it
Two angles, and they do different jobs.
**Travel angle** is the lean along the direction of travel. For stick welding, drag the rod: tilt the top of the electrode back about 5 to 15 deg from vertical so it trails behind the pool as it moves. Dragging pushes the slag backwards out of the pool. (MIG is the opposite — it is usually pushed — because there is no slag to sweep.)
**Work angle** is the lean across the joint. On a flat butt weld, straight up at 90 deg. On a horizontal fillet in a tee joint, about 45 deg so the heat is shared evenly between the upright and the base; tilt towards one member and that one gets the fusion while the other gets a cold edge.
Getting the work angle wrong on a fillet is the commonest cause of a weld that looks fine and is only attached to one of the two parts.
Mga materyales para sa hakbang na ito:
Plantsang asero na malambot1 piraso Anggulong bakal na malambot na asero1 piraso
Mga kailangang kasangkapan:
Makinang panghinang na arkoHelmet sa hinang na kusang nagdidilimMga guwantes sa paghihinang Digital na Panukat ng Anggulo
Mga Materyales
3- 1 paketePlaceholder
- 1 pirasoPlaceholder
- Placeholder
Mga Kinakailangang Kasangkapan
8- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
Kaugnay na Blueprint
Ang mga blueprint na ito ay nagbabahagi ng kaalaman — mga teknik, materyales, o prinsipyo


CC0 Pampublikong Domain
Ang blueprint na ito ay inilabas sa ilalim ng CC0. Malaya kang kumopya, magbago, mamahagi, at gumamit nang walang pahintulot.
Suportahan ang Maker sa pamamagitan ng pagbili ng mga produkto sa kanilang Blueprint Komisyon ng Maker itinakda ng mga Vendor, o lumikha ng bagong bersyon ng Blueprint na ito at isama bilang koneksyon sa iyong Blueprint upang ibahagi ang kita.