
Pakikipagtulungan
SINING
BEAUTY AT WELLNESS
CRAFTS
KULTURA AT KASAYSAYAN
LIBANGAN
KAPALIGIRAN
PAGKAIN AT INUMIN
REVERSE ENGINEERING
AGHAM
ISPORTS
TEKNOLOHIYA
MGA WEARABLE
Plastic Syringe Set: Moulded Barrel and a Soft Polyethylene Piston
Emma

Nilikha ni

Emma

26. Oktubre 2026SE
13
0
0
0
0

Plastic Syringe Set: Moulded Barrel and a Soft Polyethylene Piston

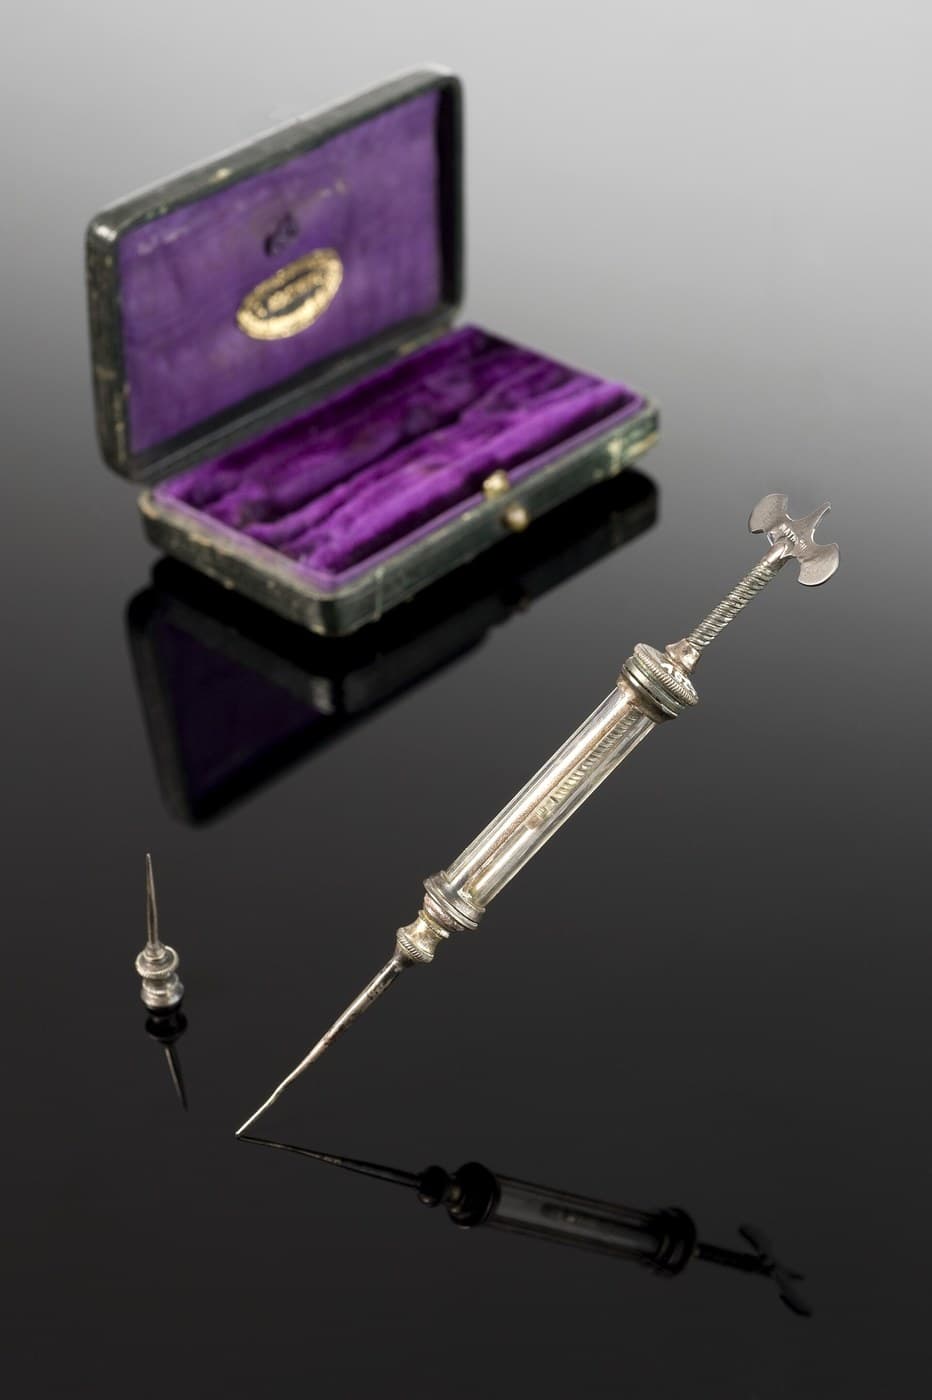
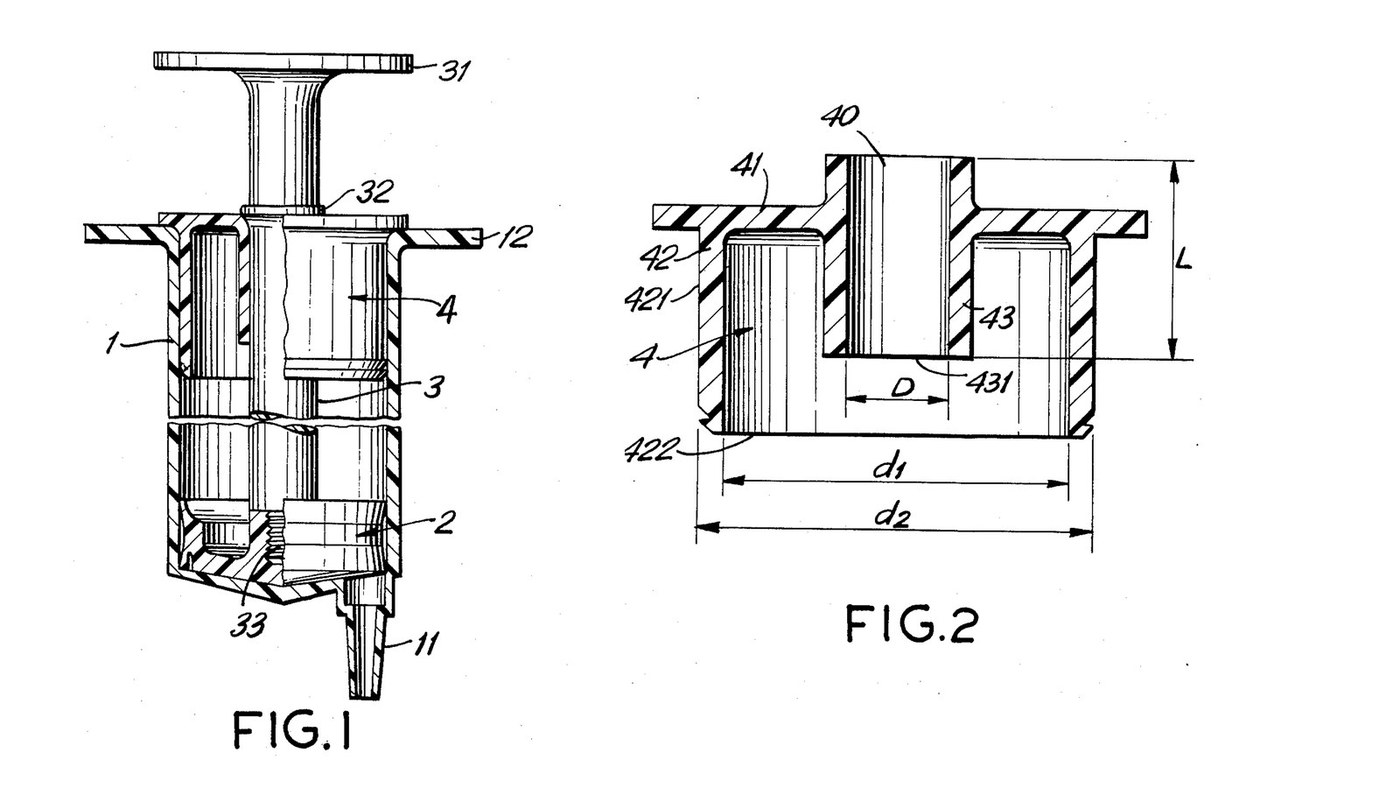
Four moulded parts make a plastic syringe with no rubber seal and no grease: a stiff barrel with a taper nozzle, a bell-shaped piston whose thin polyethylene lips seal against the wall, a slim plunger shaft, and a cap whose long sleeve guides the shaft so it cannot bend and tilt the piston (Adorján & Dávid, US 4,704,105, 1987). Mould one set of moulds per size for a set of syringes for hydraulic models. The piston figures are the patent's. Polypropylene, LDPE, the sizes and the mould making are ours. Not for medical use. The picture: Figs. 1-2.
Abantado
3 days (moulds) + 1 hour per batch

Mga Tagubilin

1

The moulding process

Drying, mould, injection, cooling and inspection all follow this blueprint. The steps below add only what the syringe needs.
2

Mill the barrel mould

Mill a two-plate mould for the barrel (1): a stiff-walled tube closed at one end by a nozzle (11) with a standard needle taper (ours: the Luer taper), and two finger grips (12) at the open end. One mould per syringe size you want, for example 5, 50 and 60 ml (ours).

Mga kailangang kasangkapan:

Makinang panggiling ng metalMakinang panggiling ng metal
Bloke ng aluminyo para sa moldeng iniksiyon (2 plato)Bloke ng aluminyo para sa moldeng iniksiyon (2 plato)
Balangkas ng hulmahan sa iniksiyonBalangkas ng hulmahan sa iniksiyon
3

Mill the piston mould

The piston (2) is a bell: a rim 5-7 mm high whose two edges flare out into lips 0.3-0.5 mm thick, a front groove 0.3-0.5 mm wide and 2-2.5 mm deep, and a central shank. The lips must come out 0.2-0.6 mm wider than the barrel bore; the rim between them no wider than the bore.

Mga kailangang kasangkapan:

Makinang panggiling ng metalMakinang panggiling ng metal
Bloke ng aluminyo para sa moldeng iniksiyon (2 plato)Bloke ng aluminyo para sa moldeng iniksiyon (2 plato)
Balangkas ng hulmahan sa iniksiyonBalangkas ng hulmahan sa iniksiyon
Digital na Kalibrador 6 PulgadaDigital na Kalibrador 6 Pulgada
4

Mill the shaft and cap moulds

Shaft (3): thumb rest (31), a bead (32) and an end projection (33) a little larger than the piston's bore. Cap (4): a disc with an outer collar (42) that force-fits the barrel and an inner sleeve (43) at least as long as the shaft is thick.

Mga kailangang kasangkapan:

Makinang panggiling ng metalMakinang panggiling ng metal
Bloke ng aluminyo para sa moldeng iniksiyon (2 plato)Bloke ng aluminyo para sa moldeng iniksiyon (2 plato)
Balangkas ng hulmahan sa iniksiyonBalangkas ng hulmahan sa iniksiyon
5

Mould the barrels

Mould the barrels from virgin plastic. The patent asks only for a rigid plastic; ours: polypropylene.

Mga materyales para sa hakbang na ito:
Butil na polypropyleneButil na polypropylene1 batch

Mga kailangang kasangkapan:
Pantuyo ng butilPantuyo ng butil
Makina ng injection moldingMakina ng injection molding
6

Mould the pistons

Mould the pistons from virgin polyethylene, which the patent wants at 65-90 degrees Shore (scale not stated). Ours: LDPE; check your grade's data sheet.

Mga materyales para sa hakbang na ito:
Butil na LDPEButil na LDPE1 batch

Mga kailangang kasangkapan:

Pantuyo ng butilPantuyo ng butil
Makina ng injection moldingMakina ng injection molding
7

Mould the shafts and caps

Mould shafts and caps. These may be reprocessed plastic, as they never touch the liquid. Ours: polypropylene.

Mga materyales para sa hakbang na ito:

Butil na polypropyleneButil na polypropylene1 batch

Mga kailangang kasangkapan:

Makina ng injection moldingMakina ng injection molding
8

Check the lip size

Measure the barrel bore and a piston's lips. The lips must be 0.2-0.6 mm wider than the bore. Adjust the mould if not.

Mga kailangang kasangkapan:

Digital na Kalibrador 6 PulgadaDigital na Kalibrador 6 Pulgada
9

Snap the shaft into the piston

Push the shaft's projection through the small bore at the back of the piston until it snaps into the wider cavity behind it.
10

Assemble

Push the piston into the barrel. Thread the shaft through the cap's sleeve and force the cap's outer collar into the open end of the barrel. Its end face now stops the piston when you draw it fully back.
11

Lock the cap

Press two dents, opposite each other, through the barrel wall into the cap collar with a hot tool so the cap cannot pull out. Ours: a soldering iron tip.

Mga kailangang kasangkapan:

De-kuryenteng KautinDe-kuryenteng Kautin
12

Test the seal

Draw water and push it out, along the whole stroke, with no grease. It should move smoothly from the start and not leak past the lips. Note the size and file it into your set.

Mga kailangang kasangkapan:

TubigTubig
Basong Salamin na Pang-aghamBasong Salamin na Pang-agham

Mga Materyales

2

Mga Kinakailangang Kasangkapan

9

Kaugnay na Blueprint

Ang mga blueprint na ito ay nagbabahagi ng kaalaman — mga teknik, materyales, o prinsipyo
CC0 Pampublikong Domain

Ang blueprint na ito ay inilabas sa ilalim ng CC0. Malaya kang kumopya, magbago, mamahagi, at gumamit nang walang pahintulot.

Suportahan ang Maker sa pamamagitan ng pagbili ng mga produkto sa kanilang Blueprint Komisyon ng Maker itinakda ng mga Vendor, o lumikha ng bagong bersyon ng Blueprint na ito at isama bilang koneksyon sa iyong Blueprint upang ibahagi ang kita.

Talakayan

(0)

Mag-login upang sumali sa talakayan

Naglo-load ng mga komento...