فن
خوبصورتی اور تندرستی
دستکاری
ثقافت اور تاریخ
تفریح
ماحول
خوراک اور مشروبات
ریورس انجینئرنگ
سائنسز
کھیل
ٹیکنالوجی
پہننے والے آلات
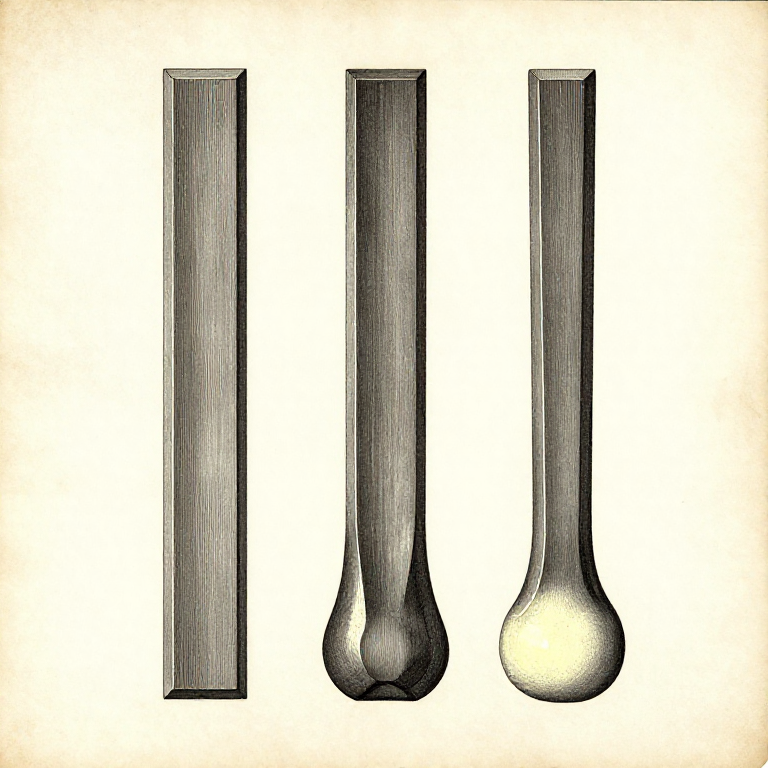


Upsetting: Making It Thicker by Making It Shorter
Upsetting is drawing out in reverse: shortening a bar to make part of it thicker. It is how you get a head on a bolt, a boss in the middle of a bar, or extra material where a joint needs it.
It is also the hardest basic operation, because a hot bar struck on its end wants to BUCKLE sideways rather than compress. Control that and upsetting works; lose it and you get an S-bend that has to be straightened out or cut off.
The answer is localised heat and short unsupported length — the same two levers, used deliberately.
اعلیٰ
3 hours
ہدایات
1
1
Heat ONLY the part you want to thicken
Heat ONLY the part you want to thicken
Bring a short section to a bright forging heat and leave the rest of the bar dark. Cold metal will not move, so the cold section acts as a rigid column and the deformation is confined to the hot part.
This is the heating-evenly rung used in reverse: there you were fighting uneven heat, here you are creating it on purpose. Quench the neighbouring section in water if it has picked up too much heat — a few seconds is enough.
The length of hot metal is what you are controlling. A long hot section buckles; a short one upsets. As a rule of thumb, keep the unsupported hot length under about two and a half times the bar's thickness.
اس مرحلے کے لیے مواد:
 نرم فولاد کی سلاخ1 ٹکڑا
 پانی1 ٹکڑا
درکار اوزار:
 لوہار کی بھٹی
 لوہار کی سنڈاسی
 بھٹی کے لیے گہرے رنگ کی عینک
 لمبے چمڑے کے دستانے
2
2
Strike along the axis, dead square
Strike along the axis, dead square
Stand the bar on end on the anvil face and strike straight down its axis, or hold it vertically and hammer the top. Every blow must be along the length of the bar, not at an angle.
An angled blow bends rather than upsets, and once a bend has started every subsequent blow makes it worse, because the bar is now a lever. Stop at the first sign of it and straighten before continuing.
For a heavy bar, reverse the method: heat the end, then drop the bar end-down onto the anvil so its own weight does the upsetting. The mass of the bar delivers far more energy than a hammer can, and it is automatically axial.
اس مرحلے کے لیے مواد:
نرم فولاد کی سلاخ1 ٹکڑادرکار اوزار:
 نہائی
 لوہار کا ہتھوڑالوہار کی سنڈاسیلمبے چمڑے کے دستانے
3
3
Straighten early and often
Straighten early and often
Check for straightness every few blows by sighting along the bar, and correct any bend immediately while the section is still hot.
A small bend corrected now takes two blows. The same bend after ten more upsetting blows has become a fold, and a fold in hot steel welds shut on itself and becomes a permanent internal flaw — a COLD SHUT — which is a crack waiting to open under load.
That is why upsetting is rated harder than drawing out. Drawing out forgives inattention; upsetting punishes it with a defect you often cannot see until the piece fails.
اس مرحلے کے لیے مواد:
نرم فولاد کی سلاخ1 ٹکڑادرکار اوزار:
نہائیلوہار کا ہتھوڑا پیمانہ
 مکبر لوپ
4
4
Or design so you never have to
Or design so you never have to
The honest professional answer to upsetting is often to avoid it. Start with a bar thick enough for the biggest section and DRAW DOWN everything else, rather than starting thin and upsetting a lump.
That is usually less work, always more controllable, and it is what the volume arithmetic in the drawing-out rung is for: pick the stock from the thickest part of the finished piece.
Upsetting earns its place where the thick section is in the MIDDLE of a long bar, or where drawing down would waste an unreasonable amount of material. Knowing which situation you are in before lighting the fire is the real skill here.
اس مرحلے کے لیے مواد:
نرم فولاد کی سلاخ2 ٹکڑےدرکار اوزار:
 حساب کرنے والا آلہپیمانہ
متعلقہ بلیو پرنٹ
یہ بلیو پرنٹ علم بانٹتے ہیں — تکنیک، مواد یا اصول

CC0 پبلک ڈومین
یہ بلیو پرنٹ CC0 کے تحت جاری کیا گیا ہے۔ آپ اجازت لیے بغیر اس کام کو نقل، ترمیم، تقسیم اور کسی بھی مقصد کے لیے استعمال کرنے کے لیے آزاد ہیں۔
میکر کی حمایت کریں ان کے بلیو پرنٹ کے ذریعے پروڈکٹس خرید کر جہاں وہ میکر کمیشن وینڈرز کی طرف سے مقرر، کماتے ہیں، یا اس بلیو پرنٹ کی نئی تکرار بنائیں اور آمدنی شیئر کرنے کے لیے اسے اپنے بلیو پرنٹ میں کنکشن کے طور پر شامل کریں۔