SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA
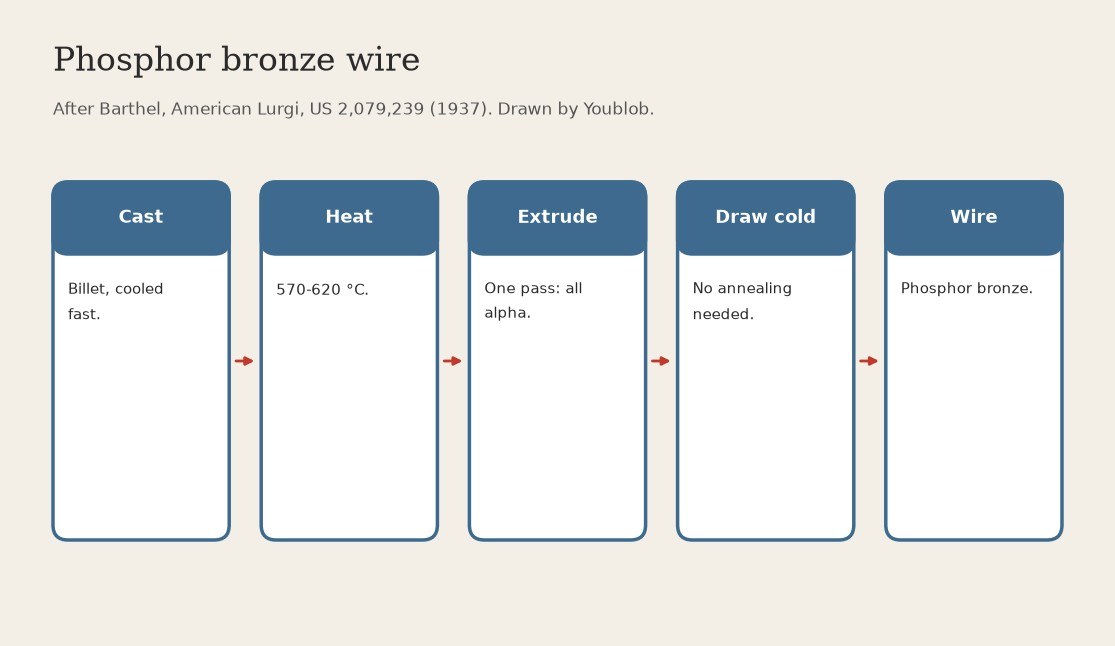

Phosphor Bronze Wire: Cast Billet Extruded at 570-620 °C, then Cold Drawn without Annealing (Barthel, Lurgi, US 2,079,239)
Cast phosphor bronze holds a brittle tin-rich phase that made wire drawing a long round of drawing and annealing. Barthel found that extruding the casting at 570-620 °C kneads it into one soft, even phase, after which it draws straight down to wire.
Result: phosphor bronze wire, drawn without intermediate annealing.
Source: Barthel, US 2,079,239 (American Lurgi, 1937). His temperature is for about 8 % tin; our ingot has about 9 %, so the same range is ours. Not given: extrusion ratio, die sizes. Picture drawn by Youblob.
Zaawansowany
2 days
Instrukcje
1
1
Cast a billet and cool it fast
Cast a billet and cool it fast
Melt the phosphor bronze and cast it into a billet, cooling it rapidly. Ours: cast in an ingot mould and quench.
Materiały do tego kroku:
 Wlewek brązu fosforowego1 as required
Potrzebne narzędzia:
 Tygiel grafitowo-gliniany
 Piec tyglowy
 Kokila do wlewków
 Kadź hartownicza
2
2
Heat the billet to 570-620 °C
Heat the billet to 570-620 °C
Heat the billet to between about 570 and 620 °C (Barthel's range for about 8 % tin and 0.3 % phosphorus). Temperature: 500-650 °C overall; the less tin, the hotter (about 650 °C for 6 % tin).
Potrzebne narzędzia:
 Piec muflowy
 Pirometr
3
3
Extrude it in one pass
Extrude it in one pass
Extrude the hot billet in an extrusion press. The kneading makes the metal even all through, practically all alpha. For thick products with little reduction, cold-press the billet 10-20 % first.
Potrzebne narzędzia:
 Hydrauliczna prasa do wyciskania
4
4
Cold draw to wire without annealing
Cold draw to wire without annealing
Draw the extruded rod cold through dies down to wire; Barthel's metal needs no annealing between draws. Ours: a steel drawplate with drawing lubricant, one hole smaller each pass.
Potrzebne narzędzia:
 Ciągadło stalowe
 Środek smarny do ciągnienia drutu
Materiały
1- 1 as requiredZastępnik
Wymagane narzędzia
9- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
Według tego planu powstaje
Powiązane blueprinty
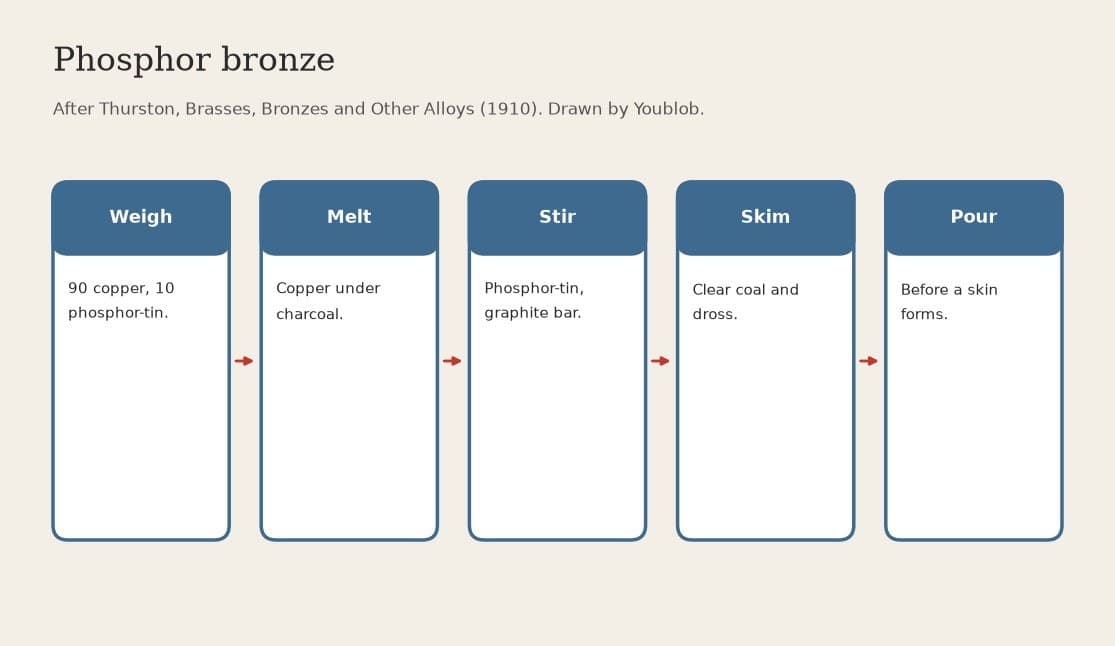
Te blueprinty dzielą się wiedzą — technikami, materiałami lub zasadami
CC0 Domena publiczna
Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.
Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.